Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
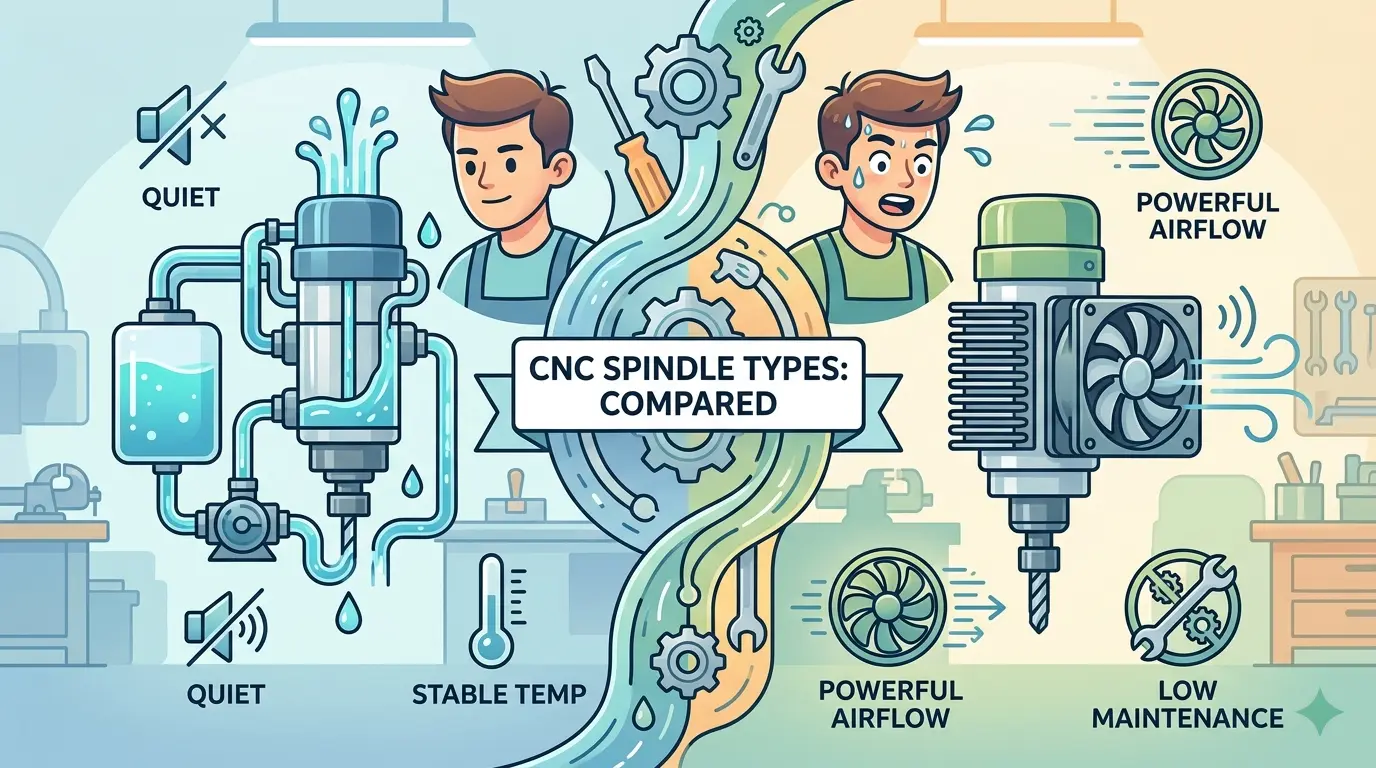
The buying question comes before comparing water-cooled versus air-cooled spindle labels, map the actual duty cycle your shop will impose on the machine. Cooling method determines thermal stability, noise, installation complexity, and which failures surface first, but it cannot compensate for weak workholding, poor tooling, or neglected maintenance. A water loop demands disciplined ownership of pumps, hoses, and coolant quality, while an air-cooled fan reacts differently to dust, enclosure airflow, and ambient heat. The correct choice is the design your production team can keep healthy week after week, not the theoretically superior concept.
Start With The Duty Cycle, Not The Cooling Label
The water-cooled versus air-cooled spindle question usually gets framed as a simple binary, but that framing misses the point. The real question is not which cooling method is more advanced or more industrial. It is which one your shop can actually support over the life of the machine without turning the spindle into a recurring maintenance problem.
Cooling affects thermal behavior, noise, installation complexity, and the types of failures you will see first. It does not make a weak machine strong, and it will not rescue poor tooling, weak workholding, or inconsistent operating habits. A busy panel shop running long routing cycles has a different answer from a prototype room making short sample parts. A compact mixed-material workshop may value simpler ownership more than maximum thermal control. The correct spindle is the one your routine can keep healthy week after week.
Cooling Is Part Of The Ownership Package
Many buyers start thinking about spindle cooling only after they have already chosen table size, machine format, and spindle power. By then the choice often gets reduced to sales language. Water cooling sounds more industrial. Air cooling sounds simpler. Neither phrase is enough.
If you choose water cooling, you are not just buying a spindle. You are buying a loop, a pump or chiller arrangement, hoses, fittings, and a maintenance responsibility. If you choose air cooling, you are accepting fan-based heat rejection, a different local noise profile, and a design that reacts differently to dust, enclosure conditions, and ambient temperature.
Spindle trouble rarely shows up as an abstract engineering debate. It shows up as shop-floor frustration. The spindle runs hot late in the shift. Noise becomes more tiring than expected. A neglected coolant loop creates a preventable failure. An air-cooled spindle inside a dusty enclosure runs warmer than the brochure suggested. The winner is not the theoretically superior concept. It is the design the plant can actually support reliably.
Map The Spindle’s Real Duty Pattern First
Before comparing cooling methods, describe the spindle’s normal day honestly. Does it run in short bursts with long idle gaps? Does it spend hours profiling sheet goods or repeat parts? Is the machine enclosed? Does the room run hot in summer? Are most programs short enough that the spindle gets recovery time, or is the duty pattern heavy enough that heat accumulates across the shift?
These questions matter because thermal behavior is cumulative. A spindle that runs intermittently does not demand the same cooling discipline as one that stays under real load for most of the day. Shops often overestimate how hard the spindle will run when they are still shopping and underestimate how long programs feel once production becomes routine.
A cabinet shop using a router in all-day panel work may care more about long-run stability, operator comfort, and noise accumulation than a prototype room making short sample parts. A compact machine used for sign work, fixture making, or occasional acrylic jobs may benefit more from straightforward ownership than from deeper thermal management. The answer changes with the duty pattern, not with the label.
What Water Cooling Actually Gives You
Water cooling manages sustained heat differently. In the right setup, it can remove heat from the spindle body more effectively over long runs, which makes it attractive for continuous-duty routing, enclosed machines, or environments where spindle-area noise matters. It also appeals to buyers who want a quieter spindle zone because the cooling approach does not rely on an onboard fan the way air-cooled designs do.
Those benefits are real, but they stay real only if the cooling loop is treated like production equipment. Water-cooled spindles reward disciplined ownership:
- The pump has to run correctly.
- Flow has to remain stable.
- Coolant quality matters.
- Hoses and fittings need inspection.
- Seasonal conditions have to be respected.
A careless shop can take a theoretically strong water-cooled spindle and turn it into a service issue that has nothing to do with cutting performance. Water cooling usually makes the most sense when the plant already treats preventive maintenance as normal instead of optional. A shop that already manages spoilboard condition, vacuum reliability, cabinet cleanliness, and tooling discipline is much more likely to benefit from water cooling than a shop that struggles with basic upkeep.
What Air Cooling Actually Gives You
Air cooling stays attractive for the opposite reason: the ownership model is simpler. There is no dedicated coolant loop to install, monitor, and service. There are fewer fittings, fewer leak points, and fewer subsystems to diagnose if a problem appears. For many shops, especially smaller ones, that simplicity is not a compromise. It is the feature.
If the spindle does not live under heavy continuous demand, air cooling can be the smarter economic choice because it removes infrastructure the plant may never use enough to justify. It also tends to be easier for lean maintenance teams, remote shops, and first-time buyers who would rather avoid another layer of commissioning responsibility.
That said, air-cooled does not mean maintenance-free. Fan pathways still need to stay clean. Dust still matters. Ambient heat still matters. Poor enclosure airflow can still create thermal trouble. The difference is that the maintenance burden is usually more straightforward and more familiar. Air cooling asks the shop to keep the machine clean and sensibly installed rather than to manage a second cooling system.
Noise, Dust, And Enclosure Behavior Shift The Decision
Cooling interacts with the room around the machine. Air-cooled spindles usually add more direct fan noise at the spindle. On a loud production floor, that may not matter. In a smaller shop, training room, or quieter prototype area, it may matter much more than the buyer expects. Water-cooled systems often reduce that spindle-area noise, but they do not erase the reality that the machine still lives inside a broader acoustic environment shaped by vacuum pumps, extraction, and general shop layout.
Dust changes the decision too. In woodworking and composite routing, contamination is not a side issue. It shapes reliability. An air-cooled spindle in a poorly managed dusty environment can suffer because the cooling path is only as good as the cleanliness around it. A water-cooled spindle avoids some of that direct fan issue, but only if the coolant loop is maintained well enough not to become its own weak point.
Cooling should be judged in the context of the whole machine package. Hold-down, extraction, enclosure design, and job sequencing may influence spindle life just as much as the cooling method itself. If the real process problem is poor vacuum stability or weak panel support, the cooling choice is not where the battle is being won or lost.
The Most Common Buying Error Is Asking Cooling To Solve A Different Problem
Cooling affects thermal behavior. It does not fix a machine that was weak somewhere else. A poorly trammed spindle, loose collet system, bad toolpath logic, incorrect VFD parameters, or unstable workholding can all produce poor finish, chatter, or burned edges with either cooling type. Buyers who expect water cooling to rescue a bad setup usually end up disappointed. Buyers who blame every thermal symptom on air cooling may be ignoring enclosure airflow, duty cycle, or basic maintenance neglect.
Spindle cooling should be discussed only after the broader spindle package is credible. Machine structure, electrical integration, cable routing, warm-up practice, tooling quality, and chip-load logic all matter first. If those basics are weak, changing the cooling method simply changes the shape of the same problem.
Quote discipline matters here as well. If one machine offers water cooling but the supplier cannot explain loop design, monitoring, or support expectations, that specification is not automatically stronger. A simpler but better-documented air-cooled package may be the safer commercial buy.
When Water Cooling Makes Sense
Water-cooled spindles usually become the better answer when three conditions exist at the same time.
First, the spindle really does run hard enough for sustained thermal control to matter. That means repeated long-duty programs, enclosed-machine heat buildup, or a workload that leaves little idle time for recovery.
Second, the shop values operating calmness enough to care about lower spindle-area noise and steadier long-run thermal behavior.
Third, the team has the maintenance discipline to own the loop with confidence. If nobody wants responsibility for coolant condition, hose checks, pump reliability, or startup verification, the water-cooled advantage becomes much harder to preserve.
When those three conditions are present, water cooling often feels like part of a mature production package rather than an optional upgrade.
When Air Cooling Makes Sense
Air-cooled spindles usually win when the conditions point the other way.
First, the spindle duty pattern is moderate enough that the shop does not need maximum thermal management for long continuous production.
Second, easier installation and simpler service are more valuable than reducing fan noise at the spindle.
Third, the team prefers fewer subsystems to monitor because the business priority is getting the machine installed, running, and supportable without adding a loop that could become another maintenance responsibility.
That makes air cooling especially attractive in lean shops, prototype environments, compact routing setups, and lower-volume production cells where the machine must stay useful without becoming infrastructure-heavy.
Small Routers And Production Cells Should Not Be Judged By The Same Cooling Logic
One reason cooling advice becomes confusing is that people mix very different machine classes together. A desktop or compact router, a small ATC platform, and a production nesting machine do not ask the same thing from a spindle. A buyer evaluating a compact multi-tool machine should think first about whether the broader spindle system fits the workload, not just about whether it is air- or water-cooled. That is where a related question like whether a small ATC spindle really fits the cycle can be more useful than a generic cooling debate.
Likewise, buyers running routers in all-day sign, panel, or cabinet work need to keep cooling in proportion. The spindle matters, but so do feed stability, hold-down quality, extraction, and tool strategy. In those cells, throughput and finish are often shaped as much by process organization as by the cooling method attached to the spindle body.
Put Cooling Into The Quote Review, Not At The End Of The Conversation
Cooling decisions should be made during quote review, not after the machine is already emotionally chosen. Ask exactly what is included. Is the water loop complete? Is flow monitoring included? What startup checks are required? What maintenance intervals are expected? If the package is air-cooled, what assumptions were made about enclosure airflow, duty cycle, and ambient conditions? What support path exists if temperature-related alarms or bearing issues appear later?
These questions belong inside the same diligence process used for any serious machine quote. Buyers should compare not only spindle power and cooling labels, but also commissioning responsibility, electrical requirements, service access, and spare-parts logic. This is the same disciplined review Pandaxis recommends in broader guidance on comparing machinery quotes without missing important details and checking factory-direct machinery offers before committing.
Cooling is one line in that larger ownership calculation. It is not the whole machine.
Choose The Cooling Method Your Shop Can Keep Healthy
Water-cooled spindles are strong when continuous duty, heat control, and operator comfort justify the added infrastructure and the plant is ready to maintain it correctly. Air-cooled spindles are strong when simpler installation, easier ownership, and lower subsystem complexity matter more than maximum thermal control. Neither method is automatically better by itself.
The practical rule is simple: choose the cooling design your shop can keep healthy without heroics. A well-supported air-cooled spindle is better than a neglected water-cooled one. A properly maintained water-cooled spindle is better than an air-cooled package forced into a duty pattern it cannot comfortably support. Once buyers stop treating cooling as a prestige badge and start treating it as an ownership decision, the answer becomes much easier to defend.