Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
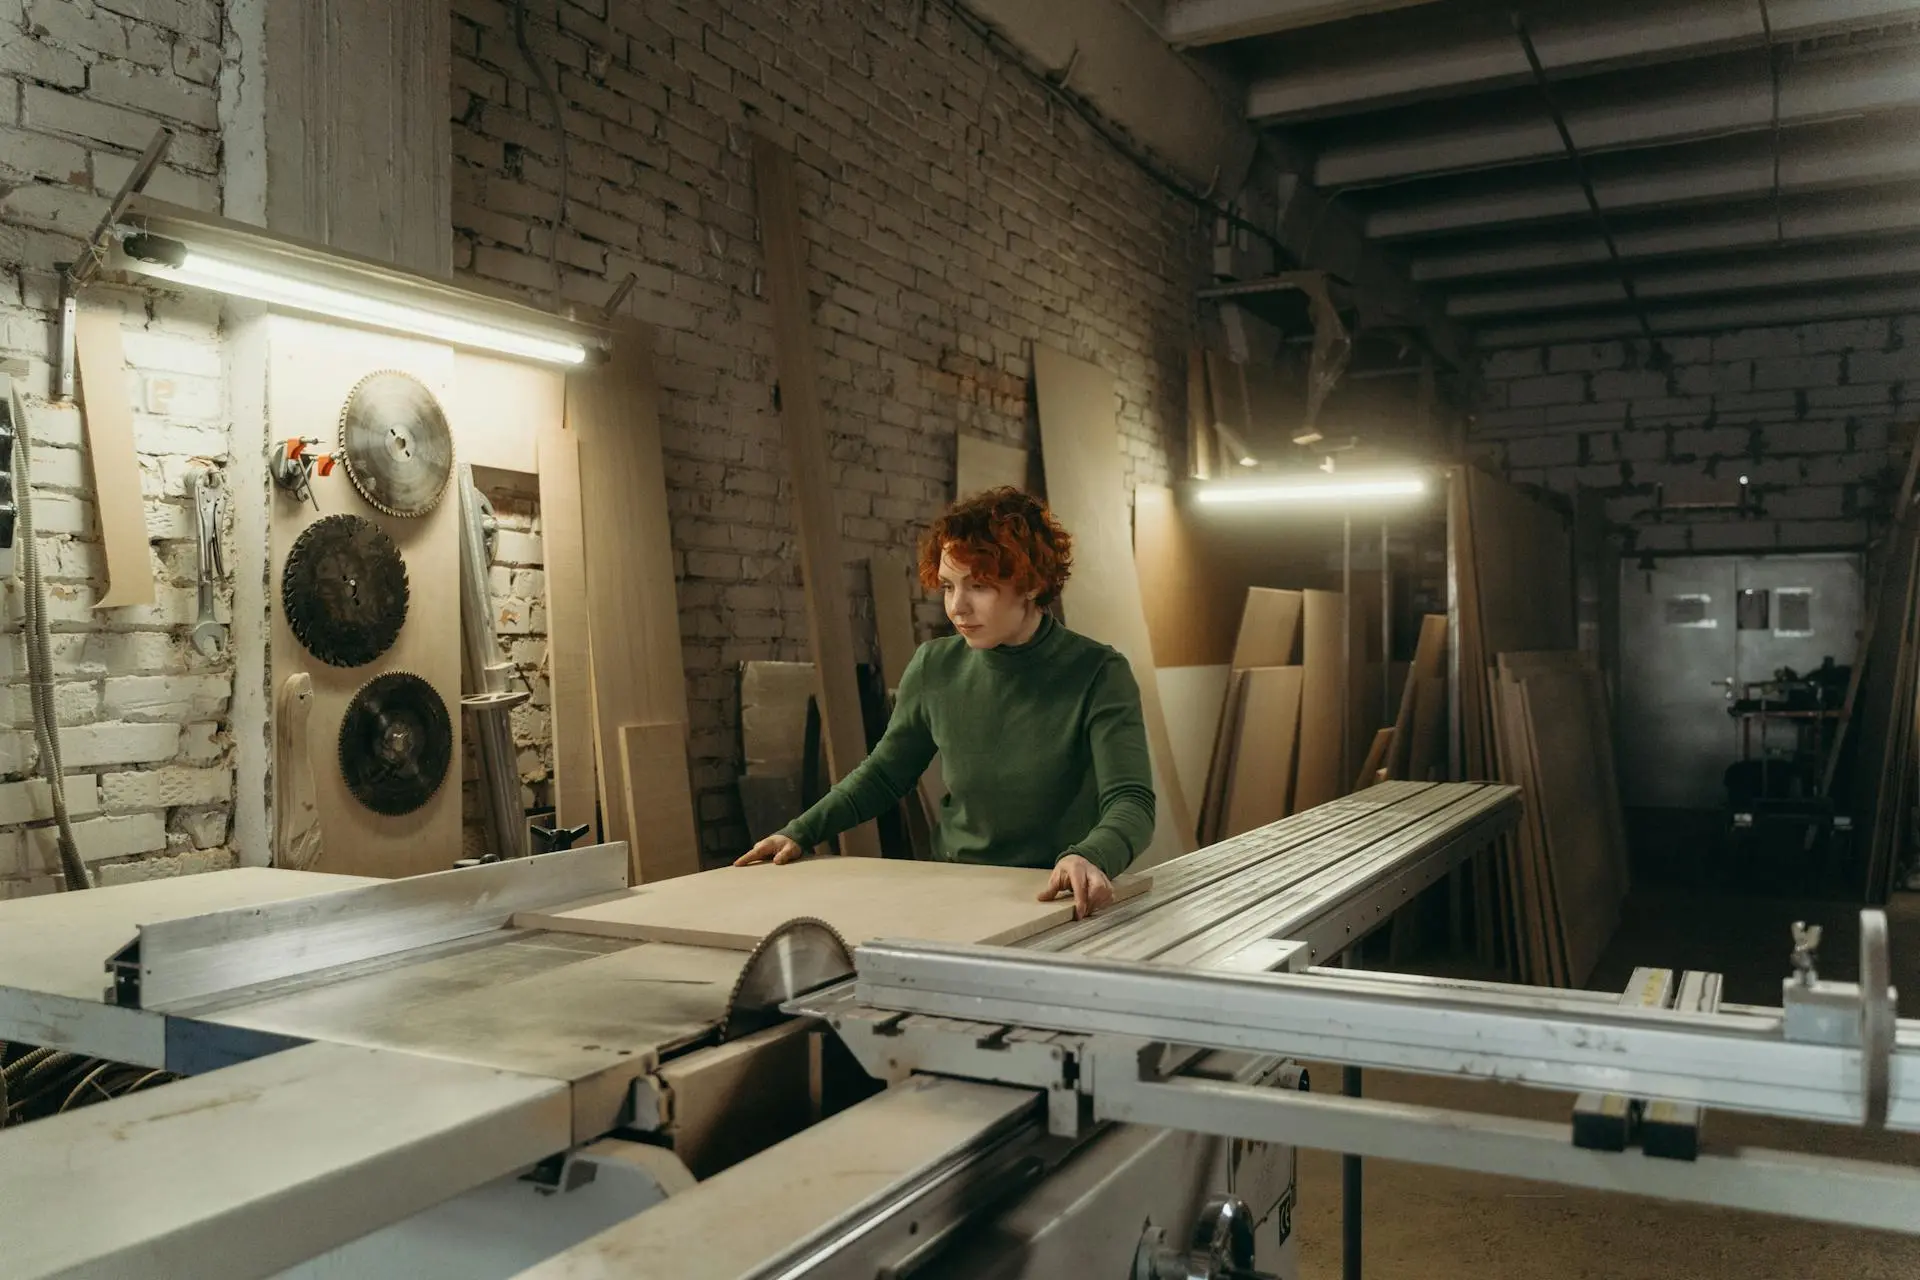
Sliding table saw accuracy failures rarely announce themselves as dramatic machine breakdowns. They surface as a 1 mm oversize panel, a drawer box that binds during fitting, or a miter joint that opens at the outside cornerâsymptoms that only become visible after parts have moved through edging, boring, and assembly. This article addresses the real production problem: accuracy drift is usually a workflow issue, not a machine defect. For cabinet shops, furniture manufacturers, and mixed-material producers, the decision to treat fence verification, blade condition, panel support, and first-part approval as routine disciplines determines whether small errors multiply into costly rework or stay contained at the saw.
Why Sliding Table Saw Accuracy Fails on the Shop Floor
In cabinet, joinery, and furniture production, sliding table saw accuracy problems rarely announce themselves as a dramatic machine failure. They surface as a panel that is 1 mm off size, a component that is not perfectly square, an edge that needs extra cleanup before edging, or an assembly step that suddenly consumes more time than it should. The first sign might be a drawer box that binds during fitting, a cabinet carcass that racks when clamped, or a miter joint that opens up slightly on the outside corner. By the time these symptoms reach the assembly bench, the source of the error is usually buried under several hours of production.
That is why cut accuracy should be treated as a workflow issue, not purely a machine issue. A well-run sliding table saw can support clean, repeatable daily cutting, but only when the reference points, blade condition, panel support, and operator routine are all working together. When accuracy starts to drift, the root cause is often a basic process mistake that has become normalized under production pressure. The saw itself may be perfectly capable of holding tight tolerances; the process around it is what fails.
Understanding how these errors propagate matters. A part that is cut 0.5 mm oversize on the sliding table saw may still pass an initial visual check. But when that part reaches the edgebander, the band may not seat flush. When it reaches the boring machine, the reference edge shifts, and dowel holes land slightly off pattern. When the cabinet goes to assembly, the mismatch shows up as a gap or a forced fit that racks the entire structure. The cost of a small saw error multiplies at every downstream station.
Accuracy Problems Usually Start Before the Cut
Many shops assume accuracy loss begins at the blade. In practice, it often begins earlier: a fence was not rechecked after changeover, a full sheet was poorly supported, a worn blade was left in service too long, or the operator adjusted material position while already committed to the cut. These are not dramatic failures. They are quiet, cumulative errors that build into visible quality problems over the course of a shift.
That matters because sliding table saws are valued for flexibility, not for removing the operator from the process. The same flexibility that makes them useful in mixed-production environments also means accuracy remains sensitive to setup discipline and handling quality. A CNC nesting machine holds position through programmed axes and vacuum hold-down. A sliding table saw depends on the operator to seat the material against the fence, maintain consistent feed pressure, and recognize when something is not right. That is not a weakness; it is the nature of the machine. But it means the shop must build accuracy into the routine rather than expecting the machine to compensate for process gaps.
Consider a typical mixed-production day. The morning run is 18 mm melamine-faced particleboard for cabinet carcasses. Mid-morning, the shop switches to 12 mm plywood for drawer boxes. After lunch, there is a run of solid oak components for a custom job. Each material change brings different blade requirements, different feed behavior, and different chip characteristics. If the operator treats all three runs as the same process, accuracy will drift. The melamine may chip at the exit edge. The plywood may tear out on the cross-grain cuts. The oak may burn if the feed rate is too slow. None of these problems is caused by the saw itself. They are caused by a process that has not been adjusted for the material in front of the blade.
Quick Diagnostic Table for Common Accuracy Problems
| Symptom on the Floor | Common Mistake | Practical Fix |
|---|---|---|
| Parts vary slightly in final size | Fence or stop settings are treated as stable without verification | Recheck reference settings at the start of the shift and after every meaningful changeover |
| Panels are dimensionally correct but not fully square | Material is not seated consistently against the intended reference | Standardize loading position and confirm contact before each cut |
| Edges chip, burn, or require extra cleanup | Blade condition or blade choice does not match the job | Clean, inspect, and replace blades on a schedule tied to material mix and finish expectations |
| Accuracy drops on large sheets | Panel support across the carriage and outfeed is unstable | Improve support before cutting rather than compensating during feed |
| First parts after setup are often reworked | The shop skips first-part approval to save time | Treat the first cut after setup as verification, not production |
| Results differ by operator or by shift | Accuracy depends too heavily on individual correction habits | Build a repeatable setup and checking routine that reduces informal compensation |
This table is not meant to be exhaustive. It is a starting point for troubleshooting. When a shop sees one of these symptoms repeatedly, the fix is usually not a machine adjustment. It is a process correction that removes the source of variation before it reaches the cut.
Mistake 1: Treating Fence Settings as Set and Forget
One of the most common sources of size drift is assuming that yesterday’s fence setting, or even the last job’s setting, is still reliable enough for the next run. In a real factory, changeovers, vibration, rushed setup, or incomplete locking can all introduce small errors that become visible only after several parts have already moved downstream. A fence that is off by 0.3 mm may not be noticeable on the first cut. But when that 0.3 mm error repeats across forty parts, the shop ends up with a batch of components that are all slightly oversize or undersize, and the entire run may need to be reworked or scrapped.
This mistake is especially costly because it can look like a material or operator problem when the real issue is reference control. The operator may compensate by nudging the material slightly, which introduces a different error. The material may be blamed for inconsistent thickness when the real problem is that the fence moved between jobs. The saw may be blamed for poor accuracy when the fence was never locked properly in the first place.
Practical fixes include:
- Verifying fence and stop positions at the start of each shift.
- Rechecking settings after blade changes, maintenance, or heavy repositioning.
- Using a first-part confirmation routine before releasing full production.
- Training operators to treat reference verification as part of throughput, not as a delay.
- Marking frequently used fence positions with reference marks so operators can quickly confirm that the setting has not drifted.
The goal is not perfect calibration theater. The goal is making sure the saw starts the job from a trusted reference instead of from assumption. A 30-second check at the beginning of a run can prevent an hour of rework at the end of the day. In shops that run multiple shifts, this check becomes even more critical because the second shift inherits whatever settings the first shift left behind.
Mistake 2: Running a Blade That No Longer Matches the Job
Factories sometimes talk about accuracy as if it were purely geometric, but edge quality and cut stability matter just as much in real production. A dull blade, a dirty blade, or a blade that is poorly matched to the panel surface and finish standard can create chipping, burning, unstable feed behavior, and apparent dimensional inconsistency. The blade is the point where the machine meets the material, and if that interface is compromised, nothing else in the process can fully compensate.
In those situations, operators often try to correct the result by changing feed style or applying more attention during the cut. That usually hides the real cause instead of fixing it. A dull blade may still cut, but it cuts with more resistance, more heat, and more tear-out. The operator slows down to control the cut, which increases heat and burn. The material surface degrades, and the part may even change dimension slightly as the blade deflects under load. None of this is visible as a dramatic failure, but it all shows up in the final product.
Practical fixes include:
- Matching blade condition to the material mix actually being processed.
- Cleaning resin, dust, and buildup before they begin affecting cut behavior.
- Replacing worn blades before quality loss becomes normalized.
- Reviewing blade strategy whenever the shop switches between laminated board, plywood, MDF, or solid wood tasks.
- Keeping spare blades on hand so a dull blade can be swapped out immediately rather than run until the end of the shift.
Blade selection also matters. A blade designed for ripping solid wood has a different tooth geometry than a blade designed for cross-cutting melamine-faced panels. A combination blade may work acceptably for mixed use, but it will not deliver the same edge quality as a dedicated blade for each material class. Shops that run a wide variety of materials should maintain a small inventory of blades matched to their most common jobs, rather than relying on one blade to do everything.
The right blade routine does not make a sliding table saw universally better than other cutting systems. It simply protects the accuracy and finish level the machine is capable of delivering in flexible production. A sharp, clean, correctly matched blade is the cheapest accuracy upgrade a shop can make.
Mistake 3: Letting Material Support Carry the Accuracy Risk
Large panels, narrow parts, and mixed-size components all behave differently on a sliding table saw. When support across the carriage, side table, or outfeed is inconsistent, the workpiece can sag, rotate slightly, or shift under feed pressure. The operator may still complete the cut, but squareness and repeatability start to depend on manual compensation rather than on controlled movement.
That is one reason accuracy often becomes less stable on full sheets or awkward parts, even when the saw itself seems mechanically sound. A 2440 mm by 1220 mm sheet of 18 mm particleboard weighs roughly 40 kg. If that sheet is only supported at the carriage and the outfeed table is slightly low, the unsupported end will sag. The sag may be only a few millimeters, but it is enough to change the angle of the cut relative to the reference edge. The part may come off the saw looking acceptable, but it will not be perfectly square, and the error will show up when the part reaches assembly.
Practical fixes include:
- Confirming that large panels stay properly supported through the full cut path.
- Adjusting support strategy for heavy, long, or unbalanced parts before production begins.
- Avoiding rushed handling that forces the operator to fight gravity and alignment at the same time.
- Separating support problems from machine problems during troubleshooting.
- Checking that outfeed tables and roller stands are level with the saw table surface before starting a run.
Narrow parts present a different challenge. A 60 mm wide strip cut from a full sheet may flex during the cut, especially if the operator is pushing from the carriage side and the strip is unsupported on the outfeed. The fix is not to push harder; it is to provide adequate support so the strip does not flex in the first place. Some shops use a dedicated support table or a secondary fence for narrow ripping operations.
If the workpiece is unstable, the cut is already at risk before the blade enters the material. The operator cannot compensate for a sagging panel by pressing harder or adjusting feed speed. The support structure must be correct before the cut begins.
Mistake 4: Correcting the Cut Mid-Feed Instead of Fixing the Setup
Another frequent mistake is allowing skilled operators to rescue unstable cuts by changing hand pressure, feed behavior, or body position in real time. Experienced people can often keep production moving that way for a while, but it creates accuracy that depends on individual judgment rather than on process control.
That usually leads to a familiar pattern: one operator gets acceptable results, another struggles, and management concludes that the problem is inconsistency in labor rather than inconsistency in the setup. In reality, the setup is marginal, and the skilled operator is compensating for it through experience. The less experienced operator does not know how to compensate, so the errors become visible. The shop blames the operator instead of fixing the setup, and the problem persists.
Mid-feed corrections are particularly dangerous because they are reactive. By the time the operator notices that the material is shifting or the cut is not tracking straight, the blade is already engaged. Trying to correct the feed at that point can cause the blade to bind, the material to kick, or the cut to deviate further. The safe response is to stop the feed, back the material out if possible, and address the root cause before attempting the cut again.
Practical fixes include:
- Standardizing how material is referenced before feed begins.
- Stopping the process when binding, lift, or instability appears early in the cut.
- Reviewing operator movement and loading habits as part of accuracy control.
- Removing informal workarounds that only function under one experienced operator.
- Documenting the correct feed sequence so all operators follow the same steps.
Sliding table saws are commonly chosen because they preserve operator control. That does not mean they should rely on operator improvisation. The operator should control the cut through a consistent, repeatable routine, not through real-time corrections that vary from person to person and from part to part.
Mistake 5: Skipping First-Part Verification After Every Real Change
When the shop is busy, first-part checking is often the first discipline to disappear. Teams assume the next run will behave like the last one, especially if the machine was cutting well earlier in the shift. But blade changes, new panel batches, altered dimensions, or different cut sequences can all introduce small changes that only become obvious after rework begins to accumulate.
A blade change is an obvious trigger for first-part verification, but it is not the only one. A new batch of panels from a different supplier may have slightly different thickness or surface characteristics. A change in cut sequence may place different demands on the fence or the support system. A dimension change may require the operator to reposition the fence, and that repositioning may introduce a small error that is not visible until the part is measured.
Practical fixes include:
- Requiring first-part approval after every meaningful setup change.
- Checking size, squareness, and edge condition before full release.
- Treating first-part verification as protection for throughput, not as an administrative step.
- Tracking where rework begins so repeated changeover errors become visible.
- Using a simple check gauge or template for frequently repeated dimensions so verification takes seconds rather than minutes.
The first part after a changeover is not production; it is verification. If the shop treats it as production, the first several parts may all carry the same error, and the entire batch may need to be reworked. A 30-second check of the first part can prevent that outcome. This is one of the simplest ways to protect downstream edging, boring, assembly, and final fit.
Mistake 6: Ignoring the Fence and Carriage Relationship
Beyond the basic fence setting, the relationship between the fence and the carriage deserves attention. The fence must be parallel to the blade and perpendicular to the table surface. If the fence is slightly out of parallel, the part will be cut with a taper, even if the fence setting is correct at the front of the blade. If the fence is not perpendicular to the table, the part may stand slightly off vertical, which becomes visible when the part is placed on a flat surface or when it is joined to another component.
Carriage wear is another factor. The sliding table moves on bearings or guides, and if those components wear unevenly, the carriage may not track perfectly straight. This can cause the cut to deviate slightly from the intended line, especially on longer cuts. Regular maintenance of the carriage system, including cleaning and lubrication, is essential to maintaining accuracy over the life of the machine.
Practical fixes include:
- Checking fence parallelism to the blade at regular intervals.
- Verifying that the fence face is straight and free of damage.
- Cleaning and lubricating the carriage guides according to the manufacturer’s schedule.
- Inspecting the carriage for play or looseness that could affect tracking.
- Having a qualified technician check the machine geometry if accuracy problems persist after process corrections.
These checks are not difficult, but they require discipline. In a busy shop, it is easy to assume that the machine geometry is stable because it was stable last month. But wear, vibration, and accidental impacts can all change the geometry over time. A periodic check of the fence-carriage relationship is a low-cost way to catch problems before they become quality issues.
Mistake 7: Blaming the Saw When the Real Problem Is Workflow Fit
Not every accuracy complaint means the machine is being maintained poorly or operated badly. Sometimes the saw is being asked to carry a production pattern that no longer fits its strongest use case.
If the factory increasingly runs repeated rectangular panel sizing at sustained volume, management may notice that accuracy pressure rises because the process depends on constant manual handling and repeated reference checks. In that case, the question is no longer only how to tune the sliding table saw. The better question is whether the front-end cutting workflow should become more process-driven.
That is where dedicated panel saws often enter the discussion. A sliding table saw remains a strong choice for custom work, mixed materials, short runs, and operator-led flexibility. A more dedicated panel-cutting system is often better suited to repeated, high-volume sizing where consistency across shifts matters more than cut-by-cut adaptability.
This tradeoff should be discussed honestly. The sliding table saw is not less valuable because another system may fit a different production pattern better. It simply means accuracy problems sometimes come from a mismatch between workflow and machine category, not from one bad adjustment.
Consider the production pattern. A shop that cuts fifty different part sizes per day, with frequent material changes, is well served by a sliding table saw. The operator can adjust quickly, and the flexibility of the machine matches the variability of the work. A shop that cuts the same twenty part sizes every day, with long runs of each, may find that the sliding table saw requires too much manual attention to maintain consistency. The same machine that is an asset in the first shop becomes a bottleneck in the second.
The decision to move to a different machine category should be based on production data, not on frustration. Track the number of changeovers per shift, the average run length, the rework rate, and the time spent on setup and verification. If the data shows that the shop is spending more time managing the process than cutting parts, it may be time to consider a more automated approach.
Build an Accuracy Routine Instead of Chasing Isolated Errors
Shops usually improve faster when they stop treating every bad cut as a separate event. A more reliable approach is to build a short routine that protects accuracy before volume starts.
A practical routine usually includes:
- Clean reference surfaces before production starts.
- Verify fence and stop accuracy before releasing the first job.
- Match blade condition to the material and finish requirement.
- Confirm stable support for full sheets and awkward parts.
- Approve the first part after each real setup change.
- Stop and troubleshoot recurring drift instead of normalizing compensation.
- Check the fence-carriage relationship on a regular schedule.
- Document the routine so all shifts follow the same steps.
This kind of routine matters because accuracy is cumulative. Small, repeated mistakes at the saw do not stay at the saw. They move into edge banding, drilling, fitting, assembly, and delivery. A part that is 0.5 mm off at the saw may require an extra pass at the edgebander, a shim at assembly, or a rework at final fit. Each of those corrections consumes labor and time that could have been avoided with a better routine at the saw.
The routine does not need to be elaborate. It needs to be consistent. A shop that checks the fence at the start of every shift, verifies the first part after every changeover, and keeps the blade clean and sharp will catch most accuracy problems before they become quality issues. The routine becomes part of the production process, not an interruption to it.
Production Takeaway: Sliding Table Saw Accuracy
Most sliding table saw accuracy problems come from ordinary mistakes that become invisible through repetition: unverified fence settings, blade neglect, weak panel support, mid-cut correction habits, and skipped first-part checks. None of those problems is especially complicated, but each one can quietly undermine repeatability, cut quality, and downstream efficiency.
For shops that depend on flexible daily cutting, the most effective fix is usually not a dramatic machine intervention. It is a tighter process around references, blades, support, and verification. When those basics are controlled, a sliding table saw is well suited to delivering cleaner, more dependable results in custom and mixed-production environments. When accuracy pressure keeps growing even after the routine improves, that is often the point where the shop should reassess whether the cutting workflow still matches the machine category.
The sliding table saw remains one of the most versatile cutting tools in woodworking. It handles solid wood, panels, laminates, and plastics. It supports custom work and short runs. It gives the operator direct control over the cut. But that control comes with responsibility. The operator and the shop must manage the process around the machine, or the machine will not deliver the accuracy it is capable of. A disciplined routine, a clean blade, and a stable setup will protect accuracy far more effectively than any single adjustment or upgrade.
For shops evaluating their cutting workflow, the sliding table saw is worth keeping in the mix for its flexibility and control. The key is to treat accuracy as a process outcome, not a machine feature. When the process is right, the saw delivers. When the process drifts, the saw gets blamed. The fix is usually not the machine; it is the routine around it.