Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
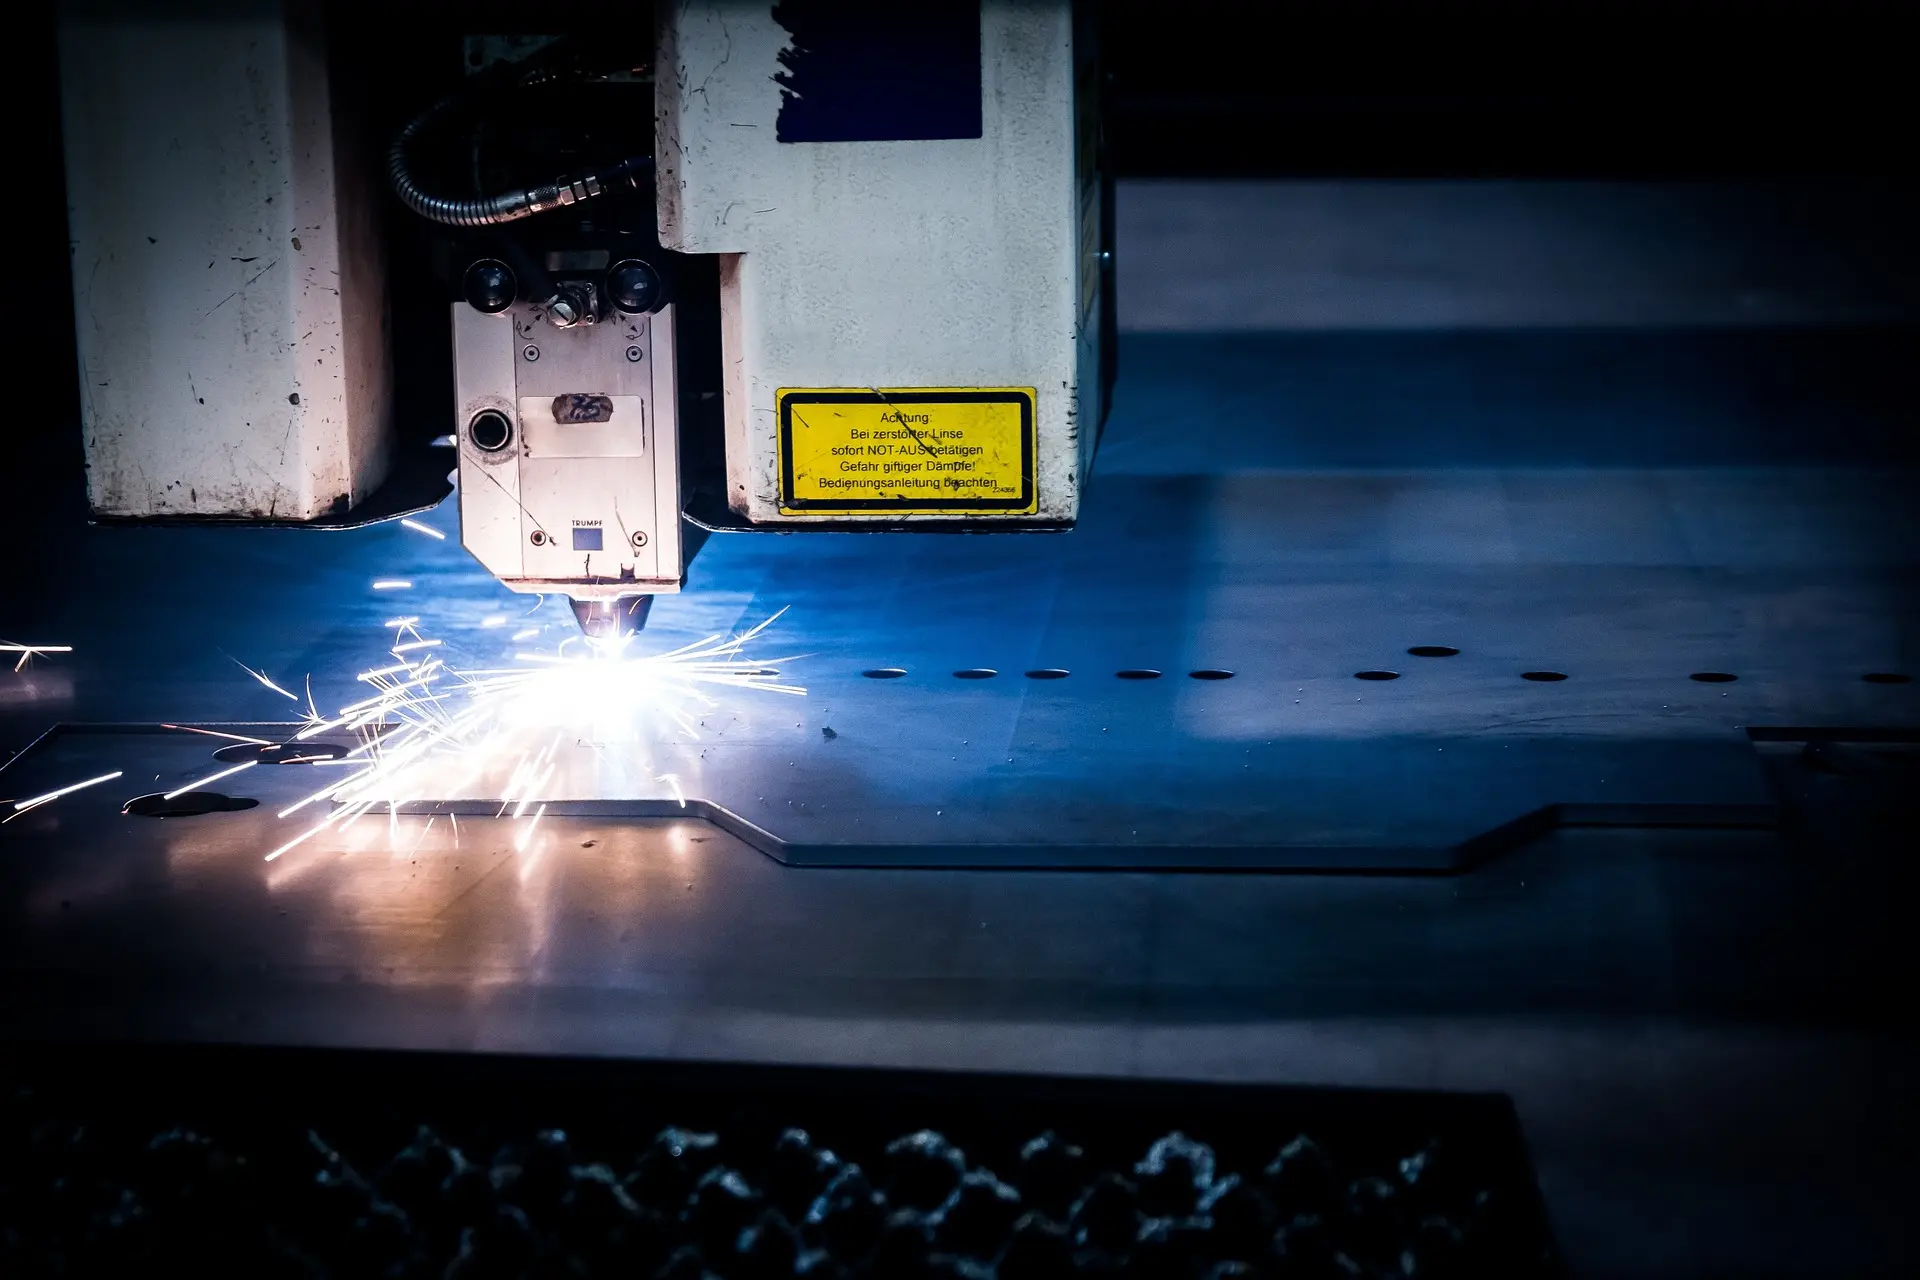
Comparing laser cutter quotations by wattage alone is a trap that leads to costly missteps in production planning. Two machines with identical power ratings can differ dramatically in price because of what they were actually built to do—frame rigidity, motion control, working area, extraction, cooling, and automation all shift the real cost, both upfront and across the machine’s working life. This guide breaks down the cost drivers that matter most, from material fit and edge quality expectations to hidden expenses like installation, consumables, and training. The goal is to help you compare quotes on total cost of ownership, not headline price, so the machine you select actually matches your production load and protects schedule reliability.
Why Laser Cutter Quotes Vary So Widely
Two laser cutting machines can carry similar power ratings and still land at dramatically different price points. The gap usually comes down to what the machine was actually built to do. A unit designed for occasional short-run cutting of thin acrylic or light engraving work has a fundamentally different cost structure than one expected to run repeat jobs across full shifts with stable output and minimal rework.
The mistake many shops make is comparing base quotations as if they were buying a commodity. Power is only one variable. Working area, frame rigidity, motion control, extraction, cooling, automation, and the support package behind the machine all shift the real cost—both upfront and over the machine’s working life.
The Cost Drivers That Matter Most
| Cost Driver | Lower-Cost End | Higher-Cost End | Why It Changes Price |
|---|---|---|---|
| Laser Type and Application Fit | Light-duty cutting and engraving for simple non-metallic workflows | Systems built for faster output, larger parts, or broader material demands | Source type, optics, cooling, and machine build all shift with the target application |
| Working Area | Small-format beds for compact parts | Large-format beds for sheet handling or batch work | Bigger machines need heavier frames, longer rails, stronger extraction, and more floor space |
| Motion and Frame Quality | Basic movement systems for light use | More rigid frames and more stable motion control | Better repeatability, smoother edges, and lower vibration come from stronger machine construction |
| Automation Level | Manual loading, unloading, and setup | Dual tables, conveyors, feeding systems, or workflow aids | Automation raises initial cost but reduces labor, handling time, and bottlenecks |
| Supporting Equipment | Minimal accessories | Full extraction, cooling, enclosure, and safety package | Stable production usually depends on more than the beam source alone |
| Software, Service, and Training | Base machine with limited onboarding | Better training, spare-parts planning, and support response | Faster ramp-up and lower downtime often justify a higher quote |
Start With Material Fit, Not Wattage
The first pricing decision is not about power. It is about what the machine will process day to day. Machines aimed at light non-metallic cutting and engraving—wood, acrylic, MDF-faced decorative components, display parts, signage—sit in a different price band from systems configured for heavier workloads or more demanding industrial output.
The source type, optics package, cooling requirements, and chassis design all change based on the intended application. A machine that cuts 3 mm acrylic cleanly may struggle with thicker material or produce charred edges on certain woods if the optics and extraction were not specified for that work.
Buyers should define the material range and job types before comparing quotes. If the real workload is wood, acrylic, or similar non-metallic sheet goods, the pricing logic should center on clean edges, stable motion, extraction, and repeatable detail. If the intended use moves into a different material category, the cost structure changes with it.
How Material Thickness and Edge Quality Shift the Quote
Material thickness is one of the most underweighted variables in laser cutter comparisons. A machine that handles 3 mm acrylic with clean edges may produce unacceptable charring on 10 mm material if the optics, focal length, and assist-gas setup were not configured for deeper cuts. The difference is not simply wattage. It is the combination of beam delivery, lens selection, and the machine’s ability to maintain focus across the full depth of cut.
Edge quality expectations also drive cost. A shop producing display components where edges are visible to end customers needs a machine that delivers consistent, clean cuts without secondary sanding or polishing. That requires better motion control, more stable beam delivery, and extraction that clears vapor from the cut zone before it re-deposits on the surface. These requirements push the specification upward, and the price follows.
Conversely, a shop cutting internal components where edges are hidden in assembly may tolerate slightly rougher cuts. That shop can often specify a simpler machine and save money without compromising the final product. The key is knowing which edges matter and which do not before you compare quotes.
Working Area and Frame Rigidity Drive the Quote Up Fast
Once the application is clear, the next pricing jump comes from machine format. A larger working area almost always raises cost. The reason is mechanical, not arbitrary: a bigger bed needs a stronger frame, longer travel components, better flatness support, and more robust extraction and motion control.
Processing larger sheets or nesting more parts per cycle is not just about extra cutting area. It is about the structural stability required to keep that area useful. A machine that flexes during rapid direction changes produces inconsistent cuts across the bed. That shows up as edge variation, corner rounding, or unstable engraving detail—problems that cost time and material to correct.
Frame quality matters for the same reason. A lighter machine can look attractive on paper, but rigidity affects vibration, cut consistency, and repeatability across longer runs. In production, that translates to more operator intervention and more rejected parts.
Motion system quality also changes the price because it changes the result. Better control over acceleration, direction changes, and positioning supports cleaner detail, less scrap, and more predictable output. Two quotations may list similar power levels while the real difference sits in how the machine moves, not just how the beam is generated.
The Real Cost of Bed Size: Floor Space, Extraction, and Material Handling
Bed size affects more than the machine price tag. A larger working area demands more floor space, which may require reorganizing the production floor or expanding the facility. It also requires a more powerful extraction system to handle the larger cutting area, since smoke and fumes must be cleared from a bigger volume. Ducting runs get longer, filter capacity increases, and the electrical load grows.
Material handling is another hidden cost tied to bed size. A small-format machine can be loaded by hand with minimal effort. A large-format machine handling full sheets often needs a loading table, lift assist, or conveyor to move material efficiently. That equipment adds cost and takes up additional floor space. Shops that process full sheets should factor these handling costs into the comparison, not just the machine price.
For shops that process a mix of part sizes, a mid-format bed may offer the best balance. It handles most jobs without the expense of a full-sheet system, and it keeps material handling simple. The right bed size is the one that matches the actual part mix, not the largest sheet the shop occasionally processes.
Automation and Supporting Systems Add Cost for a Reason
In many shops, the difference between a basic laser cutter and a more expensive system is not the beam source alone. It is the amount of workflow support built around it. That may include:
- Conveyor or pass-through handling for continuous material flow
- Dual work areas or faster part changeover arrangements
- More stable cooling and smoke extraction support
- Better enclosure and safety design
- Autofocus or easier setup features that reduce operator variability
- Software features that make nesting, job setup, or repeat work easier to manage
These features increase capital cost, but they often lower labor cost and downtime. A machine that saves only a few minutes per job can materially improve output over a month if the production schedule is busy.
Extraction and cooling are easy to treat as accessories until poor fume removal, heat instability, or inconsistent cutting starts interrupting jobs. A laser cutter that cannot clear smoke from the cutting path produces hazy edges and slower processing. A cooling system that cannot hold stable temperatures causes power drift and inconsistent results across a shift.
Why Dual-Table and Pass-Through Configurations Change the Economics
For shops running repeat jobs, the difference between a single-table and dual-table machine can be significant. A dual-table configuration allows the operator to unload and reload one table while the other is cutting. That overlap eliminates the dead time between jobs, which is often longer than the cutting time itself for small parts.
Pass-through configurations add another level of flexibility. They allow material to feed continuously through the machine, which suits shops processing long runs of identical parts or material that arrives in roll form. The cost increase over a basic machine is real, but so is the throughput gain. A shop that runs the same part repeatedly can often justify the higher price through reduced labor and faster cycle times.
The decision comes down to job mix. A shop with highly varied work may not benefit from automation that is optimized for repeat runs. A shop with steady production of similar parts will see the payback quickly. Evaluate the actual job mix before deciding whether automation features are worth the premium.
Hidden Costs Often Decide Whether the Machine Is Actually Affordable
This is where many buying decisions go wrong. Buyers compare the headline machine price, but the total spend depends on everything required to make that machine run well in a real factory or workshop environment.
The hidden-cost checklist usually includes:
- Shipping, installation, and site preparation. A machine may need more power planning, ventilation layout, or floor allocation than expected.
- Extraction, cooling, and safety equipment. Some quotations separate these items instead of bundling them.
- Consumables and wear items. Lenses, mirrors, filters, nozzles, and routine maintenance items affect running cost.
- Training and process ramp-up. A cheaper machine can become expensive if setup inconsistency slows production.
- Spare parts and support response. Downtime is rarely cheap when orders are scheduled tightly.
- Scrap and rework. If cut quality or repeatability is unstable, the machine is costing more than its purchase price suggests.
Total cost of ownership matters more than the entry quote. The machine price starts the conversation, but operating stability usually decides whether the purchase was economical.
Consumables and Maintenance: The Recurring Cost That Compounds
Laser cutters consume more than electricity. Lenses and mirrors degrade with use and require periodic replacement. Filters in the extraction system need changing based on cutting volume and material type. Nozzles wear and affect gas flow and cut quality. These items are not expensive individually, but they add up over a year of production.
Maintenance intervals also differ between machine classes. A basic machine may require more frequent alignment checks and adjustments. A higher-end system with more stable construction holds alignment longer, which reduces downtime and the labor cost of maintenance. Shops running multiple shifts should weigh these differences carefully, since maintenance hours directly reduce available production time.
The material being cut also affects consumable life. Cutting materials that produce heavy residue or abrasive particles will shorten filter and lens life. Shops processing such materials should budget for more frequent replacement and factor that into the operating cost comparison.
How to Compare Quotes Without Missing the Real Decision
The best way to compare laser cutting quotations is to force every supplier comparison back to the same production question: what problem is this machine solving, and how reliably will it solve it at the output level you need?
When comparing quotations, ask for the following in clear terms:
- The target materials: Confirm exactly what materials and job types the quote is meant to support.
- The real production scenario: Ask whether the quote is based on prototyping, short runs, or repeated daily production.
- The included equipment: Separate machine price from extraction, cooling, software, delivery, and installation.
- The quality expectation: Clarify whether the machine is being positioned for speed, detail, edge cleanliness, or a balance of all three.
- The support scope: Ask what training, warranty coverage, spare-parts planning, and technical response are included.
- The proof of fit: Request sample output on materials and geometries close to your own parts.
This kind of comparison makes weak quotations easier to spot. If one quote is much lower but leaves too many supporting items undefined, it is not really cheaper. It is simply incomplete.
Sample Testing: The Only Reliable Way to Compare Cut Quality
Specifications sheets and marketing materials cannot tell you how a machine will perform on your specific materials. The only reliable way to compare cut quality is to run sample parts on each candidate machine. Bring the actual materials you process, including the thickest and thinnest variants, and request cuts that match your typical geometries.
Examine the samples for edge cleanliness, corner sharpness, and consistency across the full bed area. Cut the same part in multiple locations on the bed to check for variation. If the machine cannot produce consistent results across its working area, that inconsistency will show up in your production as scrap and rework.
Also test engraving quality if your work includes detailed marking or surface texturing. Engraving consistency depends heavily on motion control and beam stability. A machine that cuts acceptably may still produce uneven engraving depth or blurred detail. Sample testing reveals these issues before you commit capital.
When a Higher-Priced Machine Makes Better Business Sense
Not every shop needs the most expensive configuration. A lower-volume workshop with mixed jobs and flexible scheduling may be better served by a simpler system if the material range and quality expectations are realistic.
But a more expensive machine usually makes better business sense when the production environment depends on one or more of the following:
- Repeat jobs with tight delivery windows
- High labor cost around loading, setup, or rework
- Strong need for edge consistency or fine detail
- Frequent changeovers that reward easier setup
- Growth plans that will push output beyond a basic machine’s comfort zone
In those cases, the extra investment is not about buying a premium label. It is about buying stability, throughput, and lower process friction. The better machine is often the one that protects schedule reliability and keeps downstream work from slowing down.
Calculating Payback: When the Higher Quote Wins
The decision between a lower-priced and higher-priced machine often comes down to payback calculation. Estimate the labor hours saved per week with the more expensive machine, including setup time, loading and unloading, and rework reduction. Multiply those hours by your loaded labor rate to get weekly savings. Then compare that figure against the price difference.
Also consider throughput. If the more expensive machine cuts faster or runs unattended longer, it may allow you to accept more work without adding staff. That additional revenue capacity can justify the higher price even if the machine is not running at full utilization immediately.
Scrap reduction is another payback driver. If the cheaper machine produces 5 percent scrap on a material that costs $50 per sheet, and the shop processes 100 sheets per week, the weekly scrap cost is $250. A more stable machine that cuts scrap to 1 percent saves $200 per week. Over a year, that is more than $10,000—enough to close a significant price gap.
Price Should Follow Workflow, Not the Other Way Around
The most practical way to control laser cutting machine cost is to define the workflow first, then choose the configuration that fits it cleanly.
If your jobs are mainly decorative cutting, acrylic components, signage elements, wood panels, or engraving-heavy work, the right questions are not just “How cheap is the machine?” but also “How stable is the cut quality?” “How much manual handling remains?” and “How easily can this machine support repeat production?”
For buyers focused on wood, acrylic, and similar workflows, reviewing options in the Pandaxis laser cutters and engravers category is more useful than relying on generic market price assumptions that ignore process fit. If laser processing is only one step inside a larger equipment-planning decision, the Pandaxis product catalog can help buyers evaluate laser equipment alongside adjacent production categories instead of treating it as an isolated purchase.
The right machine does not come from chasing the lowest quote. It comes from matching machine type, format, and support level to the actual production load. That is what keeps the final cost aligned with the return.
Common Budgeting Mistakes in Laser Cutter Purchases
One recurring mistake is budgeting only for the machine and forgetting the installation and commissioning costs. Electrical work, ventilation ducting, compressed air lines, and floor preparation can add several percent to the total project cost. Shops that skip these items in the budget often face delays and cost overruns during installation.
Another mistake is underestimating the cost of training. A machine is only as productive as the operator running it. If the shop does not budget for proper operator training, the machine may sit underutilized or produce inconsistent results while operators learn by trial and error. The cost of that learning period often exceeds the price of formal training.
A third mistake is ignoring the cost of downtime during the transition. When a new machine replaces an existing process, there is a ramp-up period where output may be lower than planned. Shops that schedule the installation during a slow period and build in buffer time for the learning curve avoid the pressure of trying to hit full production immediately.
Future-Proofing: Buying for the Work You Will Have Next Year
Laser cutting machines are long-term assets. The configuration that fits today’s workload may not fit next year’s. Shops that expect growth should consider whether the machine can be upgraded or expanded to handle larger formats, additional materials, or higher output.
Some machines allow for software upgrades that unlock additional features. Others can be fitted with different optics or lens options to handle a broader material range. A machine with a modular design may accept a larger bed or additional automation later. These upgrade paths add value even if they are not used immediately.
However, future-proofing has limits. Buying a machine far larger or more capable than current needs ties up capital that could be used elsewhere. The practical approach is to buy for the next 18 to 24 months of expected workload, with a clear understanding of what upgrades are possible if growth accelerates.
FAQ
What is the biggest factor in laser cutting machine price?
Application fit. A machine built for light non-metallic work costs far less than one designed for larger formats, tighter tolerance, higher output, or more demanding production conditions.
Is higher wattage always a better buy?
No. Higher wattage raises cost, but value depends on material, edge quality, and cycle time. Overspending on power you will not use often produces weaker ROI than buying better motion quality or workflow support.
Why do similar-looking machines have very different quotes?
Similar-looking machines can differ in frame rigidity, motion control, optics, software, extraction, cooling, safety, warranty, and support. Those differences affect repeatability, downtime, and operating cost more than appearance suggests.
Should I compare only the base machine price?
No. Base price often excludes shipping, installation, training, software, extraction, cooling, consumables, spare parts, and service response. Total cost of ownership is the more accurate way to compare industrial laser quotations.
When is a more expensive laser cutter worth it?
A more expensive laser cutter is worth it when it reduces labor, scrap, setup time, rework, or downtime enough to improve output and protect delivery schedules in repeat production.
How important is sample testing before purchase?
Sample testing is the only reliable way to verify cut quality, edge cleanliness, and consistency across the bed. Specifications cannot reveal how a machine performs on your specific materials and geometries. Always request samples before committing to a purchase.