Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
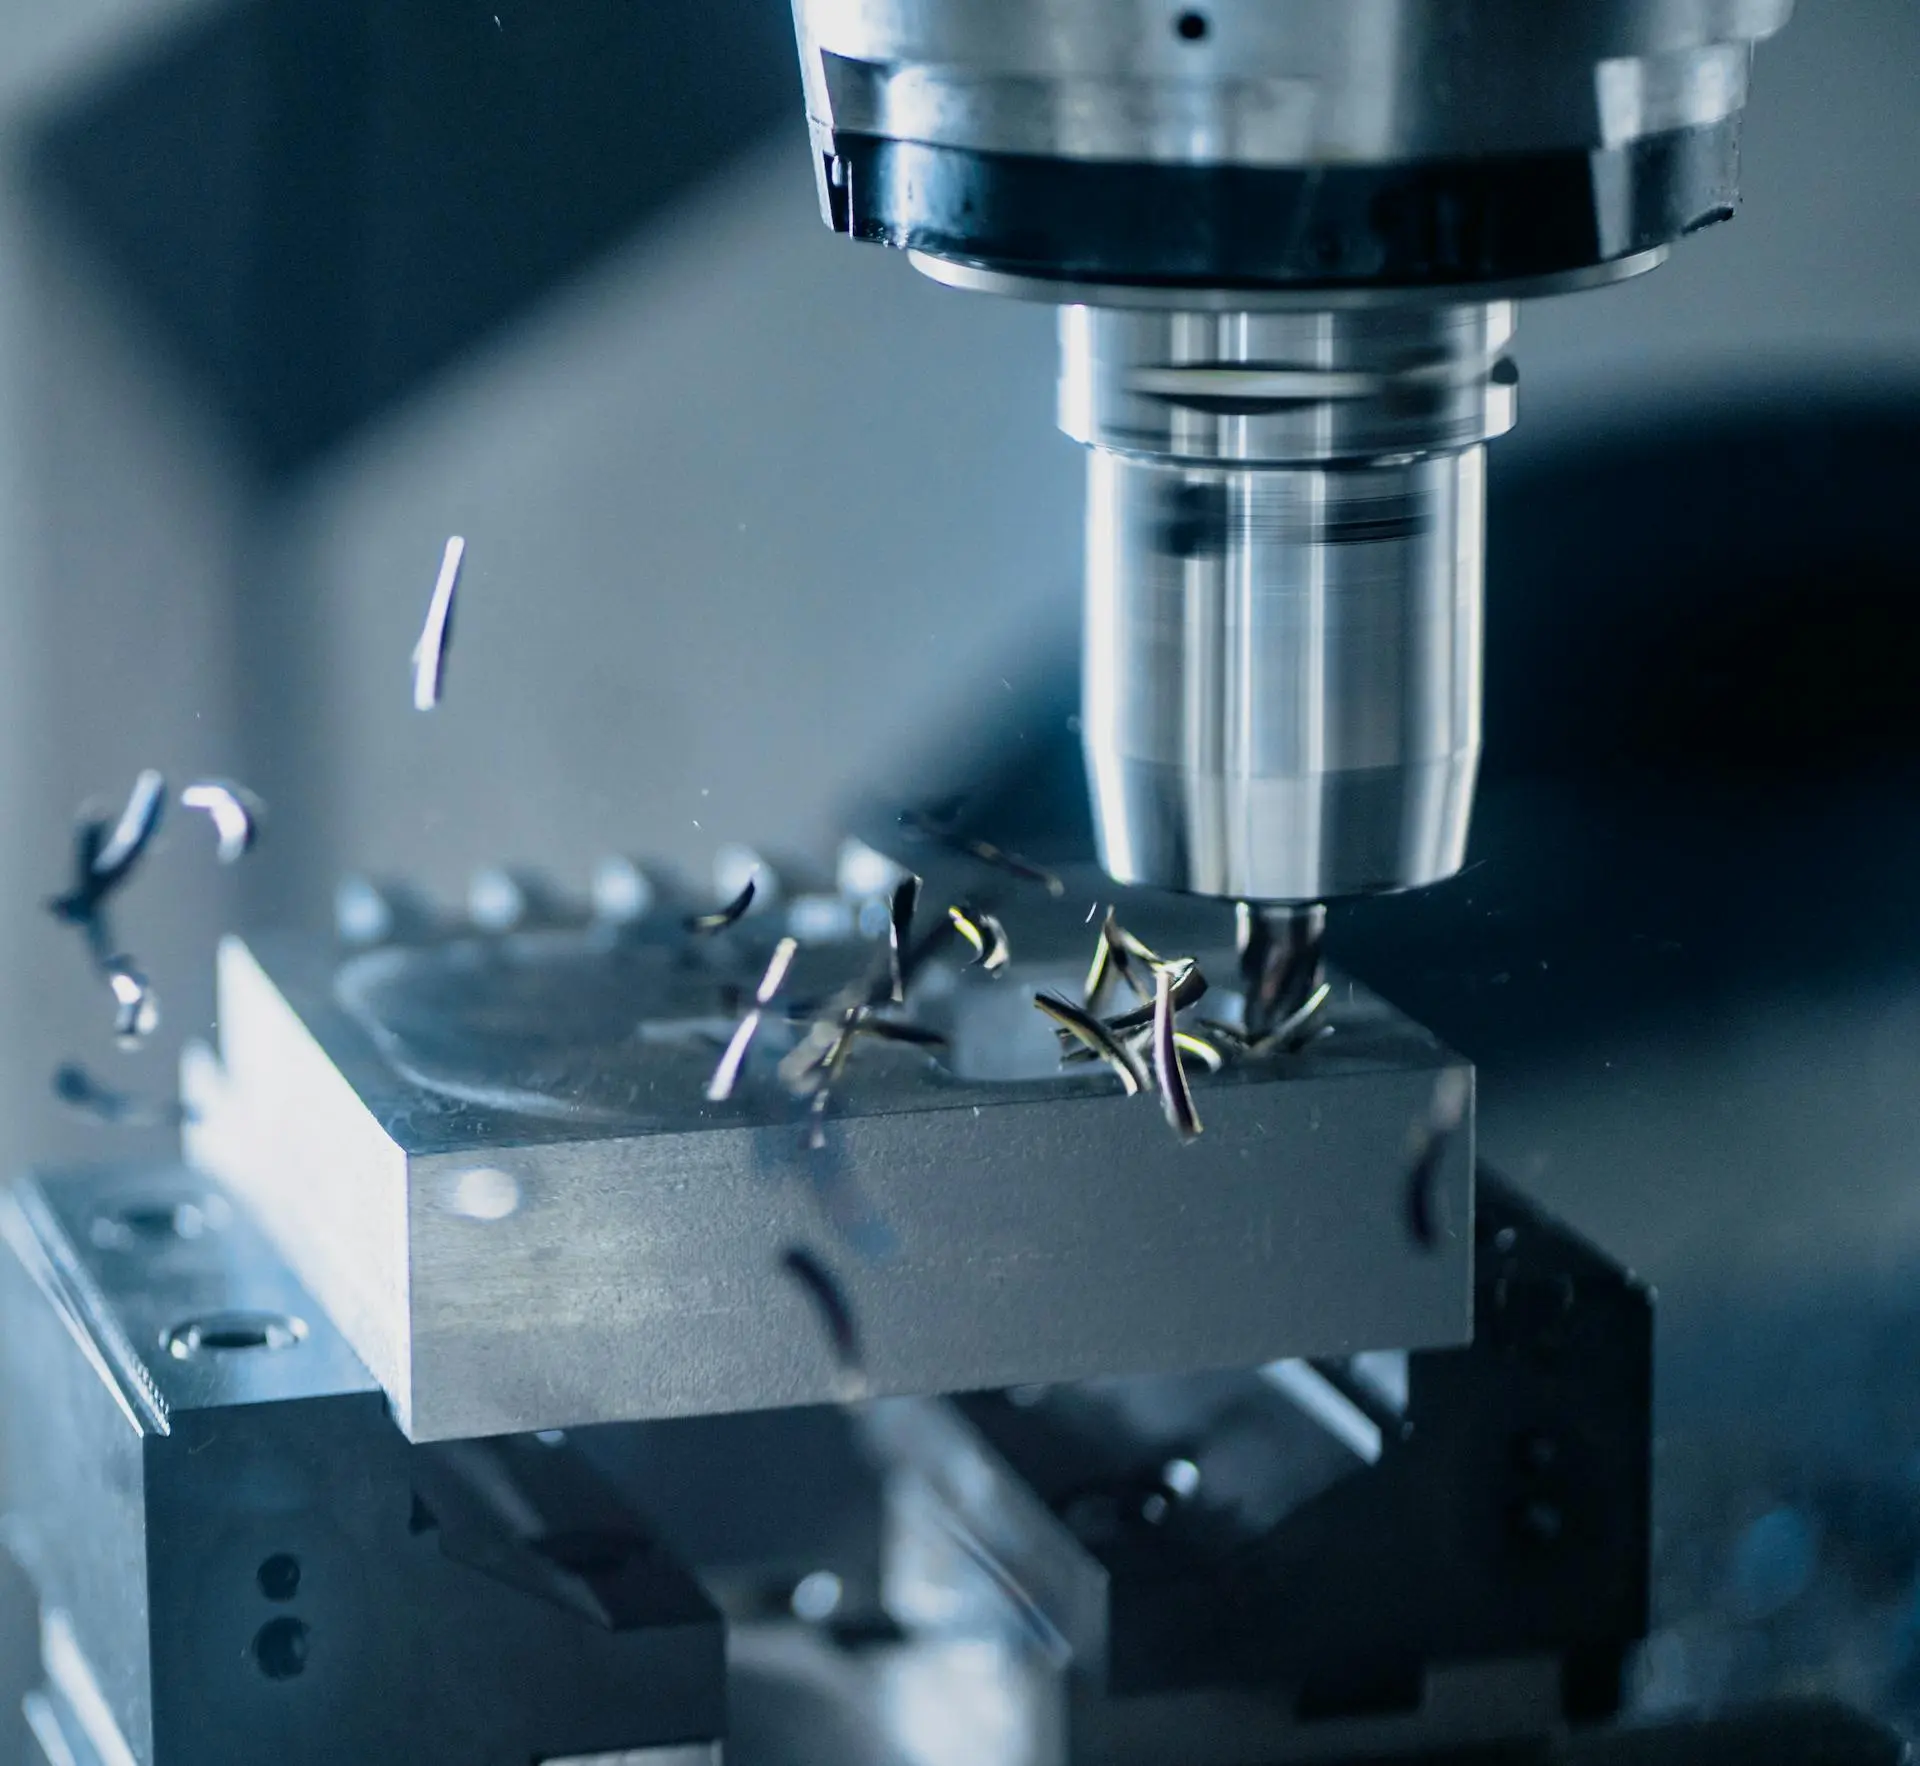
When cabinet, wardrobe, or modular furniture parts require holes on more than one face, the true production cost is rarely the drilling cycle itself. It is the cumulative handling burden: flipping the panel, re-establishing a reference edge, checking orientation, and hoping the relationship between holes on different faces remains true. For many shops, this is where throughput quietly dies and where hardware misfits are born.
For buyers comparing boring and drilling machines for multi-side panel processing, the strongest decision usually comes from matching the machine to part flow, pattern variety, and reference control—not from assuming the most complex configuration is automatically the best fit.
Multi-Side Processing Changes the Buying Question
In straightforward drilling work, the main question is often simple: how quickly can a machine produce repeated hole patterns on one face? Multi-side processing changes that logic entirely. Now the factory must control the relationship between holes on different faces, reduce the number of manual touches, and keep every part aligned as it moves through the drilling step.
In practical terms, a good multi-side drilling solution should help create:
- Fewer manual flips and reference resets
- More consistent hole relationships between faces
- Less manual marking, measuring, and verification
- Smoother hardware fit during assembly
- Better throughput in mixed or repeated batches
If a machine drills quickly but still leaves operators constantly repositioning parts and checking orientation, the factory may not gain much. The value of multi-side capability shows up when the workflow becomes easier to control, not just when the spindle cycle looks fast on paper.
Define What Multi-Side Processing Means in Your Factory
One reason buyers make poor comparisons is that “multi-side processing” can describe very different production realities. In one factory, it may mean processing two key faces with minimal re-handling. In another, it may mean drilling adjacent edges and surfaces while preserving a consistent datum through indexed movement. In a more varied operation, it may mean changing hole logic from part to part without forcing manual layout each time.
Before comparing machines, it helps to clarify the real part flow:
- Are most parts repeated cabinet components or mixed custom panels?
- Do panels need drilling on opposing faces, adjacent edges, or several surfaces in one release sequence?
- Is drilling happening before or after the part becomes dimensionally final in the line?
- How much manual turning is still acceptable at target output levels?
- Are operators mainly drilling parts, or spending too much time sorting, checking, and reorienting them?
These questions matter because the right drilling machine is not the one with the broadest theoretical capability. It is the one that matches the actual way parts move through the plant.
Accuracy Starts With Referencing and Clamping
In multi-side drilling, hole quality is not only a function of drilling units or machine size. The more important issue is whether the part stays reliably referenced as different faces are processed. Small alignment drift that might look manageable on one face becomes much more costly when hinge plates, connectors, dowels, cam fittings, or drawer hardware have to line up across multiple surfaces.
That is why buyers should pay close attention to how the machine establishes and protects the part datum. The key issue is not whether the machine can reach another side. It is whether it can do so without introducing cumulative alignment error.
What usually matters most includes:
- How the part is referenced on first contact
- Whether that reference is preserved through indexed movement or repositioning
- How securely the part is held during processing
- How well smaller, narrower, or more delicate panels stay supported
- Whether the workflow reduces operator guesswork about part orientation
Consider a typical cabinet side panel. It needs dowel holes on the top and bottom edges, shelf pin holes on the inner face, and hinge cup bores on the inner face near the front edge. If the machine processes the face, then flips the part to drill the edges, the datum must be re-established each time. A machine with pneumatic stops and clamping that reference the same corner or edge on every operation will hold face-to-edge relationships far better than one that relies on the operator to align the part visually. In practice, this means asking the supplier how the part is registered on the table, whether the clamping sequence is automatic, and what happens when panel width or thickness varies slightly from batch to batch.
Multi-side drilling magnifies the cost of weak reference control. If the datum shifts between faces, the problem will usually show up later as difficult assembly, hardware misfit, or repeated checking at downstream stations.
Pattern Variability Often Determines Whether CNC Control Pays Off
Some factories run a narrow range of cabinet parts with highly repeated drilling logic. Others work across many cabinet sizes, wardrobe variants, hardware formats, and project-specific part programs. Both environments can justify a drilling investment, but not necessarily the same kind of one.
If patterns are stable and repetitive, a simpler dedicated boring workflow can still be highly effective. If patterns change constantly, programmability becomes far more important. In that case, the machine has to support frequent job changes without turning every new batch into a manual setup exercise.
This is where CNC control usually creates value. Not because it sounds more advanced, but because it can make variable hole patterns easier to release with less manual translation between production data and the machine. If the part program changes often, the real productivity gain comes from cleaner changeovers and fewer avoidable setup mistakes.
Buyers should therefore look beyond the drilling cycle itself and ask:
- How often do hole patterns change in daily production?
- How much manual input is required between jobs?
- How easily can operators confirm the correct program and part orientation?
- Does the machine support repeatable job release in a mixed-batch environment?
The more varied the work becomes, the more valuable structured CNC control usually is.
When a Multi-Spindle Boring Machine Is Enough and When CNC Flexibility Matters More
Not every multi-side drilling task requires the same level of programmability. A factory producing repeated carcass parts with highly standardized hole locations may benefit more from process stability and straightforward throughput than from maximum programming flexibility. A factory handling frequent model changes, hardware variation, and batch complexity may need a more adaptable CNC drilling approach.
| Production Condition | Simpler Dedicated Boring Workflow | More Flexible CNC Drilling Workflow |
|---|---|---|
| Repeated cabinet carcass parts with stable patterns | Often a strong fit because simplicity supports repeatable daily throughput | Useful, but may offer more flexibility than the job mix requires |
| Frequent model changes and mixed part programs | Can become more setup-dependent and less efficient | Usually better suited because pattern changes are easier to manage |
| Multi-face accuracy is a recurring quality issue | May work if reference control is strong and part logic is simple | Often stronger when reduced handling and better program control are needed |
| Hardware formats change often across orders | Less convenient if adjustments are frequent | Better fit when job variation is part of normal production |
| Very high volume of similar panels | Often attractive because the workflow can stay stable | Valuable if the line still needs more flexible release logic |
| Growth toward more product variation | Can be outgrown if complexity rises | Usually easier to scale with a more mixed product structure |
The honest tradeoff is this: more CNC flexibility becomes valuable when the production problem is complexity, handling, and pattern change. If the work is simple and repeated, a less complicated drilling solution may remain the smarter choice.
The Buying Factors That Usually Matter Most
Multi-side drilling decisions are strongest when buyers compare machines against workflow criteria instead of isolated features.
| What to Evaluate | Why It Matters in Multi-Side Processing | What to Ask Internally |
|---|---|---|
| Number of faces per part | Determines how much handling the drilling process must absorb | Are we trying to reduce one extra flip, or redesign a heavily re-clamped process? |
| Part mix | Repetitive work and mixed work do not benefit from the same machine logic | Are most parts standardized, or does drilling logic shift constantly? |
| Reference stability | Face-to-face hole relationships depend on consistent datum control | Where do alignment mistakes currently enter the process? |
| Changeover frequency | Frequent batch changes quickly expose weak setup logic | How much time is lost between one drilling pattern and the next? |
| Operator dependency | Strong dependence on one skilled operator makes output harder to scale | Is quality process-driven, or person-driven? |
| Handling burden | Manual turning, checking, and resorting often limit true output | Is the bottleneck drilling, or everything around drilling? |
| Downstream assembly sensitivity | Drilling errors become obvious when hardware and panels must fit cleanly | Where do hinge, connector, or drawer-fit problems actually start? |
| Future product direction | The right machine should fit not only today’s mix but near-term complexity | Are we moving toward more volume, more variation, or both? |
Factories that answer these questions clearly usually make better buying decisions than factories that compare only spindle layouts, machine size, or headline automation language.
Match the Machine to the Entire Panel Workflow
A drilling machine does not operate in isolation. Its value depends on where it sits between panel cutting, edge processing, part identification, hardware preparation, and final assembly. If upstream parts arrive in the wrong order, without stable dimensions, or with weak part tracking, a more advanced drilling machine may not solve the real problem.
That is why buyers should evaluate the full workflow around the machine:
- Are panels arriving in a stable, traceable order?
- Is the drilling step working from reliable part dimensions?
- Will the machine reduce manual checking before assembly?
- Does it make batch release cleaner for the next station?
- Will it remove a real bottleneck or simply move the bottleneck elsewhere?
In many plants, the hidden cost is not insufficient drilling power. It is the time lost in confirming part identity, correcting orientation mistakes, or compensating for alignment drift before the part can move forward.
Signs You Need a Better Multi-Side Drilling Solution
The need for a different machine often becomes visible before management formally decides to upgrade.
Common signs include:
- Operators are spending too much time repositioning parts between faces.
- Assembly teams regularly correct hardware-fit problems that start at drilling.
- Pattern changes slow output more than the drilling cycle itself.
- Quality depends too heavily on one experienced operator.
- Multi-face panels need repeated verification before release.
- Production growth is increasing part variety faster than the current drilling process can absorb.
When these conditions show up consistently, the buying question usually shifts from “Can the current machine still drill parts?” to “Can the current drilling process still support the line without excess handling and correction?”
Selection Focus: a CNC Drilling Machine for Multi-Side Processing
Choosing a CNC drilling machine for multi-side processing is really about choosing how the factory wants to control part handling, datum accuracy, and pattern change. The right machine is not automatically the one with the highest perceived complexity. It is the one that reduces unnecessary re-clamping, keeps hole relationships stable across faces, and matches the actual mix of repeated and variable work.
If the factory runs highly repetitive panel parts, a simpler dedicated boring approach may still deliver strong results. If the production model includes frequent design variation, hardware changes, or a growing need to process multiple faces with less manual intervention, a more flexible CNC drilling workflow usually becomes easier to justify. The practical test is simple: judge the machine by what happens after drilling. If hardware fits more reliably, assembly needs less correction, and operators spend less time turning and checking parts, the machine is solving the right problem.