Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
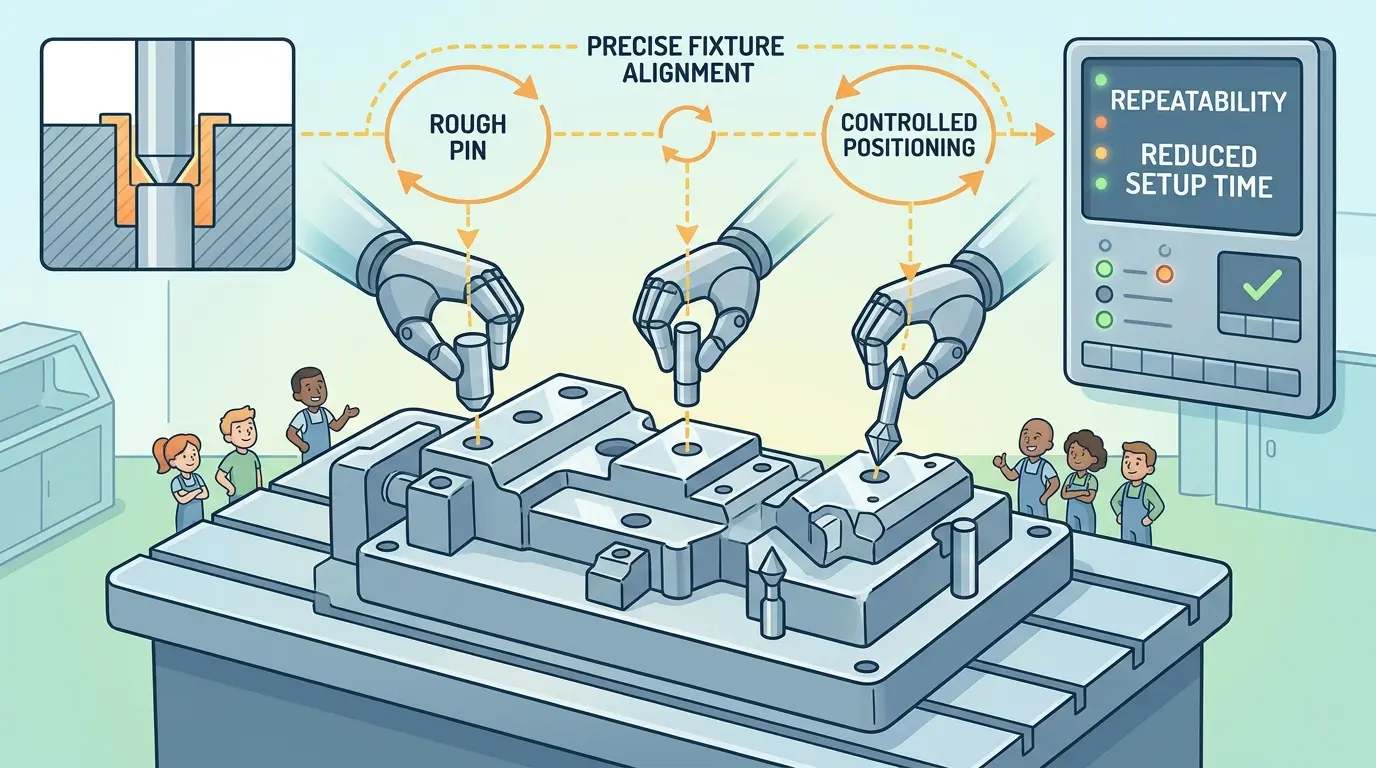
When repeatability drifts on a CNC fixture, the first instinct is to blame the program, the spindle, or the machine itself—but the fault often lies in how the part is seated before cutting ever begins. This article addresses that hidden failure point by explaining the true function of locating pins: establishing repeatable reference points that turn a clamping arrangement into a coordinate device. For production engineers and fixture designers, the distinction between locating and clamping, the risks of overconstraint, and the impact of chips and burrs on seating are decisions that determine whether every cycle starts from the same datum or quietly introduces error that inspection will later expose.
Why Repeatability Fails Before the Spindle Ever Moves
Shops usually start asking about locating pins when repeatability begins slipping in a way that is hard to explain. The fixture still looks solid. Clamps still tighten. The same program still runs. Yet the part no longer seems to return to exactly the same place from one cycle to the next. Operators start compensating. Inspection takes longer. Loading becomes more cautious. Eventually someone realizes the issue may not be the program or the spindle at all. It may be the way the part is being told where to sit.
That is where locating pins matter.
CNC accuracy does not start at the spindle. It starts at the seating relationship between the part, the fixture, and the machine coordinate system. If that relationship changes, the machine can execute a perfect program in the wrong place. Locating pins remove uncertainty from placement and turn a fixture from a clamping device into a repeatable reference system.
The Core Function: Eliminating Guesswork Before Cutting Starts
The shortest practical definition is this: CNC locating pins are used to put a workpiece, pallet, jig, or subfixture back in the same place repeatedly. They establish repeatable reference points so the machine does not have to depend on operator judgment every time a part is loaded.
That sounds simple, but the value is large because repeatability is often lost in very small moments of doubt:
- Is the part fully seated?
- Is it slightly rotated?
- Did it creep while clamping?
- Is this cycle really starting from the same datum as the last one?
Locating pins remove that uncertainty when the fixture is designed correctly. They let the loading sequence begin from defined contact logic instead of approximation. That shortens setup time, improves confidence, and removes hidden variables that would otherwise disturb the programmed result.
This is why locating pins are much more than small accessory hardware. They are part of the datum logic the whole process depends on.
Turning a Fixture Into a Coordinate Device
Many weak fixturing conversations focus too much on hardware count and not enough on function. A fixture plate with clamps may look robust, but until the workpiece is forced into a known and repeatable relationship, the fixture is still missing its most important job.
Locating pins are often the point where that change happens. They convert a general holding arrangement into a system that can repeatedly define position. Once that happens, the fixture is no longer just holding a part against cutting force. It is helping establish where the machine believes the part exists.
That distinction is critical. If the machine coordinate system expects one relationship and the fixture produces another, the control can still perform flawlessly while the part comes out wrong. The machine is not confused. The datum chain is weak.
This is why mature shops treat locating features as part of process accuracy, not as cheap consumable hardware.
Locating and Clamping Are Not the Same Function
One of the most important rules in fixturing is that locating and clamping do not do the same job. Locating establishes where the part belongs. Clamping keeps it there.
When these functions get blurred, fixtures become harder to load, more likely to distort the part, and less trustworthy under repeat production. If clamping force is also being asked to shove the part into position, the system is already unstable. If the part must be forced onto the pins because the fit is too aggressive for real production variation, the fixture becomes slow, awkward, and easier to damage.
Good locating strategy is not about using the most pins or the tightest fit. It is about using enough controlled reference to remove ambiguity without turning normal loading variation into friction, impact, and delay.
That is why a good fixture often feels calmer than a bad one. The operator is not wrestling the part into place. The part arrives at the references, settles predictably, and then gets held.
Datum Logic, Not Pin Count
In practice, locating pins can support several different fixturing strategies. Some systems use a fixed-and-relieved combination so the part is controlled without being overconstrained. Some fixtures use pins to re-establish a pallet or modular subfixture. Others use them for recurring small-part loading where cycle speed matters and the operator needs unmistakable reference points.
The geometry changes with the part, but the principle stays the same: the pin strategy should match the datum strategy on the drawing and the inspection logic downstream.
This is where the discussion becomes more mature. The right question is not “how many locating pins should I use?” The right questions are:
- Which surfaces or features are supposed to establish the part’s orientation?
- Which degrees of freedom need to be controlled?
- Which constraints should remain free so the part is not fighting the fixture?
- Does the loading logic match the inspection logic later?
Many fixture schemes are built around primary, secondary, and tertiary restraint logic, often described in simplified terms as 3-2-1 location. The exact implementation depends on part geometry, but the larger lesson is that locating pins are only useful when they participate in a restraint plan that is internally consistent.
That is why locating pins should be discussed in the language of datums and contact logic, not only as catalog items.
Where Locating Pins Create the Most Value
Locating pins become especially valuable in repeat jobs, modular fixtures, palletized work, assembly-related machining, and any process where parts are removed and reloaded but still need to return to a stable coordinate relationship. They are equally important in small-part fixturing because small parts usually leave very little tolerance for sloppy placement.
This is where fixture design becomes a workflow issue rather than a hardware exercise. If the loading routine still leaves the operator unsure whether the part is fully seated, the fixture is not finished yet. That broader lesson shows up clearly in small-part fixturing practice, where locating, support, chip escape, and clamp sequence all affect whether repeatability survives real production.
Locating pins are often the quiet center of that system. When they are right, the fixture feels obvious. When they are wrong, every cycle contains a small amount of hesitation even if nothing looks dramatically broken.
Typical high-value use cases include:
- Recurrent loading of the same family of parts.
- Secondary machining after one operation has already defined key features.
- Modular fixture bases where different top plates must return to known positions.
- Palletized work where parts or fixtures move between stations.
- Assembly-related machining where hole patterns or edges must stay in predictable relationship to earlier features.
In all of these, the locating pin is helping preserve positional trust through the full process, not just during one clamp event.
Small Errors in the Pin Zone Create Large Downstream Problems
Because locating pins are simple parts, their failure modes are easy to underestimate. A pin does not need to shear off to become expensive. Small wear, slight mushrooming, edge burrs, contamination, or repeated impact loading can gradually reduce how honestly the part seats.
The result is rarely dramatic at first. Instead, the fixture becomes less trustworthy.
Operators start nudging parts by feel. Inspection becomes more defensive. Loading slows down because the fixture no longer communicates certainty. Scrap may not rise immediately, but process trust falls before the first obvious nonconformance appears.
That is why locating-pin maintenance should not wait for visible collapse. A worn locating feature may already be costing the shop money long before anyone calls it failed.
The cost shows up in:
- Slower loading.
- More frequent verification.
- Repeated cleaning or reseating.
- Quiet operator compensation.
- Hard-to-explain repeatability drift.
This is also why replacement should be easy. If a fixture depends on a locating pin but replacing it is awkward, the shop will tend to postpone the work too long.
Chips, Burrs, and Surface Condition Often Matter More Than Pin Diameter
A locating pin only works if the mating surfaces can actually seat against it cleanly. Chips, coolant residue, dust, burrs, and rough incoming edge condition often cause more repeatability loss than the nominal pin dimensions do.
Shops sometimes blame the pin when the real problem is that the locating zone traps contamination or the incoming part cannot sit cleanly because of edge condition from a prior step. In that situation, replacing the pin may improve the process briefly, but the underlying weakness remains.
This is why good fixtures do not simply include locating pins. They support locating pins with practical loading behavior.
That means thinking about:
- Where chips go.
- How mating surfaces are approached.
- Whether burrs will collect in the seating zone.
- Whether the operator can load cleanly without scraping or impact.
- Whether the fixture gives contamination a way to escape instead of trapping it.
If the setup only works when the operator cleans obsessively and aligns by feel, then the pin strategy is incomplete. The whole locating environment needs review.
That broader workholding view matters because locating pins never work alone. They operate inside a system of supports, clamps, approach paths, and debris behavior. Teams trying to stabilize repeatability should often review the wider logic of how fixturing improves accuracy instead of changing one component in isolation.
Fit Choice Is a Cycle-Time Decision As Much As an Accuracy Decision
Very tight location can sound ideal in theory because it appears to promise precision. In real production, the fit has to match the full operating environment: loading speed, incoming part variation, cleanliness, thermal behavior, burr condition, and the actual repeatability requirement.
A fit that is too loose leaves room for ambiguity. A fit that is too tight may slow loading, encourage impact damage, or create a false sense of precision while operators fight the interface by hand.
That is why locating-pin selection should be made with the cycle in mind, not just the drawing.
Useful questions include:
- How fast must the operator load?
- How consistent is the incoming part condition?
- How clean is the process zone in real life?
- How often are parts swapped?
- What repeatability is truly required for this operation?
The correct answer is rarely “choose the hardest, tightest pin and forget it.” The right answer is to match the locating method to the real workflow.
This also means replacement should not always be automatic like-for-like substitution. If cycle time, part mix, tolerance expectations, or fixture duty changed, the original locating strategy may no longer be the best one.
Overconstraint Is One of the Most Common Quiet Design Mistakes
Another reason locating pins cause trouble is overconstraint. Shops sometimes add locating features with good intentions but create a fixture that asks the part to satisfy more positional conditions than the part can comfortably meet.
When that happens, loading becomes forceful, parts rock or bind, or clamping hides the fact that the part was never resting naturally. The fixture may appear precise, but it is actually fighting the workpiece.
This is why combinations such as fixed and relieved location are so useful. The goal is not to trap the part from every possible direction. The goal is to control the required degrees of freedom without creating unnecessary conflict.
A locating strategy is strong when the part can find its intended position cleanly and repeatably. It is weak when the part must be muscled into theoretical perfection.
Locating Pins Are Different From Bushings and Guide Features
It is useful to separate locating pins from CNC bushings because both can affect repeatability while doing different jobs.
Locating pins define where the workpiece, pallet, or fixture sits. Bushings usually protect or guide a moving interface, such as a tool or a guided element in the fixture system. If a process is losing repeatability, the problem may be in the seating relationship, the guided motion relationship, or both.
Treating every repeatability problem as a locating issue can waste time. So can blaming all positional error on machine wear when the part is actually being seated inconsistently.
Good diagnosis asks one simple question first: which relationship is moving when it should not be?
If the part is not landing consistently, the locating strategy deserves attention. If the part is seated properly but motion is wandering, the problem may live elsewhere.
When Replacing the Pin Is Not Enough
Sometimes a damaged or worn locating pin truly is the whole problem. But if doubt keeps returning, the smarter move is to review the whole loading concept rather than repeatedly ordering the same replacement.
The best test of a locating system is not whether it looks precise on paper. It is whether it removes repeated doubt during live production. If operators still hesitate while loading, if chips repeatedly foul the seating points, if clamping disturbs the part after location, or if the fixture is hypersensitive to burrs or incoming variation, then the pin strategy may need redesign instead of simple replacement.
Likewise, if pins wear repeatedly, the next question should not only be about hardness or material. Ask whether the loading motion is abusive, whether the fixture encourages impact, whether contamination is trapped, and whether the datum scheme is too ambitious for the part family.
A pin that keeps failing may be doing its best inside weak fixture logic.
That is why the mature response is broader than swapping hardware. Review the datum plan, the contact surfaces, the clamp path, the debris path, and the operator approach path. Then decide whether the pin itself, the fit, or the whole locating concept needs correction.
A Very Small Part Can Control the Honesty of the Whole Process
CNC locating pins are used to make placement repeatable. They shorten setup, reduce operator interpretation, and help fixtures return parts or subassemblies to the same reference position from one cycle to the next. Their importance is easy to underestimate because they are physically small and mechanically simple. In reality, they sit at the beginning of positional trust.
The most useful way to think about them is this: locating pins are there to remove doubt before the machine ever starts moving. If the part enters the cycle from a stable, clean, repeatable reference, everything after that becomes easier to trust. If the datum is weak, even very good motion control cannot fully rescue the job.
That is why locating pins deserve more respect than their size suggests. They are not just fixture accessories. They are one of the small features that determine whether repeatability is real or merely assumed.