Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
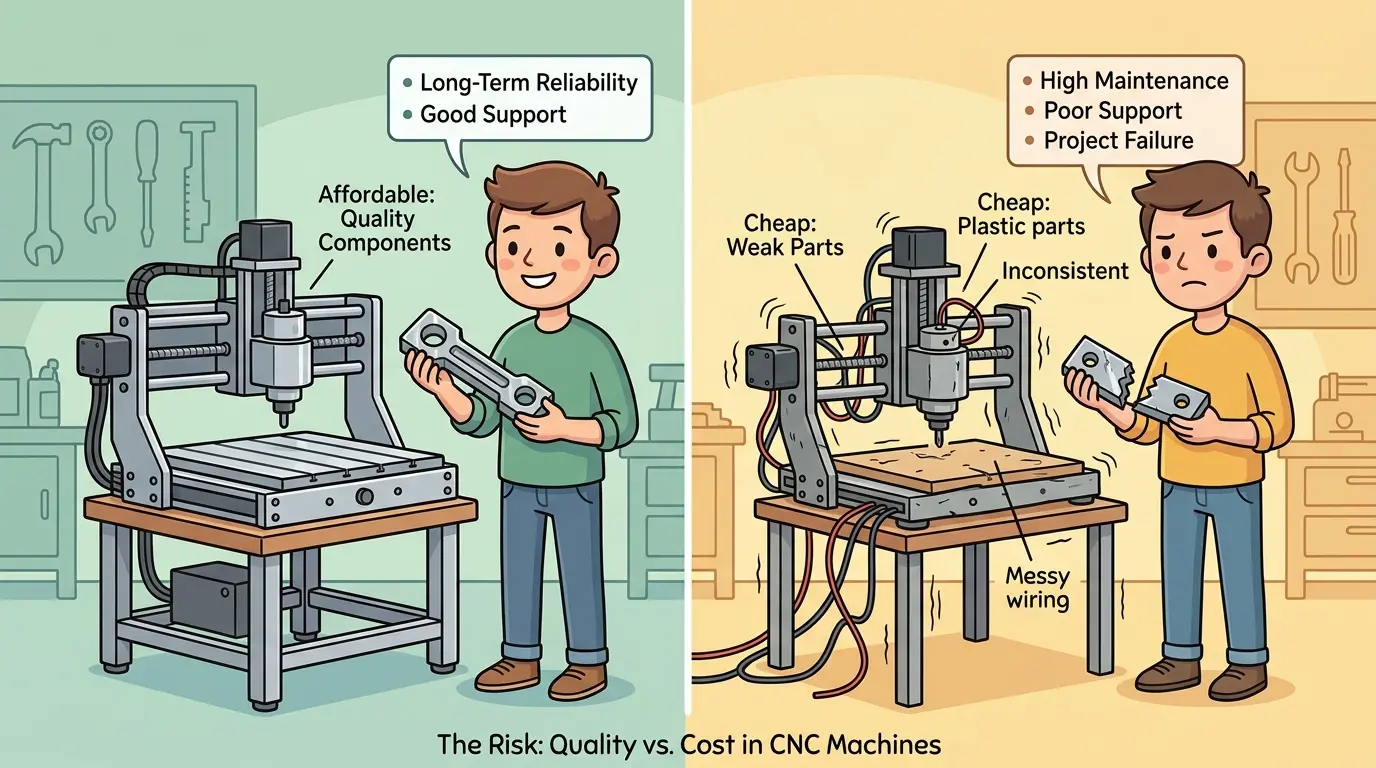
Two CNC quotations can list identical work envelopes, spindle ratings, and controller names—yet one machine will carry a two-shift cabinet shop for years while the other quietly consumes operator hours in feed-rate compensation, alarm recovery, and undocumented troubleshooting. The difference is not the price tag but where the missing money went: honest simplification removes capability you do not need, while cheap construction transfers structural rigidity, diagnostics, documentation, and support burdens downstream into daily labor. Before comparing bottom-line numbers, screen every candidate for hidden burden transfer, because the real cost of cheapness shows up in throughput penalties and maintenance time, not on the invoice.
Why Two Similar Quotes Can Lead to Very Different Outcomes
At the quotation stage, an affordable CNC machine and a cheap CNC machine can look nearly identical. Both may list a similar work envelope, a comparable spindle figure, the same controller name, and a bottom-line price that undercuts premium options by a wide margin. The real difference usually appears later—when one machine starts the shift calmly and the other starts a conversation nobody wanted to have.
That is the actual distinction. Affordable and cheap are not separated by price alone. They are separated by where the missing money went.
A shop considering a low-cost machine needs to understand that distinction before signing, because the gap between these two categories determines whether the purchase becomes a dependable production asset or a recurring source of labor drain. This article walks through the practical differences, the specific failure points to inspect, and the questions that separate a sound low-cost purchase from a costly mistake.
Affordable Usually Means Narrower But Honest
An affordable machine is often less expensive for reasons that still protect the intended job. The manufacturer reduced cost by removing capability the shop does not need, not by weakening the capability it does need.
That may mean:
- A smaller working area because the shop does not need more.
- Fewer automation layers in a workflow that is still operator-centered.
- A simpler control environment that still fits the process.
- A lighter machine category used deliberately for training, prototypes, or low-risk output.
The lower price still protects the intended work. The machine is less ambitious, not less trustworthy inside its role. If the machine is specified for light-duty nesting and the shop runs light-duty nesting, the machine can be a sound production asset for years.
Consider a cabinet shop that cuts only sheet goods up to 18 mm thick, runs two shifts, and has an experienced operator who has run the same control platform for a decade. A machine with a modest spindle, a rigid welded frame sized for that duty, and a control with clear diagnostics can serve that shop well for years. The manufacturer saved money by not engineering for heavy aluminum plate or 24-hour continuous roughing. That saving passes to the buyer without compromising the intended work.
Cheap Usually Means The Burden Was Moved Downstream
Cheap equipment is different. It may still produce an acceptable sample part, and it may even look convincing in a demonstration. The missing value usually shows up later, in the parts of ownership that were hard to see in the quote.
That often means:
- Less stable structure or motion behavior.
- Thinner diagnostics and recovery visibility.
- Electrical execution that is harder to recover when something goes wrong.
- Documentation too thin for fast troubleshooting.
- Vague startup, training, or spare-parts support.
- More tuning and operator compensation to keep the process calm.
In effect, the machine is cheap because the buyer has quietly agreed to absorb more uncertainty later. The price difference is not a discount. It is a down payment on future labor.
A typical scenario: a shop buys a low-cost nesting machine because the price is half that of a comparable unit from a recognized brand. The first month runs acceptably. By the third month, the operator notices that the machine needs slower feeds on certain grain directions to avoid tear-out. By the sixth month, the Y-axis drive begins making noise on rapid traverses. The supplier’s response time is measured in days, not hours, and the spare part requires a two-week lead time. The machine still cuts, but the shop has quietly absorbed a 15 percent throughput penalty and a maintenance burden that was never part of the purchase calculation.
The First Useful Question Is Not “Can It Cut?”
Many low-price mistakes begin with the wrong opening test. Buyers ask whether the machine can cut the material or whether the sample part looks acceptable. Those questions are not useless. They are incomplete.
The better question is what kind of operating burden comes with the cut.
A low-cost machine may still be commercially weak if it requires:
- More cautious feeds to stay stable.
- More supervision to protect finish quality.
- More manual intervention after stops or alarms.
- More troubleshooting every time setup changes.
- More hidden time to get back to a known-good state.
“It still cuts” is a weak defense if the machine keeps collecting labor around the cut. A machine that produces a good part but demands constant attention is not a production tool. It is a project.
The sample-part test has another weakness: it is usually performed under ideal conditions. The supplier sets up the material, the tooling is fresh, the operator is careful, and the machine has been warmed up and calibrated. That is not the same as running the machine at 7:30 on a Tuesday morning with a batch of warped board, a worn tool, and a deadline. The real test is whether the machine holds quality when conditions are not perfect.
A Quick Screen For False Savings
The table below separates honest simplification from hidden burden transfer. Use it as a first-pass filter before any quotation comparison goes deeper.
| Area | Affordable Signal | Cheap Signal |
|---|---|---|
| Scope | The machine is openly positioned for a narrower workload | The machine is marketed as suitable for almost everything |
| Structure | Lower price comes with believable duty limits | Frame quality is vague or hand-waved away |
| Controls | Simpler control is still appropriate for the intended use | Diagnostics and recovery feel thin or unclear |
| Documentation | Limits, setup, and maintenance are explained clearly | Real recovery work still depends on guessing |
| Service | Support path is visible even if basic | Startup, spares, and escalation remain fuzzy |
| Workflow Fit | Buyer can name the exact jobs the machine will carry | Buyer is hoping the machine will grow into a much larger role |
This is usually the first separation buyers need to make: honest simplification versus hidden burden transfer. Run every candidate quotation through this screen before comparing prices in detail. If a machine fails on three or more rows, the low price is not a bargain—it is a warning.
Where Cheapness Usually Shows Up In Daily Work
Cheapness rarely appears as one dramatic failure on day one. More often it appears as recurring friction that slowly reshapes how the shop operates.
Typical symptoms include:
- Extra tuning before the cut feels trustworthy.
- Slow alarm recovery.
- Conservative programming done “just to be safe.”
- Less confidence in repeat jobs.
- More labor moving from production into babysitting.
That is what makes underbuilt machines expensive. They alter behavior quietly. A machine with weaker structure or weaker diagnostic support may still complete the part, yet the shop never fully trusts it with the work it was meant to carry. Operators start running slower feeds, checking dimensions more often, and hesitating before committing to a run. None of that shows up on the invoice, but all of it shows up in the cost per part.
Consider a concrete example. A shop runs a batch of 200 cabinet doors on a CNC router. On a dependable machine, the operator loads the material, starts the program, and checks the first part for dimensional accuracy. The remaining 199 parts run with minimal supervision. On a machine with weak structural rigidity, the operator may need to check every fifth part for edge quality, adjust the spindle speed when the bit dulls slightly, and stop the machine twice during the batch to clear a fault that the control cannot explain. The batch takes 20 percent longer, and the operator’s attention is divided the entire time. That is the real cost of cheapness—it is measured in labor hours, not in the purchase price.
Control Quality Decides How Expensive Abnormal Events Become
Buyers naturally compare size, spindle, tool count, and travel first. The control often gets treated as background. That is risky, because control quality decides how fast the machine returns to normal after something unexpected happens.
Weak control depth usually means:
- Harder fault diagnosis.
- Less visibility into why the machine stopped.
- More trial-and-error recovery.
- Less confidence after restarts.
- More time lost every time behavior deviates from the ideal cycle.
One blunt rule helps here: if every abnormal event turns into a team discussion, the low quote is probably being repaid in labor. A control with clear alarm history, logical fault messages, and straightforward recovery procedures turns a five-minute interruption into a five-minute interruption. A weak control turns the same event into a 45-minute investigation followed by a cautious restart and a test part.
The control also determines how much operator skill is required to run the machine effectively. A well-designed control interface lets a competent operator manage tool changes, offsets, and program selection without constant reference to a manual. A poorly designed interface buries essential functions in nested menus, uses cryptic alarm codes, and requires the operator to remember undocumented workarounds. That difference matters most during shift changes, when a new operator must quickly understand what the previous shift was doing.
Documentation And Recovery Matter More Than Buyers Expect
Documentation feels secondary until the first real interruption. Then it becomes central. A machine with clear startup guidance, understandable alarms, realistic maintenance routines, and usable commissioning information settles into production faster.
A machine with vague documentation turns every nonstandard event into local improvisation. The operator tries one thing, then another, then calls someone who may or may not know the machine. That lost time rarely appears on the commercial summary. It shows up later in delayed shift starts, uncertain fault recovery, and technicians repeating the same detective work because the machine never came with enough practical guidance.
For shops without a dedicated maintenance engineer, documentation quality is not a minor consideration. It is the difference between a machine the team can support and a machine that supports itself only when everything goes exactly as planned.
Ask to see the actual documentation before purchase, not just a sample page. A complete manual should include:
- Mechanical drawings and lubrication points.
- Electrical schematics with labeled components.
- Alarm code tables with probable causes and remedies.
- Setup procedures for common operations.
- Preventive maintenance schedules with specific intervals.
- Troubleshooting flowcharts for common failure modes.
If the supplier cannot provide these documents before the sale, they will not magically appear after the sale. The documentation gap is a reliable indicator of the support gap.
Structure And Motion Quality: The Hidden Cost Drivers
The frame and motion system are the parts of a CNC machine that are hardest to evaluate in a showroom demonstration but most influential on long-term performance. A machine with a rigid, well-designed frame holds accuracy over years of service. A machine with a marginal frame develops problems gradually—slightly worse edge quality, more vibration at speed, and increasing difficulty holding tolerances as components wear.
The key structural elements to inspect include:
- Frame material and welding quality.
- Ribbing and reinforcement at stress points.
- Linear guide size and preload.
- Ball screw diameter and mounting method.
- Spindle mounting rigidity.
- Overall machine weight relative to work envelope.
A machine that is significantly lighter than comparable models from established brands is not necessarily worse, but the weight difference must be explained. If the manufacturer saved weight by using thinner plate, fewer ribs, or smaller linear guides, the machine will likely flex more under cutting loads. That flex translates directly into reduced edge quality, faster tool wear, and poorer dimensional accuracy on heavier cuts.
The motion system also determines how the machine behaves during acceleration and deceleration. A machine with properly sized servos and well-tuned drives moves smoothly between cuts. A machine with undersized drives or poor tuning hesitates, overshoots, or vibrates at certain speeds. These behaviors are visible in a careful demonstration, but only if the buyer knows what to watch for.
Electrical Execution: The Part Nobody Sees Until It Fails
The electrical cabinet is another area where affordable and cheap machines diverge. A well-built electrical system uses properly sized components, clean wiring, labeled terminals, and adequate cooling. A poorly built system uses marginal components, messy wiring, and minimal labeling.
The practical consequences of poor electrical execution include:
- Intermittent faults that are hard to reproduce.
- Longer downtime when components fail.
- More difficult troubleshooting because wiring is not labeled.
- Higher risk of electrical noise affecting control signals.
- More frequent component failures due to inadequate cooling or undersized parts.
Ask to see the electrical cabinet during a factory visit or demonstration. Look for organized wiring, labeled components, and adequate ventilation. If the cabinet looks like a tangle of wires with no obvious organization, the machine will be harder to maintain and repair throughout its life.
Cheap Can Still Be Rational If The Role Is Honest
Not every very low-cost machine is automatically a bad decision. Cheap equipment can still make sense when the buyer is deliberately accepting its limits.
That can include:
- Training.
- Proof of concept.
- Prototype experiments.
- Process learning.
- Educational use.
The key word is deliberately. The problem starts when the business buys the same machine as if it were a dependable production asset without pricing in the likely burden. A machine bought for training that gets pressed into production is not a bargain. It is a risk that was never budgeted for.
One useful test is simple: if the machine performs exactly as conservatively as the safest reading of the quote suggests, does the business case still work?
If the answer is no, the buyer is not really buying affordability. The buyer is betting on optimism.
A training machine that produces acceptable prototype parts at reduced feeds, requires occasional manual intervention, and needs a patient operator is a reasonable purchase if the shop understands those limits. The same machine becomes a liability when a production manager schedules it for customer orders and expects it to run at the same speeds and reliability as a machine costing twice as much.
Read The Low Quote For What It Omits
When one quotation is much lower, the first useful question is not “How did they get so efficient?” It is “What is no longer included, no longer protected, or no longer supported?”
Normalize more than headline specs. Compare:
- Structure and motion quality.
- Control visibility and recovery depth.
- Electrical and safety detail.
- Installation and startup scope.
- Training, documentation, and support path.
- Spare-parts access and escalation logic.
This is exactly why disciplined teams compare machinery quotes line by line instead of focusing only on spindle size, work envelope, and bottom-line number. The quote that looks cheapest on paper often carries the most hidden cost in practice.
A practical approach is to create a comparison matrix that includes not just the headline specifications but also the ownership factors that affect daily operation. Assign a weight to each factor based on the shop’s specific priorities. A shop with experienced operators might weight control familiarity heavily. A shop with limited maintenance capacity might weight documentation and support heavily. A shop running long production runs might weight structural rigidity and thermal stability heavily. The machine that wins this weighted comparison is not always the cheapest, but it is usually the most cost-effective over the machine’s working life.
When Paying More Is Actually Safer
The case for spending more becomes much stronger when the business cannot absorb instability gracefully.
That usually includes cases where:
- The machine will carry customer-facing production.
- Scrap or rework is materially expensive.
- Runs are long, repeated, or schedule-sensitive.
- Troubleshooting capacity is thin.
- Recovery speed matters almost as much as cycle time.
In those environments, dependability is not a luxury. It is part of the economics. A machine that runs consistently at rated feeds, recovers quickly from alarms, and holds repeatability across shifts is not just more convenient. It is cheaper per part than a machine that costs less upfront but demands constant attention.
That is also why buyers often benefit from stepping back and asking what industrial CNC equipment is actually buying beyond raw motion. The answer usually includes predictable behavior, recoverable faults, and support that does not disappear after the check clears.
For a shop that runs customer-facing production, the cost of a machine failure is not just the repair cost. It is the missed delivery date, the expedited shipping cost to recover the schedule, the overtime labor to make up the lost production, and the potential loss of customer confidence. These costs are rarely quantified in a purchase decision, but they are real. A machine that fails once per quarter and takes two days to repair costs more than a machine that costs 20 percent more upfront but fails once per year and is repaired in four hours.
The Best Buying Rule
Do not ask only whether the machine is cheap or expensive. Ask where the savings came from.
If the savings come from features the shop does not need, the purchase may be smart. A smaller table, a simpler control, or a lighter frame can all be legitimate ways to reduce cost without compromising the intended job.
If the savings come from the parts of the system that keep production calm—structure, diagnostics, documentation, support—the machine will usually become expensive later in exactly the way the original quote did not show. The price difference will be repaid in operator time, delayed shifts, and rework that never appears on the purchase order.
The final test is simple. Write down the machine’s intended role, the expected duty cycle, the operator’s skill level, and the shop’s tolerance for downtime. Then compare each candidate machine against those specific requirements. A machine that meets the requirements at a lower price is affordable. A machine that falls short of the requirements at any price is cheap—and the cost of that shortfall will be paid in labor, scrap, and lost production long after the invoice is forgotten.
For shops evaluating their options, a practical starting point is to review the machine categories that match the intended workload. Nesting machines, panel saws, edgebanders, and related woodworking equipment each have their own duty expectations and support requirements. Understanding what a given machine category should deliver—and what a low price usually means within that category—helps buyers separate genuine value from hidden burden.