Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
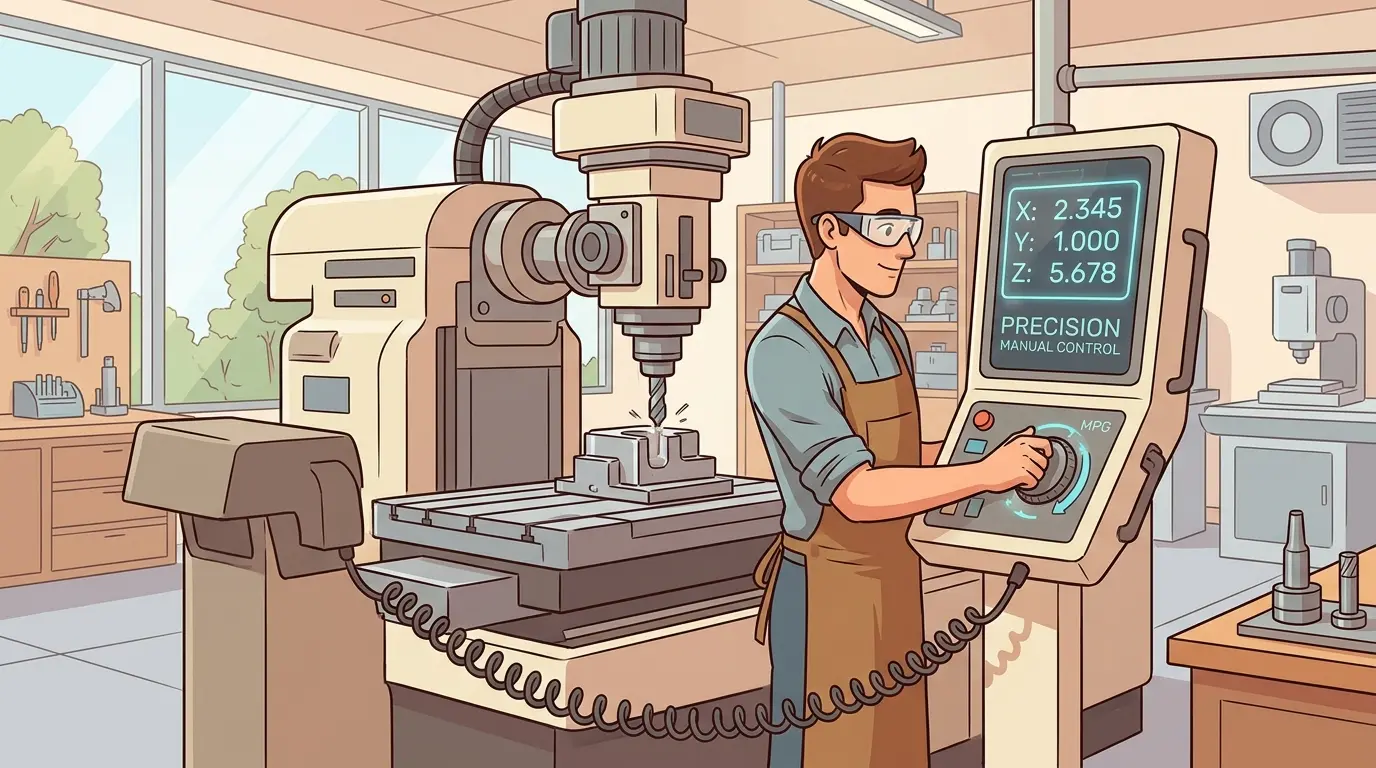
Before you finalize a CNC machine specification, the manual pulse generator deserves more scrutiny than its modest size suggests. This article examines why the handwheel remains a critical operator interface during the highest-risk moments in production: setup, tool touch-off, fixture clearance checks, and alarm recovery. The decision matters because a single wrong move near a clamp, touch plate, or finished surface can cost hours of rework. Buyers must evaluate not just whether an MPG exists, but how axis selection, increment scaling, and physical placement affect operator confidence and error rates.
Why a Small Wheel Earns Its Place on a CNC Control
A CNC handwheel, or manual pulse generator (MPG), is easy to overlook on a machine specification sheet. Compared with the spindle, servo package, or control software, it looks like a minor component. On the shop floor, however, it often becomes one of the most frequently used operator tools. That is because the highest-risk moments in CNC work rarely happen during a stable automatic cycle. They happen during setup, tool touch-off, fixture clearance checks, alarm recovery, and restart decisions—situations where a wrong move can cost hours and thousands of dollars in rework.
The MPG exists precisely for those moments. It is a manual interface that converts the operator’s physical rotation of a wheel into controlled axis movement at selected increments. Instead of holding a jog button and guessing when to release it, the operator selects an axis, chooses a movement scale, and advances the machine in deliberate, measurable steps. Some machines integrate the wheel into the control panel; others use a handheld pendant. Either configuration serves the same purpose: giving the operator calmer, more precise control when incorrect motion would be expensive.
This is why the handwheel should not be dismissed as a legacy feature. It is a tool designed for the most error-sensitive inches of machine travel.
Controlled Approach, Not Fast Travel
The clearest way to understand the handwheel’s value is to observe when operators actually reach for it. They rarely use it during routine automatic cutting. They reach for it immediately before a cycle starts, right after an interruption, or whenever the machine must move near something that cannot tolerate a mistake.
Typical applications include:
- Approaching a work datum during initial setup
- Bringing a tool toward a touch plate or tool setter
- Checking clearance around clamps, pods, vises, or custom fixtures
- Nudging an axis during alignment or inspection
- Repositioning after an alarm, stop, or broken tool event
- Verifying clearance before committing to cycle resume
The objective is not speed. It is controlled approach. When the next wrong move can clip a fixture, break a tool, mar a finished surface, or shake a new operator’s confidence, deliberate movement is more productive than fast movement. The handwheel converts a potentially stressful, high-stakes positioning task into a measured, step-by-step process.
What the Handwheel Changes in Operator Behavior
The MPG is conceptually simple, but its real value comes from pacing. Instead of commanding motion through timed button presses, the operator meters travel through physical wheel rotation. This changes the feel of close-range movement. The machine no longer seems to be waiting for the operator to release a button in time. It responds proportionally to what the operator can see and judge in real time.
That difference matters because setup stress is as much about confidence as it is about mechanics. The handwheel gives the operator a proportional relationship to machine movement. Used correctly, it reduces overshoot risk and eliminates the frantic stop-and-start behavior that often accompanies screen or panel jogging near a fixture or touch point. The operator can creep up on a reference point, observe the gap closing, and stop precisely where intended.
Safety Lives in the Control State, Not the Wheel
Because the device feels intuitive, operators sometimes assume the wheel itself creates safety automatically. It does not. Safety comes from the combination of the wheel and the control state surrounding it.
Every careful handwheel move still depends on:
- Correct axis selection
- Correct increment or scale setting
- Correct machine mode
- Accurate understanding of current position and offsets
The handwheel slows the operator down physically. It does not think for the operator. It provides a more controlled input method, but the operator must still confirm what the machine believes about its state before making a move. This distinction is critical for training and for avoiding the false confidence that can come from a smooth-feeling control device.
Most Handwheel Mistakes Are State Errors, Not Hardware Failures
In practice, the majority of MPG-related mistakes come from wrong-state decisions rather than from any defect in the wheel itself. The hardware is straightforward; the surrounding decisions are where errors creep in.
| Decision Point | Why It Matters | What Usually Goes Wrong If It Is Wrong |
|---|---|---|
| Active axis | Determines which axis actually responds to the wheel | The move is controlled, but on the wrong axis |
| Increment or scale | Determines how much travel each pulse commands | A coarse setting near the part creates an expensive surprise |
| Machine mode and position awareness | Confirms what the move means in the current situation | The operator trusts the wheel feel more than the machine state |
This is the heart of disciplined MPG use. The wheel can feel calm and controlled while still delivering the wrong result if the state around it was not confirmed first. A controlled move on the wrong axis is still a wrong move. A fine increment on the wrong reference is still an error.
Why Modern CNC Workflows Still Benefit from MPG Control
It is tempting to assume that as CNC systems become more automated, handwheels matter less. That assumption is only partly correct. Automation removes some manual tasks, but it does not eliminate the moments where humans must judge approach, confirm setup, or recover after interruption.
Real shops still deal with:
- First articles and prototypes
- Mixed fixtures and short runs
- Restarts after tool breakage
- Offset checks after unexpected stops
- Inspection and verification steps
In those moments, the handwheel often remains the calmest way to move the machine. Experienced operators continue to value it even on modern control packages because the more automated the cycle becomes, the more important it feels to have one manual tool that behaves proportionally when the machine leaves the routine path. Automation handles the repetitive work; the handwheel handles the judgment calls.
The MPG Supports Good Setup Practice Instead of Replacing It
One common misunderstanding is to treat the handwheel as a substitute for structured setup methods. That is not its role. Touch plates, tool setters, probing cycles, and sound fixture logic remain the foundation of repeatable setup. The handwheel supports those methods rather than replacing them.
For example, a touch plate may provide a more reliable work zero than visual estimation, but the operator still needs a calm way to approach that plate without rushing or overshooting. The MPG is often the best tool for that approach. The same applies to careful movement around workholding and to restart checks after interruptions.
The handwheel fits naturally beside structured zeroing practices such as touch-plate setup and repeatable zeroing. It is not competing with setup discipline. It is helping the operator execute that discipline with less stress and greater precision.
Recovery Work Is Where the Handwheel Proves Its Value
The easiest way to underestimate an MPG is to judge it only during normal production. Normal production minimizes manual motion by design. The real value appears when something stops being normal.
A broken tool, a stop for inspection, a restart after an alarm, or uncertainty about a safe return point all create moments where the operator needs the machine to move carefully without feeling overpowered by a fast jog command. That is where the handwheel becomes the most trusted interface on the machine.
It lets the operator rebuild confidence one controlled increment at a time instead of jumping immediately back into motion with a command method that feels too coarse for the situation. One careful restart can justify the feature more clearly than weeks of routine cutting. The cost of a single collision during a hasty restart often exceeds the value of the handwheel many times over.
Button Jogging and MPG Control Are Not the Same Experience
On a feature checklist, panel jogging and handwheel jogging can look redundant. In real use, especially near the part, they are not the same.
Button jogging asks the operator to translate intention into timed control input. The operator chooses a jog mode, holds or taps a button, and relies on release timing. An MPG turns the physical wheel rotation into the pacing device itself. That difference becomes obvious when the tool is close to the workpiece, fixture, or reference point.
Buyers should not dismiss the handwheel simply because the controller already offers manual jogging on screen or on keys. The question is not feature duplication. The question is whether the operator can stay calmer and more accurate during the most expensive manual moves. In practice, the proportional feel of a handwheel is distinctly different from the on-off nature of a jog button.
Where the MPG Adds the Most Value in Real Shops
The MPG is not equally important in every environment. Its real payoff depends on how often the workflow requires careful manual movement.
It tends to matter more in:
- Prototype and toolroom work
- First-article setup
- High-mix, low-volume production
- Fixture-heavy environments with tight clearances
- Shops training less-experienced operators
- Recovery-heavy workflows where interruptions are common
It tends to matter less in:
- Highly standardized production with fixed setups
- Mature nesting routines where manual close approach is rare
- Cells where probing handles most approach logic automatically
Even in those environments, many shops keep appreciating the feature because it pays for itself on the days when the normal flow breaks. A single avoided collision during an unusual event can justify the presence of the handwheel for years.
Pendant Versus Built-In Wheel Is a Workflow Question
The presence of an MPG is not enough by itself. How the operator uses it physically matters considerably.
A panel-mounted wheel can work well if the operator still has a clear view of the work area during use. A pendant can be better when it allows the operator to stand where sightlines and posture are safer. Neither layout is automatically superior. The real issue is whether the operator can watch the tool, understand the control state, and make the move without awkward body position or divided attention.
Buyers should judge the feature in person when possible. The same MPG logic can feel excellent on one machine and irritating on another because the human-use geometry changed. A pendant that forces the operator to look away from the work area to see the axis display may be worse than a well-placed panel wheel.
Training Should Tie Motion to Setup Logic
One weakness in some shops is teaching the handwheel as a motion device first and only later connecting it to offsets, restart logic, and work reference thinking. That order is risky.
The operator needs to understand not just that the wheel moves an axis, but what the machine believes about its current state, what reference is being approached, and why the move is being made. Otherwise the handwheel becomes a calmer way to make the wrong move.
Better training ties together:
- Axis selection
- Increment choice
- Current coordinate understanding
- Offset awareness
- The physical target being approached
When those pieces are trained together, the MPG becomes a setup-control tool. When they are taught separately, the operator may trust the feel of the wheel before confirming the machine state that gives that feel meaning. This is a training issue, not a hardware issue, but it determines whether the handwheel improves or complicates the workflow.
New Operators Benefit More Than the Spec Sheet Suggests
There is also a human-side productivity point. Newer operators often find button jogging too binary near the part. One touch feels too little, the next feels like too much. The handwheel gives them a more proportional relationship to movement. Used properly, that reduces panic, overshoot, and hesitating corrections.
Setup quality is not just a technical question. It is also a confidence question. A calm operator tends to make fewer rushed corrections and fewer last-second mistakes. In that sense, the MPG can improve setup behavior even if the actual movement is not faster in the narrowest cycle-time sense. For shops training new hires, the handwheel can shorten the learning curve for close positioning work.
Woodworking and Panel-Processing Applications
In industrial woodworking and panel processing, the question is usually not whether a handwheel is mechanically useful. The question is where it fits the operating routine.
A highly standardized nesting line may not rely on an MPG every hour. Once zoning, datum strategy, and setup methods are mature, much daily work may happen without delicate manual approach. But many woodworking operations are not that uniform. Custom cabinetry, mixed fixtures, setup verification, and restart events still create moments where careful human-scale movement matters.
In those environments, the MPG becomes less of a legacy feature and more of a precision recovery tool. It helps the operator approach stops, edges, references, and inspection points without turning every close move into a stressful panel-jog event. The practical question for a woodworking shop is how much deliberate manual positioning the real workflow still requires, not whether the machine looks modern without a handwheel.
What Buyers Should Test Before Deciding
The fastest way to judge handwheel value is not to debate it in the abstract. It is to test it against a real setup scenario.
Useful checks include:
- Can the operator clearly see the tool and reference while using it?
- Is axis selection easy to confirm and hard to misread?
- Are increment changes obvious before close approach?
- Does the physical placement support safe posture?
- Does the feature help during restart and recovery, not only during ideal-day setup?
These checks usually reveal the truth faster than opinion does. A shop may find it rarely needs the feature, or it may realize the handwheel improves operator control exactly where mistakes are most expensive. The evaluation should happen on the shop floor, with the actual operators who will use the machine.
The Practical Buying Conclusion
Pandaxis readers typically evaluate machinery by how it behaves during real setup, recovery, and production pressure rather than by how modern the feature list sounds. Under that standard, the handwheel matters whenever the workflow still contains moments where careful human-controlled motion is useful.
A CNC handwheel or MPG is a manual pulse generator that lets the operator move axes in deliberate increments during setup, touch-off, inspection, and restart. Its value is not nostalgia. Its value is control when the machine is closest to doing expensive damage.
The right buying question is not whether the wheel looks old. The right question is whether the workflow still contains high-risk inches of motion that benefit from calmer human control. In many real factories, the answer is still yes, and the MPG proves its worth exactly when the cycle stops being routine.