Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
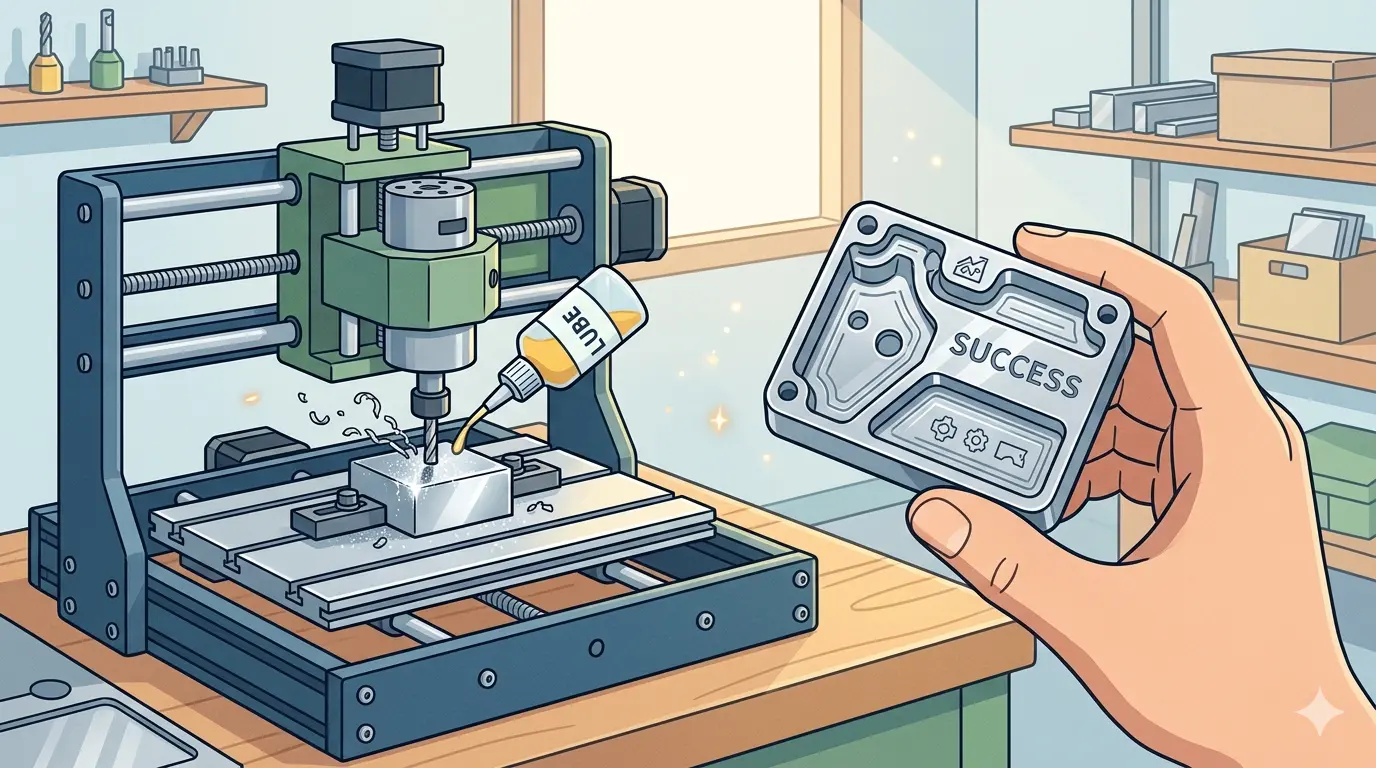
Before you tune spindle speeds or debate feed rates on a 3018, the real decision is whether your aluminum part belongs on that frame at all. This article separates realistic desktop work—learning coupons, small flat brackets, and one-off prototypes—from jobs that will collapse into chatter, chip recutting, and operator overload. It identifies the four failure patterns that destabilize light-machine routes first and explains why workholding and chip evacuation matter more than parameter debates. The key takeaway for production teams: judge the process by the tenth part, not the first, and recognize when the machine stops teaching and starts delaying real deadlines.
Start With Part Value, Not With the Word Aluminum
Before asking whether a 3018 can mill aluminum, ask why this specific part belongs on this specific machine. That question separates realistic work from expensive experiments faster than any specification sheet. A learning coupon, an internal fixture tab, and a repeat customer bracket may all be aluminum parts, but they do not ask the same thing from the machine.
The jobs that still make sense on a 3018 are usually the ones that can tolerate slow proving-out, close supervision, conservative toolpaths, modest finish expectations, and value measured in learning, prototyping, or internal use. If the part must ship repeatedly, look the same next month, and run without constant attention, the economics usually change before the machine capability changes.
What Usually Works Best
The aluminum work that fits a 3018 is normally small, flat, well-supported, and not too valuable to run slowly. Typical examples include learning coupons used to understand tool behavior, small prototype brackets or tabs, light internal fixture parts, thin flat plates with simple features, and one-off parts where the main return is design validation.
These jobs work because they let the operator stay conservative without destroying the purpose of the part. If the part still creates value while the cut stays light and carefully watched, the route can be reasonable.
A Quick Fit Table Tells the Truth Faster
| Aluminum Job Type | Fit on a 3018 | Why It Can Still Make Sense | What Usually Breaks the Route |
|---|---|---|---|
| Learning Coupons | Good | Cheap way to learn setup, sound, and chip behavior | Treating one good sample as production proof |
| Small Flat Internal Brackets | Fair to Good | Geometry is simple and support is usually manageable | Repeat runs become labor-heavy fast |
| One-Off Prototype Parts | Fair | Insight can justify slow cycle time | Prove-out burden grows if geometry changes often |
| Cosmetic Customer Parts | Weak | Sometimes technically possible | Finish consistency and repeatability become fragile |
| Deep Pockets, Tall Parts, or Demanding Tolerance Work | Poor | Very little reserve in the machine | Flex, recutting, and operator overload show up quickly |
This is the most useful meaning of “actually works.” It means the machine can finish the part with a level of stress and intervention that still makes sense.
What Usually Destabilizes the Route First
On a 3018, aluminum jobs usually break down through one of four failure patterns.
First, the stock is not supported honestly enough. Light machines do not forgive flex, tall clamps, or springy setups. The workholding that works fine for wood or foam becomes a liability the moment the cutter engages aluminum. A part that vibrates under load will recut chips, dull the tool faster, and produce a finish that changes with every pass.
Second, chips stop leaving the cut cleanly. Once recutting begins, sound, finish, and confidence usually degrade together. Aluminum chips are stringy and sticky compared to wood dust. They weld back onto the cutter, clog flutes, and turn a controlled cut into a rubbing, heating mess. On a machine with limited rigidity, that transition happens quickly and is hard to reverse mid-job.
Third, the tool stops cutting cleanly and starts rubbing. Aluminum punishes that much faster than forgiving materials do. A dull or chipped cutter on a 3018 does not just leave a poor finish; it pushes the machine into chatter, increases spindle load, and can break the tool entirely. The operator usually hears the change before seeing it in the part.
Fourth, the job itself is asking too many hard things at once. Deep engagement, small tools, tall stock, and commercial finish expectations can each be manageable alone. On a 3018, stacking them is where the route usually stops being sensible. The machine has no reserve capacity to absorb compounding errors.
Setup Rules Matter More Than Heroic Parameter Debates
If you want aluminum jobs to stay usable on a small machine, the broad strategy matters more than one perfect number set. Operators who spend hours debating spindle speed and feed rate while ignoring workholding and chip evacuation are optimizing the wrong variables.
The most practical rules are usually these:
- Keep parts small and well supported. Flat stock and short grip conditions are much easier to trust than tall or flexible setups. If the part extends far above the table or hangs off the edge of the spoilboard, the machine will amplify that instability.
- Treat chip clearing as part of the cut. If chips stay in the cut, the route is already drifting toward noise, finish loss, and tool trouble. Compressed air, a vacuum attachment, or simply pausing to clear chips manually are all valid strategies, but they need to be planned before the job starts, not improvised mid-cut.
- Prefer simple geometry over impressive geometry. Light profiles, shallow features, and clear tool access are where small aluminum work stays most believable. Deep pockets, thin walls, and intricate details multiply the chances of deflection and tool breakage.
- Stop using a tool that has started rubbing. Desktop aluminum routes do not have much spare stiffness to hide weak cutting action. If the cutter is no longer shearing cleanly, replace it. The cost of a new tool is almost always lower than the cost of scrapped material and wasted time.
- Judge the method by repetition, not by one good bracket. The tenth part is usually more honest than the first one. If the process only works when the operator is fully focused and the stars align, it is not a process yet.
What a Stable Cut Feels Like
A healthy aluminum cut on a 3018 usually feels uneventful. The sound stays controlled, the chips leave the cut, and the part looks connected to a method you could repeat later. The spindle note is steady, the machine frame is quiet, and the operator can watch the cut without hovering.
A weak cut feels different. The machine sounds tense, the finish changes with the path, and the operator spends more time reacting than trusting. That does not always mean failure is seconds away. It does mean the process is already borrowing confidence from the operator instead of generating it on its own.
That distinction matters because many users mistake “it survived” for “it works.” On a desktop machine, those are not the same standard. Surviving means the cut finished without breaking anything. Working means the cut finished predictably, with acceptable quality, and without requiring constant intervention.
Know When You Are Buying Insight Instead of Output
Many aluminum jobs on a 3018 are worth doing precisely because they teach the owner where the machine becomes uncomfortable. That is real value. It helps a shop understand how much setup honesty, chip control, and rigidity the material actually demands. An operator who has pushed a 3018 through aluminum understands why production shops invest in heavier frames and more rigid spindles.
The mistake is treating that learning value as proof that the machine is now a routine aluminum solution. If the route still needs constant supervision, frequent adjustment, and generous patience, the machine may be a good teacher and a weak production tool at the same time. The insight gained is valuable; the output produced is not necessarily commercial-grade.
Low Machine Price Can Hide High Process Cost
One reason owners keep pushing a 3018 into aluminum work is that the machine is already on the bench and the purchase price looked attractive in the first place. That can hide the real economics. Aluminum work on a small machine often accumulates cost through operator attention, repeated proving-out, shortened tool life, setup correction, scrap, deburring, and extra inspection.
That hidden cost matters most after the first few successful parts. Early wins are easy to overvalue because the geometry is chosen carefully and the operator is fully engaged. The important test is the routine case. If the same job comes back again, is this still the best use of time?
That is where buyers should stop asking what the machine can do in theory and start asking what the workflow costs in practice. If every acceptable result depends on unusually high supervision, the low machine price has already become less meaningful. The true cost per part includes the operator’s attention, and that attention has a real value.
At that point, the better comparison is not against doing nothing. It is against what a calmer machine class would save in setup time, scrap exposure, and operator energy. That is also why it helps to step back and ask what industrial CNC equipment is actually worth paying for once the aluminum work starts carrying real deadlines.
Know the Point Where the Machine Stops Teaching and Starts Delaying
There is usually a clear point where the 3018 is no longer being used to learn or prototype, but to protect real deadlines. That is when the platform begins carrying a role it was not selected to carry well. The transition is gradual, but the signs are consistent.
The warning signs are usually easy to recognize:
- Chatter keeps returning even after careful setup. No amount of speed adjustment or tool selection eliminates it.
- The operator cannot comfortably leave the machine during the cut. Every pass requires presence, and leaving the shop floor for even a few minutes feels risky.
- More accessories or adjustments are being added, but the route is still fragile. Stiffer springs, different clamps, new tool holders, and modified dust shoes all help marginally, but the fundamental instability remains.
- Inspection, deburring, or cleanup is wiping out the value of making the part in-house. The machining time is short, but the manual finishing and verification time is not.
- The same job would become painful immediately if volume doubled. The process has no headroom, and any increase in demand would require a different approach entirely.
When those signs appear, the next useful decision is rarely another small adjustment. It is a broader equipment decision built around rigidity, repeatability, and the value of a calmer process. If replacement is becoming realistic, buyers should compare machinery quotes line by line instead of reacting only to surface specifications. The calmer route is not always the cheapest line item, but it is often the cheaper process.
The Real Answer
A 3018 can mill aluminum. What actually works on it is small, conservative, well-supported, and closely watched. That makes the machine useful for learning, prototyping, and selective low-risk parts where patience is part of the plan. The machine is a legitimate tool for understanding what aluminum demands from a cutting process.
It becomes the wrong answer when aluminum work has to be routine, commercially dependable, and calm enough that the operator is not constantly rescuing the cut. At that point, the productive move is usually not another round of bench-top tuning. It is a more honest machine-selection decision built around process stability rather than possibility. For shops that have outgrown the desktop class, reviewing industrial CNC options with real rigidity and spindle capacity is the practical next step.
Use the 3018 to understand what aluminum demands. Do not use it as a reason to delay admitting when the workload already needs a different class of machine. The desktop machine has a legitimate role in the shop, but that role is teaching and prototyping, not sustained production.