Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
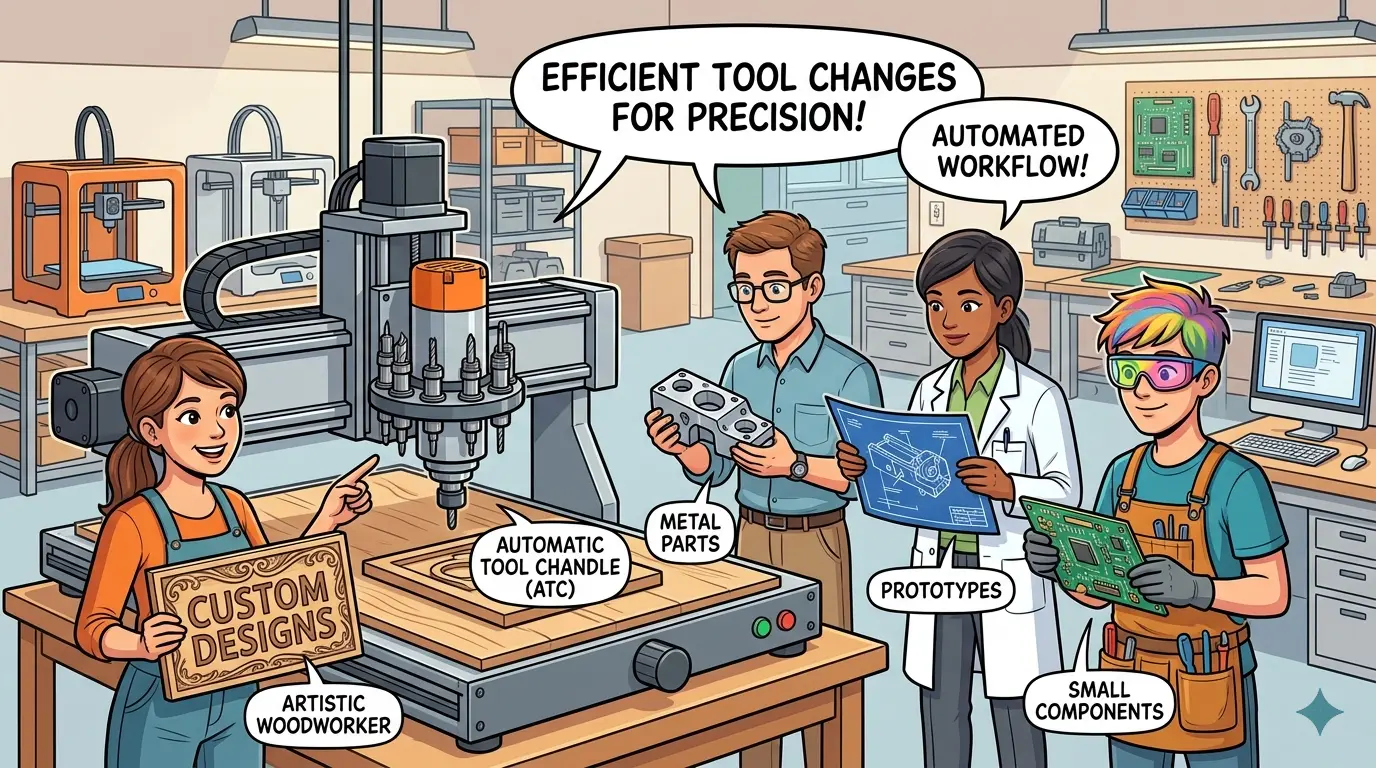
Before you spec a small ATC spindle for a compact CNC router or mill, stop counting tool pockets and start counting interruptions. This article forces that shift by framing the purchase around measurable production drag rather than automation prestige. It walks through the real decision criteria: how many manual wrench changes occur per shift, whether your base machine holds tolerances well enough to justify multi-tool sequencing, and whether your team can manage holders, offsets, and magazine discipline. The core question is whether the spindle recovers visible lost minutes or simply adds complexity to a workflow that never asked for it.
Start With the Interruption, Not the Automation
A small ATC spindle is a compact automatic tool-change system designed for smaller CNC routers, mills, or prosumer platforms. It brings multi-tool automation to machines that would otherwise require manual wrench changes between operations. The appeal is straightforward: fewer stops, less operator hovering, and the ability to run multi-tool jobs without babysitting every cutter swap.
But the buying decision should not start with whether automatic tool changing sounds convenient. It should start with whether your machine is actually losing meaningful time to manual changes. The value of a small ATC spindle is tied directly to cycle interruption—not to how professional the feature looks on a spec sheet.
What a Small ATC Spindle Actually Changes
The obvious difference is automatic tool changing. The operational difference is larger than that. Once ATC enters the picture, you are no longer managing spindle rotation. You are managing a tooling system.
That shift brings new daily responsibilities:
- Tool holders become part of routine planning rather than an afterthought.
- Offsets require disciplined management and consistent measurement.
- Tool pocket or magazine positions matter on every job, not just complex ones.
- Error recovery becomes a defined procedure instead of an improvised fix.
- Multi-tool job planning gets easier, but sloppy organization becomes less forgiving.
A small ATC spindle is therefore a workflow change, not just a spindle upgrade. The hardware may be compact. The process discipline it demands is not.
The Strongest Justification Is a Repeated Annoyance
The cleanest ATC decisions are built on a pattern the shop already recognizes. The operator keeps stopping to swap tools. Multi-tool parts keep breaking flow. Small jobs that should feel fast keep feeling slow because manual changes dominate actual cutting time.
Once those interruptions are visible, the case for ATC becomes concrete. The feature is no longer abstract automation. It is an answer to lost minutes that already exist on the shop floor.
Without that pattern, a small ATC spindle can still be attractive, but it becomes much harder to defend as a practical investment.
Who Actually Benefits Most
Small ATC spindles help most in shops where the work already behaves like multi-tool production. Typical candidates include:
- Cabinet or panel routing jobs that require several operations per part.
- Sign or parts work that moves through multiple cutters in a single cycle.
- Compact production environments where one operator covers several responsibilities and every manual interruption pulls attention away from other tasks.
The feature is not strongest where people are most excited by automation. It is strongest where the cycle already proves that automation belongs there.
Who Should Skip It
Not every machine needs ATC. Shops that spend most of their time with one cutter, one operation, or very simple tool sequences often gain less than they expect. The strongest ATC case appears when several conditions line up at once:
- Parts use multiple tools regularly.
- Manual changes interrupt output often enough to be noticed.
- The machine is already rigid and accurate enough to justify more complex multi-tool workflows.
- The shop is willing to manage holders, offsets, and magazine discipline properly.
The deciding factor is not whether ATC sounds professional. It is whether tool-change frequency is already a visible production drag.
The Trap: Buying the Feature, Not the Outcome
Compact ATC systems can look like a clean step toward industrial capability. They borrow the language and convenience of larger machines, which makes them easy to admire. But admiration is not ROI.
If the machine only rarely changes tools, a small ATC spindle may become more of a machine-identity feature than a productivity feature. The owner pays for extra complexity without reclaiming enough real time to justify it. That does not mean the system is bad. It means the cycle did not ask for it strongly enough.
The Base Machine Still Has to Be Worth Automating
A small ATC spindle makes sense on a machine that already holds tolerances and process discipline well enough to benefit from faster multi-tool sequencing. If the platform is still limited by rigidity, motion quality, or basic setup stability, automation may make the machine more convenient without making it more commercially convincing.
Good buyers look at the whole platform, not just the spindle. Faster tool changing is only valuable if the rest of the machine can turn that convenience into predictable output.
What to Count Before You Shop
The best place to start is with a simple count:
- How many tools does a normal job actually use?
- How many manual tool changes happen per shift?
- How much operator attention is lost to those changes?
- How often does the tool sequence interrupt otherwise smooth work?
These are not glamorous questions, but they are the right ones. They tie the decision to the actual rhythm of production. If the answers show repeated interruption, ATC has a practical case. If they do not, the feature may be interesting but not urgent.
Estimating Payback Without a Financial Model
Buyers do not need a polished financial model to make a better ATC decision. A simple workflow estimate is often enough. Count how many times a typical job stops for a tool change. Estimate how long each interruption really takes once wrenching, restarting, checking, and re-centering operator attention are all included. Multiply that across a shift, a week, or the actual part families that keep returning.
This simple exercise often reveals whether the spindle is solving a real bottleneck or only a theoretical one. If the time recovered is small, the feature may not be urgent. If the interruption cost keeps accumulating across jobs, then ATC starts looking less like a luxury and more like a workflow correction.
The practical advantage of compact ATC buying is that the best justification is usually visible before the spindle is purchased. The shop can already see the lost minutes if it is willing to count them honestly.
Moderate Volume Can Still Justify the Feature
Some buyers assume ATC only makes sense in high-volume production. That is too narrow. Compact ATC can also be justified in moderate-volume environments when:
- One operator covers too many tasks and cannot afford to stand at the spindle during every change.
- The machine handles repeated multi-operation parts where tool sequencing is predictable.
- Setup interruptions create fatigue and inconsistency out of proportion to the official volume numbers.
In those cases, the gain is not only cycle-time reduction. It is also smoother workflow management. The machine can move through more of the routine itself while the operator handles inspection, loading, unloading, or another machine. For smaller shops, that flexibility can matter almost as much as the raw time savings.
The key remains the same: the feature should answer a repeated interruption pattern that the shop already experiences.
When Compact ATC Becomes Overhead
The opposite case is equally important. A small ATC spindle can become overhead when:
- The work is mostly simple and the tool count stays low.
- The team is not prepared to manage holders, offsets, and tool organization with discipline.
- Recovery procedures are improvised rather than documented.
In that environment, the spindle may reduce a few manual motions while adding a larger burden of inventory control, pocket management, and recovery procedures. Compact ATC is not automatically the right next step for every smaller CNC machine. It is the right step when the workflow is already structured enough to benefit from it. If the shop still struggles with basic tool control, the feature can expose that weakness rather than solve it.
Ownership Changes, Not Just Capability
Once the spindle changes tools automatically, the shop owns a new layer of discipline. Holder inventory, pocket management, offset control, tool-length consistency, and recovery routines all matter more than they did before.
This is one reason some buyers overestimate the gain. They imagine only the convenience side of ATC and underestimate the organizational side. Compact tool automation rewards shops that already think systematically about tooling. It is less forgiving in environments where tool control is loose and process recovery is improvised.
That does not make the feature unsuitable for smaller shops. It simply means the shop has to be ready to own the system, not just admire the spindle.
How to Place the Decision in Your Production Context
ATC logic matters in production-oriented woodworking and router throughput discussions. Small ATC spindles sit in the space where a compact machine starts borrowing some of the workflow logic of larger automated equipment. If you are evaluating whether your machine class and workload justify more serious automation spending, the useful habit is to keep the feature connected to production rhythm rather than to specification prestige. For shops working through this decision, reviewing the range of CNC and production equipment options can help clarify what level of automation actually fits the work you are running.
Questions to Ask Before Paying for It
The most useful questions are ordinary ones:
- How many tools does a typical part really need?
- How much time is manual changing costing now?
- Is the base machine good enough to exploit multi-tool automation?
- Is the team ready to manage holders and offsets properly?
- Would the same budget solve the bottleneck better somewhere else?
These questions usually tell the truth faster than any spindle brochure. They force the buyer to decide whether the spindle is solving a visible workflow problem or only promising a nicer-looking machine.
The Best Use Case Is Repeated Multi-Tool Friction
A small ATC spindle is strongest when the machine already suffers from repeated multi-tool friction. That might mean cabinet parts that run several operations in sequence, panel work that keeps stopping for tool swaps, or compact shop workflows where the operator’s time is already split across several tasks.
In those cases, the spindle is not an indulgence. It is a practical response to an established bottleneck. Once the shop can state the lost minutes clearly, the feature becomes easier to justify and easier to evaluate after installation.
What Good Small-ATC Adoption Looks Like
Good adoption usually looks organized rather than dramatic. The shop knows which recurring jobs need multiple tools. Holder lengths are controlled. Offsets are not treated casually. Tool pockets are assigned with intention. Operators understand recovery steps when a cycle is interrupted. None of this is glamorous, but all of it determines whether the compact ATC spindle feels like a productivity upgrade or a fussy subsystem.
That is why the best buyers do not stop at “who needs one?” They also ask “are we ready to run one well?” When the answer is yes, compact ATC can be very useful. When the answer is no, the machine may become more complicated before it becomes more productive.
Buy It to Recover Time, Not to Signal Advancement
A small ATC spindle is a compact automatic-tool-change system meant to bring multi-tool automation into smaller CNC platforms. It can be very useful when the machine repeatedly stops for manual tool changes and those interruptions are already limiting output.
Its value weakens fast when the machine mostly runs one or two simple tools or when the buyer cannot point to the time problem it is meant to solve. That is the safest rule to use: buy compact ATC to recover repeated lost minutes, not to make the machine look more advanced than the workflow actually requires.