Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
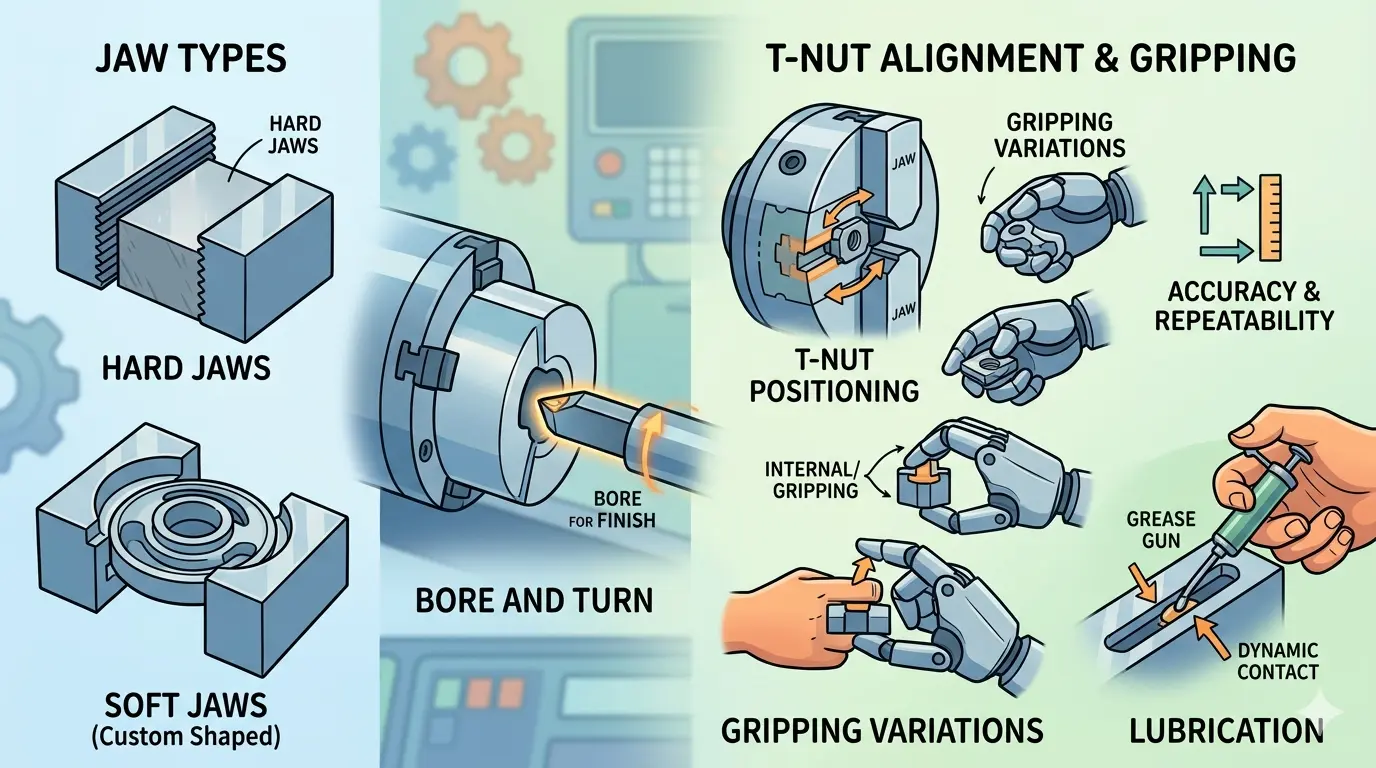
CNC jaw setting rarely announces itself as the culprit when turned parts drift, chatter, or show taper; it masquerades as program error, insert wear, or spindle trouble, sending shops down the wrong diagnostic path. This article forces that issue into the open by treating chuck-jaw preparation as a formal process-control step rather than a setup habit. For production engineers and factory managers, the stakes are concrete: grip diameter, contact pattern, clamping force, and grip length must match the part geometry and cutting load, or thin-wall parts distort, re-chucked features lose concentricity, and repeat jobs quietly degrade. Judge the grip before you blame the machine.
Why Jaw Setting Deserves Process-Control Status
CNC jaw setting is the controlled preparation of chuck jaws so a turned part is gripped in the correct location, with the right contact pattern, and with enough repeatability to survive the cut without slipping or distorting. On paper that sounds routine. On the shop floor it is one of the fastest ways to turn a stable process into an unreliable one.
When jaw setting is wrong, the symptoms often look like something else. Operators start chasing offsets, inserts, spindle condition, or program changes when the real problem started at the chuck. That is why jaw setting deserves to be treated as a process-control step, not as a minor setup habit.
What Jaw Setting Actually Covers
Jaw setting is broader than simply tightening the chuck. In day-to-day turning work it usually includes:
- Selecting hard jaws, soft jaws, liners, or a custom jaw arrangement.
- Deciding the grip diameter and grip length.
- Defining where the contact band will sit on the part.
- Choosing a clamping force that holds without over-distorting.
- Boring soft jaws under the right conditions for repeat jobs.
- Checking whether the part repeats after multiple reload cycles.
Each of these choices affects how honestly the part is being held. The jaw does not merely stop the part from falling out. It locates the workpiece, resists cutting load, and can add distortion before the tool even touches the material.
Bad Jaw Setting Usually Appears As A Different Problem
One reason the topic is misunderstood is that poor jaw setting rarely announces itself clearly. The part may show runout, chatter, taper, finish variation, or drift from piece to piece even when the machine and program look healthy.
That makes troubleshooting slower than it should be. Shops that handle turning well usually check workholding early because grip errors can make a good machine look unstable.
A Symptom Table Helps Narrow It Down Faster
| Shop Symptom | Jaw-Setting Risk Worth Checking First |
|---|---|
| Part runs out differently after each reload | Inconsistent jaw contact or poor repeatability |
| Thin-wall part goes out of round after clamping | Too much clamping force or poor contact pattern |
| Part moves under heavier load | Too little grip length or wrong jaw choice |
| First piece is good, later pieces drift | Jaw wear, contamination, or unstable loading practice |
| Operators keep adjusting offsets | Workholding variation masquerading as program error |
The table does not prove every problem starts at the chuck. It simply shows why jaw setting belongs near the top of the diagnostic list.
Contact Pattern Matters More Than Many Shops Admit
Good jaw setting is not about holding hard. It is about holding correctly. The contact area needs to support the part geometry without concentrating force so heavily that it bends, marks, or distorts the work.
A setup that feels secure on a thick blank can be completely wrong for a thin-wall tube, a short grip part, or a component that will be re-chucked later. This is why soft jaws are so common on repeat precision work. They are not a ritual. They let the contact pattern match the part more honestly.
Hard Jaws, Soft Jaws, And Liners Solve Different Problems
Shops often talk about jaw selection as if there is one correct default. There is not.
- Hard jaws are durable and practical, but they are not automatically best for precision repeat work.
- Soft jaws are useful when the part family justifies machining the contact to match the geometry.
- Liners or special contact solutions help when marking, odd shapes, or fragile surfaces are the main risk.
The correct choice depends on the part family, the material, the expected repeat volume, and the distortion risk. Habit is a poor decision rule here.
Grip Length And Clamping Force Must Match The Cut
Many jaw-setting mistakes come from a simple mismatch between how the part is gripped and how the cut loads the workpiece. Too little grip length can allow movement. Too much clamping force can deform the part before machining starts. Interrupted cuts, thin sections, short parts, or higher cutting forces all narrow the safe window.
For that reason, jaw setting cannot be reduced to “tight enough.” The grip must suit the geometry and the cutting load. Otherwise the chuck either holds dishonestly or damages the part while trying to hold securely.
Re-Chucking Often Exposes Weak First-Op Thinking
Secondary operations are where a careless jaw decision often becomes expensive. If the part must be flipped, re-gripped, or aligned from a machined feature, the first jaw-setting choice needs to protect those later requirements.
This is one reason good setup planning starts with the full route, not the first clamp only. A grip that looks fine for first-op metal removal can create second-op concentricity trouble, jaw marks on a future datum, or poor access to the surfaces that actually need control.
Repeat Work Should Not Depend On Memory
Once a turning job repeats, proven jaw logic should be captured. Useful setup records often include:
- Jaw type and identification.
- Grip diameter.
- Contact location.
- Soft-jaw boring condition.
- Special support or loading notes.
- The inspection point that confirmed the setup was repeating correctly.
That documentation does more than shorten setup time. It reduces operator variation and makes troubleshooting much faster when the process drifts.
Soft-Jaw Success Depends On Matching Conditions, Not Just Part Number
Shops sometimes say they are using soft jaws correctly when what they really mean is that the jaws were once bored for a similar job. That is not enough. Soft-jaw preparation only protects repeatability when the boring condition, clamping state, and support assumptions still match the live production setup.
Changes in raw-stock tolerance, grip length, clamping practice, or secondary-op routing can make an older jaw setup less truthful than it once was. The failure is usually subtle. It often appears as creeping repeatability loss rather than an obvious crash or catastrophic defect.
Buyers Should Ask Suppliers About Workholding, Not Just Tolerance Claims
When buyers outsource turned parts, they often focus on machine lists, quoted tolerances, or lead time. Those things matter, but workholding discipline matters too. A supplier that cannot explain how it grips thin-wall parts, protects awkward geometry, or controls repeatability through reloads is still a process risk even if the quotation looks polished.
This is where supplier screening overlaps with broader sourcing discipline. Buyers comparing turning suppliers may also want to review how to compare precision turning partners beyond simple capability claims and how to compare machinery or supplier quotes without missing hidden risk.
Judge The Grip Before You Blame The Program
CNC jaw setting is the controlled preparation of chuck jaws so turning work is gripped accurately, repeatably, and honestly for the operation. Its importance is practical: poor gripping can imitate many other failures and send the shop in the wrong diagnostic direction.
The simplest rule is still the best one. Judge the grip before blaming the program, the insert, or the machine. If the jaw setting is wrong, the whole route is standing on a weak foundation.
How Jaw Setting Interacts With Machine Condition
Jaw setting does not happen in isolation. The chuck mounts to the spindle, and the spindle carries the workholding system. If the chuck body, mounting bolts, or spindle nose have wear or contamination, even a perfectly prepared jaw set will not hold true. Shops that treat jaw setting as a standalone ritual often miss the interaction between the chuck and the machine.
Check the chuck mounting surface for burrs, chips, or rust before you install jaws. Verify that the chuck bolts are torqued to the manufacturer’s specification, not just “tight.” A loose chuck body can introduce runout that looks like a jaw problem but is actually a mounting problem. Similarly, the spindle nose taper or flange face must be clean and free of nicks. A small chip under the chuck can tilt the entire workholding system and create a taper that no amount of jaw adjustment will fix.
This is why a complete jaw-setting procedure includes a quick inspection of the chuck and spindle interface. It takes minutes and prevents hours of chasing a phantom problem. Shops that skip this step often find that their “jaw setting” issues disappear after a thorough cleaning and re-torquing of the chuck mounting.
Clamping Force: The Balance Between Hold And Distortion
Clamping force is not a single number that works for every job. It depends on the part material, wall thickness, grip diameter, and the cutting forces expected during the operation. A thick steel blank can handle high clamping force without distortion. A thin-wall aluminum tube will collapse or go out of round with the same force.
Many modern CNC lathes allow the operator to set clamping pressure through the machine control. This is a valuable feature, but only if the operator understands what pressure to use. Start with the chuck manufacturer’s recommendations for the jaw type and grip diameter, then adjust based on the part’s sensitivity. For thin-wall parts, reduce pressure until the part holds securely without visible deflection. You can check deflection with a dial indicator on the part OD before and after clamping.
The cutting force also matters. A heavy roughing pass on a large diameter generates significant torque and radial force. The clamping force must be high enough to prevent the part from slipping in the jaws. But if the part is thin-wall, you may need to balance roughing parameters against clamping force. Reduce depth of cut or feed rate to keep the cutting force within what the grip can safely resist without distortion.
Interrupted cuts are a special case. When the tool hits a keyway, hole, or other discontinuity, the cutting force spikes momentarily. The jaws must absorb that shock without allowing the part to shift. This often requires higher clamping force than a continuous cut would suggest. If the part cannot tolerate that force, consider a different workholding strategy, such as a steady rest or a custom fixture that spreads the load.
Grip Diameter And Its Effect On Runout
The grip diameter is the diameter at which the jaws contact the part. It is not always the same as the part’s nominal diameter. For example, if you are gripping a part with a machined shoulder, the jaws may contact the shoulder rather than the full OD. The grip diameter determines the lever arm for the clamping force and the contact area available.
A larger grip diameter generally provides more stability because the jaws have more surface area in contact with the part. However, it also means the clamping force is applied farther from the part’s centerline, which can increase the bending moment on thin sections. A smaller grip diameter concentrates the force closer to the center, which can be better for thin-wall parts but may not provide enough grip area for heavy cuts.
The relationship between grip diameter and runout is also important. If the jaws are bored to a diameter that does not match the part’s actual OD, the contact will be uneven. The part may sit on three high spots rather than across the full jaw face. This creates a three-lobed clamping pattern that shows up as runout on the machined surface.
To avoid this, bore the soft jaws to the actual grip diameter, not the nominal part size. Measure the part OD at the grip location and bore the jaws to that dimension with a small allowance for the clamping action. The jaws should contact the part across the full width of the jaw face, not just at the edges.
Grip Length: How Much Is Enough
Grip length is the axial distance over which the jaws contact the part. It is determined by the jaw width and the part geometry. A longer grip length distributes the clamping force over a larger area, reducing the risk of local deformation and improving stability against bending moments.
For short parts, the grip length is limited by the part itself. If you only have 10 mm of material to grip, you cannot create a 30 mm grip length. In that case, you need to consider whether the part can be held securely at all with a standard chuck. Options include using a collet chuck, a custom jaw with a longer contact surface, or a fixture that supports the part from the end.
For longer parts, the grip length should be as long as practical without interfering with the machining operation. A longer grip length also helps with concentricity when the part is re-chucked for a second operation. If the first operation grips a short section, the second operation may not have enough material to grip accurately.
A common mistake is to grip only the minimum length needed to hold the part for the first cut. This can work for a simple facing operation, but it fails when the part must be turned along its full length or when the cutting forces are high. The part can deflect or shift, causing taper or runout that is difficult to trace back to the grip.
Soft Jaw Boring: Process Conditions That Matter
Boring soft jaws is a common practice, but the conditions under which the jaws are bored determine how well they will hold the part. The jaws should be bored while mounted on the chuck, at the same clamping pressure that will be used in production. If you bore the jaws at low pressure and then clamp at high pressure, the jaw bores will expand and the contact pattern will change.
The boring operation should also be done at the same spindle speed and feed rate that will be used for the production job, or as close as practical. This ensures that any centrifugal effects on the jaws are accounted for. At high spindle speeds, the jaws can expand slightly due to centrifugal force, which changes the grip diameter. If the jaws are bored at low speed and used at high speed, the grip will be too tight or too loose.
The tool used for boring should be sharp and rigid. A dull tool can push the jaws slightly, creating a taper in the bore. The bore should be straight and parallel to the spindle axis. Check the bore with a dial indicator after boring to confirm that it is true.
Finally, the jaws should be bored to the correct diameter for the part. This is not always the same as the part OD. If the part has a tolerance band, you may want to bore the jaws to the midpoint of the tolerance so that the grip is consistent across the tolerance range. If the part is a casting or forging with significant size variation, you may need to bore the jaws to the largest expected size and use a different clamping strategy for smaller parts.
Jaw Wear And Contamination: The Slow Drift
Jaw wear is a gradual process that is easy to miss. The jaw teeth or serrations wear down, the contact surface becomes polished, and the grip becomes less secure. The part may start to slip under heavy cuts, or the runout may increase slowly over time.
Contamination is another culprit. Chips, coolant residue, and dirt can accumulate on the jaw faces or in the chuck mechanism. This changes the effective grip diameter and can cause the part to sit at an angle. A quick visual inspection before each job can catch most contamination issues. Wipe the jaw faces clean and check the chuck mechanism for debris.
The frequency of jaw replacement depends on the material being machined, the clamping pressure, and the number of cycles. Abrasive materials like cast iron or hardened steel wear jaws faster than aluminum or brass. High clamping pressure accelerates wear. A shop that runs the same job continuously may need to replace jaws more often than a job shop that changes setups frequently.
A good practice is to include jaw inspection in the preventive maintenance schedule. Check the jaw faces for wear, the serrations for damage, and the chuck mechanism for smooth operation. Replace jaws that show significant wear before they cause quality problems.
Documenting Jaw Settings For Repeat Jobs
The value of documentation becomes obvious when a job returns after weeks or months. Without a record, the operator has to rediscover the correct jaw setting through trial and error. With a record, the setup is straightforward and the first piece is likely to be correct.
A useful setup record includes more than just the jaw part number. It should include the grip diameter, the clamping pressure, the contact location, and any special notes about loading or support. It should also include the inspection point that confirmed the setup was correct. This could be a specific dimension, a runout reading, or a surface finish requirement.
The record should be stored where the operator can find it easily. This could be in the machine control, in a setup sheet, or in a digital work instruction system. The key is that the information is available when the job is set up again.
Documentation also helps with troubleshooting. If a job that used to run well starts producing bad parts, the setup record provides a baseline. The operator can compare the current setup to the documented setup and identify what has changed. This is much faster than starting from scratch.
Training And Operator Skill
Jaw setting is a skill that improves with practice and understanding. A new operator may know how to load a chuck but not understand why the grip diameter matters or how clamping pressure affects distortion. Training should cover the principles behind jaw setting, not just the steps.
A good training program includes hands-on practice with different jaw types, different part geometries, and different materials. The operator should learn to recognize the symptoms of poor jaw setting and know how to correct them. They should also learn to use measuring tools like dial indicators and bore gauges to verify the setup.
Cross-training is also valuable. If one operator is the only person who knows how to set up a particular job, the shop is vulnerable when that operator is absent. Documenting the setup and training others reduces that risk.
Supplier Evaluation: Workholding Discipline As A Screening Criterion
When a buyer evaluates a turning supplier, workholding discipline is a legitimate screening criterion. A supplier that cannot explain its jaw-setting procedures may struggle with repeatability, especially on complex or thin-wall parts. The buyer should ask specific questions about how the supplier handles different part geometries and materials.
Questions to ask include: How do you set clamping pressure for thin-wall parts? How do you ensure concentricity when a part is re-chucked? What is your procedure for boring soft jaws? How do you document setups for repeat jobs? The answers reveal the supplier’s level of process control.
The buyer should also look for evidence of workholding discipline in the supplier’s quality records. If the supplier tracks scrap and rework by cause, workholding issues should appear as a category. If the supplier cannot provide this data, it may not have the process visibility needed for reliable production.
Practical Steps To Improve Jaw Setting Today
Improving jaw setting does not require new equipment or a major investment. It starts with a few practical steps that any shop can implement:
- Create a standard procedure for jaw installation and inspection.
- Train operators on the principles of grip diameter, grip length, and clamping force.
- Document setups for repeat jobs, including jaw type, grip diameter, and clamping pressure.
- Include jaw inspection in the preventive maintenance schedule.
- Use dial indicators to verify runout after jaw installation.
- Bore soft jaws under production conditions, not as a separate operation.
- Monitor clamping pressure and adjust for thin-wall or fragile parts.
These steps do not require a large budget. They require discipline and attention to detail. The payoff is a more stable process, fewer rejected parts, and less time spent troubleshooting problems that originate at the chuck.
The Bottom Line On CNC Jaw Setting
CNC jaw setting is not a minor setup detail. It is a process-control step that affects every part that comes off the machine. When the jaws are set correctly, the part is held accurately, repeatably, and without distortion. When they are set incorrectly, the consequences show up as runout, taper, chatter, or drift that is easy to misattribute to other causes.
The practical rule is simple: judge the grip before blaming the program, the insert, or the machine. If the jaw setting is wrong, the entire operation is built on an unstable foundation. Investing time in jaw setting, documentation, and operator training pays off in reduced scrap, faster setups, and more reliable production.