Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
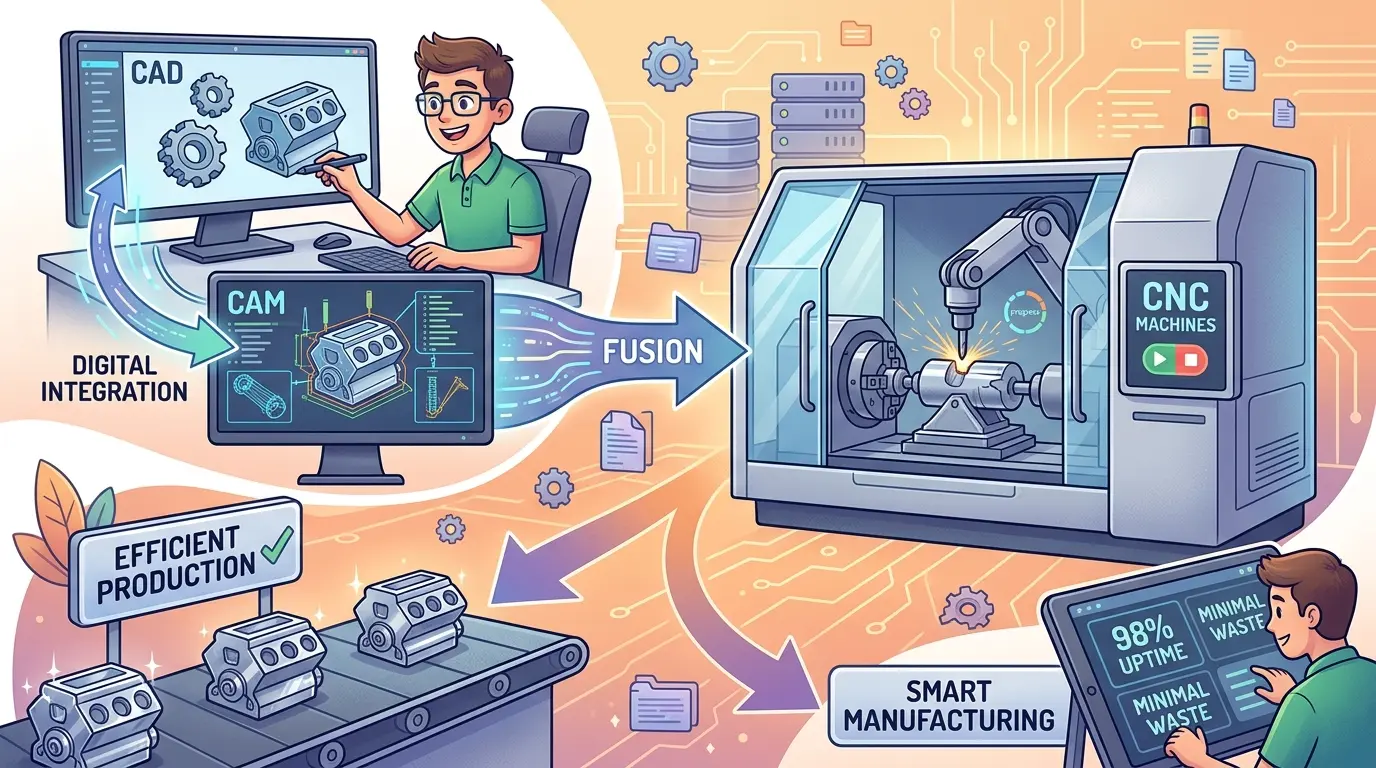
When a programmer, production manager, and purchasing agent each hear “Fusion CNC” differently, quoting and equipment decisions stall before they start. This article unpacks that ambiguity by separating the CAD/CAM software environment from integrated workflow shorthand and from casual search behavior. For shops evaluating whether design-to-toolpath handoffs justify a software standard, the distinction matters: postprocessor reliability, revision handling, and training burden are operational facts, while compatibility claims remain vague until tested on a real job. Clarify which meaning applies before comparing subscriptions against machine specifications, or you will waste hours solving the wrong problem.
Why “Fusion CNC” Causes Confusion on the Shop Floor
Walk into any production meeting and say “Fusion CNC,” and you will likely get three different interpretations from three different people. The programmer hears a CAD/CAM environment. The production manager hears a workflow promise. The purchasing agent hears a compatibility claim to verify in a quotation. Everyone believes they are aligned. They are not.
This ambiguity is not a minor terminology issue. It directly affects how teams evaluate software, compare machine options, and set workflow expectations. When the phrase is left undefined, shops waste hours comparing software subscriptions against machine specifications as if they were the same decision. They are not, and the cost of that confusion shows up in delayed quoting, mismatched equipment purchases, and rework caused by unclear handoffs.
Three Distinct Meanings Behind the Same Phrase
In practice, “Fusion CNC” almost always points to one of three situations:
- A team discussing CNC programming work that runs through a Fusion-based CAD/CAM environment.
- A programmer or manager describing an integrated design-to-toolpath workflow, using the software name as convenient shorthand.
- A buyer or researcher typing familiar software language into a search bar while investigating machines, posts, or production methods tied to a software ecosystem they already know.
Each meaning leads down a different decision path. The software interpretation raises questions about model handling, postprocessor behavior, and revision flow. The workflow interpretation raises questions about handoffs and standardization. The search interpretation raises questions about machine categories and process fit. Until the group agrees on which meaning applies, every subsequent discussion is built on a shaky foundation.
The Software Meaning Is the Most Technically Accurate
In day-to-day usage, the most precise reading of “Fusion CNC” is software-centered. The phrase usually refers to CNC programming or machining workflow built around a Fusion CAD/CAM environment. The discussion then centers on model handling, toolpath preparation, revision management, postprocessor behavior, and how design changes translate into manufacturing output.
This interpretation is useful because it points to a real operational question: does the integrated environment reduce enough friction to justify how the team currently works? For shops handling frequent revisions or mixed production runs, the answer can be genuinely valuable. For stable, high-volume routines, the answer may be less compelling.
Search Behavior Makes the Term Less Precise
Outside the programming desk, the term becomes sloppier. Searchers often combine a known software name with a manufacturing term when they are not fully certain whether they need a machine, a workflow explanation, a postprocessor answer, or training guidance. That means “Fusion CNC” shows up in machine research even when the software environment is only one part of the buyer’s actual uncertainty.
This matters because the search term can sound narrower than the real commercial question behind it. A buyer searching for “Fusion CNC machine” may actually be trying to determine whether their existing programming skills transfer to a new equipment purchase. The software name becomes a proxy for familiarity, not a specification of what the machine must do.
A Clarification Table Prevents Teams from Talking Past Each Other
| If Someone Says “Fusion CNC” and Means… | The Real Decision Usually Is… | What Should Be Clarified Next |
|---|---|---|
| Integrated CAD/CAM workflow | Whether design-to-toolpath handoff is efficient enough | File flow, revision speed, and post reliability |
| Programming in a familiar software environment | Whether the team should standardize on that software | Training burden, machine mix, and job type |
| General machine or production research | Which process family and machine class actually fit the work | Material, geometry, volume, and workflow goal |
This table is a better starting point than forcing one universal definition onto the phrase. It forces the group to state which meaning applies before the conversation moves forward.
The Workflow Value Lives in Fewer Handoffs
When the term is used in the software sense, the value proposition usually centers on reducing friction between model changes and machine output. Teams may want fewer manual handoffs, easier revision handling, cleaner visibility between design and toolpath decisions, or a more consistent way to keep programming tied to the current geometry.
That value is most apparent in prototype work, mixed production, or environments where changes arrive frequently. It also matters in smaller operations where one environment is easier to teach and support than several disconnected tools. The fewer times a model must be exported, imported, and reinterpreted, the fewer opportunities exist for errors to creep in.
Software Familiarity Is Not the Same as Process Fit
One of the most common mistakes is assuming that because a team knows a software environment well, it is automatically the best answer for every CNC task the shop will face. Familiarity matters, but it is not the whole decision. The real questions remain about part mix, machine types, material behavior, setup complexity, and whether the workflow removes actual delay or only feels comfortable to current users.
Strong shops separate software comfort from manufacturing fit. They evaluate the workflow against representative jobs, not against the ease of the demo. A programmer who can move quickly in one environment may still be slower overall if the posted output requires constant manual correction at the machine.
The Phrase Does Not Describe a Machine Category
This point deserves to be stated plainly. “Fusion CNC” is not a machine class. It does not tell a buyer whether the work belongs on a router, a lathe, a vertical machining center, a nesting machine, or any other platform. It only suggests that the software environment may be part of the conversation.
Once buyers forget that distinction, they start treating workflow language as machine-selection language. That leads to vague equipment discussions and weak quoting comparisons. A machine is selected based on material, part geometry, production volume, and tolerance requirements. Software familiarity is a secondary consideration, not a primary driver.
Different Departments Mean Different Things
Inside one company, the same words can carry very different assumptions. Engineering may hear “Fusion CNC” and think about model-driven programming. Production may hear it and think about posted output and machine behavior. Purchasing may hear it and think about compatibility claims in a quotation. Management may hear it and assume a simpler training or standardization path.
None of those interpretations are irrational, but they are not identical. The phrase compresses several decisions into one label. Unless the label is unpacked, the meeting sounds more aligned than it really is. Experienced teams can still talk past each other for hours before realizing they were discussing different problems.
When the Phrase Is Actually Useful
The phrase is useful when it helps teams talk about integrated CAD/CAM workflow, post compatibility, revision handling, or the general benefits and tradeoffs of programming in a single design-to-manufacturing environment. In those cases, it functions as efficient shorthand, provided everyone agrees on the meaning.
It becomes unhelpful when it stands in for unanswered questions about the actual manufacturing route. If the team has not yet decided whether the part belongs on a nesting machine or a sliding table saw, software vocabulary will not resolve that question.
Sometimes the Real Question Is Standardization
In some shops, interest in “Fusion CNC” is really interest in standardizing around one environment so models, edits, toolpaths, and training expectations stay closer together. That is a very different conversation from simply asking whether the software can create toolpaths. It is an organizational decision about how engineering and programming should interact day after day.
Standardization can create real benefits, especially when teams are small or revisions are frequent. But it should still be judged against workload, machine mix, and the cost of forcing every job into one preferred environment. A shop running highly specialized nesting work may find that a dedicated solution outperforms a general-purpose integrated environment, even if the general-purpose option is more elegant on paper.
Evaluate with Real Jobs, Not Software Prestige
If a shop is genuinely considering whether this style of workflow fits, the strongest test is a representative job. Follow the part from geometry change to toolpath update to posted output. Measure where time is saved, where confusion disappears, and where the shop still relies on manual interpretation or workaround behavior.
A glossy demo proves much less than a routine revision on a real part family. The demo shows what the software can do under ideal conditions. The real job shows what the workflow does under the conditions the shop actually faces, including tight deadlines, incomplete model data, and operators who may not have written the original program.
Postprocessor Reliability Matters More Than Advertised
Another trap is assuming that integrated software value ends at the toolpath screen. It does not. The posted output still has to behave properly on the control environment actually installed on the shop floor. If postprocessor behavior is weak or inconsistent, the promise of a smooth CAD/CAM workflow is only half delivered.
Shops sometimes discover this too late because they evaluated software elegance more carefully than machine-output reliability. The fix is straightforward: test the workflow all the way to the machine before committing. Run a representative part, inspect the posted code, and verify that the machine behaves as expected. That test takes hours, not weeks, and it prevents costly surprises after purchase.
Quotation Language Should Never Stop at “Compatible”
Suppliers and integrators sometimes use compatibility language too casually. “Fusion CNC compatible” can sound reassuring while revealing almost nothing. Compatible in what sense? Model import? CAM workflow? Post support? Proven output on a specific machine-control combination? Ease of revision?
Buyers should press harder here. The goal is not to trap the supplier. The goal is to make sure the phrase points to something testable instead of something comforting. Ask for a specific postprocessor file, a reference installation, or a test cut. If the supplier cannot provide any of those, the compatibility claim is not yet an operational fact.
The Best Choice Depends on the Dominant Workload
Some shops gain real value from keeping design and CAM closer together in one environment. Others benefit more from specialized software built around the way they process routing, nesting, turning, or more complex machining work. The answer depends on what dominates the schedule.
Prototype-heavy work, frequent revisions, and mixed job flow may point one way. Stable high-volume routines or specialty programming needs may point another way. The phrase should always be translated back into the workload before a decision is made. A software environment that excels at one job type may be a poor fit for another, regardless of how well the team knows it.
Integration Is Not Automatically Lower Friction
A more integrated stack can reduce handoffs, but only if the work actually benefits from staying there. In some shops, the integrated path is genuinely cleaner. In others, a more specialized package handles the dominant manufacturing task more directly, even if the overall software landscape becomes less elegant on paper.
Decision-makers should resist the temptation to treat integration itself as the goal. The goal is lower operational friction. Sometimes integration provides it. Sometimes specialization does. The only way to know is to measure the workflow on real jobs and compare the results.
Clarification Helps Procurement as Much as Programming
This is not only a technical desk issue. Procurement teams, integrators, and machine buyers also benefit when the phrase is clarified early. If a supplier says a workflow is “Fusion CNC compatible,” buyers should ask whether that means post support, model import convenience, programmer familiarity, or something broader.
Without that step, commercial conversations can sound precise while remaining operationally vague. Clear language prevents expensive misunderstanding later in the machine or software selection process. A quotation that says “compatible” without specifying the postprocessor, the control version, and the tested machine model is not yet a usable document.
Training and Hiring Effects Are Part of the Decision
Software choices do not only shape programming flow. They also shape training speed, cross-coverage, hiring assumptions, and how fast another person can take over a job when the main programmer is unavailable. If a team is using “Fusion CNC” as shorthand for a more unified workflow, those labor questions deserve explicit attention.
This does not mean the answer must always favor one environment. It means that software meaning, staffing meaning, and process meaning are often intertwined. The term becomes much more useful once that is acknowledged directly. A shop that cannot hire programmers familiar with the chosen environment may face a longer ramp-up than the software demo suggested.
CAD/CAM Questions Still Need to Be Tied Back to CAM Reality
If the conversation is fundamentally about how geometry becomes machine motion, it helps to step back and review where CAM software actually fits in the CNC workflow. That anchor is usually more useful than debating a shorthand phrase in isolation, because it returns the discussion to programming responsibility, post behavior, and manufacturing handoff.
The CAM stage is where design intent becomes machine instructions. It is also where most workflow friction accumulates. Understanding that stage clearly makes the “Fusion CNC” discussion more productive, because it focuses attention on the actual points of failure rather than on software branding.
Sometimes the Real Question Is Simply the Machine
In other situations, the phrase is only a search habit that delays the real buying decision. If the team is no longer debating software workflow but actual equipment families, the clearer next step is to compare the relevant machine types directly through the Pandaxis machinery lineup. Software vocabulary can help frame the discussion, but it should not keep the team from specifying the production route the factory actually needs.
For woodworking and panel processing, that might mean comparing nesting machines against panel saws, or evaluating edgebanders and boring machines as part of a complete production line. The software question is secondary to the material handling, throughput, and part quality requirements that define the machine selection.
A Short Clarification Script Saves Hours
Before a meeting moves too far, one person can usually reset the discussion with a few direct questions. Do we mean the Fusion software environment itself? Do we mean a broader integrated CAD/CAM workflow? Do we mean post support for a specific machine? Or are we still trying to decide what machine category or manufacturing route fits the work?
That short reset is usually enough to turn a vague conversation into a solvable one. It takes less than a minute to ask, and it prevents the team from spending an hour comparing software features when the real decision is about machine class.
Use the Phrase Only After You Know What It Stands For
“Fusion CNC” is best understood as shorthand around integrated CAD/CAM workflow or search behavior, not as a standalone machine category. That is the practical conclusion. The safest rule is simple: before using the phrase in a decision, force it to mean one exact thing. Once the meaning is clear, the real software or machine question becomes much easier to solve.