Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
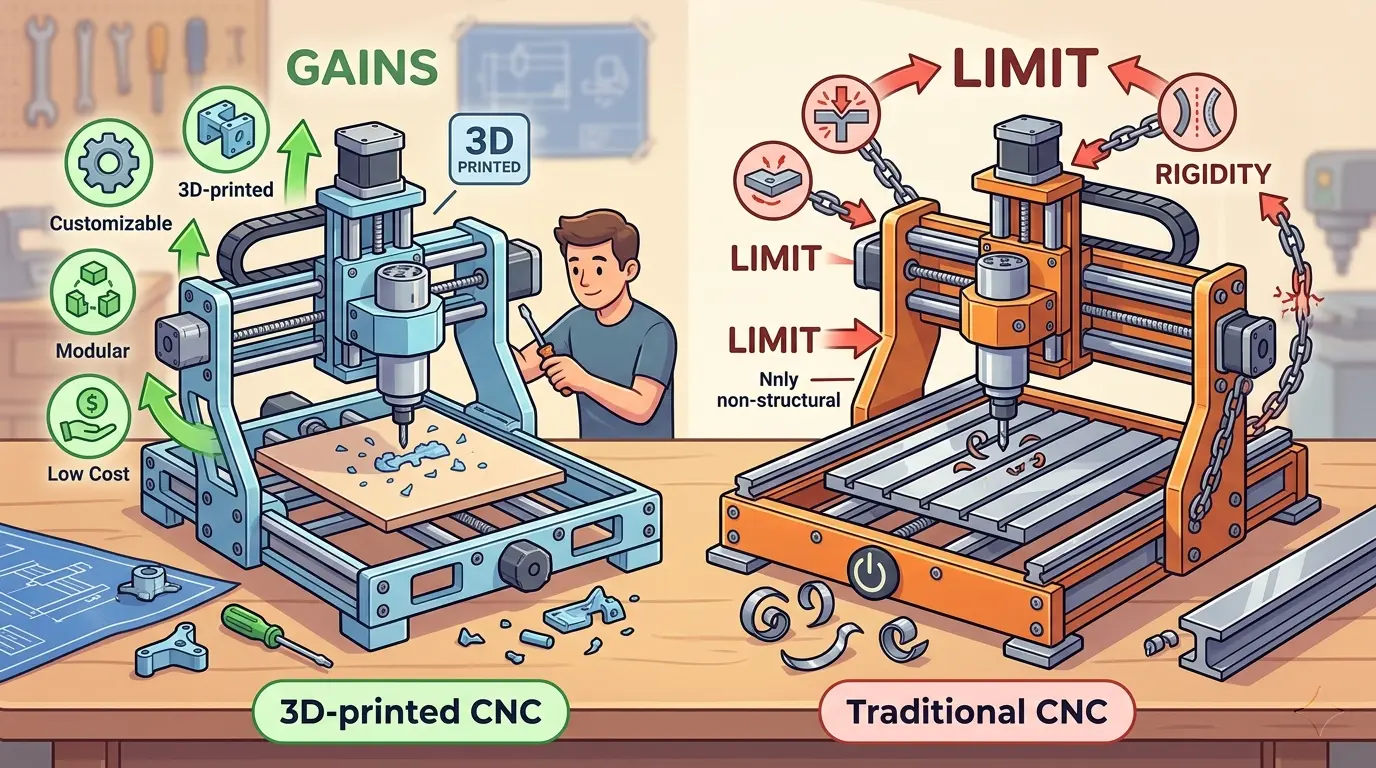
Before you commit a 3D printed CNC to any recurring shop task, the real question is not whether it can move accurately in air, but how calmly it holds position once the cutter meets resistance. This article walks through the structural ceiling that printed frames hit under load—visible flex, vibration, and drift that narrow the process window and quietly consume operator attention. For production engineers and shop managers weighing a low-cost build against a rigid router or nesting machine, the decision hinges on matching the platform to the workload: foam and light engraving tolerate the limits, while harder materials and customer-facing repeat parts expose them fast.
Why a Printed CNC Looks So Appealing
A 3D printed CNC machine can be assembled for the cost of a few spools of filament, a handful of hardware, and a weekend of focused work. That low entry price is genuinely attractive to classrooms, makerspaces, and R&D labs where capital budgets are tight and curiosity is abundant. The machine is also fully transparent. Every bracket, joint, belt path, and bearing block is visible, which makes it an unusually effective teaching tool for understanding how motion systems behave under load.
The appeal is real, but so is the structural ceiling. A printed frame behaves fundamentally differently from a welded steel or cast-iron structure. It flexes more, absorbs vibration differently, and drifts with temperature and humidity. That does not make it useless. It makes it a tool with a specific role, and that role is not high-throughput manufacturing. The mistake is not in building one. The mistake is in expecting it to behave like a production machine once the novelty wears off.
What a Printed Frame Actually Teaches You
The most valuable output of a 3D printed CNC is not the parts it cuts. It is the understanding the builder gains. Because the structure is modular and reprintable, you can test how gantry placement affects deflection, how belt tension changes motion feel, and how spindle mounting influences cut quality. These are lessons that are difficult to learn on a rigid industrial machine because the structure hides the cause-and-effect relationships. On a printed frame, those relationships are visible and adjustable.
In a training environment, that visibility is worth more than the machine’s cutting capacity. Students and engineers can:
- Observe how cutting force translates into visible flex in the frame
- Test how different bearing and rail configurations change repeatability
- Understand why spindle rigidity matters more than spindle power
- Learn proper cable management and assembly discipline that carries over to industrial equipment
- Develop a feel for feed rates and depth of cut by watching the machine react in real time
The machine becomes a physical textbook. It is not producing saleable parts at volume, but it is producing skilled operators and better-informed buyers. That is a legitimate return on investment, provided the expectations stay aligned with the platform.
Where a Printed CNC Performs Well
The operating envelope for a printed CNC is narrow but legitimate. It is strongest when the work tolerates iteration, low cutting force, and close supervision. Typical good-fit roles include:
- Foam cutting and light engraving on soft materials
- Plotting and marking tasks that require accuracy in air rather than under load
- Prototype parts where proof of concept matters more than throughput
- Classroom demonstrations and student projects
- Internal jigs, templates, and low-risk bench experiments
- CAM and post-processor validation before committing to more expensive tooling
These applications work because the machine is being valued for insight and flexibility, not for production calm. The cutting forces are low enough that the structure’s limitations rarely become the limiting factor. When you are cutting foam or engraving a soft plastic, the tool is not asking much of the frame. The machine can deliver acceptable results because the workload is within its design envelope.
Matching the Machine to the Workload
A simple fit assessment helps clarify where printed CNC makes sense and where it becomes a liability. The dividing line is not whether the machine can move accurately in air. It is how calmly it behaves once the tool meets resistance. A machine that positions beautifully with no load can become a different machine entirely when the cutter engages the material.
| Use Case | Fit On Printed CNC | Why It Can Work | What Usually Breaks First |
|---|---|---|---|
| Learning and CNC skill building | Good | Low-risk experimentation is the point | None, if the goal is education |
| Foam, light engraving, and very light routing | Fair to good | Low cutting load gives the structure more margin | Finish sensitivity rises as load rises |
| Internal fixtures and simple prototypes | Fair | Value comes from convenience and iteration | Repeatability can drift if setup discipline slips |
| Customer-facing repeat parts | Weak | A few parts may still look acceptable | Supervision, finish, and repeatability become too narrow |
| Harder materials or higher load work | Poor | Possible only in narrow cases | Rigidity limit shows up quickly as vibration and caution |
The pattern is consistent. The more the machine is asked to behave like a production tool, the more its structural limitations dominate the conversation. A printed CNC can produce a beautiful part. It can even produce several beautiful parts in a row. But the process window narrows quickly as the workload grows, and the operator has to compensate for what the structure cannot provide.
How Rigidity Limits Show Up on the Shop Floor
Weak rigidity rarely announces itself through one dramatic crash. It usually appears as a narrower process window. The machine will cut a part acceptably one day, then produce a slightly rougher edge the next, and the operator cannot easily explain why. That unpredictability is the real cost of a flexible structure.
In practical terms, the rigidity limit shows up in several ways:
- Finish quality changes more easily with tool wear or material variation
- Edge quality depends too much on conservative feed rates and shallow passes
- Repeatability drops after small setup disturbances, like a bumped limit switch or a loosened bolt
- Tool behavior degrades earlier because vibration appears sooner at lower cutting forces
- Operator attention goes up because margin goes down
- Chatter marks appear on the workpiece at cutting depths that would be routine on a rigid machine
- Tool life shortens because the cutter is absorbing vibration that the frame should be damping
The part may still get made. It just gets made with less calm and more babysitting. In a learning environment, that is acceptable, even instructive. In a production environment, it competes directly with paid work. Every minute spent watching a printed machine struggle through a cut is a minute not spent on work that actually generates revenue.
Repeatability Is the Real Threshold
One strong sample is weak evidence. The real test is whether the machine can return to the same result tomorrow under normal behavior, after normal handling, without turning the process into a supervision project. A machine that produces one beautiful part is not the same as a machine that produces a hundred consistent parts.
Useful questions to ask before committing a printed CNC to any recurring task:
- How much does the result change after a minor setup disturbance?
- How often does the machine need rechecking or retensioning?
- Does finish stay acceptable across repeated runs, or does it drift with ambient temperature?
- Is the machine still serving its intended role, or has it become a tuning hobby?
- Can a different operator achieve the same results, or does the machine depend on one person’s accumulated feel for its quirks?
- How much time is spent on verification versus actual cutting?
Those answers tell a more honest story than a highlight reel ever will. The gap between a prototype machine and a production machine is not measured in spindle speed or travel distance. It is measured in how consistently the machine delivers the same result under normal working conditions.
The Hidden Cost of DIY Is Attention
A printed build can be affordable in hardware terms and still expensive in operator attention. Every extra alignment check, cautious toolpath revision, interrupted cut, or finish correction consumes time. That time has a cost, whether it is billed to a project or simply subtracted from other work.
Consider a typical scenario. A shop prints a CNC frame, assembles it, and gets it cutting. The first few parts look good. Then a tool wears slightly, and the finish degrades. The operator slows the feed rate to compensate. Then the ambient temperature changes, and the frame drifts. The operator re-levels the machine. Then a limit switch gets bumped during a tool change, and the next part is slightly off. The operator re-homes the machine and runs a test cut.
None of these steps is dramatic. Each one takes only a few minutes. But they add up across a day, a week, and a month. The machine is not failing. It is just demanding more attention than a production machine would. In a learning environment, that may be completely acceptable. The attention is the point. In a commercial environment, it competes with quoting, production, shipping, and other work that needs the same skilled attention.
So the same machine can feel brilliant to one owner and limiting to another. One values experimentation. The other values dependable output. Neither is wrong. They are just measuring different things.
Modifiability Is a Strength, Not a Substitute for Stability
One major advantage of printed CNC is how easily it can be revised. Parts can be reprinted, mounts can be changed, and design ideas can be tested without heavy fabrication expense. That makes it an ideal platform for iterative development. If a gantry design flexes too much, you can print a revised version overnight and test it the next day. That kind of rapid iteration is simply not possible with welded steel or cast iron.
But modifiability and trust are not the same thing. A platform that is easy to change is not automatically easy to believe. If the machine remains under constant revision, it may stay educational while never becoming operationally calm. There is a real risk that the machine becomes a permanent project rather than a working tool.
This becomes important when a shop starts depending on it. There is a difference between a machine that is being improved and a machine that is never finished. The latter consumes attention indefinitely. Every improvement cycle introduces new variables, and every new variable requires verification before the machine can be trusted again. That is fine for a hobby or a classroom. It is a liability in a production environment.
Material Choice Exposes the Limit Unevenly
Soft materials, shallow passes, and non-critical finish expectations let printed CNC stay useful much longer. Harder substrates, longer tools, and heavier cutting loads expose the structure much faster. The machine does not fail dramatically. It just becomes harder to get a good result, and the operator cannot easily pinpoint why.
That unevenness can create false confidence. A machine that performs well on foam or light engraving can look ready for more demanding work until one material or geometry suddenly narrows the process window sharply. Consider what happens when you move from foam to plywood. The cutting forces increase significantly. The printed frame flexes more under load. The tool deflects. The finish degrades. The operator slows down the feed rate to compensate, which increases cutting time, which increases heat, which affects the printed structure’s dimensional stability. The process spirals.
Buyers should screen by recurring material family, not by the single best successful test. If the work is always foam and engraving, a printed CNC may be a reasonable fit. If the work includes plywood, hardwood, or acrylic at any depth, the structural limit will appear quickly. The question is not whether the machine can cut the material at all. It is whether the machine can cut the material repeatedly, with acceptable finish, without demanding constant supervision.
Use It as a Stage, Not as a Hidden Factory Plan
Printed CNC is often most valuable when it sits inside a staged capability path. It helps a team:
- Learn why rigidity matters before spending capital on a rigid machine
- Build better fixturing habits that transfer to industrial equipment
- Improve CAM and post-processor discipline without risking expensive tooling
- Validate low-risk product or tooling ideas before committing to production
- Clarify what the next machine purchase really needs to solve
- Develop a maintenance mindset that treats the machine as a system, not a black box
That learning can make the next equipment purchase much better. In that sense, a printed CNC can pay back by improving the quality of the machine decision that follows it. A team that has struggled with a flexible frame understands why a rigid gantry matters. A team that has fought with belt tension understands why ball screws are worth the cost. A team that has watched finish quality drift with temperature understands why thermal stability is a specification worth paying for.
When It Is Time to Graduate
The right time to move on usually arrives when the workflow stops rewarding experimentation and starts rewarding stability. That shift is not always obvious, but the warning signs are consistent:
- Customer deadlines matter more than learning value
- Part quality must repeat across runs or across operators
- Supervision burden starts crowding out paid work
- Scrap or rework costs matter more than capital savings
- Structural calm matters more than ease of modification
- The machine is being asked to cut harder materials or deeper passes than it was designed for
At that stage, the buyer is usually better served by a more rigid router platform, a broader machinery option from a supplier like Pandaxis, or, in sheet-based woodworking contexts, a move toward CNC nesting machines. The decision should be driven by the process window the work actually requires, not by the appeal of a low-cost build.
When you make that transition, the printed machine does not need to be discarded. It can be reassigned to the educational role it was always best suited for. It can train new operators. It can validate toolpaths. It can test fixturing ideas. It can continue to serve as a low-risk platform for experimentation while the rigid machine handles the work that pays the bills.
The Honest Bottom Line
The strongest reason to use a 3D printed CNC is not to imitate industrial hardware cheaply. It is to learn, test, and build process understanding with lower capital exposure. The machine is a legitimate educational tool and a reasonable platform for low-force prototyping. It teaches real lessons about rigidity, vibration, repeatability, and process discipline that transfer directly to industrial equipment.
It becomes disappointing only when a learning platform is quietly promoted into a production role it was never designed to carry. The machine does not change. The expectations do. Keep the expectations aligned with the structure, and a printed CNC can be a genuinely useful addition to a shop’s capability path. Push it beyond that, and the rigidity limit will make itself known in finish quality, repeatability, and operator attention.
Before you build or buy, be honest about the role the machine will play. If it is a teaching tool, a prototyping platform, or a low-force experiment station, a printed CNC is a defensible choice. If it is expected to produce customer-facing parts on a schedule, the structural ceiling will eventually cost more in supervision and rework than the initial build saved in capital. Match the machine to the workload, and you will get value from it. Mismatch them, and you will spend your time fighting the frame instead of making parts.