Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
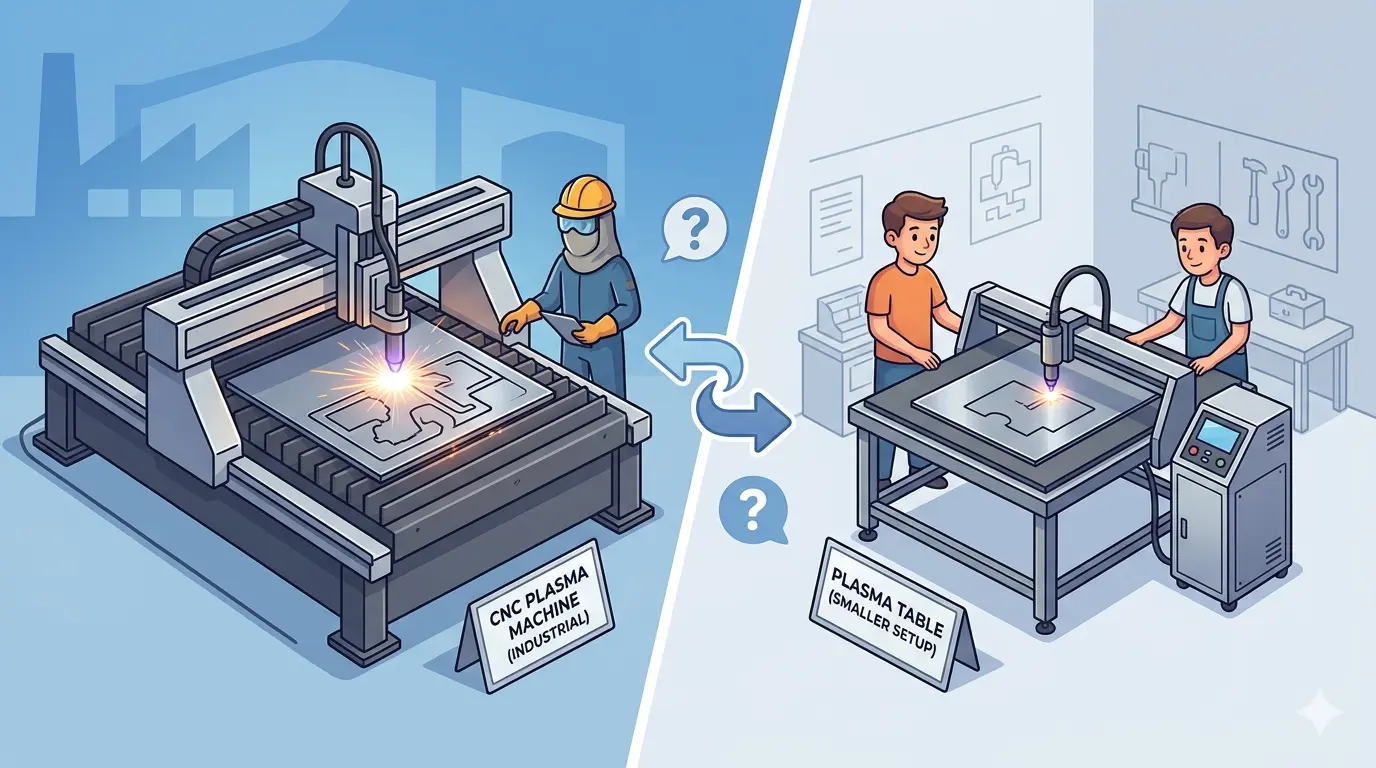
Fabrication buyers often stall at the quote stage because “plasma table” and “CNC plasma cutting machine” sound like different equipment classes when the torch physics are identical. The real distinction is scope: one label covers the flatbed platform, while the other implies the integrated production cell around it—motion, height control, software, extraction, and startup support. Before you compare prices, you must normalize each quote against five concrete items: usable cut area, THC inclusion, control workflow, fume extraction assumptions, and commissioning scope. Otherwise, you risk paying for packaging that does not solve your actual bottleneck or buying a bare bed that fights you daily.
Start With The Work, Not The Wording
When a fabrication shop starts comparing quotes, the terminology can create confusion before the first specification is even reviewed. A supplier offers a “plasma table.” Another quotes a “CNC plasma cutting machine.” The buyer assumes these are two different pieces of equipment with different capabilities, so the comparison begins on the wrong footing.
In most cases, the cutting physics are identical. The torch, the power source, and the basic thermal cutting process are the same. The real difference is scope. One label points to the flatbed cutting platform. The other points to the broader production station built around it: motion system, height control, controller, software flow, extraction assumptions, and startup support.
Read the labels as clues about what the supplier is including in the package, not as proof of fundamentally different process behavior. The question is not which phrase sounds more capable. The question is which scope actually solves the bottleneck in your shop.
What A Plasma Table Usually Includes
In most quotations, “plasma table” refers to the physical work platform: the flatbed support area where sheet or plate sits while the CNC-guided torch follows the programmed path. That sounds straightforward, but the table is far more than a flat surface. It is where material support, slat wear, loading access, scrap clearing, remnant handling, and day-to-day housekeeping all converge.
When a supplier emphasizes the table, they are usually emphasizing the production base: the bed, the slats, the cutting zone, and the immediate area where the operator loads material and retrieves parts. The table is the physical anchor of the cutting operation.
This matters because the table determines how well the shop handles the routine realities of thermal cutting. Slats wear and need replacement. Scrap and skeletons accumulate and must be cleared. Fumes affect visibility and operator comfort. Loading large sheets requires clearance and access. If the table design does not support these daily tasks, the cutting process will feel clumsy regardless of how capable the torch is.
Consider a shop that cuts 4×8-foot sheets of mild steel plate in the 10–20 mm range. The operator loads a sheet, runs a nest of parts, and then spends twenty minutes clearing the skeleton and sorting remnants. If the table has a water table with a removable slag tray, that clearing job is straightforward. If the table is a dry table with fixed slats and no easy access underneath, the operator is fighting heavy scrap every single run. The torch never changes. The ownership experience changes completely.
What A CNC Plasma Cutting Machine Usually Implies
When a supplier says “CNC plasma cutting machine,” the phrase typically stretches beyond the bed. It suggests the cutting system as a whole: the motion package, the height control, the controller, the software assumptions, the power-source integration, and the wider logic around operating the cell consistently.
This broader framing matters when the cutting station is expected to behave as a managed production step rather than just a torch above a bed. The machine label implies that the supplier has considered how the components work together: how the controller interprets the part program, how the height control responds to plate variation, how the motion system maintains cut quality across the full bed, and how the operator interacts with the system from setup to part removal.
Sometimes this difference is meaningful. The supplier may have integrated the components into a more coherent package with better documentation, more thorough startup support, and a more mature software workflow. Other times, the broader language is mostly sales framing applied to nearly the same flatbed setup.
The label alone is weak evidence. The included system definition is what matters.
Verify These Five Items Before Comparing Prices
Instead of reacting to category language, normalize the quote. Ask each supplier to confirm the same set of specifications so the comparison is apples to apples. These five items account for most of the practical difference between a basic table and a managed cutting cell:
- Usable cut area: Confirm the actual cutting envelope, not the overall machine footprint. Rail travel, torch clearance, and material support all affect what you can actually process. A machine that claims to handle 4×8 sheets may have a torch that cannot reach the full width when the height control is at its highest setting.
- Height control inclusion: Is the torch height control (THC) included in the base price, or is it an option that gets added later? This is one of the most common sources of quote creep in plasma purchases. A basic THC that maintains a fixed standoff distance is very different from an advanced THC that senses arc voltage and adjusts in real time across warped plate.
- Control workflow: What software does the operator use to create, import, and run part programs? Is nesting included? How long does it take to go from drawing to first cut? Some controllers accept DXF files directly and generate toolpaths automatically. Others require a separate CAM package and a post-processor that the operator must learn. The difference in setup time is measured in hours per week, not minutes.
- Extraction assumptions: Does the quote include fume extraction, or is that assumed to be a shop responsibility? Undersized extraction degrades visibility, operator comfort, and cut quality. A downdraft table with integrated extraction is a different machine than a dry table that relies on ambient shop ventilation.
- Startup scope: What happens after delivery? Is installation, commissioning, and operator training included, or is the machine delivered as a kit that the shop must bring online? A machine that arrives with a technician who spends two days on-site is worth more than a machine that arrives on a pallet with a manual and a phone number.
If these answers are fuzzy, the difference between “machine” and “table” language may only be the difference between precise scope and imprecise scope.
When A Table-Centered Purchase Is The Right Call
Many fabrication shops do not need an oversized, highly integrated plasma solution. They need dependable flat-sheet cutting that matches the material formats, staffing level, part mix, and downstream rhythm already in the building.
A table-centered purchase can be the right commercial answer when the real need is straightforward:
- Put stock on the bed reliably.
- Cut common parts predictably.
- Recover remnants and scrap without chaos.
- Maintain acceptable height behavior and consumable discipline.
- Keep cleaning and maintenance manageable.
If the real bottleneck is simply lacking in-house thermal cut capacity, buying a more complex system may add cost without removing the actual constraint. A shop that cuts a few sheets per day, has one experienced operator, and does not feed a tightly scheduled downstream department may find that a well-built table with reliable height control is sufficient. The extra integration and software sophistication of a broader machine package would not change the daily output.
Think about a small job shop that fabricates brackets, base plates, and simple structural components. The owner operates the plasma table personally. The part mix is stable. The tolerances are generous. The shop does not run second shifts. In this scenario, a table with a solid THC, a straightforward controller, and a proven extraction setup will deliver exactly what the business needs. Adding a fully integrated machine package with advanced nesting software and remote diagnostics would add cost without adding throughput.
When Broader Machine Scope Pays Back
The broader machine-package framing becomes more valuable when the plant expects the cutting station to behave as a managed production step. That usually happens when duty cycle is higher, multiple operators share the cell, output feeds other departments tightly, or management wants steadier daily behavior.
At that point, buyers need to care more about:
- Height-control stability across normal plate variation. Warped or slightly bowed plate is common, and the THC must respond without crashing the torch or producing inconsistent edge quality. A basic THC that only maintains a fixed standoff distance will struggle with plate that varies by more than a few millimeters across the bed.
- Program repeatability from shift to shift. If two operators run the same program and get different results, the station is not behaving like a managed production step. The controller should store parameters, consumable settings, and cut recipes so that any trained operator can reproduce the same cut quality.
- Operator handoff burden. How much setup, adjustment, and troubleshooting does each part run require? A more integrated system reduces the tribal knowledge needed to get good cuts. When the experienced operator is on vacation, the second-shift operator should still be able to produce acceptable parts.
- Extraction, material movement, and routine cleaning support uptime. A station that takes 30 minutes to clean between runs is a station that loses production capacity every single day. A machine with a removable slag tray, a water table with easy drain access, or a downdraft extraction system will keep the operator cutting instead of cleaning.
- Manageability during longer or busier operating periods. When the shop is running at capacity, the cutting station must hold up without constant babysitting. Consumable life, torch cooling, and motion-system reliability all become more important when the machine runs eight or more hours per day.
If the cutting station feeds a bending department, a welding line, or a finishing operation, the cost of inconsistent output multiplies downstream. A part that arrives at the press brake with a slightly rough edge may require extra deburring. A part that arrives at the welding station with inconsistent bevel quality may require rework. In that context, the broader machine package is not overhead. It is insurance against production variability.
Extraction, Scrap Clearing, And Height Control Decide The Ownership Experience
Buyers often over-focus on the torch and under-focus on the annoyances that define ownership. Slats wear. Scrap builds up. Skeletons must be cleared. Fumes affect visibility and operator comfort. Maintenance access matters more after installation than it ever does in the demo.
Ask directly:
- How are slats serviced and replaced? Are they standard sizes that are easy to source, or proprietary parts with long lead times? A shop that cuts heavy plate will replace slats regularly. If the slats are a standard profile that any local steel supplier can cut, the replacement cost is low. If they are proprietary, the shop is locked into the supplier’s pricing and lead times.
- How is scrap removed in normal operation? Does the table design allow for efficient clearing, or does the operator have to climb over the bed and fight with heavy skeletons? A table with a tilting bed, a removable slag tray, or a water table with a mechanical lift will make scrap removal a routine task rather than a physical struggle.
- What fume-management logic is actually assumed? Is extraction sized for the cut area and material thickness you plan to run? A downdraft table that pulls fumes through the bed is very different from a side-draft hood that only captures a portion of the plume. Undersized extraction will leave the operator working in a haze and will allow particulate to settle on machine ways and electronics.
- Is height control included clearly, or buried in vague language that gets clarified only after the purchase order is signed? The THC is the single most important component for cut quality consistency. If the quote does not specify the THC model and its capabilities, ask for the details in writing before committing.
- Can the operator clean and access the table without a fight? Downtime for cleaning is real production time lost. A table with easy access to the cutting zone, removable slats, and a clear path for scrap removal will keep the operator productive.
These questions separate a quote that will feel professional in daily operation from one that will generate frustration within the first month.
Normalize The Quote Before You Compare The Promise
One of the most common procurement traps is assuming that “CNC plasma cutting machine” automatically means a more mature solution and “plasma table” automatically means something more basic. Sometimes the offers are close. Sometimes they are not.
It helps to compare machinery quotes line by line instead of reacting to category language. Build a comparison spreadsheet with the five items listed above as columns. Fill in each supplier’s answer. Where the answers are vague, ask for clarification in writing. Where the answers differ, evaluate whether the difference matters for your specific production situation.
If the buying path is factory-direct or otherwise lighter on local service, buyers should also review what needs to be verified before low-support machinery becomes a recovery problem after delivery. A machine that arrives with minimal documentation and no local support may be cheaper upfront, but the cost of troubleshooting a controller issue without a phone number to call can quickly exceed the savings.
Sometimes The Real Decision Is Plasma Versus Another Process
Some shops ask this question too narrowly. If the real pain is edge condition, smaller-feature quality, thermal effect, or downstream cleanup burden, then debating “table” versus “machine” may not solve the real process problem. The better comparison may be whether plasma itself is the right route.
Plasma is a thermal cutting process. It produces a heat-affected zone, and it leaves dross on the bottom edge of thicker material. If the shop’s real requirement is clean edges with minimal secondary processing, a different process may be more appropriate.
Consider a shop that cuts thin stainless steel sheet for architectural panels. The parts require clean edges, minimal distortion, and no secondary deburring. Plasma will struggle to meet those requirements consistently. A fiber laser or a waterjet would be a better fit, even though the capital cost is higher. The plasma table versus machine debate is irrelevant if the process itself is wrong for the application.
Similarly, a shop that cuts thick structural steel plate for heavy fabrication may find that plasma is the only practical thermal process. In that case, the table versus machine question matters, but the process choice is already settled.
When that broader process choice is still unsettled, it helps to step back and consider which larger production workflow a machine choice is really meant to support. Map the full material flow: incoming stock, cutting, edge preparation, forming, welding, finishing, and assembly. Identify where the quality bottleneck actually sits. If the bottleneck is downstream of cutting, a better cutting process may not solve it. If the bottleneck is the cutting station itself, then the plasma table versus machine decision is the right focus.
Choose The Scope That Solves The Bottleneck
For most shops, a plasma table refers mainly to the flatbed cutting base and the operating zone around it, while a CNC plasma cutting machine usually points to the broader system built around that base. Sometimes the difference is substantial. Sometimes it is mostly wording.
The stronger buying move is not to decide which phrase sounds more correct. It is to identify what production problem needs solving and then buy the exact scope that solves it. Map the daily work: material formats, part mix, operator skill level, downstream demand, and maintenance capacity. Then compare quotes on the five items that matter: usable cut area, height control, control workflow, extraction, and startup scope.
A shop that cuts a few sheets per day with one experienced operator may find that a well-built table with reliable height control is the right purchase. A shop that runs the cutting station across two shifts, feeds multiple downstream departments, and needs consistent output from any trained operator will benefit from the broader machine package.
The label on the quote is a starting point, not a conclusion. The production bottleneck is the real decision driver.