Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
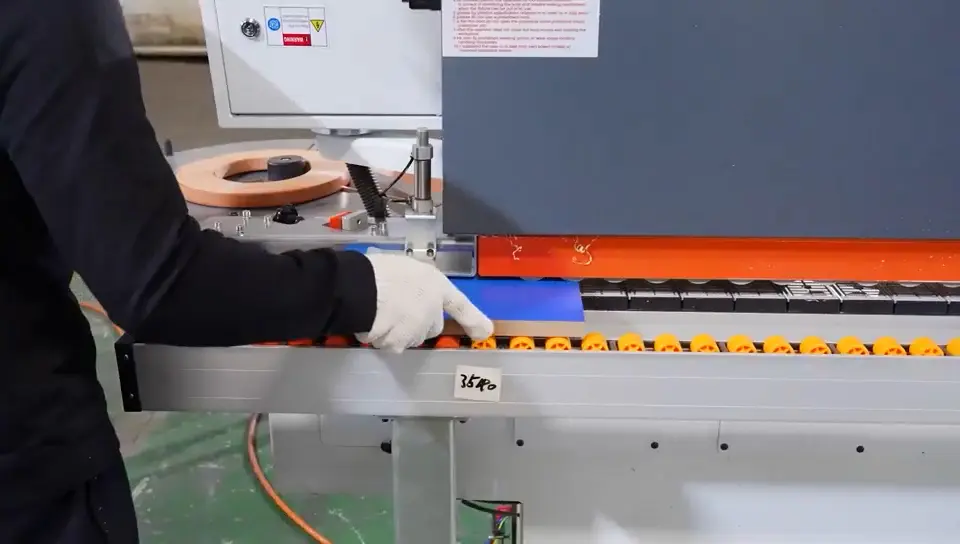
Start with the job, then compare automation labels, the real question is where your edgebanding line loses time: operator repositioning, manual trimming, or changeover between short runs. This article forces you to map batch sizes, measure the pause between panels, and count rework events before committing capital. An automatic machine stabilizes output and reduces labor dependence, but it amplifies upstream panel defects and punishes frequent job changes. A semi-automatic unit preserves flexibility for mixed production, yet its output scales only with operator discipline. The decision matters because the wrong configuration becomes a permanent bottleneck, costing you in labor, rework, and missed delivery dates long after the purchase order is signed.
Start With the Bottleneck, Not the Machine Label
In most panel-processing shops, the sequence is predictable. The CNC router or panel saw sets the pace, the edgebander is expected to keep up, and the bottleneck quietly moves to wherever the operator has to slow down. If you have ever watched a semi-automatic line where the operator is constantly repositioning panels, checking glue application, or hand-trimming the ends of a batch, you already know where the time goes. The question is whether that time is a tolerable cost of flexibility or a structural limit on what the shop can ship each week.
The decision between an automatic and a semi-automatic edgebander is not about which machine is “better” in the abstract. It is about which one removes the dominant source of delay from your specific workflow. Shops that compare automation levels before they map out their actual material flow often end up with a machine that is either overbuilt for the workload or underpowered for the growth they have planned. The purchase price is only the first number. The real cost shows up in how many panels move through the machine per shift, how much rework the finishing department absorbs, and how many operators you need to keep the line running.
Edge-banding productivity is shaped by several factors that have nothing to do with the automation label on the brochure:
- Panel feeding and positioning time
- Consistency of edge preparation before banding
- Stability of glue application across a shift
- How many trimming, scraping, and finishing steps remain manual
- How much output depends on individual operator technique
- How smoothly finished panels move into drilling, assembly, or packing
A more automated machine is not automatically the better investment if your real problem is irregular batch sizes or constant product changeovers. Conversely, a semi-automatic machine is not automatically the lower-value option if you do not yet have the volume to justify continuous processing. The right choice removes the most expensive source of friction from your line, and that requires knowing where the friction actually is before you sign the purchase order.
What an Automatic Edgebander Actually Changes on the Floor
For factories running repeated cabinet parts, wardrobes, office furniture, and other panel-based products, automatic edgebanders are the standard choice because they turn edge finishing into a controlled sequence rather than a series of manual interventions. The advantage is not just higher line speed. It is stable output across a full shift, which matters more for planning and labor allocation. When you know the machine can process a consistent number of panels per hour without quality drift, you can schedule downstream operations with more confidence and staff the line accordingly.
When feeding, banding, pressing, trimming, and finishing happen in a continuous sequence, the process becomes less dependent on constant operator correction. That shift produces several measurable outcomes at the same time: edge appearance becomes more consistent from panel to panel, manual rework drops, and downstream assembly sees fewer interruptions caused by uneven finishing or visible glue lines. The operator’s role changes from controlling the finish to managing the flow, which is a fundamentally different labor model. Instead of watching every panel for defects, the operator monitors the machine, loads material, and handles exceptions. That is a more sustainable job over a ten-hour shift, and it reduces the variance that comes from different operators applying different levels of care.
Automatic edgebanders are usually the strongest fit when a shop needs:
- Higher sustained daily output on repeated part families
- Consistent glue-line appearance across batches and shifts
- Lower dependence on individual operator skill
- Repeatable part quality for assembly or hardware installation
- Fewer manual touches between banding and finished panel output
In practical terms, an automatic machine makes edge banding behave like a production station. The operator’s role shifts from controlling the finish to managing the flow, which is a fundamentally different labor model. That shift has real consequences for hiring, training, and shift planning. A shop running automatic equipment can often cross-train operators more quickly because the machine handles the critical process steps. The operator needs to understand material flow, glue temperature, and basic troubleshooting, but does not need the same level of hand-finishing skill that a semi-automatic line demands.
Consider a typical cabinet shop producing kitchen cabinets in batches of fifty to two hundred identical door and carcass parts. With an automatic edgebander, the operator loads a stack of panels, sets the parameters for the current part family, and the machine processes each panel through the full sequence. The operator’s main tasks are keeping the infeed loaded, checking the first few panels after a changeover, and pulling finished panels off the outfeed. Over a shift, that shop can process several hundred panels with minimal variation in edge quality. The same shop on a semi-automatic machine would need the operator to handle each panel individually, position it against the fence, feed it through, and then manage the trimming and finishing steps. The output per operator drops, and the quality depends heavily on how consistently that operator performs the same motions all day.
Where Semi-Automatic Edgebanders Still Make Sense
The case for a semi-automatic edgebander is different, and it is not a weak case. It is usually stronger when flexibility and lower process complexity matter more than maximum continuous output. In a shop handling short runs, mixed part sizes, custom orders, or unpredictable scheduling, a semi-automatic setup can protect productivity because it lets the team adapt without forcing the entire workflow into a continuous production rhythm. If the daily workload changes constantly, the value of a simpler machine comes from easier operation, faster adjustment between jobs, and a lower penalty when the line is not being fed continuously.
Think about a custom millwork shop that produces one-off reception desks, retail fixtures, and architectural panels. The parts are rarely identical, the sizes vary widely, and the edgebanding requirements change from job to job. On an automatic machine, every changeover requires adjusting the machine parameters, testing a sample panel, and confirming the setup before running the batch. If the batch is only five panels, the setup time can exceed the processing time. A semi-automatic machine, by contrast, allows the operator to adjust the setup quickly and handle each panel individually, which is often faster for very small batches and highly varied work.
That configuration often makes sense when the workflow includes:
- Lower or irregular daily panel volume
- Frequent job changes and short production runs
- A wide mix of panel sizes or product types
- Skilled operators who can manage more of the finish process directly
- A need for a practical step between manual edge work and full production automation
The tradeoff is real. Output and finish consistency depend more on operator discipline. As volume rises, the same flexibility that helps a mixed-production shop becomes the factor that limits scaling. You can add labor, but you cannot easily add consistency. A semi-automatic line with two operators might produce the same daily output as an automatic line with one operator, but the quality will vary more, and the labor cost per panel will be higher. The decision comes down to whether you are paying for flexibility or paying for consistency, and which one drives more revenue in your market.
Another situation where semi-automatic equipment remains practical is the shop that is transitioning from manual edgebanding or hand-applied edging. The jump from a manual process to a fully automatic line is large in terms of investment, training, and workflow redesign. A semi-automatic machine offers a middle step that introduces mechanical glue application and trimming while keeping the operator in control of the process. That can be the right move for a shop that wants to improve quality and throughput without committing to the full automation model yet.
Side-by-Side Comparison
| Decision Factor | Automatic Edgebander | Semi-Automatic Edgebander | Stronger Fit |
|---|---|---|---|
| Sustained output on repeated parts | Usually stronger because the workflow is built for continuous processing | Usually lower because more handling or intervention remains manual | Automatic |
| Finish consistency across a shift | Commonly stronger because more steps stay under one controlled sequence | More dependent on operator rhythm and follow-up handling | Automatic |
| Adaptability for short runs | Can be less efficient if jobs change constantly and volume stays low | Often more practical when batches are fragmented or highly varied | Semi-Automatic |
| Labor dependence | Usually lower once the workflow is organized | Usually higher because the operator influences more of the cycle | Automatic |
| Ease of scaling output | Commonly stronger for growing panel-based production | Often requires more labor or more time as output targets rise | Automatic |
| Simplicity for smaller shops | Can add process complexity if the workload does not justify it | Often easier to match to lower-volume or transitional production | Semi-Automatic |
| Rework risk from process variation | Usually lower when the line is properly set up and fed consistently | Usually higher when part handling and finishing vary by operator | Automatic |
| Changeover time between jobs | Longer because multiple parameters must be adjusted and verified | Shorter because the operator adapts the setup more directly | Semi-Automatic |
| Best use case | Repeated cabinet and furniture production with stable demand | Flexible, lower-volume, or mixed-production environments | Depends on workflow |
The table makes the tradeoff explicit. Automatic edgebanders deliver better results when the factory is trying to standardize output. Semi-automatic edgebanders make more sense when the business is trying to stay adaptable without building the whole workflow around continuous production. Neither choice is wrong in isolation. The wrong choice is the one that does not match the actual production pattern of the shop.
The Hidden Costs Buyers Often Miss
The wrong machine is often chosen because buyers focus on the automation label and ignore where real cost shows up later. Both configurations have failure modes that are predictable if you know what to look for. The purchase price is the visible cost. The invisible costs are the ones that accumulate over months and years of operation, and they are the ones that determine whether the machine pays for itself or becomes a source of ongoing friction.
For automatic edgebander buyers, the most common mistake is assuming the machine alone will solve quality and throughput problems. It will not. If panels arrive out of square, edge preparation is inconsistent, tape selection changes without discipline, or batches are not organized well, the value of higher automation drops quickly. An automatic edgebander performs best when the upstream process is stable enough to keep the machine working in a controlled rhythm. If your saw or nesting output is erratic, the automatic machine will simply process that erratic flow faster. You will still get inconsistent panels, but you will get them faster and in larger quantities, which means more rework downstream.
Consider the panel preparation step. An automatic edgebander assumes the panel edges are clean, square, and free of loose fibers. If your panel saw produces tear-out on the bottom edge, or if the nesting machine leaves a rough surface, the edgebander will apply the tape over that defect. The result is a visible glue line or a tape that lifts after a few weeks in the field. The automatic machine does not fix upstream quality problems. It amplifies them by processing defective panels at higher speed. Shops that invest in automation without fixing their saw maintenance, blade sharpening schedules, or nesting parameters often find that the edgebander simply produces more defective parts per hour than the old manual process did.
For semi-automatic buyers, the most common mistake is underestimating how much labor variation affects output over time. A capable operator can keep a semi-automatic machine productive, but as volume grows, more time is lost to repositioning, visual checking, edge touch-up, and small corrections that do not look expensive one panel at a time but become significant over a full shift. That labor cost is real, and it scales with your output. A shop running one shift on a semi-automatic machine might not feel the pressure. The same shop running two shifts, or pushing for higher daily output, will quickly discover that the operator is the limiting factor. The machine can run faster, but the operator cannot feed it faster, check the output faster, and handle the finishing steps faster all at the same time.
The most common hidden losses are:
- Waiting time between panels instead of continuous flow
- Manual rework on glue lines or edge finish
- Inconsistent results across operators or shifts
- Slower handoffs into assembly because finished parts need extra attention
- Difficulty raising output without adding more labor pressure
- Setup and changeover time that eats into productive hours on short runs
- Training time for new operators who need to develop hand-finishing skill
The better investment is usually the machine that removes the dominant source of waste from the line, not simply the one that sounds more advanced or more affordable in isolation. That means calculating the real cost per panel, not just the machine price. Include labor, rework, scrap, changeover time, and the cost of quality issues that reach the customer. When you add those numbers, the decision often becomes clearer than the brochure comparison suggests.
How to Map Your Workflow Before You Decide
Before you compare machine specifications, take a week to document what actually happens on your edgebanding line. Track every panel that goes through the process and note where time is lost. You will likely find that the delays fall into a few predictable categories, and each category points toward a different machine configuration.
Start with batch size and frequency. Count how many jobs you run in a typical week and how many panels each job produces. If you run twenty jobs a week with an average batch size of fifteen panels, you are in a high-changeover environment. The setup time on an automatic machine will be a significant portion of your total production time, and a semi-automatic machine might serve you better. If you run five jobs a week with an average batch size of two hundred panels, the changeover cost is negligible compared to the processing time, and the automatic machine will deliver a clear advantage.
Next, measure the time between panels. On a semi-automatic machine, the operator has to position each panel, feed it, and then handle the trimming and finishing. That creates a natural pause between panels. Over a shift, those pauses add up to a significant portion of the available production time. On an automatic machine, the panels flow continuously, and the only pauses come from loading new stacks or clearing the outfeed. The difference is not just the machine speed. It is the utilization rate of the machine and the operator across the full shift.
Then look at the finishing steps. If your current process requires hand scraping, touch-up sanding, or rework on a noticeable percentage of panels, that is a signal that the machine is not delivering the finish quality your downstream operations need. An automatic edgebander with integrated trimming and scraping stations will reduce that rework, but only if the upstream panel quality is consistent. If the rework is caused by operator technique on the semi-automatic machine, the automatic machine will eliminate that source of variation. If the rework is caused by poor panel preparation, the automatic machine will not help.
Finally, consider your labor situation. If you have experienced operators who can handle the demands of a semi-automatic line, the machine can be productive. If you are struggling to find and retain skilled operators, or if you expect to grow and need to train new people quickly, the automatic machine reduces the skill requirement for consistent output. The operator still needs training, but the machine handles the critical process steps, and the learning curve is shorter.
Which Shops Usually Benefit Most From Each Option
An automatic edgebander usually makes more sense when:
- Most daily work involves repeated panel parts with stable dimensions.
- The shop wants more stable finish quality across shifts and operators.
- Edge banding is already becoming a bottleneck after cutting or nesting.
- Management is trying to reduce manual rework and labor dependence.
- Downstream assembly benefits from more predictable part quality.
- The shop has consistent upstream panel quality from the saw or nesting machine.
- Production volume is expected to grow over the next two to three years.
A semi-automatic edgebander usually makes more sense when:
- Daily volume is still modest or inconsistent.
- The job mix changes frequently and batch sizes are small.
- Flexibility matters more than maximum continuous throughput.
- Skilled operators are available to manage more of the process directly.
- The business wants a practical production upgrade without moving immediately to a more structured high-output workflow.
- Panel sizes vary widely and changeovers would consume too much time on an automatic machine.
- The shop is transitioning from manual edgebanding and needs a manageable step up in capability.
These are not small differences. They determine whether edge banding behaves like a scalable production process or a flexible finishing step controlled mainly by operator handling. The right choice depends on which operating model matches your current reality and your growth plan. A shop that expects to double its output in two years should not buy a machine that will be the bottleneck at the new volume. A shop that values the ability to take on varied custom work should not buy a machine that forces every job into a continuous production rhythm.
Production Fit: Automatic Edgebander vs. Semi-Automatic Edgebander
If your goal is higher sustained output, more consistent edge quality, and smoother flow into assembly, an automatic edgebander usually delivers the better long-term result. If your goal is to keep mixed jobs moving, stay flexible at lower volume, and avoid building the whole shop around continuous panel processing too early, a semi-automatic edgebander can still be the smarter fit.
The real choice is not between two machine labels. It is between two operating models: one built for repeatable production flow and one built for flexibility with more manual involvement. Map your workflow, identify where the time actually goes, and the right automation level becomes much easier to see. Track your batch sizes, measure the time between panels, count the rework events, and look at your labor situation honestly. The machine that removes the dominant source of waste from your line is the one that will pay for itself, regardless of which category it falls into.
If you are evaluating specific machine configurations for your panel line, reviewing the available edgebander options against your actual batch sizes and shift structure is a practical next step. Bring your production data to the conversation, not just your budget. The machine that fits your workflow will deliver value from the first week. The machine that does not fit will cost you in labor, rework, and missed delivery dates for as long as you run it.