Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
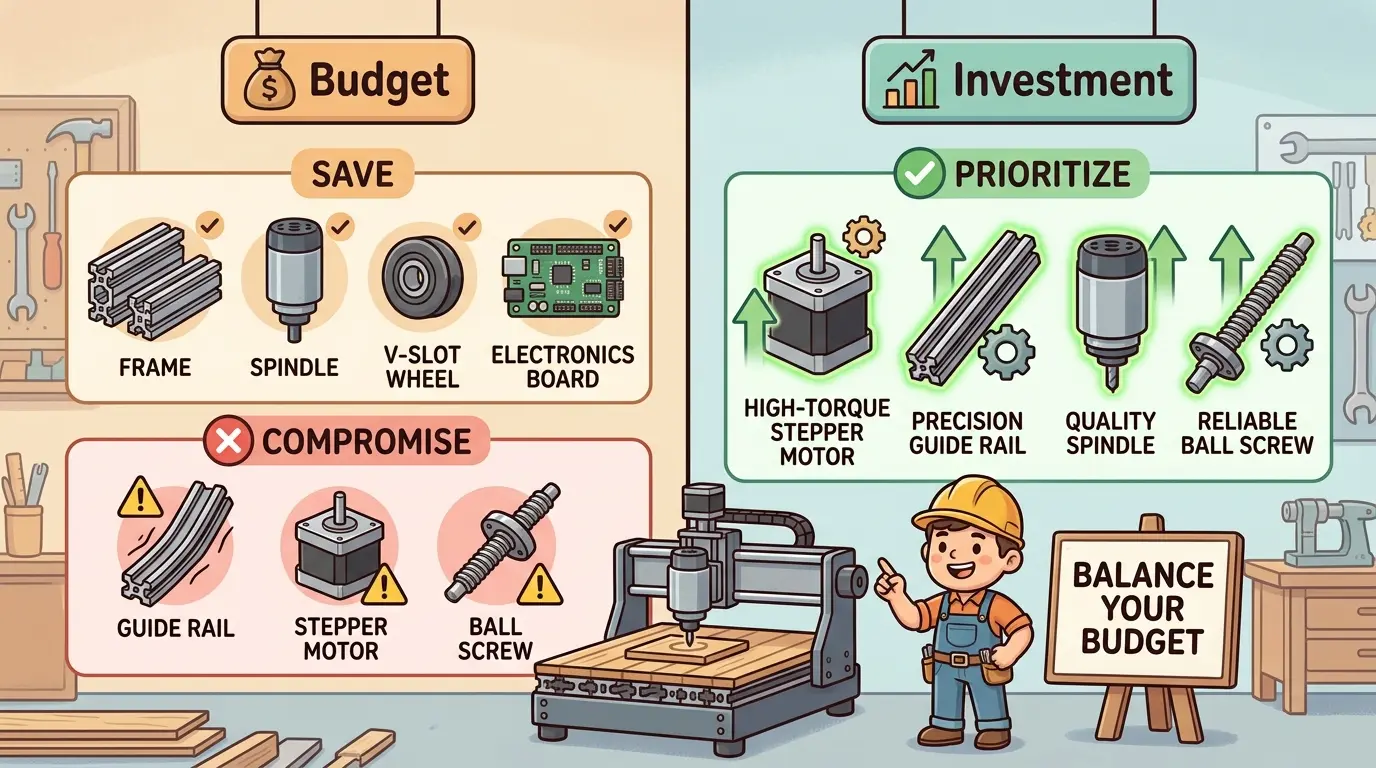
Budget CNC procurement fails when buyers start with a price ceiling and work backward, turning the decision into specification shopping before defining what underperformance would actually cost the shop. A bad week on a customer-facing machine—delayed delivery, lost margin, operator distrust—is expensive even if the equipment technically runs. This guide forces a practical triage: sort every expense into protection, capacity, or convenience, then cut from the last two first. The real risk is trimming ownership infrastructure—structure, motion quality, documentation, service response—to preserve visible ambition. Compare quotes by risk transfer, not headline price, and budget the whole cell, not just the base machine.
Start With the Cost of a Bad Week, Not the Spending Ceiling
The most common mistake in budget CNC buying is starting with the price cap and working backward. That approach turns the decision into specification shopping before anyone has defined what machine underperformance would actually cost the business. Different machine roles justify very different levels of risk, so the first question should always be practical: what happens if this machine is harder to set up, less stable than expected, or slower to recover from ordinary problems?
If the CNC is for learning, internal experimentation, fixture development, or low-risk prototype work, the business can tolerate more limitation and more buyer-managed inconvenience. A slower recovery path or narrower scope may be acceptable. If the machine will support customer delivery, scheduled internal throughput, commercial quoting, or repeat production, the budget must buy more than cutting ability. It must buy dependability. A bad week in that environment is expensive even if the machine technically still runs.
Delayed delivery, lost margin, avoided jobs, and operator distrust are the real costs of a weak purchase. Once those consequences are defined, the budget conversation changes. Buyers stop treating every line item as equally negotiable and start protecting the things that keep the workflow stable.
Sort Every Expense Into Protection, Capacity, or Convenience
A useful budgeting habit is to classify each cost into one of three groups:
- Protection: spending that keeps the current workflow stable.
- Capacity: spending that expands future scope, output, or growth headroom.
- Convenience: spending that helps the operator but does not materially protect output.
This framework changes how a quote reads. Structure, motion quality, electrical clarity, service response, documentation, safety, and installation discipline belong in protection. Larger work envelope, more ambitious automation, and speculative future capability belong in capacity. Accessories, optional software layers, or light-efficiency additions may fall into convenience depending on the application.
Once the quote is sorted this way, cost removal becomes cleaner. The first money removed should usually come from capacity and convenience before it comes from protection. Many buyers do the reverse. They hold onto future ambition because it is visible on the quote and quietly reduce the support and stability features that ownership depends on. That is why some apparently larger purchases underperform smaller, calmer ones. The bigger machine may have won on visible specification while losing on the things that make equipment usable every day.
Where Buyers Can Usually Save Without Hurting Today’s Work
The safest budget savings come from trimming features that solve tomorrow’s possible workload rather than today’s actual workload. Common examples include:
- Excess work envelope that the current part family does not require.
- Automation layers that current volume, staffing, or changeover patterns do not justify.
- Optional accessories that improve convenience without protecting process quality.
- Future-growth scope bought mainly out of anxiety rather than a near-term production plan.
These are sensible places to save because they reduce aspiration rather than reliability. A buyer who narrows unused capacity may still end up with a machine that runs present jobs well. A buyer who refuses to reduce visible ambition often ends up compromising the quieter parts of the ownership model instead. Smaller, more coherent machines frequently outperform overextended purchases. A shop that truly needs a modest work envelope and predictable daily behavior is often better served by honest fit than by a larger platform whose ownership conditions are thinner than the workload can tolerate.
Where Cheap Turns Into Daily Friction
Some budget cuts look harmless because the machine may still run and may even make an acceptable sample part. The trouble appears later, in drift, hesitation, inconsistent results, and maintenance burden.
| Budget Cut | Why It Looks Harmless at Purchase Time | What It Often Becomes in Real Ownership |
|---|---|---|
| Weak structure for the intended cut load | The sample part still looks acceptable | Finish inconsistency, more setup sensitivity, and lower operator confidence |
| Thin motion-system quality | The machine still moves and positions | Daily variation, more tuning, and harder recovery after wear begins to show |
| Vague control and electrical support | The interface still powers on and runs programs | Slower troubleshooting, more commissioning confusion, and higher dependence on one expert user |
| Minimal documentation | Buyers assume they can learn by doing | Lost time on normal maintenance, uncertain recovery steps, and avoidable downtime |
| Weak parts path or service response | It does not matter on day one | Small failures become long stops because the shop cannot recover quickly |
Budget buyers should be skeptical whenever savings come from the ownership infrastructure rather than from unused scope. The machine may not fail dramatically. It may simply become expensive to live with. The regretted budget machine is often not the one that collapsed. It is the one that remained just functional enough to keep the shop adapting around it while quietly consuming time and confidence.
Budget the Whole Cell, Not Only the Base Machine
Another frequent mistake is spending nearly everything on the base machine and leaving too little for the rest of the cell. CNC performance is shaped by more than the iron or frame. Tooling, workholding, extraction or coolant handling, inspection tools, CAM preparation, material staging, and operator readiness all influence whether the equipment performs as expected.
Buyers should budget the full operating system around the machine:
- Tooling that actually suits the planned materials and finish expectations.
- Hold-down or fixturing strong enough to produce repeatable work.
- Measurement tools that match the actual tolerance risk.
- Safe and clean operation around chips, dust, coolant, or noise.
- Programming and setup discipline appropriate to the team’s skill level.
If those pieces are weak, the machine often gets blamed for performance that the broader cell never supported. This matters especially in woodworking, panel processing, and mixed-material fabrication, where the CNC is only one step in a longer flow. Reviewing the Pandaxis machinery lineup as a system reminder rather than treating the CNC purchase as an isolated object can help buyers keep that broader perspective. The goal is not to spend more for the sake of completeness. It is to avoid the false economy of buying a machine that cannot show its value because the surrounding workflow was starved.
Smaller, Used, or Simpler Can Beat Bigger and Under-Supported
Budget buying does not always mean stripped-down new equipment. Sometimes the strongest move is a smaller machine whose support model is clearer. Sometimes it is a simpler automation level that the team can run confidently. Sometimes it is a used machine, provided the buyer understands the service history, wear state, control condition, and spare-parts exposure.
The key is not new versus used or simple versus advanced. The key is whether the choice preserves enough protection for the role the machine will actually play. A used machine can be the right buy when the shop knows how to inspect condition, evaluate recovery risk, and absorb some self-managed technical responsibility. A simpler new machine can be the right buy when it removes unnecessary complexity while still protecting daily stability. A larger low-price machine can be the wrong buy when the ownership burden is vague and the recovery path is weak.
Budget decisions should be made with the operating environment in mind. A small shop buying its first serious CNC usually cannot absorb the same level of ambiguity as a plant with experienced maintenance staff and deep process knowledge. The lower quote is not automatically the stronger budget fit if it assumes internal capabilities the buyer does not really have.
Match the Buying Strategy to the Shop You Actually Run
Budget logic changes depending on what kind of shop is making the purchase.
- Learning or lab environment: Safer to save on future headroom and advanced automation. Less safe to save on clarity, safety, and ease of recovery.
- Small job shop: Safer to save on speculative envelope. Less safe to save on flexibility, support, and tooling readiness.
- Growing cabinet or panel shop: Safer to save on decorative extras. Less safe to save on stability, hold-down logic, and how the machine fits the wider line.
- Capacity-constrained production supplier: Safer to save nowhere that slows recovery or creates operator doubt. Once the machine supports delivery, dependability becomes a budget requirement.
This framing helps prevent generic advice from being misapplied. The same budget cut can be harmless in a training environment and dangerous in a customer-facing production environment. Buyers need to judge each cost reduction against the business role of the machine, not against a universal budget rule.
Compare Quotes by Risk Transfer, Not Only by Headline Price
One reason the cheapest quote often wins is that risk transfer is hard to see quickly. A lower number may reflect more buyer-managed commissioning, thinner documentation, slower support, weaker parts access, or a greater expectation that the shop will solve problems alone. That can still be acceptable if the buyer chooses it knowingly. It is a bad budget decision when the buyer assumes the lower number represents the same ownership promise at a lower cost.
The right move is to compare quotes by scope and risk transfer. Ask:
- What is included in installation support?
- What documentation exists for routine maintenance and recovery?
- How does spare-parts access actually work?
- Which problems is the supplier prepared to help solve?
- Which problems is the buyer expected to solve without support?
Disciplined teams learn to compare CNC machinery quotes line by line rather than reacting to the headline number. Budget buying is not just spending less. It is making sure the reduced spend does not remove protections the workflow cannot afford to lose.
Know When the Budget Class Has Already Been Outgrown
Sometimes the cleanest budget decision is not a different cheap machine. It is acknowledging that the workload has already outgrown the budget class being considered. That point usually arrives when the machine is expected to support repeated customer deadlines, harder materials, longer production windows, or commercial consequences that punish weak recovery. Once the cost of underperformance becomes high enough, the buyer should stop pretending that every CNC category is financially interchangeable.
In those cases, reviewing what makes industrial CNC equipment worth the investment helps because the real buying question is no longer how to spend the least. It is how to avoid paying twice through downtime, workarounds, and eroded delivery confidence. The budget-class machine may still make sense for support work, prototyping, or learning. It just may no longer make sense as the main answer to the production problem.
A Final Approval Test Before You Sign
Before approving a budget CNC purchase, buyers should run a short practical test against the full ownership picture:
- Does this machine fit today’s real workload better than it fits tomorrow’s imagined workload?
- Have we protected stability, recovery, and safety before buying extra ambition?
- Is there enough budget left for tooling, fixturing, inspection, and normal operation?
- Do we understand which risks are being retained by the supplier and which are being shifted into our shop?
- Can our actual team support the level of ambiguity this purchase requires?
- If the machine has a bad week, will the business feel inconvenience or real damage?
If those answers remain uncomfortable, the machine is probably cheap in the wrong places. If the answers are calm and specific, the budget may be disciplined rather than merely low. Good budget CNC buying is not about winning the price contest. It is about deciding where savings are safe, where they are dangerous, and how to keep today’s workflow protected before paying for tomorrow’s ambition.