Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
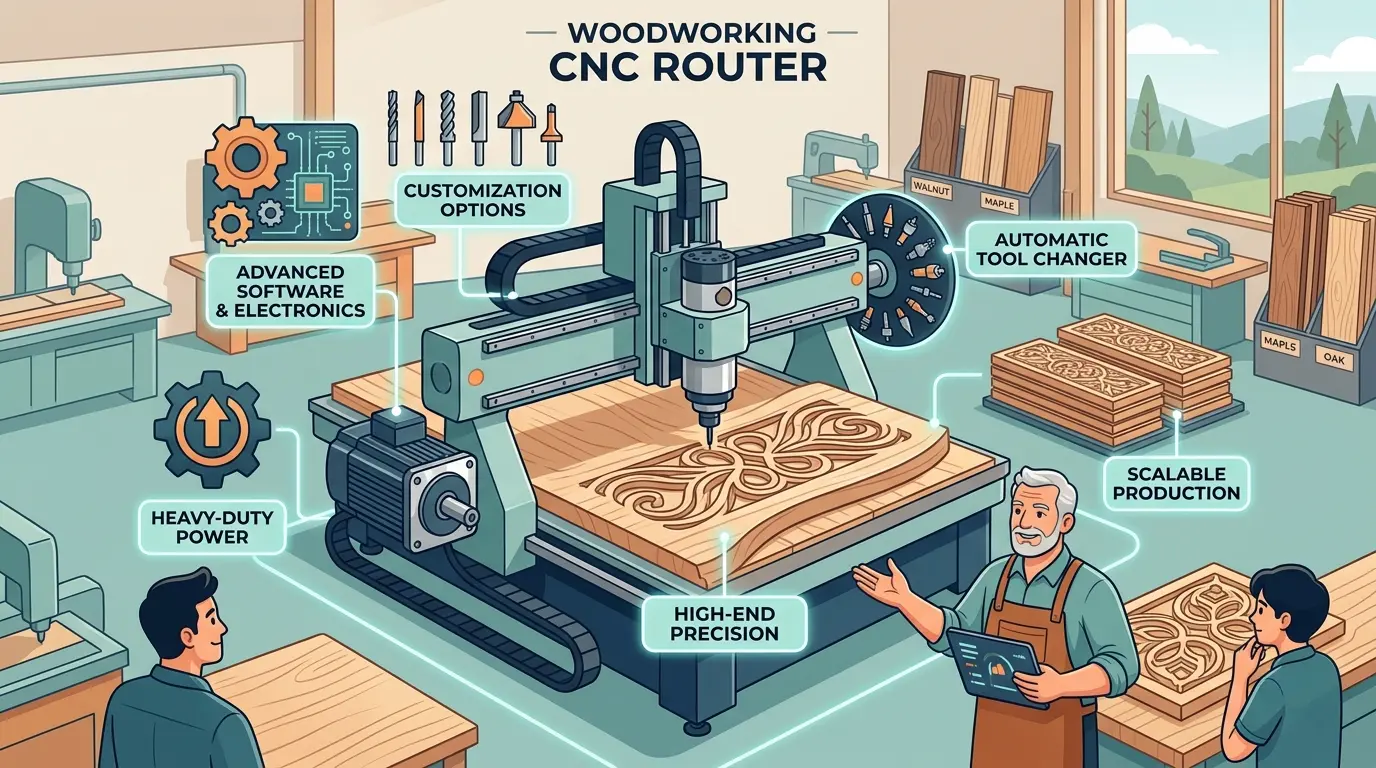
CNC router quotes for the same nominal task can diverge by tens of thousands of dollars, and the gap is rarely about brand markup. It is about the production assumptions buried in each offer: whether the frame can hold tolerances under sustained cutting, whether the vacuum table can keep small nested parts from shifting, and whether the quoted price includes startup support or leaves extraction, tooling, and training for you to solve after delivery. Before comparing top-line numbers, define the daily production burden the machine must carry, because an under-scoped router will cost more in labor, scrap, and downtime than the price difference it saved at purchase.
Why CNC Router Prices Vary So Widely in Woodworking
Ask five suppliers for a CNC router quote and you may receive five numbers that span a surprisingly wide range. On the surface, all five machines appear to do the same thing: they cut sheet goods with a computer-controlled spindle. Yet the price gap is rarely about markup or brand prestige. It is almost always about what each machine is actually expected to do on your shop floor.
A router that handles occasional custom work in a small job shop is a different machine from one that must run nested cabinet parts eight hours a day, five days a week. Both are called CNC routers. Both cut wood. But they are engineered to different production realities, and their prices reflect that difference.
This guide breaks down the cost drivers that separate one router quote from another. Instead of offering a single price range, we will walk through the production factors that determine what a router should cost for your specific workload.
The Quote Is a Production Assumption, Not Just an Equipment Price
Every router quote carries an implicit assumption about how the machine will be used. A lower-priced quote typically assumes a lighter duty cycle, more operator involvement, and less demanding material handling. A higher-priced quote assumes the machine must hold tolerances under sustained cutting loads, manage full sheets and small nested parts without shifting, and integrate into a broader production flow.
When buyers compare only the top-line numbers, they miss these assumptions. The machine that looks expensive may include a vacuum table with multiple zones, a higher-capacity spindle, and software that reduces setup time. The machine that looks cheap may require manual clamping, slower feed rates, and frequent operator correction. Both cut wood. Only one is scoped for daily production.
The price difference becomes visible only when the workload is defined. That is why the first step in any router purchase is not comparing quotes. It is defining the production burden the machine must carry.
Four Cost Layers That Explain Most Router Price Differences
Most router quotes can be understood by separating them into four layers. Each layer addresses a different production risk, and each one adds cost when it is specified properly.
| Cost Layer | What the Buyer Is Paying For | What Happens When It Is Under-Specified |
|---|---|---|
| Machine Stability | Structural rigidity, motion control, repeatable behavior under load | Slower feed rates, weaker edge quality, operators compensate manually |
| Cutting Environment | Spindle quality, toolholding, material range support | Heat buildup, rough edges, inconsistent performance across mixed jobs |
| Table and Hold-Down | Vacuum zones, clamping logic, sheet control, small-part stability | Part movement, extra tabs, hand finishing, wasted material |
| Startup and Ownership | Controls, software flow, diagnostics, training, service readiness | Long learning curves, difficult troubleshooting, hidden downtime |
This framework is more useful than the common cheap, mid-range, and premium labels because it shows what the extra money is actually preventing. A machine that costs 30 percent more than another is not necessarily better built. It may simply include more of these layers at a level that matches a harder production reality.
Machine Structure: The First Visible Price Divider
As routers move from occasional use toward sustained production, the frame and motion system typically add cost first. A machine that must hold cutting behavior steady over full working days needs a heavier gantry, better linear guides, and more rigid construction than one that runs a few jobs per week.
This is where many buyers underbuy. They see a machine that can technically produce the part during a demonstration and assume it is adequate for daily work. But a router chosen for production must do more than touch the material. It must maintain consistent cutting behavior so operators do not slow down feed rates to protect finish quality or dimensional accuracy.
Higher structural cost is not about buying prestige. It is about buying a wider zone of process stability. When the machine holds its behavior under load, operators trust it. When it does not, they compensate by cutting slower, checking parts more often, and reworking edges. That labor cost appears nowhere on the invoice, but it shows up in every production run.
Table Design and Hold-Down: Where Production Risk Hides
Table configuration is one of the clearest router price drivers because it determines whether the machine can hold full sheets, small nested parts, and mixed panel geometry with confidence. A vacuum table with multiple zones costs more than a simple T-slot table, but it removes real production risk.
This is especially important in CNC nesting machines, where weak hold-down forces programmers to add tabs, slow down cutting paths, and avoid small parts late in the nest. Every tab adds hand finishing. Every shifted part adds scrap. Every cautious programming choice adds cycle time.
Many early budgets underestimate this area because buyers think they are pricing a router when they are actually pricing only the cutting frame. The table is where the quote starts revealing whether the machine is meant for occasional flat work or for serious digital sheet conversion. If your workload includes nested cabinet parts, small components, or laminated panels, hold-down capability is not an accessory. It is the difference between a machine that runs unattended and one that demands constant attention.
Spindle and Tooling: The Cutting Environment Around the Motor
Buyers often treat the spindle as a single specification: horsepower. But price usually follows the broader cutting environment around it. Spindle quality, toolholding discipline, compatibility with the real material mix, and the operating range the router must support across panels, profiles, laminates, and acrylics all affect the quote.
The practical question is not simply how powerful the spindle is. It is what weekly job mix the spindle and tooling environment must support without becoming the line’s weak point. A machine that must stay believable across changing materials and visible-quality jobs may require a more disciplined cutting environment than one that runs the same material day after day.
This is why low-price comparisons become misleading. One offer may include a spindle that is acceptable under narrow conditions. Another may include a wider and calmer operating window. Both machines cut. Only one maintains edge quality and tool life across a demanding job mix.
Automation and Labor Economics: The Cost That Changes the Business Model
Loading support, unloading help, labeling logic, and broader handling integration naturally raise the router quote. They also change the labor model. In higher-output environments, these additions may make the difference between a router that cuts well and a router that actually fits the line rhythm.
Buyers sometimes compare automated and manual quotes as if both describe the same production reality. They usually do not. One may be selling base cutting capacity. The other may be selling lower operator dependence, faster job turnover, and a different daily output ceiling.
Automation is not necessary for every shop. A lighter-duty operation with occasional jobs may not justify the added cost. But automation cost should be judged against labor burden, not against a vague instinct to keep the price down. If the router requires one operator to load, monitor, and unload every part, that labor cost repeats on every job. Automation that reduces that burden may pay for itself quickly in a busy shop.
Software, Controls, and Diagnostics: The Hidden Ownership Cost
Some of the most important router cost drivers are hard to see in a short comparison. Control usability, software flow, diagnostics, training, startup support, and how easily the machine fits into the shop’s file and production process all influence the true cost of ownership.
Buyers often undervalue this layer because it is less visible than table size or spindle power. Over time, though, a machine that is awkward to program, harder to troubleshoot, or slower to stabilize can become more expensive than a higher-priced machine that starts faster and runs more predictably.
Experienced buyers stop thinking in terms of purchase price only. They think in terms of how long the machine takes to become ordinary. A router that reaches daily routine faster is often commercially cheaper than one that keeps demanding interpretation. If your programmers spend hours fighting the software, or your operators cannot diagnose a simple fault without calling support, the machine is costing you money every day it runs.
Startup Scope: What Happens After Installation
Price misunderstandings usually become expensive when buyers assume the quoted number already describes a production-ready system. One supplier may show a lower number because the buyer is expected to solve more of the surrounding system alone: extraction coordination, sheet handling, startup readiness, tool strategy, or parts of the hold-down logic. Another quote may look higher because it reflects a more complete package.
The lower quote is not automatically the cheaper choice. It may simply be less complete.
Experienced teams ask what happens in the first weeks after installation. Who helps stabilize production? How much of the setup logic is already anticipated? How much hidden engineering is still being pushed back onto the buyer? These questions rarely change the brochure headline, but they often change the real ownership cost.
A machine that arrives with unclear tooling requirements, no extraction coordination, and minimal training will take weeks to reach stable production. During that time, it is consuming labor, material, and patience. A machine that arrives with a clear startup plan may cost more upfront but reach full production much faster.
When a Lower Price Is Rational and When It Is a False Economy
Not every buyer should chase the most complete or most expensive router package. A lighter-duty shop, a more occasional custom workload, or a business still testing whether routing belongs in its mix may not need the same structural or automation scope as a factory depending on stable daily output.
Lower price becomes rational when the workload is genuinely lighter, the job mix is less punishing, and the business accepts more operator involvement without damaging margin. Lower price becomes false economy when the shop is quietly expecting stable production behavior from a machine that was never scoped to carry that burden calmly.
The important point is not that cheap is bad or expensive is good. It is that the price must match the severity of the production reality. A machine that is under-scoped for its workload will cost more in labor, scrap, and downtime than the price difference it saved at purchase.
When a Router Is the Wrong Machine Entirely
If the workload is mostly rectangular panel breakdown, buyers should pause before paying for routing flexibility they may not actually need. In that case, the shop should compare the router investment against the more direct logic of panel saws. The wrong comparison is expensive router versus cheap router. The better comparison may be router versus another machine family that removes the bottleneck more directly.
This is a major source of pricing confusion. A router can look expensive if the buyer is really shopping for rectangular throughput. The machine is then being judged against the wrong production goal. Once the workload shifts toward shape variation, drilling integration, or nested conversion, the economics change. But if the shop mostly needs straight panel sizing, router price will naturally feel harder to justify.
What Higher Price Usually Buys
In practice, higher router prices usually arise because the buyer wants one or more of these outcomes:
- More production stability under real cutting load.
- Less manual labor around loading, hold-down, or recovery work.
- Less missing scope after installation.
That framing is more useful than arguing about cheap versus premium equipment because it makes the spend objective visible. Extra money is usually trying to buy out a future operational problem. If the machine must hold tolerances on visible laminated parts, keep small nested components stable, and support consistent daily output, the quote naturally rises because the consequences of weak performance rise.
Common Pricing Mistakes Buyers Repeat
The most common router pricing mistakes are consistent across shops:
- Comparing only top-line numbers and not the production assumptions behind them.
- Overbuying for a future plan that never becomes a real workload.
- Underbuying structural confidence or hold-down in a production environment.
- Treating training, extraction coordination, tooling readiness, and service support as if they sit outside the machine decision.
- Comparing automated and manual offers as though they imply the same labor model.
These are not small details. They are the reason one machine can look attractively priced at purchase and become expensive in use.
Compare Quotes as Scope Maps, Not Price Tags
The cleanest way to compare price is to treat each quote as a scope map. What table configuration is actually included? What hold-down assumptions are built in? What startup support, software expectations, training, tooling logic, and handling structure are part of the offer? What is left for the buyer to solve after delivery?
For broader catalog-level comparison, some buyers also benefit from stepping back and reviewing the wider Pandaxis machinery lineup before finalizing whether they are actually choosing between router tiers or between different machine categories altogether.
The Right Price Is the Price of Enough Stability for the Work You Have
Router cost in woodworking is driven by the level of production risk, labor burden, and missing system scope the machine is expected to remove. The correct price is not the lowest number on the page. It is the price of enough structure, hold-down confidence, workflow support, and startup readiness to fit the shop’s actual workload without buying unnecessary capacity.
Once the buyer defines that workload clearly, the quote usually stops feeling mysterious. It becomes a decision about which problems the machine will remove, which ones it will leave behind, and how much uncertainty the business is willing to carry after the purchase order is signed.