Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
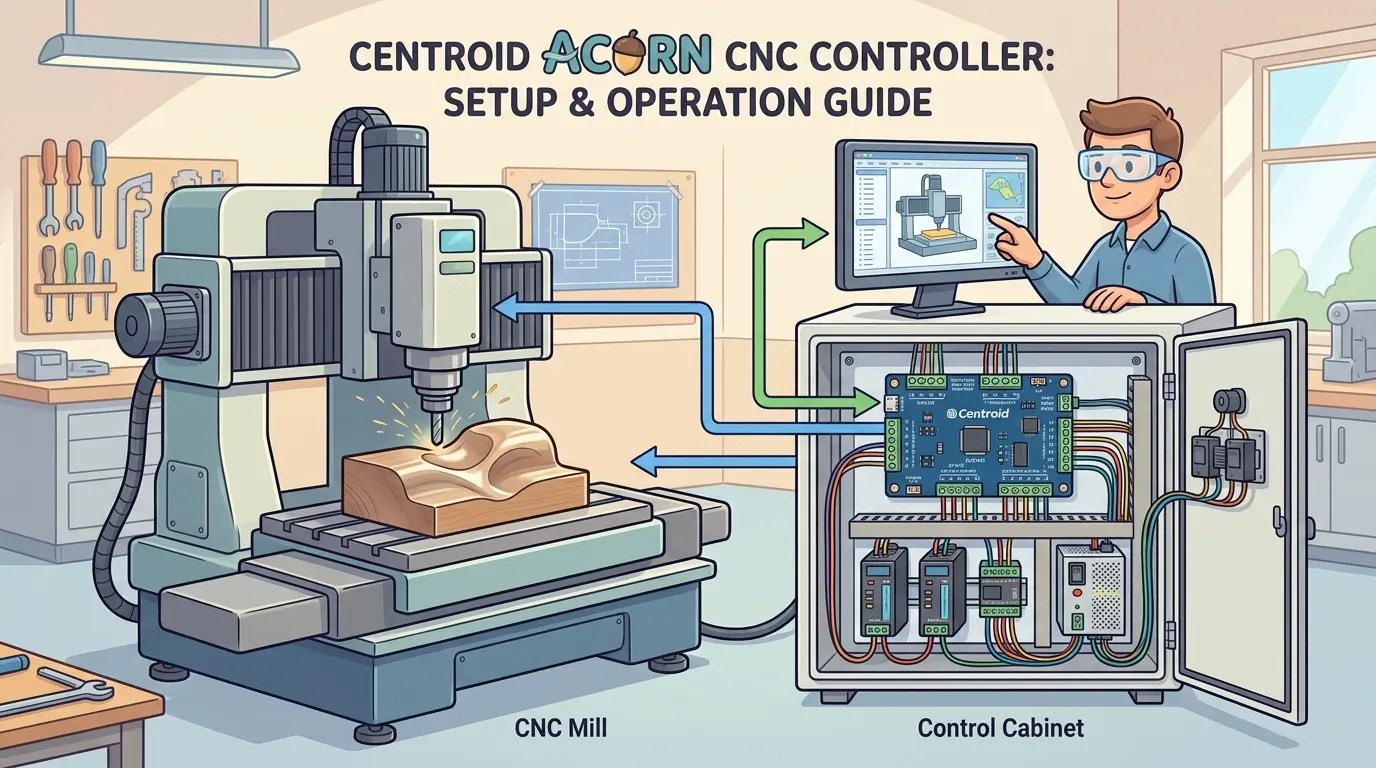
Before you spec a Centroid Acorn retrofit, stop comparing input counts and motor compatibility. The real decision hinges on whether your machine’s daily interruptions are control-layer failures or mechanical decay. If startup sequences shift, homing feels inconsistent, or work offsets depend on operator memory, a modern controller directly removes that uncertainty. But if vibration marks, backlash, or dimensional drift dominate part quality, no control upgrade will stiffen a worn frame or repair tired ways. Screen the donor honestly first, because the controller only pays back when the mechanical foundation is sound enough to benefit from disciplined repetition.
Start With the Operating Problem, Not the Feature List
Retrofit conversations often begin with the wrong question. Shops ask whether a controller like the Centroid Acorn has enough inputs, whether it supports their motors, or how it compares on paper to another brand. Those questions have answers, but they are not the first questions that matter.
The first question is simpler: what exactly is unreliable about the machine’s current behavior?
If startup routines change from day to day, if homing feels like a negotiation, if work offsets depend on one operator’s memory, or if recovery after an interruption turns into guesswork, those are control-layer problems. A modern controller can address them directly.
If the machine chatters because the frame is weak, if the spindle sounds rough, if backlash dominates part quality, or if the cabinet wiring is a tangle of unlabeled wires, a new controller will not fix those issues. It may make them easier to measure, but it will not make them go away.
The cleaner the pain statement, the more rational the controller decision becomes. Write down the three most frequent interruptions to production on the target machine. If at least two of them involve starting, referencing, offsetting, or resuming, the control layer is a legitimate suspect. If the interruptions are mechanical—vibration marks, inconsistent finish, dimensional drift across a single part—the control layer is not the bottleneck.
What a Modern Control Layer Actually Improves
When the donor machine is mechanically sound, upgrading the control environment changes daily operations in specific, measurable ways.
Startup becomes repeatable. Operators trust machines that power up the same way every morning. Homing and limit behavior becomes understandable, which matters because a machine that always knows where it is becomes easier to run without hesitation. The sequence is the same every day: power on, wait for the control to initialize, home each axis in the same order, verify the tool position, and load the last-used work offset. When that sequence is stable, the first part of the shift stops being a troubleshooting session.
Work-offset handling becomes structured rather than improvised. That is not glamorous, but it separates dependable machining from guesswork. A structured offset system means the operator records the zero position for each fixture once, labels it clearly, and recalls it when the job returns. No one has to re-find the edge, re-tram the vise, or re-measure the stock because the previous operator left the machine in an unknown state.
Accessory integration—spindle control, coolant, probing, auxiliary functions—becomes organized instead of ambiguous. When the spindle start command is tied to a clear M-code, when coolant follows the toolpath logic, and when probing routines run from a saved cycle rather than a hand-written macro, the machine behaves predictably across shifts.
Interruption recovery improves. Machines are judged hardest when a job stops mid-cycle, not when the first demo cut looks clean. A controller that makes restart predictable removes a significant source of shop-floor friction. The operator needs to know exactly where the tool is, what the machine believes the current position to be, and what the next move will be. If the controller can answer those three questions without guesswork, the restart takes minutes instead of an hour.
These benefits all point in the same direction: they remove uncertainty from repetition. That is what most small shops and retrofit builders are really buying when they upgrade control.
What a Controller Cannot Fix
The boundary matters as much as the benefit.
A controller cannot create rigidity where the donor lacks it. It cannot remove wear from ways, bearings, screws, or spindle components. It cannot make careless cabinet wiring safe by simply being installed. It cannot turn a mechanically tired machine into a dependable production platform through interface quality alone.
Consider a knee mill that has been in service for twenty years. The ways are worn in the center of travel, the spindle bearings have a detectable rumble at operating speed, and the leadscrew backlash measures several thousandths. A new controller will make the axis moves smoother, but the physical backlash remains. The part dimensions will still vary by the same amount. The controller can compensate for backlash in software, but the compensation is a constant value applied across the entire travel. If the wear is uneven, the compensation is wrong in some zones and right in others.
The same logic applies to a router frame that flexes under cutting load. The controller can accelerate and decelerate the axes cleanly, but it cannot stiffen the gantry. The deflection is a function of the frame geometry and the cutting forces, not the control loop.
It also cannot rescue a project with no commissioning discipline. A strong controller still needs a proper electrical plan, correct grounding, thoughtful I/O mapping, sensor validation, and a prove-out routine that checks real machine behavior rather than assuming success from first motion.
Some retrofit projects fail and the controller gets blamed because it is the newest visible component. The true weakness usually lives elsewhere. Buyers who stay honest about this distinction save money and frustration.
The Features That Matter Are the Boring Ones
Controller discussions tend to drift toward flashy capabilities, but the features that earn their keep are the ones operators stop noticing once they work reliably.
Good homing behavior matters because nobody wants to negotiate machine position every morning. The homing sequence should be deterministic: each axis moves toward its limit switch at a defined speed, backs off, then approaches again at a slower speed to find the exact index position. If the machine homes the same way every time, the operator can trust the coordinate system from the first cut of the day.
Stable offset management matters because repeat jobs are where machine discipline pays off. When a job comes back after three weeks, the operator should be able to load the program, call up the saved offset, and start cutting. If the offset system is reliable, the setup time drops from an hour to ten minutes.
Clear I/O behavior matters because ambiguous accessory control wastes time and confidence. The spindle should start when the program says start, the coolant should flow when the program says flow, and the probe should trigger when the program says probe. If the operator has to check whether the accessory actually responded, the machine is not doing its job.
Predictable machine state matters because operators need to know what the machine believes, not guess what it might do. The control should display the current mode, the active offset, the tool number, and the feed rate override at all times. If the operator has to search for that information, the interface is failing.
Consistent recovery matters because every shop eventually sees stops, restarts, tool changes, or interrupted jobs. The recovery procedure should be the same every time: identify the current position, verify the tool, decide whether to restart from the beginning of the current operation or from a safe retract point, and execute the restart. If the operator has to invent the procedure on the spot, the machine is not dependable.
The best features are not the ones that sound advanced in a forum thread. They are the ones that reduce the number of sentences an operator has to say before cutting. If the machine starts, homes, references, and resumes with less explanation, the controller is doing useful work.
Setup Is Three Separate Projects, Not One Board Swap
The phrase “controller upgrade” makes the work sound smaller than it is. In practice, setup breaks into three connected projects.
The first is electrical architecture. Cabinet layout, power distribution, grounding, shielding, cable routing, noise management, and safe separation of signal and power all live here. If this layer is careless, the rest of the project inherits that carelessness.
A typical retrofit cabinet needs a main disconnect, a transformer if the machine runs on different voltage than the shop supply, fuses or breakers for each branch circuit, a DC power supply for the logic and I/O, and a separate supply for the motor drives. The signal cables from the encoders and limit switches should run in shielded cable, with the shield grounded at one end only. The power cables to the motors should be routed separately from the signal cables, ideally in a different wire duct or at least on the opposite side of the cabinet.
Grounding deserves special attention. The control chassis, the motor drives, the spindle drive, and the machine frame should all be tied to a single ground point. If the machine has multiple ground paths, ground loops can form, and those loops cause erratic behavior that looks like a controller fault but is actually an electrical problem.
The second is machine behavior mapping. Inputs must be assigned sensibly. Limits and homing must be validated. Motion assumptions must match reality. Spindle and accessory logic must be tested under real conditions, not just once on the bench.
This means checking that the limit switches actually trigger at the right positions, that the homing direction is correct for each axis, that the axis directions match the program conventions, and that the spindle enable signal reaches the drive. It also means verifying that the emergency stop chain works: pressing E-stop should remove power from the motor drives, not just stop the program.
The third is operator routine design. This part is ignored too often. The machine needs a repeatable start sequence, referencing process, offset routine, tool-change logic, and recovery method that another operator could understand. A working retrofit that only the builder can drive is still a weak business asset.
Write the start-up procedure on a card and tape it to the cabinet. Include the power-on sequence, the homing order, the offset loading steps, and the first-part inspection check. If the procedure takes more than one page, simplify it. The goal is that a new operator can follow the card and get the machine cutting without calling the builder.
The controller does not become valuable until all three projects are finished well enough to survive ordinary use.
Strong Use Cases for an Acorn-Style Upgrade
This controller path makes the most sense when the donor still has mechanical value and the workload is regular enough that better control discipline will pay back.
Strong use cases include:
- Retrofit mills or routers whose base structure is still worth keeping.
- Small shops modernizing machine behavior without discarding good iron.
- Owners frustrated by awkward legacy routines rather than by raw machine geometry.
- Environments where the same jobs return often enough that startup, offsets, and recovery need to become predictable.
- Teams willing to do real cabinet, wiring, and commissioning work instead of treating the controller like a shortcut.
In those cases, a controller like Acorn can help transform a machine from “something that runs” into “something that runs with structure.”
Consider a small job shop that runs a Bridgeport-style mill for prototype work and short production runs. The machine is mechanically sound, the spindle is true, and the backlash is within acceptable limits. But the existing control is a legacy unit that requires a specific sequence of button presses to start, has no saved offsets, and loses its position reference if the power blips. Every job starts with a fifteen-minute argument with the machine. That shop is a strong candidate for a retrofit.
The same logic applies to a router table used for cabinet parts. The frame is rigid, the spindle is new, and the vacuum table holds the stock reliably. But the control is an open-source board that requires a laptop to operate, has no dedicated interface, and crashes if the USB connection is disturbed. The operator spends more time managing the computer than cutting parts. A dedicated controller with a proper pendant and a stable interface would eliminate the daily friction.
Weak Use Cases That Usually Lead to Disappointment
There are also cases where the controller decision is more emotional than rational.
If the donor is mechanically exhausted, the controller may simply make old flaws easier to measure. If the electrical cabinet is treated casually, the project may become a troubleshooting loop instead of an upgrade. If the machine is only cut occasionally and the operator routine stays informal, the return from a modern control layer may be smaller than expected.
If the owner is really trying to avoid admitting that the whole machine should be replaced, the control project can turn into delayed purchasing rather than sound modernization.
These are not rare cases. They are common enough that they should be screened openly before spending begins.
A machine that has been crashed repeatedly, has a bent spindle, or has ways that are visibly scored is not a good retrofit candidate. The controller will not straighten the spindle or repair the ways. The machine will still produce parts that are out of tolerance, and the operator will still spend time measuring and rejecting work.
Similarly, a machine that runs only a few hours per week may not justify the retrofit effort. The controller will improve the experience, but the payback period will be long. If the machine is a backup that gets used once a month, the upgrade is hard to justify on financial grounds.
Judge the Upgrade by Repetition, Not by First Motion
A controller project is not successful because the axes move. That milestone matters, but it is far too early to declare the machine upgraded.
The real test is repetition.
Can the machine power up the same way tomorrow? Can it home consistently with confidence? Can work offsets be applied without private knowledge? Can another operator recover after an interruption without calling the builder? Can the same part be run again next week without rediscovering the workflow?
If the answer to those questions is yes, the control layer is doing real work. If the answer is no, the retrofit may have moved forward technically while still failing operationally.
The best prove-out method is a repeated job that includes normal shop friction: power cycles, operator changes, tool changes, and at least one interruption. Controllers earn their reputation in ordinary moments, not in clean demos.
Set up a test that runs the same part three times over three days. On the first day, run the part, shut the machine down, and leave it overnight. On the second day, have a different operator start the machine, home it, load the offset, and run the same part. On the third day, interrupt the cycle mid-way through, simulate a tool change, and restart the job. If the machine handles all three scenarios without confusion, the retrofit is working.
When the Upgrade Reveals the Donor Has Reached Its Limit
Sometimes a better control path is still the correct move even if it exposes bad news. A modern control can clarify the machine’s remaining weaknesses so sharply that the owner finally sees the next decision clearly.
Maybe startup is fixed, but the machine still cannot hold the tolerance the work now needs. Maybe offset handling becomes clean, but backlash or wear still dominates outcomes. Maybe the cabinet is now disciplined, but the donor’s structure still makes confident repeat work unrealistic.
That result is not a total loss. It can be a useful diagnosis. The trouble begins only when the owner keeps spending as if the controller proved the donor deserves unlimited continuation.
If the machine discussion is widening into a larger equipment decision, it helps to compare machinery quotes without missing critical details and to revisit what makes industrial CNC equipment worth the investment. In some cases, the smartest upgrade is the one that tells you to stop upgrading.
If the conversation broadens further, the Pandaxis product catalog can serve as a category reference for new equipment options, not as proof that every retrofit should keep evolving forever.
Budgeting the Retrofit Realistically
A retrofit is not just the cost of the controller board. The total budget includes the controller, the motor drives if the existing ones are not compatible, the power supply, the cabinet components, the wiring, the connectors, the limit switches if the existing ones are unreliable, the pendant or operator interface, and the labor hours for the electrical work and commissioning.
A common mistake is budgeting only for the controller and then discovering that the existing stepper drives are too old to interface cleanly, or that the spindle drive needs a separate analog signal converter, or that the limit switches are mechanical units that need to be replaced with inductive sensors for reliable homing.
The labor hours are often the largest line item. A clean retrofit with a well-documented cabinet can take a skilled electrician or machine builder forty to sixty hours. That includes the cabinet layout, the wiring, the testing, the commissioning, and the documentation. If the shop does the work in-house, those hours are still real costs because they are hours not spent on production.
The payback calculation should include the reduction in setup time, the reduction in scrap from mispositioned parts, the reduction in troubleshooting time, and the improvement in operator confidence. If the machine currently loses an hour per shift to control-related issues, the retrofit pays for itself quickly. If the machine runs smoothly most of the time and the control is only mildly annoying, the payback is slower.
Commissioning Checklist Before First Production Cut
Before the machine is allowed to cut a production part, the following checks should be complete:
- All limit switches trigger the correct axis and direction.
- Homing completes in the same position every time, verified by a dial indicator.
- Axis directions match the program conventions; a test move in each direction confirms the sign.
- Backlash compensation is measured and entered for each axis, if the control supports it.
- Spindle start, stop, and speed commands are verified at the spindle, not just at the interface.
- Coolant and any auxiliary outputs are verified under program control.
- Emergency stop removes power from the motor drives and the spindle.
- A test part is cut and measured against the drawing, with the dimensions recorded.
- The start-up procedure is written, posted, and followed by a second operator without assistance.
Each of these checks takes a few minutes, but together they prevent the most common failure modes. A machine that passes this checklist is ready for production. A machine that fails any item is not ready, regardless of how good the controller feels.
The Right Controller Choice Feels Operational, Not Emotional
Acorn makes the most sense when you need a better operating system for a machine that still deserves disciplined use. Its most important features are the ones that remove uncertainty from daily repetition. Its biggest setup risk is treating the project like a simple board replacement when it is really an electrical, behavioral, and operator-routine overhaul. Its best use cases begin with mechanically worthwhile donors and teams that care about running the machine cleanly, not just moving the axes.
If that is your situation, the controller can be a meaningful upgrade. If it is not, the controller may only shine a brighter light on problems the project was trying not to name. That is still useful information, but it is not the same thing as a successful modernization path.
The decision ultimately comes down to the machine’s mechanical condition and the shop’s willingness to do the full scope of work. A clean retrofit on a sound machine is one of the best investments a small shop can make. A rushed retrofit on a tired machine is a way to spend money and still end up with a machine that cannot hold tolerance. Screen the machine honestly, budget the labor realistically, and commission the control thoroughly. If those three conditions are met, the retrofit will earn its keep.