Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
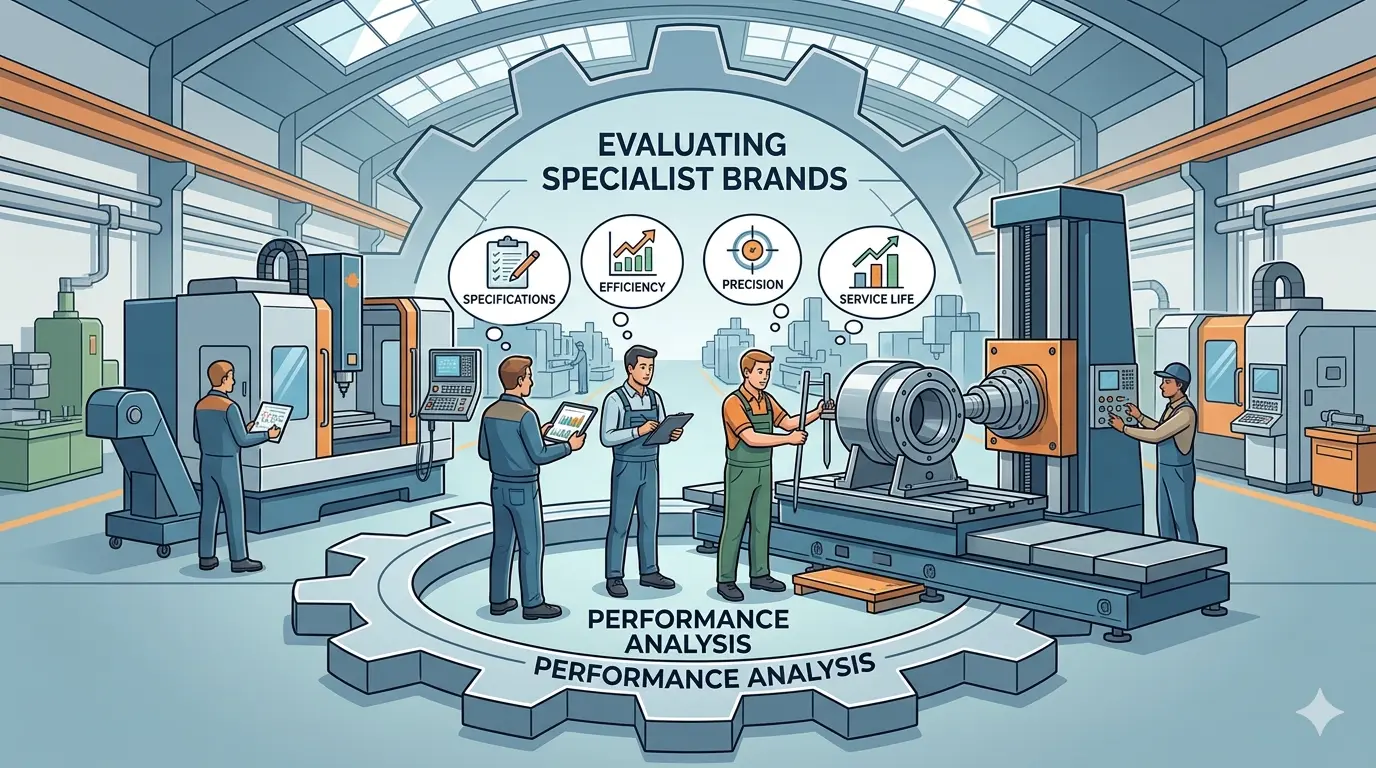
When a production manager enters a capital-equipment review already convinced that a Chevalier grinder or a Kuraki boring mill is the answer, the procurement process has already gone sideways. A respected nameplate does not solve a bottleneck; it only becomes relevant after you have proven that your part family demands a specialist machine class, that your plant can support the ownership model, and that local service reality will keep the machine cutting. This evaluation sequence forces buyers to anchor every decision in physical production facts—part size, weight, access, finish, and fixturing—before any brand badge carries the argument. Skip these gates, and you risk buying prestige instead of uptime.
Start With the Work, Not the Nameplate
Every few months, a production manager walks into a capital-equipment review with a name already on their lips. Chevalier. Kuraki. Sometimes it is a machine they ran at a previous plant. Sometimes it is a brand that came up in a trade publication or a conversation with a competitor. The instinct is understandable. These builders have decades of engineering behind them, and their machines carry real weight on a shop floor.
But the name is not the decision. The decision is whether your plant has a problem that a specialist machine class can solve, whether your facility can support the ownership model that comes with it, and whether the specific machine you are considering will remove the friction you actually live with. A respected brand attached to the wrong machine family, or installed in a plant that is not ready for it, produces the same downtime, rework, and frustration as any other mismatched purchase. It just costs more upfront.
This article walks through a practical evaluation sequence for specialist industrial machines. The logic applies whether you are looking at a Kuraki boring mill, a Chevalier grinder or machining center, or any other builder with a strong reputation in a narrow product category. The goal is to keep the evaluation anchored to physical production realities instead of letting brand prestige carry the argument.
Gate 1: Prove the Problem Is Actually Specialist
Before any brand enters the conversation, define the production problem in concrete language. What exactly is the current equipment failing to do cleanly? Write it down. Be specific.
Are workpieces now large or heavy enough that ordinary handling is becoming slow, risky, or inconsistent? A part that used to fit comfortably on a standard machining center table may now require awkward overhang, temporary fixturing, or multiple setups that each introduce error. When operators start building custom risers, extension plates, or improvised outrigger supports, that is a signal the work has outgrown the machine class.
Are deep-access features, long reaches, or part geometry turning conventional setups into compromises? Boring mills exist because some work requires reaching deep into a part, machining large-diameter features with tight concentricity, or holding alignment across long travel distances. If your parts increasingly look like that, you are drifting toward boring-mill territory whether you planned to or not.
Are finish, flatness, or geometry demands pointing toward grinding or other specialist process logic? A machining center can produce acceptable finishes for many applications, but when tolerances tighten or surface requirements become consistent and demanding, the process logic changes. Grinding is not a variation of milling. It is a different physical process with different machine stiffness, different spindle characteristics, and different thermal behavior.
Are current jobs technically possible but only after too much staging, too much operator workaround, or too much lost time? This is often the quietest signal. The parts get made. The quality passes inspection. But the setup takes twice as long as it should, the operator has developed a personal sequence of tricks to make it work, and every repeat order feels like reinventing the process.
If those pressures are still vague, the specialist shortlist is premature. Specialist machines make sense when the pain is specific, repeatable, and expensive enough that a narrower machine class is justified. If the plant cannot explain the bottleneck clearly, it is not ready to compare prestige-heavy brands honestly. The comparison will default to marketing material and reputation, which is exactly where expensive mistakes begin.
Gate 2: Name the Machine Family Before the Badge
This is the gate many buyers resist because it removes some of the glamour. A boring mill conversation is not the same as a general machining-center conversation. A grinding machine conversation is not the same as a broad milling conversation. A large bridge-type or floor-type machine has a different ownership model than a flexible all-purpose machining center. Different machine families create different handling demands, different uptime risks, different staffing expectations, and different floor-planning consequences.
Consider the practical differences. A horizontal boring mill typically handles large, heavy workpieces that need machining on multiple faces. The work often stays stationary while the tool moves, which means fixturing strategy is fundamentally different from a VMC where the part moves through the spindle. Setup time on a boring mill is measured in hours, not minutes, and the payoff comes from holding tight geometry across large features without re-fixturing.
A surface grinder, by contrast, is a finishing machine. It removes small amounts of material with high precision. The work envelope is usually smaller, the setup logic is different, and the machine is judged by its ability to hold flatness and finish over long cycles. Comparing a grinder to a machining center on price alone misses the point entirely. They solve different problems.
That is why the plant has to decide the machine family first. Kuraki matters only after the boring-mill question is real. Chevalier matters only after the shop knows what process burden it is actually trying to solve. The same is true for every respected specialist builder. The brand becomes relevant only after the machine class is already justified by the work. When buyers skip this gate, the brand becomes a proxy for ambition rather than a solution to a physical problem.
Gate 3: Translate the Parts Into Physical Demands
Good specialist-machine buying starts with physical facts, not catalog language. Write down the actual burden created by the parts:
- Size range. What is the largest envelope you must accommodate, and how often does that size actually appear in the production mix?
- Weight range. What is the heaviest workpiece, and how does that weight affect fixturing, handling, and machine rigidity requirements?
- Access requirements. Do features sit deep inside the part, on opposing faces, or in positions that require long reach or special tooling?
- Fixturing complexity. How much of the setup depends on custom fixtures, and how repeatable is that fixturing across multiple orders?
- Required surface quality. What finish do the parts actually need, and what process can deliver that finish consistently?
- Geometry stability. Are you holding tight tolerances across large dimensions, and how does temperature or part deflection affect that?
- How much of the job depends on setup integrity. If the setup shifts, does the part scrap, or can it be recovered?
- How often the same class of work repeats. Is this a recurring production family or a one-off job that will not justify a dedicated machine?
These details matter because specialist machines are usually justified by physical constraints that broader equipment cannot absorb efficiently any longer. If the part family demands large work envelopes, heavy support, stable deep-access machining, or a finish process the current line does not handle cleanly, then the machine family begins to reveal itself.
This step also eliminates false comparisons. If one candidate solves a large-work boring problem and another solves a precision grinding problem, they do not belong in the same emotional brand debate just because both are respected names. The parts should shape the shortlist before the shortlist becomes a story.
Gate 4: Make the Plant Prove It Is Ready for the Ownership Model
Specialist machines do not create value in isolation. They create value inside a plant that can support the ownership model that comes with them. That means the buyer has to ask whether the surrounding system is actually ready.
Can the plant lift, stage, and reference the target parts safely and repeatably? A boring mill that can handle a 10-ton workpiece is useless if the shop crane cannot lift it, if the floor cannot support the combined weight of machine and part, or if the staging area cannot hold the part while the machine is in cycle. Large-machine ownership is a material-handling commitment, not just a machine purchase.
Is fixturing understood, or is it still theoretical and optimistic? Some shops assume they will figure out fixturing after the machine arrives. That is a dangerous assumption. Specialist machines often require more sophisticated fixturing than general-purpose equipment because the parts are larger, heavier, or more geometrically demanding. If the fixturing plan is vague, the machine will sit idle while operators improvise.
Does metrology match the level of accuracy or finish that justifies the new machine class? A machine that can hold tight tolerances is only useful if the shop can verify those tolerances. If the current inspection equipment cannot measure the parts to the required accuracy, the new machine will produce parts that cannot be certified. That is a quality bottleneck, not a solution.
Can programming and setup teams absorb the new process logic without learning under full production pressure? Specialist machines often require different programming approaches, different tooling strategies, and different setup sequences. If the current team has never run a boring mill or a large grinder, the learning curve will be real. Training time must be budgeted before production starts, not during it.
Have utilities, floor space, maintenance access, and service clearance been planned honestly? Large machines need three-phase power, compressed air, and sometimes special foundations. They need clearance for tool changes, part loading, and maintenance access. If the machine is shoehorned into a space that does not fit it, every future maintenance event becomes a logistics problem.
If the answer to those questions is weak, the plant may not be ready even if the machine family is correct. This is an important distinction. A shop can identify the right specialist class and still buy too early because the surrounding factory system has not caught up.
Gate 5: Treat Service Geography as Part of the Machine
This gate decides many capital-equipment outcomes more than buyers like to admit. A respected specialist machine can still become the wrong purchase if local service, commissioning, alignment support, parts access, or training support are weak. In narrow-bottleneck operations, service quality is not an afterthought. It is part of the machine’s real productive value.
Consider what happens when a boring mill goes down. The machine is likely the only one in the plant capable of handling certain workpieces. Every hour of downtime is lost production that cannot be shifted to another machine. If the service technician is three days away, that is three days of dead capacity. If the spare part must be shipped from overseas, that is a week or more of downtime.
So the buyer should ask:
- Who installs and commissions the machine in this region? Is it the manufacturer, a local distributor, or a third-party contractor? What is their track record with this specific machine class?
- Who performs field geometry checks or alignment work? Large machines need periodic alignment verification. If the local service provider cannot do this, the machine will drift out of specification over time.
- How quickly can technical help arrive when the machine is down? Is there a guaranteed response time, or is it best-effort? What happens during holidays or peak seasons?
- What spare-parts path is realistic in practice, not only in theory? Are common wear items stocked locally, or must every part be ordered from the factory? What is the actual lead time for a spindle bearing or a control board?
- How much self-sufficiency will maintenance staff need to carry? If local support is thin, the plant must invest in training its own maintenance team. That is a real cost and a real capability requirement.
Those questions are not administrative details. They affect uptime, confidence, and the real cost of ownership. A specialist machine chosen to remove a high-value bottleneck can easily create a different bottleneck if support reality is weak.
Gate 6: Convert Reputation Into Plant Outcomes
Strong brands carry real reputations for a reason. Chevalier has built its name on grinding and milling equipment that performs reliably across many installations. Kuraki is known for boring mills that hold geometry under heavy cutting conditions. Those reputations are earned through years of engineering and field performance.
But reputation has to be translated into outcomes inside your own plant before it becomes economically useful. Ask what the badge becomes in practice.
Does it become lower setup compromise? If the machine family fits your part geometry honestly, setups should become simpler and more repeatable. If the machine still requires the same awkward staging and operator workarounds, the reputation has not solved your problem.
Does it become a machine family that finally fits the part geometry honestly? The right specialist machine should eliminate the compromises you have been living with. Parts should fit the work envelope without overhang tricks. Features should be reachable without custom tooling extensions. The machine should match the work, not fight it.
Does it become support you can actually reach when you need it? A brand with a strong global reputation is only useful if that reputation translates into local service reality. If the nearest qualified technician is hundreds of miles away, the global reputation does not help you on a Tuesday afternoon when the machine is down.
Does it become a realistic long-term fit for the next stage of work instead of a symbolic purchase? The machine will be on your floor for a decade or more. Will the work you are doing now still be the work you are doing in five years? If the part family is likely to change, will this machine adapt, or will it become an expensive monument to a past production strategy?
If the answer is unclear, then the reputation remains abstract. That is the missing discipline in many specialist-brand conversations. Buyers admire a respected name but never translate it into uptime, handling logic, inspection confidence, and process fit inside their own facility. The reputation may be real and still not be the right economic answer for this plant.
Gate 7: Used Specialist Machines Need Harder Evidence, Not Softer Enthusiasm
Many shops meet specialist brands through the used market. That is perfectly reasonable. A well-maintained used boring mill or grinder can deliver excellent value at a fraction of the new-machine price. It is also how many mid-size shops gain access to machine classes that would otherwise be out of budget.
But the used market increases the screening burden. Older specialist equipment needs hard evidence on condition, control generation, rebuild history, retrofit history, documentation, wear state, and local serviceability. Buyers should not ask whether the brand was excellent when the machine was new. They should ask whether this specific machine can support this specific workload without becoming a rebuild or downtime trap.
Consider the control system. A 20-year-old machine may have a control that is no longer supported by the manufacturer. If the control board fails, can it be replaced? Is there a retrofit path, and what does that cost? Some shops buy a used machine and immediately budget for a control retrofit, which changes the total cost calculation significantly.
Consider the wear state. A boring mill that has run heavy production for 15 years will have wear in the ways, the spindle bearings, and the feed system. Some of that wear can be measured and evaluated. Some of it only reveals itself under load. A machine that looks clean in a walk-around inspection may still have significant wear that affects accuracy and finish.
Consider the documentation. Does the machine come with manuals, electrical schematics, and maintenance records? If not, the maintenance team will be working blind. That is a real risk on specialist equipment where the service knowledge is less common than on standard machining centers.
This is where badge value can become dangerous. A respected used machine may still be a poor local ownership decision if its support path is weak, if the controls are too far behind the plant’s comfort level, or if the machine’s real condition is being guessed rather than verified. The stronger the brand reputation, the more tempting it is to skip inspection discipline. That temptation should be resisted hardest on specialist equipment, not least.
Gate 8: Force Every Candidate Through the Same Buying Sheet
Once a brand survives the earlier gates, compare it with a standardized buying sheet rather than open-ended storytelling. The sheet should include:
- Target part-family size and weight. Does the machine envelope actually accommodate the parts you need to run, with margin for future variation?
- Access and geometry burden. Can the machine reach the features you need to machine, and can it hold the geometry you require across the full travel?
- Finish or tolerance burden. What surface finish and tolerance can the machine hold in production, not just in the brochure?
- Handling and fixturing needs. What does the machine require in terms of part loading, fixturing, and staging? Does your plant have that capability?
- Service and commissioning path. Who installs it, who supports it, and how quickly can help arrive?
- Utility and floor-space demands. What power, air, foundation, and clearance does the machine need? Does your facility have it?
- Operator and programmer readiness. Does your team have the skills to run this machine class, or is training required?
- Maintenance burden. What routine maintenance does the machine require, and what is the expected cost and frequency?
- Whether the machine removes the dominant weekly friction cleanly. This is the bottom-line question. Does the machine solve the specific problem that brought you to the specialist market in the first place?
This method exposes the truth quickly. One candidate may fit the work technically but demand service support the region cannot provide. Another may be operationally strong but oversized for the actual workload. Another may look economical until the plant-level handling upgrades are priced honestly.
If the quote stage is already live, this is the right moment to compare machinery quotes without missing critical details. Commissioning scope, included service, and hidden ownership assumptions should be on the table. A quote that looks lower may simply exclude items that another quote includes. The buying sheet forces those differences into the open.
Gate 9: Check Whether the Purchase Removes Friction or Only Adds Prestige
This is the emotional gate. Industrial buyers can drift into a simple belief: if the work is demanding, then more specialist machine identity must be safer. That is not always true. Specialist equipment can remove friction, but it can also add cost in programming complexity, scheduling, handling, maintenance, tooling, and lost flexibility.
Consider the scheduling impact. A specialist machine is often a bottleneck by design. It is the only machine in the plant that can handle certain work. That means every job that needs that machine must be scheduled around it. If the machine goes down, the entire production plan shifts. That is a real operational risk that must be weighed against the quality and capability benefits.
Consider the programming complexity. A boring mill or a large grinder requires different programming skills than a standard VMC. The toolpaths are different, the workholding logic is different, and the setup verification process is different. If the current programming team has no experience with the machine class, the learning curve will be steep.
Consider the tooling investment. Specialist machines often require larger, more expensive tooling. Boring bars, large face mills, and specialty grinding wheels do not come cheap. The tooling budget for a specialist machine can be substantial, and it must be factored into the total cost of ownership.
So the right question is not whether the machine sounds impressive. The right question is whether the machine removes the dominant weekly friction the shop actually lives with. If setup compromise disappears, if handling becomes more stable, if the work finally fits the process instead of fighting it, then the specialist direction may be right.
If the purchase mainly adds a stronger story to tell visitors while leaving the real bottleneck only partly solved, then the plant is shopping for symbolism. This is one of the cleanest tests for brands like Kuraki, Chevalier, and similar specialists. Ignore what they symbolize. Ask what weekly pain disappears if the shop owns that class correctly.
Gate 10: Know When to Pause Instead of Forcing the Shortlist
There are times when the best procurement move is to slow down. Pause the purchase if the part family is still vague, if the plant cannot describe the handling model honestly, if service support is uncertain, or if the machine class is being justified mainly by brand prestige. Pause again if the conversation keeps widening into a broader plant-investment question that one specialist badge cannot answer by itself.
That is the moment to step back and revisit what makes industrial CNC equipment worth the investment instead of forcing a specialist-brand decision to do the work of a full capital review. If the discussion is expanding into a bigger plant plan, the Pandaxis product catalog can help reframe the conversation around machinery categories and workflow outcomes instead of isolated names.
Pausing is not indecision. Pausing is what disciplined buyers do when the evidence has not caught up with the reputation. A specialist machine is a long-term commitment. It occupies floor space, consumes capital, and shapes production strategy for years. Buying it a month earlier to satisfy a schedule is rarely worth the risk of buying the wrong machine class or the wrong support model.
How Specialist Brands Should Actually Be Evaluated
Chevalier, Kuraki, and other specialist industrial brands should be evaluated only after the plant has cleared the procurement gates in order. First prove that the bottleneck is truly specialist. Then prove the correct machine family. Then prove the plant is ready for the ownership model. Then prove service reality supports the decision. Then compare each candidate against the same buying sheet, and make sure the machine removes friction rather than merely adding prestige.
Once those gates are cleared, the brand comparison becomes much easier and much more honest. The right specialist brand is not the one with the strongest abstract reputation. It is the one attached to the right machine family, with support you can actually use, for the exact process burden your plant is carrying now.
The evaluation sequence works because it forces the conversation back to physical production realities. Parts have size, weight, and geometry. Machines have envelopes, rigidity, and accuracy. Plants have handling systems, maintenance teams, and service geographies. When those facts are aligned, the brand decision becomes straightforward. When they are not aligned, no reputation can save the purchase.
For shops that are still defining the machine family, reviewing machinery categories side by side can help clarify the options. The goal is to match the machine class to the work, then match the specific machine to the plant. That sequence produces better decisions than starting with a name and working backward to justify it.