Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
When three suppliers all quote the same drawing, the prices are close, the lead times sound similar, and every sales contact expresses confidence. The differences only start to appear when you push past the surface. One supplier asks about edge condition and material lot variation. Another gives vague answers about inspection. A third can produce a sample but cannot explain how repeat orders will stay stable after the first run. At that point, you are no longer comparing service offers. You are comparing how much risk each supplier will remove and how much risk will remain inside your own team.
That is the correct way to approach outsourced cutting. It is not only a unit-price decision. It is a supplier-risk decision.
The strongest supplier is rarely the one that sounds most effortless in the first email. It is usually the one that makes the job’s weak points visible early. That supplier asks where the tolerance really matters, what surface or edge condition is acceptable, whether you expect prototype flexibility or repeat-order stability, and where the schedule can fail if information remains loose. Buyers sometimes misread that as hesitation. In practice, it is often the clearest sign that the supplier understands what responsibility actually means.
Outsourcing Works Only If The Process Burden Really Leaves Your Team
The hidden purpose of using an outside cutting supplier is not just to borrow machine time. It is to transfer burden. You want the supplier to absorb setup effort, machine ownership, process knowledge, at least part of the quality-control load, and a meaningful share of schedule risk.
If that transfer does not happen, you have not really outsourced the process. You have only rented access to somebody else’s machine.
This distinction matters because many purchasing mistakes start here. A buyer assumes outsourcing automatically reduces complexity. It does not. Complexity only leaves your organization when the supplier has the discipline and technical judgment to control the job without constant rescue from your side.
If you still have to explain every edge expectation repeatedly, chase every revision detail manually, clarify every tolerance in panic mode, and monitor every shipment as if no process transfer ever occurred, then the supplier is not carrying enough of the burden to justify the service relationship fully.
Capability Means The Supplier Understands The Work, Not Just The Equipment
One of the most common sourcing errors is confusing machine ownership with real capability. A supplier may own a suitable cutter and still be a weak fit for your part. Real capability shows up when the supplier can explain how the work will behave in production, not just which machine will touch it.
Capability becomes visible when the supplier can discuss how similar parts are normally processed, how the material is controlled, what edge condition is realistic, which dimensions matter most, how inspection will be handled, and what variables are most likely to affect repeatability. That is the difference between a supplier who can make one acceptable part and a supplier who can keep the job stable across repeated orders.
Listen carefully to the language a supplier uses. Strong suppliers speak in process terms. They discuss material behavior, fixture or handling concerns, the likely pressure points in the drawing, and the quality checks that will matter. Weak suppliers hide behind machine names and generic assurance.
Strong Suppliers Usually Talk About Failure Modes Early
One of the best signs of real technical strength is that the supplier can name where the job is likely to fail before it fails. That might mean explaining where the edge may vary, where tolerance stack-up matters most, where the material may behave differently from lot to lot, or where the print is still ambiguous enough to create a dispute later.
This is valuable because it protects you twice. First, it reduces avoidable misunderstanding before the order is placed. Second, it reveals whether the supplier has real process judgment or only sample-making confidence.
Competent suppliers do not build trust by acting as if every drawing is effortless. They build trust by showing that the risky areas are already visible to them. If a supplier never pushes back, never clarifies, and never marks the weak points, ask whether the supplier truly understands the work or is simply trying to keep the quotation moving.
Capacity Is Mostly About Queue Truth, Not Installed Equipment
Capacity is one of the easiest claims to misunderstand. A supplier may have enough machines and enough stated throughput to look comfortable on paper. The more useful question is whether that capacity is genuinely available for your order without destabilizing the queue.
That is why capacity should be treated less as a machine-count question and more as a queue-truth question. Ask whether the quoted lead time is normal or best-case, whether any outside processes are involved before shipment, what happens when a rush order lands during a full week, how the supplier communicates schedule risk when priorities shift, and whether the supplier quotes conservatively enough that normal performance matches the promise.
Installed capacity and usable capacity are not the same thing. A supplier can own impressive equipment and still be unreliable if scheduling is optimistic, subcontracting is opaque, or queue behavior changes every time demand rises. In real sourcing, capacity becomes valuable only when it is believable.
Lead Time Is Strongest When The Supplier Can Explain The Path Behind It
A promised date means much more when the supplier can explain how the job moves from file receipt to shipment. That path does not need to be theatrical or over-documented. It just needs to show that the supplier has a controlled sequence rather than a hopeful estimate.
A believable lead time usually reflects some awareness of file review and clarification, programming or setup needs, machine scheduling, inspection checkpoints, secondary processing if any, and packing or dispatch. If the supplier can describe that path clearly, you learn something valuable: the quoted date is connected to a real process. If the supplier can only repeat the date without describing how the work will get there, you are being asked to trust optimism instead of planning.
That difference is especially important when the service is being used for repeat jobs rather than one-off samples. Repeat sourcing depends less on how quickly a supplier can respond once and more on how predictably the supplier can keep the path stable over time.
Quality Is Evidence, Not Enthusiasm
Quality claims are cheap. Evidence is what matters.
When evaluating cutting services, look for proof that the supplier has a repeatable method for controlling output. That proof does not have to be presented in flashy marketing language. It can appear through disciplined quoting questions, consistent drawing review, sample feedback, inspection records, dimensional logic, or a clearly described acceptance process.
The core question is simple: how does this supplier know the part is correct before it ships?
That question matters because many supplier relationships fail in the same way. The sample looks acceptable, the quote is competitive, and the supplier sounds cooperative. Then repeat orders drift because no one defined how the process would stay under control after the first run. Quality was assumed rather than structured.
Pay attention to whether the supplier can show a quality method, not just a quality attitude. Enthusiasm, speed, and friendliness all help the relationship. None of them replace evidence.
Quality Usually Fails Before Final Inspection
Buyers often talk about quality as though it starts at final inspection. In outsourced cutting work, quality usually starts much earlier. It begins with whether the part definition is strong enough for the supplier to make the same decision every time.
Real quality depends on stable revision control, clear material specification, visible-surface and edge expectations, critical dimensions being identified, and both sides agreeing what counts as acceptable. Strong suppliers often ask more questions before quoting seriously. That is not hesitation. It is usually evidence that they are trying to prevent a later argument.
This is a critical shift in mindset. Quality is not what happens after the cut is finished. Quality is what happens when the supplier is able to interpret the job the same way every time it is run. If interpretation keeps changing, final inspection becomes a weak safety net instead of a stable control system. The best suppliers often feel more demanding early in the relationship because they are trying to stabilize interpretation before production starts.
Communication Discipline Often Predicts Repeat-Order Stability
Communication is not a soft issue in outsourced cutting. It is a process-control issue.
The right supplier communicates in a way that lowers uncertainty. That usually means asking clarifying questions early, confirming key assumptions before cutting, flagging changes quickly, and escalating schedule or quality risk before it becomes a shipment problem.
Poor communication creates expensive ambiguity. You think the edge can be rougher than the supplier thinks. The supplier assumes material substitution is acceptable when it is not. A revision is applied in one place but not another. A lead-time risk is discovered only after the planned ship window has passed. None of these failures need bad intent. They only require weak communication discipline.
Evaluate how a supplier communicates during quoting and sampling, not just after the order is live. The quoting stage is often the best preview of future operating behavior. If the supplier is vague now, it is unlikely to become disciplined later under schedule pressure.
Good RFQs Expose Weak Suppliers Quickly
Many cutting-service sourcing problems begin with a weak RFQ. If you send an incomplete drawing package, weak suppliers are free to make convenient assumptions and strong suppliers are forced to guess.
A useful RFQ should make the following clear wherever possible: current revision, material specification, tolerance-sensitive areas, edge-quality expectations, visible-surface concerns, first-article expectations, and whether repeat production is likely. When that input package is disciplined, the quotation becomes far more useful as a selection tool.
This is one reason sourcing results vary so much even when the supplier list is good. The RFQ itself determines how much disciplined comparison is possible. A weak RFQ creates soft promises, soft assumptions, and soft accountability. A disciplined RFQ exposes whether the supplier can reason through the job with enough seriousness to support stable production. In that sense, a strong RFQ is not only a buyer document. It is a filter.
A Supplier Comparison Table Works Best When It Demands Evidence, Not Sales Language
When several suppliers appear similar, a simple evidence-based comparison table is usually more useful than a long internal debate.
| What you need to judge | Strong evidence from the supplier | Weak signal that should not be over-trusted |
|---|---|---|
| Capability | Clear explanation of similar work, known risks, material control, and inspection approach | General claims about owning the right machine |
| Capacity | Realistic lead-time logic, queue transparency, and explanation of schedule pressure | A confident date with no path behind it |
| Quality | Defined acceptance criteria, revision discipline, and repeatability logic | “We always check everything” without specifics |
| Communication | Clarifies assumptions and flags missing information early | Prices around ambiguity without resolving it |
| Repeat-order stability | Retained job knowledge, documented revisions, and consistent control points | A good sample with no explanation of how repetition is controlled |
This kind of table matters because it shifts the discussion from impression to evidence. Suppliers should not win by sounding smooth. They should win by making the work more knowable.
Repeat Orders Are Where Supplier Quality Becomes Honest
A strong sample does not prove a strong supply relationship. Many suppliers can make one acceptable part under focused attention. The real test is whether the next lot, the next revision, and the next urgent reorder remain stable.
Ask how learning is retained. Are program revisions documented? Are tooling decisions remembered? Are inspection notes retained? Does each repeat order run like a known job instead of a fresh improvisation? If the answer is unclear, the supplier may still be usable for occasional outsourcing, but not for controlled recurring work.
Repeat-order stability matters because it reveals whether the supplier has a memory system around the job. A supplier that re-discovers the work every time may still get acceptable output occasionally, but it will consume more of your oversight and create more schedule and quality volatility than a supplier that has truly retained the learning. For recurring outsourced work, retained learning is one of the most valuable commercial assets in the relationship.
A Practical Five-Pass Review Keeps Supplier Comparison Honest
When several suppliers look acceptable on the surface, a structured review helps separate real strength from polished sales language. One useful way to do that is to run five passes instead of trying to judge everything at once.
First pass: technical fit. Can the supplier explain how the material, geometry, and edge requirement will actually be handled?
Second pass: failure awareness. Can the supplier identify where the job is likely to go wrong if the definition stays loose?
Third pass: queue realism. Does the lead time reflect normal scheduling behavior rather than best-case optimism?
Fourth pass: quality evidence. Can the supplier describe how it confirms the part is right before shipment?
Fifth pass: communication behavior. Does the supplier lower uncertainty early or simply reassure without structure?
This five-pass method works because it prevents one strong trait from hiding several weak ones. A technically capable supplier with poor queue discipline may still be a schedule problem. A fast supplier with weak quality evidence may still be a cost problem. A cooperative supplier with unclear technical understanding may still leave most of the process burden on you.
Capability, Capacity, And Quality Should Agree With Each Other
The safest suppliers are usually the ones whose capability, capacity, and quality story all point in the same direction. If one of those pillars looks much stronger than the others, slow down.
A supplier may sound technically strong but quote lead times that do not match realistic queue behavior. A supplier may promise fast delivery but remain vague about inspection and acceptance criteria. A supplier may have solid quality language but show little real understanding of the material or part family.
These mismatches matter because supplier risk often hides in inconsistency. A strong outsourcing partner usually presents a coherent story. The process understanding, schedule promise, and quality control all reinforce each other. When they do not, assume that one part of the commercial case is being overstated.
When Outsourcing Stops Being The Best Long-Term Answer
Sometimes the most useful outcome of a supplier comparison is the realization that you are trying to outsource a burden that no outside partner can absorb cleanly enough. That usually happens when the work is frequent, schedule-sensitive, revision-heavy, or strategically important enough that you keep being pulled back into process control anyway.
In those situations, supplier comparison can become a sign that the business should also review an equipment strategy. If outsourced cutting still leaves too much schedule risk, too much clarification load, or too much quality exposure inside your team, then the real question may no longer be which supplier is best. The real question may be whether internal capability is becoming commercially justified.
For buyers who are already moving in that direction, the Pandaxis machinery catalog is the right next reference for comparing machine categories by production fit rather than by generic feature lists.
The strongest outsourced cutting supplier is not the one that says yes fastest. It is the one that removes the most risk while keeping the process visible and controlled. Buyers who compare capability, capacity, and quality in that order usually make better sourcing decisions than buyers who start with price and hope the rest will sort itself out later.
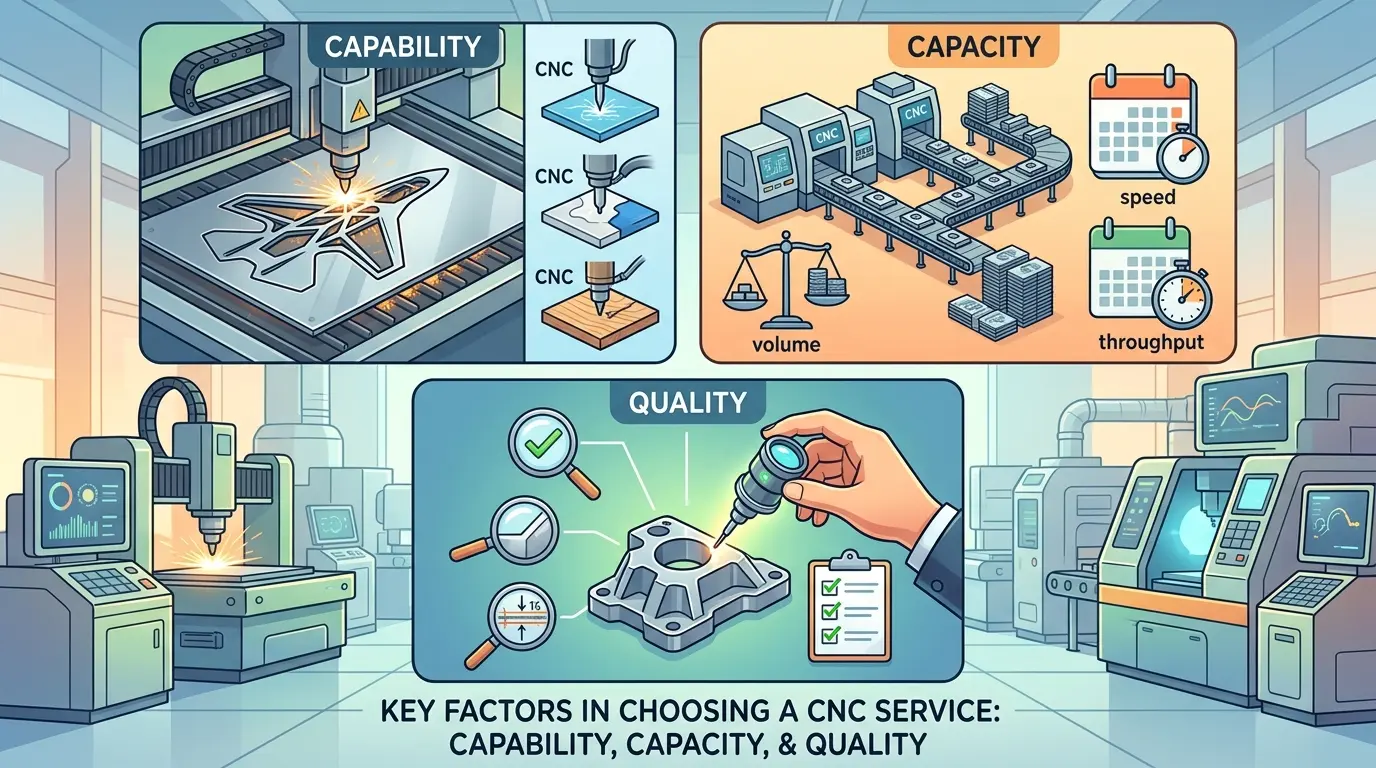
Comparing Capability, Capacity, And Quality
Capability means the supplier truly understands the process and part family. Capacity means the quoted lead time is based on real queue behavior, not optimistic quoting. Quality means the supplier can define, control, and repeat the work without relying on constant buyer intervention.
That is the practical answer to the title. Compare suppliers at those three levels together, because weakness in any one of them makes the relationship more expensive later. The better way to remember the comparison is simple: capability answers whether the supplier understands the work, capacity answers whether the supplier can absorb it reliably, and quality answers whether the result will stay stable without constant buyer rescue. When you evaluate all three through evidence instead of through confidence alone, supplier selection becomes far more durable.