Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
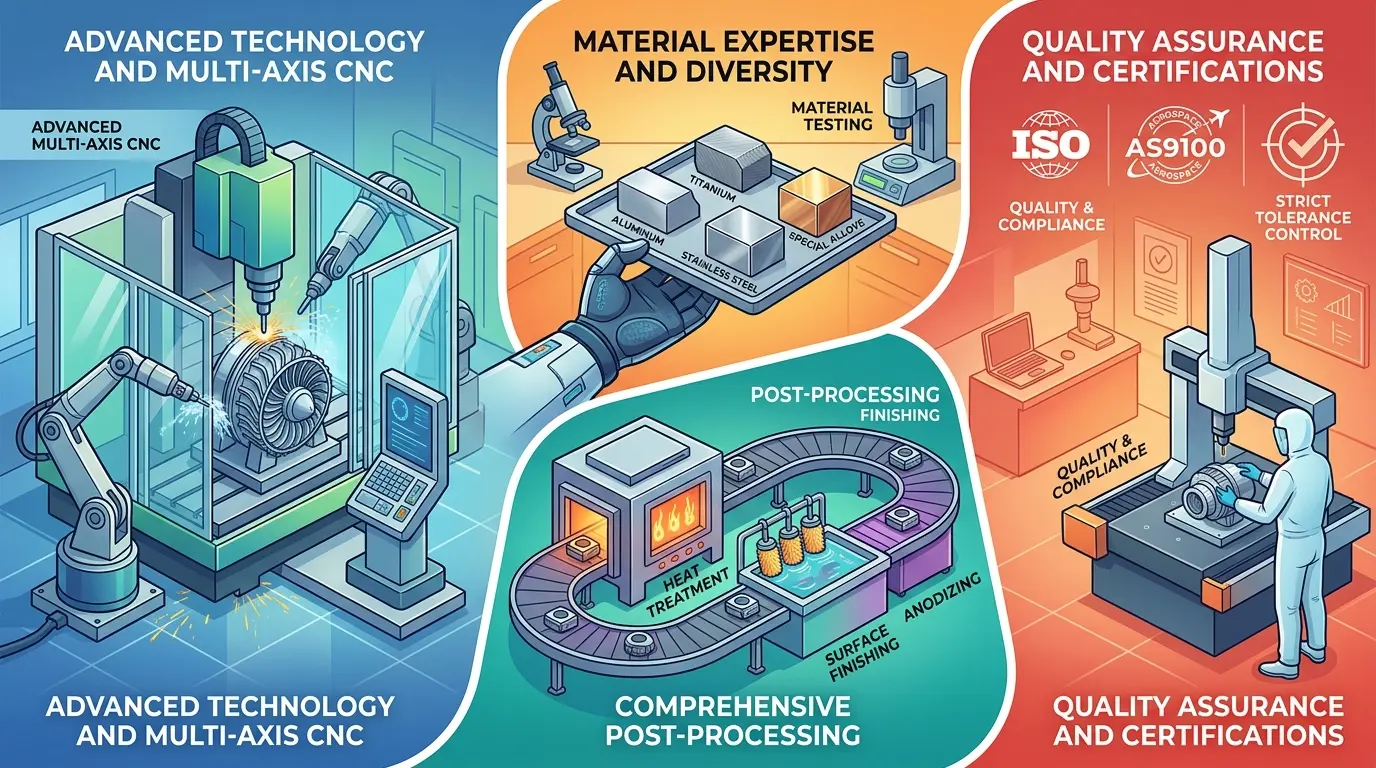
Precision failures in CNC manufacturing rarely originate at the spindle; they emerge at the handoffs between quoting, process planning, setup transfer, secondary treatment, and repeat releases. This article pushes buyers past machine counts and final CMM reports to audit where a supplier actually loses dimensional intent across the entire production route. For procurement teams and engineers qualifying sources, the decisive question is not the tightest tolerance ever held, but whether the shop controls datum location, in-process measurement timing, post-machining distortion, and documented knowledge transfer. Evaluate the continuity system, not the brochure, before committing your part family.
Where Precision Is Actually Lost in a CNC Job Shop
Most precision problems in CNC manufacturing do not start at the machine tool. They start at the handoffs: between quotation and process planning, between first operation and second operation, between machining and heat treatment, between one order and the repeat order six months later. A shop can own excellent five-axis machines, a climate-controlled inspection room, and a quality manual that reads well, yet still ship parts that drift out of tolerance because no one controlled the continuity of the part’s journey.
That is why the phrase “precision components manufacturer” should trigger a different question than “what is the tightest tolerance you have ever held?” Holding a tight number once, on a favorable part, under ideal conditions, proves very little about how a supplier will perform on your part family across multiple releases. The more useful question is: where can this supplier lose the part between RFQ and shipment, and what systems exist to stop that from happening?
Precision in production is a continuity problem. The strongest manufacturer is usually the one that reduces loss points between stages, not the one with the most impressive brochure.
Define the Precision Burden of Your Part Family Before Comparing Suppliers
Not all precision work behaves the same way. A supplier that performs well on prismatic aluminum housings with a few tight bores may struggle with thin-wall stainless components that move during machining. A shop that excels at turned parts with concentricity requirements may not have the fixturing depth for large plate work with critical flatness. Cosmetic surfaces, sealing surfaces, sliding fits, and fatigue-sensitive features all impose different demands on the process.
Before evaluating any supplier, write down what actually makes your parts demanding. Useful signals include:
- Which datum relationships truly matter in assembly or function, not just which dimensions carry a tolerance block.
- Which dimensions are safety-critical, fit-critical, or leak-critical, and what happens if they drift.
- Whether the material is stable or prone to movement during machining, heat treatment, or aging.
- Whether surfaces are cosmetic, sealing, sliding, or fatigue-sensitive, and how surface finish interacts with function.
- Which post-machining processes can disturb dimension or finish, such as anodizing, plating, heat treatment, or grinding.
- How often revisions or repeat releases are likely, and whether the part will be reordered with the same drawing or with modifications.
This exercise turns the conversation away from generic CNC capacity and toward the real burden the supplier must carry. Without it, buyers often qualify the wrong strengths. A supplier with excellent deep-hole drilling capability is irrelevant if your part family is shallow pockets and tight face-milling flatness. A shop with a five-axis machine is not automatically better than a well-organized three-axis shop if your parts are prismatic and the five-axis machine is operated by someone who rarely runs your material.
The Quotation Stage Is the First Precision Audit
Strong precision manufacturers usually show their quality level before they cut any metal. They ask about datum intent, tolerance interactions, surface function, inspection expectations, and what is actually critical versus simply dimensioned. They flag missing information, challenge vague callouts, and expose risk early. A good quoting engineer will ask whether the 0.01 mm bore tolerance is for a bearing fit or a clearance hole, because the answer changes the entire process route.
Weak suppliers often do the opposite. They respond quickly, say yes to everything, and leave interpretation gaps open until manufacturing starts. At that point the hidden cost appears as delay, rework, argument, or excessive buyer oversight. The quote that looked competitive at the start becomes expensive by the time the first article is approved, because the supplier did not understand what it was committing to.
That is why the quotation stage is not just a commercial step. It is the first precision-control audit. If the supplier does not force important ambiguity into the open before accepting the job, the shop may be relying on improvisation rather than discipline. Ask your suppliers what questions they have about the drawing. A supplier with no questions is either familiar with your exact part family or not thinking hard enough about it.
Process Planning Reveals More Than Machine Count
Buyers are often distracted by visible assets: how many machines, what brands, how large the plant, how polished the inspection room looks. Those things matter, but they do not tell you how a precision part will actually travel through the process. A shop with twenty CNC machines can still route your part poorly if the process planner does not understand where the risk actually sits.
The better question is whether the supplier can explain the route with technical clarity. Ask what features are treated as the highest-risk operations. Ask where the first true datum is created. Ask when tool wear becomes a concern and how the shop compensates for it. Ask which steps are designed to stabilize the part and which steps simply remove stock. Ask how the supplier handles the difference between roughing and finishing, and whether those operations happen on the same machine or on different machines with separate setups.
When the process explanation is coherent, the supplier is usually stronger. When the explanation stays generic, the shop may own good equipment without having a reliable plan for your part family. A supplier that can say “we rough this pocket, stress-relieve, then finish the bore in a separate setup to control the bore-to-face relationship” understands something about your part. A supplier that says “we will just hold it on the machine” may be relying on hope.
Location Strategy Determines Whether Features Stay in the Right Relationship
Many precision problems are really location problems wearing a measurement disguise. The feature may be in tolerance by itself, yet wrong relative to the datum structure that matters in assembly. A bore can be perfectly round and perfectly sized, but if it sits 0.05 mm off its true position relative to the mounting face, the part fails in the assembly even though the bore itself is good.
That is why buyers should listen carefully for how the manufacturer thinks about workholding and setup transfer. Ask how the supplier keeps location stable when the part requires multiple operations. Ask how it handles thin walls, awkward clamping, or features that become hard to reference after the first cut. Ask whether the setup logic is repeatable enough for future orders or dependent on one experienced person remembering how the first batch was rescued.
Good precision manufacturers usually talk clearly about location strategy because they know that dimensional integrity is built from how the part is held and re-held, not only from how it is measured at the end. They will explain how they establish the first datum, how they transfer that datum to the next operation, and what they do when the part geometry makes the datum inaccessible after the first cut. They will also explain how they handle the tradeoff between clamping force and part deflection, especially on thin-wall or flexible components.
Consider a part that requires machining on both faces with a critical hole pattern relative to the back face. The supplier must decide whether to machine the back face first, then use it as the locating surface for the front face operations, or whether to machine the front face features first and then reference them from the back. Each choice carries different risks. The first approach risks the front face features being slightly off if the part shifts between setups. The second approach risks the back face datum being disturbed by the front face clamping. A supplier that can articulate this tradeoff and explain its chosen strategy is managing location deliberately.
In-Process Measurement Matters More Than Final Inspection
Inspection capability matters, but buyers often evaluate it too shallowly. A coordinate measuring machine or a well-equipped inspection room is not proof that the process is under control. It may only prove that the supplier can detect failure after the expensive work has already happened. A CMM report on a finished part tells you whether the part is good or bad. It does not tell you whether the next part in the batch will be good, especially if the process is drifting due to tool wear, heat buildup, or stock variation.
The stronger question is when measurement enters the process. Precision manufacturers worth trusting usually know which features need early confirmation, which dimensions should be watched during the run, and which results trigger correction before the batch drifts. They use in-process gauging, first-article checks at critical operations, and statistical process control where the volume justifies it.
This matters especially for features influenced by tool wear, stock variation, heat input, or multi-step setups. A bore that is machined with a worn tool will drift progressively across the batch. If the supplier only measures the first and last part, the middle of the batch may be out of tolerance without anyone knowing. If the supplier measures at regular intervals and adjusts the tool offset when the dimension starts to move, the batch stays in control.
If measurement is separated from correction, then inspection becomes sorting rather than control. The buyer still receives data, but not necessarily stable production. Ask your supplier how often they check critical features during the run, what triggers a correction, and how they document the adjustment. A supplier that can show you a control chart or a log of in-process adjustments is managing precision actively. A supplier that only shows you a final inspection report is hoping the process stayed stable on its own.
Secondary Processing Is Where Precision Often Dies
Many parts lose value after the main machining step. Heat treatment can move geometry, sometimes by more than the machining tolerance itself. Anodizing and plating can change fit or finish expectations, and the growth from a hard coat anodize layer can close a clearance hole that was perfectly sized before treatment. Grinding can recover geometry or expose that the upstream route was never stable. Cleaning, deburring, marking, handling, and packaging can all damage the part if no one is clearly responsible for protection.
That is why buyers should ask where the control boundary sits once the part leaves core machining. Which processes are internal? Which are outsourced? How are critical surfaces protected during handling and transport? How are dimensional risks checked before and after treatment? What documentation follows the part through external operations when traceability matters?
Consider a hardened and ground component. The machining shop may produce the part to a pre-heat-treatment dimension, then send it out for hardening, then receive it back for grinding. The heat treater may cause distortion that the grinder must remove. If the machining shop left too little grinding stock, the part may not clean up. If it left too much, the grinding operation may introduce its own heat damage or residual stress. The supplier must coordinate these steps, not just hand the part off and hope.
For anodized aluminum parts, the anodize layer grows both outward and inward from the original surface. A hole that is specified at 6.00 mm after anodize must be machined undersized before treatment, and the supplier must know the anodize growth rate for the specific alloy and coating thickness. If the supplier treats anodizing as an external issue and does not account for it in the machining dimensions, the finished part will be wrong even though every machining operation was correct.
If the supplier is precise only inside the machine envelope and vague once the part moves outside it, then the precision story is incomplete. For many components, the handoff to secondary processing is the real test of supplier maturity.
Repeat Orders Reveal Whether the Shop Stores Knowledge or Relies on Memory
One of the most important differences between an impressive first-order supplier and a reliable long-term supplier is whether process knowledge survives once attention moves elsewhere. That is why repeat work reveals more than first articles do. A first article can be rescued by an experienced machinist who remembers how to handle a difficult setup. A repeat order, launched months later with different personnel on shift, requires documented process knowledge.
Ask how the shop preserves lessons from the first run. Are setup notes retained? Are critical checkpoints formalized? Is the inspection logic carried forward? Are drawing revisions tied cleanly to the production record? Can the supplier relaunch the part months later without rediscovering the same risk points?
Precision suppliers become commercially powerful when repeat orders become calmer rather than more fragile. If the second or third order depends on memory, heroics, or repeated buyer re-explanation, the manufacturer may be producing acceptable parts without actually owning the process. The first order may have been a triumph of individual effort. The repeat order will expose whether the process was actually under control or just lucky.
Ask the supplier what documentation exists for a part you are considering. If they can produce a setup sheet, an inspection plan, and a list of known risk points from a previous run, they are managing knowledge. If they need to start from scratch every time, you are paying for their learning curve on every order.
Engineering Response Culture Is a Stronger Signal Than Sales Confidence
Buyers often overvalue confidence and undervalue technical honesty. In precision work, the safer supplier is usually not the one that sounds easiest. It is the one that identifies what could go wrong before production starts and makes that risk visible while there is still time to adjust. A supplier that says “we can hold that” without asking what the feature does is not being helpful. It is deferring the problem to the shop floor, where it will surface as rework or a rejected batch.
This can show up in small but important ways:
- The supplier asks what the part must do, not only what the print says. It wants to know if a tight tolerance is for a bearing fit, a seal surface, or a cosmetic requirement that could be relaxed.
- It distinguishes between cosmetic and functional surfaces, and questions whether a fine finish on a hidden face is worth the cost.
- It identifies stacked tolerances that may not be manufacturable at the quoted cost, and proposes alternatives or asks for clarification.
- It questions whether post-processing could disturb the controlled features, and plans the machining route accordingly.
- It clarifies whether inspection scope matches actual risk, rather than quoting a full CMM inspection on every dimension when only a few are critical.
That behavior is valuable because it proves the team is managing precision as an engineering problem rather than only a purchasing transaction. A supplier that challenges your drawing is not being difficult. It is protecting you from a part that cannot be made as specified, or that will cost far more than necessary because the tolerance is tighter than function requires.
Commercial Clarity Usually Mirrors Technical Discipline
The quotation itself can reveal a great deal. If scope is vague, assumptions are hidden, finishing responsibility is unclear, or inspection expectations are left implied, the supplier is already behaving loosely in the same areas where precision work later gets damaged. A quotation that does not specify what is included, what is assumed, and what will change the price is a quotation that will generate disputes later.
That is why buyers should still compare quotations line by line rather than reducing the decision to unit price. Quoting discipline is part of manufacturing discipline. A supplier that cannot separate what is included, what is assumed, and what changes price later is harder to trust on controlled technical work. Look for quotations that specify material grade, heat treatment requirements, surface finish expectations, inspection scope, and packaging. Look for quotations that flag assumptions about stock size, batch quantity, or drawing interpretation.
For teams still deciding whether the job truly requires a precision-oriented source or a broader machining source, it also helps to review when precision machining really differs from general machining and how to screen a CNC machining service for custom parts. Those comparisons are useful because they help buyers separate genuine precision burdens from inflated wording. A part with one tight bore and loose everything else may not need a precision specialist. A part with multiple critical datum relationships, thin walls, and post-machining treatment almost certainly does.
Audit the First Order as a Control System, Not Just as a Shipment
When the first order is finally launched, buyers should resist the temptation to judge only the parts in the box. The stronger question is whether the supplier behaved like a controlled system from start to finish. The parts may all pass inspection, but if the process was chaotic and the supplier relied on last-minute heroics, the repeat order will not go as smoothly.
Did questions arrive early, during quotation and process planning, or did they surface only when the parts were already in production? Did the process plan reflect the true risk in the drawing, or was it a generic route that happened to work? Did in-process control show up before final inspection, or was the first indication of trouble a rejected part at the CMM? Were secondary operations handled with discipline, or did the supplier treat heat treatment and anodizing as someone else’s problem? Did paperwork, revision control, and communication stay aligned, or did the buyer have to chase down updates? Did the supplier make the hard parts visible rather than simply reassuring the buyer?
If the answer is yes, the relationship is probably becoming safer. If the answer is no, the first order may still pass while the long-term risk remains high. A first order that succeeds through individual effort is not a controlled process. It is a warning that the supplier’s system depends on the right person being on shift.
What Actually Matters Is the Ability to Preserve Intent Across the Whole Route
The best CNC precision components manufacturers are not the ones with the loudest capability claims. They are the ones that can preserve engineering intent from the first technical conversation to the repeat release months later. They control interpretation, location, measurement timing, secondary-process risk, documentation, and learning transfer.
That is the real standard buyers should use. Precision is not a machine label and not a marketing phrase. It is the supplier’s ability to keep the part from losing meaning as it crosses every handoff in the production route. A shop that asks the right questions at quotation, plans the process around the true risk, holds location across setups, measures at the right time, manages secondary processing, documents what it learned, and carries that knowledge into the next order is a precision manufacturer. A shop that only owns precision equipment is not.
When you evaluate suppliers, look past the machine list and the inspection room. Ask how the part will travel through the shop, where the risk sits, and what happens when something drifts. The answers will tell you more about precision capability than any tolerance claim ever will.