Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
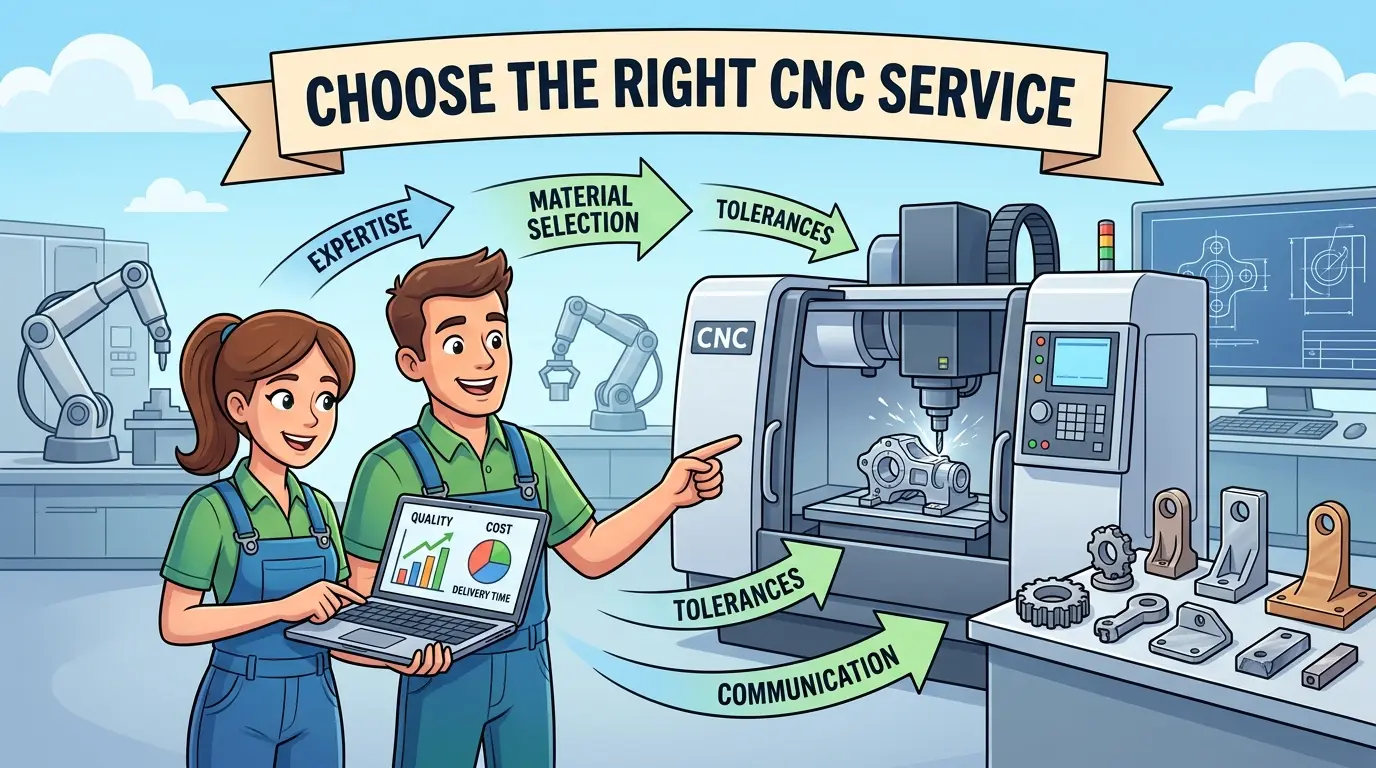
Custom CNC sourcing fails long before any tool touches stock when buyers treat the quote as a commodity purchase instead of a process-matching decision. Your part definition, RFQ discipline, and supplier screening determine whether first-article risk, drawing interpretation, and fixture design become manageable costs or hidden liabilities. This article walks through the practical evaluation sequence: defining geometry in process terms, building an unambiguous package, testing DFM behavior, comparing quotes by scope rather than price, and using pilot orders to expose real communication and quality habits. Match the supplier’s natural workflow to your part family, not to industry labels or confident delivery promises.
Why Custom CNC Sourcing Fails Before the First Chip Is Cut
Buying CNC machining capacity for custom parts is fundamentally different from purchasing standard production time. You are not renting spindle hours. You are selecting a partner who must interpret your geometry, tolerances, material callouts, finish expectations, and delivery risk—often from incomplete or imperfect information—and convert that into acceptable parts.
This distinction matters because the cheapest quote or the most confident delivery promise frequently becomes the most expensive outcome. Custom work carries first-article risk, drawing interpretation risk, fixture design risk, and the risk that the supplier’s optimized workflow simply does not match your part’s requirements. A weak supplier hides these uncertainties until inspection failures or missed dates force the real conversation. A strong supplier surfaces them early, when decisions can still be made economically.
Define the Part as a Manufacturing Problem, Not Just a Product
The quality of your supplier decision depends almost entirely on the quality of the part definition you provide. Vague specifications force every quoting engineer to make private assumptions, and you end up comparing prices that do not reflect the same scope of work.
Start with function. Which dimensions actually matter in assembly or performance? Which surfaces are purely cosmetic? Which tolerances are critical to fit, and which are legacy numbers that nobody has challenged in years? A custom part needs the supplier to understand what cannot move and what can.
Equally important is defining the geometry class. A prismatic milled plate, a turned shaft, a multi-axis housing, and a thin cosmetic bezel all qualify as custom machined parts, but they do not belong with the same ideal supplier. A shop optimized for high-mix plate work may struggle with a deep-cavity housing that requires specialized tooling reach. A turning specialist may lack the fixturing experience for thin-wall rectangular parts. Good sourcing begins when you can describe the part in process terms—milling, turning, multi-axis, plastics, secondary operations—rather than only in product terms.
Build an RFQ Package That Prevents False Confidence
A strong RFQ package does more than attach a drawing. It gives the supplier enough context to quote and plan intelligently. That means revision-controlled drawings, usable 3D models that agree with the prints, unambiguous material callouts, quantity scenarios, and explicit notes on finish, burr expectations, and inspection requirements.
When you provide a model, verify it matches the drawing. When you provide a drawing, confirm the datum strategy supports how the part will actually be inspected and assembled. When the part is new, state whether you need a prototype mindset, a bridge-to-production approach, or repeat supply. These distinctions change how the supplier plans tooling, programming, and inspection.
Ambiguity is expensive. Threads with unclear standards, mixed units, contradictory notes, undefined cosmetic surfaces, and missing finish expectations force the supplier to assume. Every assumption becomes a future schedule negotiation or quality dispute. A disciplined RFQ package is not paperwork overhead—it is the cheapest insurance you can buy.
Match the Supplier to the Process Family, Not the Industry Label
Not every capable machining shop is the right partner for your custom parts. Some shops are optimized for repeat production families and run the same geometries for years. Others excel at rescue work, prototypes, and first-article development. Some have deep experience in turned components, others in plate work, others in complex multi-axis parts, plastics, or secondary operations like grinding and EDM.
A supplier can be technically competent and still be the wrong fit if their strongest workflow is elsewhere. Screen against capability fit rather than general reputation. Ask what part families the supplier handles most often. Ask which materials they run regularly—aluminum plate is not the same as hardened tool steel or unfilled plastics. Ask how they approach first articles, fixture creation, revision changes, and secondary processes. Ask how much work is done in-house versus pushed to outside vendors.
The goal is not to find the most versatile supplier in theory. It is to find the supplier whose natural operating rhythm matches the kind of custom work you actually need.
Good Suppliers Raise DFM Concerns Before You Ask
One of the strongest screening signals is how the supplier handles design-for-manufacturing discussion. Strong suppliers do not wait until parts fail to mention concerns. They raise practical issues during quoting: difficult corner radii that force small tools, unrealistic surface finish requirements, unnecessarily tight tolerances that drive inspection cost without helping function, awkward stock choices, or geometry that will require expensive fixturing without adding value.
This is not a sign that the supplier is difficult. It is a sign that they are reading the part like a manufacturer instead of like a quoting machine. The key question is whether the supplier can challenge a drawing usefully. A good partner explains why a change matters in terms of setup time, tool access, inspection risk, or scrap exposure. A weak partner says “no problem” and leaves the unpleasant conversation for after launch, when changes are far more expensive.
Evaluate Quality Through Process Evidence, Not Just Certificates
Certifications matter, but they are only a starting point. A quality system on paper does not guarantee strong custom-part execution. For custom work, the useful evidence is practical: first-article discipline, traceable measurement methods, calibration habits, non-conformance handling, and whether the supplier can speak clearly about how they control process risk.
Ask how first articles are documented. Ask how drawing ambiguity is handled when it is discovered during programming. Ask what happens when a tolerance appears unrealistic after fixture planning or CAM review. Ask how corrective action is communicated when something goes wrong. The goal is to learn whether the supplier surfaces problems early or only after parts fail.
If possible, review sample inspection reports or at least the structure of their documentation. Strong suppliers sound specific. They name the measurement equipment, the datum scheme, and the acceptance criteria. Weak ones sound reassuring without becoming concrete.
Compare Quotes Like an Engineer, Not a Commodity Buyer
A lower quote is not automatically a better quote. It may reflect genuine efficiency, but it may also reflect omitted scope, optimistic assumptions, or a weaker interpretation of inspection and finishing requirements. Custom-part buyers need to compare quotes with engineering discipline.
Break down what is actually included. Is the material really equivalent in grade and condition? Are outside processes such as plating, heat treatment, grinding, or deburring included? Is inspection defined the same way by each supplier—are they measuring the same features with the same methods? Are first-article charges, setup work, and fixture costs clearly separated? How are revision changes handled after the first run?
If one quote is dramatically cheaper, do not assume you found a bargain. Assume there is a difference in interpretation and find it before the purchase order is released. The same discipline applies when comparing equipment quotations line by line: cheap is only useful when scope is truly the same.
Communication Quality Is a Technical Capability
In custom manufacturing, communication is not a soft skill. It is part of process control. Suppliers who ask specific questions early usually save time later. Suppliers who respond vaguely, slowly, or defensively during quoting rarely become clearer once delivery pressure begins.
One useful test is to introduce mild change pressure before award. Ask how they would handle a revision. Ask what happens if material lead time slips. Ask who owns communication if an issue appears after the first article. Strong suppliers have an answer path, not just a promise to “work it out.”
This matters because custom-part projects almost always change. The supplier does not need to be perfect. They need to be understandable under stress.
Read Lead Time as a Chain, Not a Calendar Number
Lead time failures on custom parts rarely come from spindle time alone. Material release, tooling procurement, outside processes, inspection queueing, programming, fixture creation, and internal approvals often dominate the schedule. A serious supplier understands this and can explain the critical path instead of simply naming a confident date.
Ask where the real schedule risks sit. Is the timeline sensitive to material availability? Is there a special fixture that needs design and build time? Does outside processing create the bottleneck? Are certain features likely to require slower proving-out or more inspection time? These questions separate a credible lead time from a sales lead time.
The same logic applies across sourcing regions. Domestic supply may reduce communication friction and shipping risk. Overseas supply may lower piece cost but increase revision and logistics risk. Neither is automatically right. It depends on part value, urgency, and your tolerance for coordination delay.
The Pilot Order Is More Honest Than the Sales Conversation
For meaningful custom work, a pilot order is often more informative than any certificate stack, capability slide, or website gallery. It reveals how the supplier reads drawings, asks questions, handles inspection, packages parts, and communicates when reality does not match the first assumption.
Treat the pilot as an evaluation tool, not just a procurement step. Watch communication timing. Watch report quality. Watch whether uncertainty is exposed early enough to manage. If the supplier hides problems during the pilot, expect worse behavior later when volume rises.
This is also the moment to test fit at the human level. Some buyers want rapid conversation and collaborative decisions. Others want structured documentation first. A strong match includes interface style, not only machining capability.
Define Rework, Model-Drawing Conflicts, and Revision Rules Early
Custom parts often fail not because the supplier is careless, but because intent was never made explicit. A surface finish may be judged visually by one side and functionally by the other. A tolerance may have been copied from an old design without economic logic. A drawing note may be technically legal and still practically misleading.
Discuss rework responsibility before production begins. What happens when the drawing is wrong? What happens when the model and drawing conflict? What happens when a requested revision arrives after tooling or fixtures are already committed? These are not legal side notes. They are central to selecting the right supplier because different shops handle ambiguity in very different ways.
You do not need a hostile contract discussion. You do need clarity on how surprises will be handled when they inevitably appear.
When the Question Shifts Toward Make-Versus-Buy
Sometimes the best machining service is still not the best long-term answer. If recurring spend, queue delay, and revision churn keep rising, the buyer may need to re-evaluate whether some work should move in-house. This is especially true when the parts begin to resemble routable plates, repeated sheet components, or other geometries that fit an owned digital process better than repeated vendor coordination.
This is not a decision to make lightly. In-house machining requires capital, programming skill, maintenance discipline, and floor space. But when vendor management becomes the dominant cost instead of the machining itself, the economics deserve a fresh look. For flat-part production that keeps repeating, the broader question of what makes industrial CNC equipment worth the investment becomes practical, and CNC nesting machines are often the category that changes the economics.
A Practical Supplier Scorecard
Use the scorecard below before awarding meaningful custom work.
| Area | What Good Looks Like |
|---|---|
| Process fit | Supplier regularly handles similar geometry and materials |
| RFQ response | Specific questions, clear assumptions, defined scope |
| DFM behavior | Challenges useful problems early and explains tradeoffs clearly |
| Quality discipline | First-article structure, traceable measurement, documented escalation |
| Communication | Timely, technical, and understandable under ambiguity |
| Commercial clarity | Revisions, tooling, outside processes, and lead-time risks are explicit |
| Pilot performance | Parts, reports, packaging, and issue handling match the promise |
If the supplier is weak in several of these areas, the lower price rarely compensates for the risk.
Clarity Is the Best Predictor of a Good Custom-Part Relationship
Choose a CNC machining service for custom parts by aligning the supplier’s real process strengths with your real part requirements, not by comparing slogans or headline prices. Strong suppliers make uncertainty visible early, document their assumptions, and stay understandable when the job changes.
The best decision comes from disciplined RFQ preparation, careful pilot evaluation, and an honest review of where schedule and quality risk actually sit. In custom manufacturing, clarity is not paperwork overhead. It is the main protection against expensive surprises.