Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
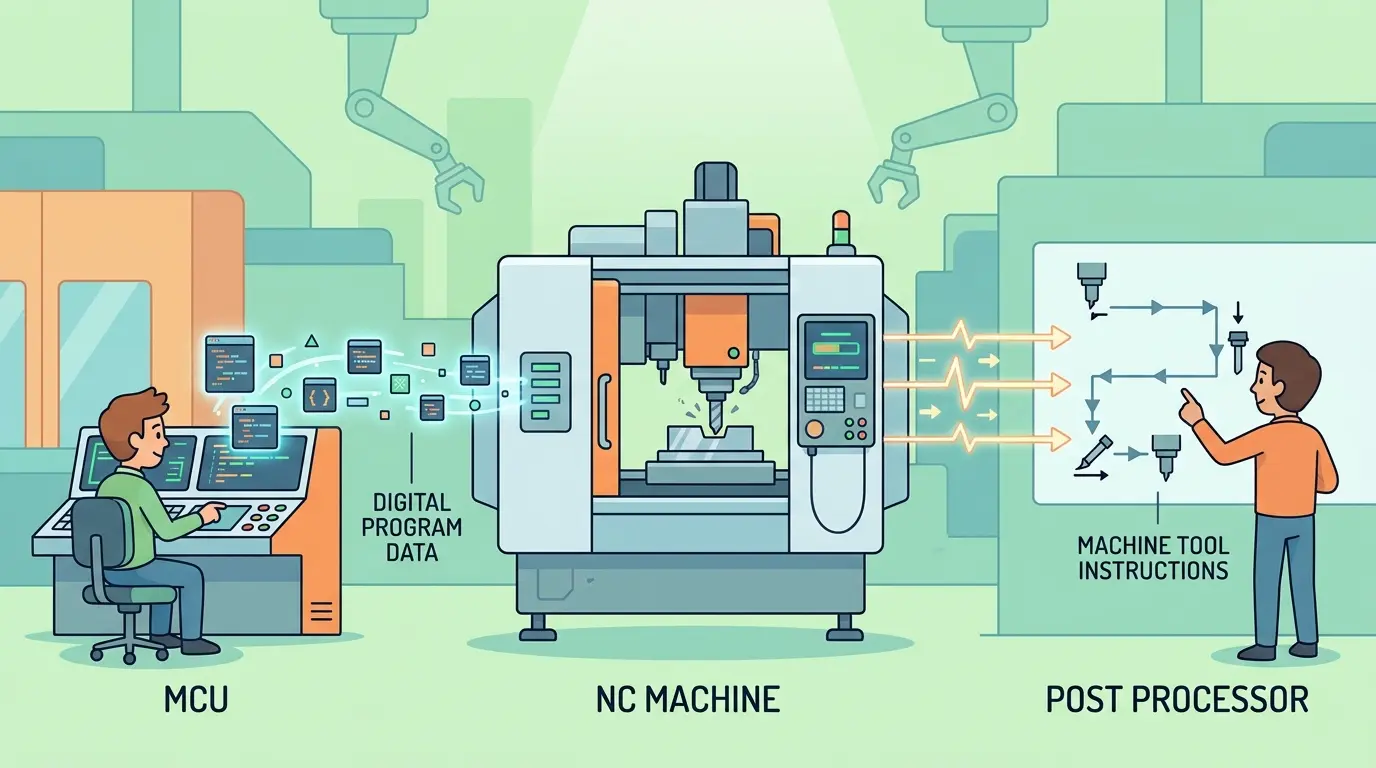
Most machine buyers can recite the standard component list—controller, servos, spindle, frame—but that checklist tells you nothing about why one machine holds tolerance for a decade while another drifts within months. This article breaks down the NC machine as a layered system where structure, motion transmission, process head, control logic, feedback, workholding, and support systems must work as one integrated stack. Before you compare axis counts or spindle power, you need to understand which layer will fail first under your actual workload, because the machine only performs as well as its weakest component.
Why a Component List Is Not Enough for Machine Buyers
Ask most people what makes up an NC machine and you will get a familiar list: a controller, servo motors, a spindle, and a frame. That answer is technically correct but practically useless for anyone who has to choose between two machines, keep one running in production, or diagnose why a part suddenly drifts out of tolerance.
The problem is that numerical control is not a single technology. It is a layered system where a program becomes physical motion only when structure, drives, control logic, feedback, tooling, workholding, and support systems all work together. If any one layer is weak, the entire machine becomes less trustworthy, regardless of how impressive the other components look on a spec sheet.
This article walks through each layer in the order it matters on the shop floor, from the foundation up to the support systems that determine whether a machine holds its accuracy over years of service.
NC and CNC: Same Physical Stack, Different Control Sophistication
Before examining components, it is worth clearing up a terminology issue that confuses many buyers. The difference between NC and CNC is often overstated. In practical terms, both machine types rely on the same physical architecture: structure, guided motion, a process head, workholding, feedback, and support systems. The real difference lies in the sophistication of the control and data handling, not in a fundamentally different hardware universe.
This distinction matters because it shifts the conversation from historical labels to production reality. Whether a machine uses a simpler NC path or a full CNC system, it succeeds or fails based on whether the physical stack can execute instructions repeatedly. A newer control label does not rescue weak mechanics, and an older control does not automatically make a rigid machine obsolete.
The production question stays the same regardless of terminology: can this machine translate programmed intent into stable, repeatable physical work day after day?
Structure Comes First Because Everything Else Depends on It
The base, frame, column, or gantry is the first component that matters because it defines whether the machine can hold alignment while loads, heat, vibration, and repeated cycling work against it. Every other component depends on that foundation remaining honest.
Structure rarely gets the attention it deserves in casual machine comparison. Buyers often discuss axis count or spindle power before asking how the machine resists movement it did not command. A weak structure does not always fail dramatically. More often, it shows up as finish instability, drifting accuracy, shortened tool life, or a machine that feels overly sensitive to setup variations.
For shops evaluating a new machine, the structure should be assessed against the actual workload, not just the brochure. A casting that is adequate for light routing may flex noticeably under heavy cutting or when the machine runs continuously through a long production shift. The details vary by machine type, but the principle holds across all of them: if the structure is weak for the workload, the rest of the stack spends its life compensating.
Motion Components Carry the Program into Physical Space
Once structure exists, the machine needs a motion layer. Guides, bearings, rails, screws, belts, couplings, and drive components are what turn control commands into actual axis travel. This is where the program stops being abstract and becomes physical movement.
Motion quality is not a single part but a chain. Guides affect smoothness and alignment. Transmission elements affect stiffness, speed, and responsiveness. Couplings and drive interfaces determine how honestly torque and rotation become linear travel. The result the shop sees at the tool tip is the cumulative behavior of that entire chain.
This is why machine comparison becomes dangerous when buyers reduce motion to a single headline number like rapid speed or servo power. The more useful questions are: how is motion carried, how well does it stay aligned over time, and what maintenance burden does the chosen transmission create under the real workload? A machine that moves fast but loses alignment under load is not faster in production; it is simply faster at making scrap.
The Process Head Turns Motion into Material Change
No numerically controlled machine is useful until it can actually act on the material. In milling and routing, that means the spindle or process head. In other machine types, it may be a cutting, drilling, sawing, engraving, turning, or shaping unit, but the logic is the same. This component is where motion meets work.
The process head defines how the machine applies the movement that the control and motion stack make possible. It influences toolholding, cutting behavior, vibration response, surface finish, thermal behavior, and part quality. On routing and milling platforms, the spindle arrangement matters because it is where structure, motion, tooling, and setup all converge.
Spindle or process-head comparison should never happen in isolation. The working end of the machine only delivers honest performance when the rest of the stack can support it. A high-speed spindle mounted on a flexible frame or paired with poor toolholding will not produce the surface quality its rating suggests.
The Control Layer Interprets Instructions and Coordinates Sequence
The control layer reads instructions, coordinates axis behavior, manages sequence logic, and tells the machine what should happen next. It links programmed intent to actual machine timing. Without it, the other components are only mechanical possibility.
But the control is not valuable simply because it exists. It is valuable because it can manage motion, inputs, outputs, interlocks, and operator interaction in a stable way that fits the production task. A control with rich features may still be a poor fit if the machine around it is weak or if the shop cannot support its complexity.
Buyers should judge the control both by function and by integration. How easy is it to set up, recover, edit, diagnose, and run repeatedly? How clearly does it coordinate the rest of the machine? Those questions reveal much more than the brand name on the screen. A control that is difficult to navigate or prone to confusing fault messages will cost more in operator time than any feature list can recover.
Program Delivery Is Part of the Machine Stack
Short explanations of NC machines often skip program delivery, but the machine needs a practical way to receive, store, edit, or call up instructions. In some environments that burden is light. In others, it shapes daily uptime, changeover speed, and the risk of human error. A strong mechanical platform with clumsy data handling can still frustrate production.
Input method should be treated as part of the machine’s working components rather than as a side issue. If the shop changes jobs frequently, revises programs often, or needs clean communication between office and machine, program delivery becomes part of repeatability. The physical cut may still be excellent, but the workflow may be weak if data handling is unreliable or awkward.
A useful system view therefore includes not only the cutting hardware and control logic, but also the path by which instructions become the right instructions at the right machine at the right time.
Feedback and Reference Systems Tell the Machine Where Reality Is
An NC machine does not only need to command motion. It needs to know what actually happened. Feedback devices, encoders, switches, probes, reference systems, and measurement routines close that loop. They tell the machine, and the people around it, whether commanded reality and physical reality still match.
Feedback deserves to be treated as a core component layer instead of an optional refinement. Without credible feedback, the machine becomes harder to trust over time. Axes may move, but the process cannot confirm that position, sequence, and machine state remain aligned with expectation.
The same principle applies at the human level. Setup measurements, reference checks, and process verification are part of the component stack because they protect how the machine is actually used. A machine that depends on invisible correction by experienced operators is still missing repeatability, even if the hardware list looks complete.
Workholding and Toolholding Are Basic Components, Not Accessories
Many quick explanations of NC machines understate this layer. But workholding and toolholding are absolutely basic components because they define how securely the material and the tool exist inside the machine’s coordinate system. If the work shifts or the tool interface is inconsistent, the quality of the frame, drives, and control becomes less meaningful.
Fixtures, clamps, vacuum systems, chucks, collets, holders, and their related interfaces belong in any serious answer to this topic. These parts do not only support the process. They determine whether the machine can use its programmed precision repeatedly.
This is also where daily production pain often begins. A shop may blame the machine when the real weakness is unstable workholding or casual tool setup. In practice, the NC machine is only as repeatable as the physical relationships it can hold under load and across repeated cycles.
Support Systems Keep the Main Components Inside a Healthy Operating Window
Lubrication, cooling, chip management, guarding, sealing, cable handling, enclosure behavior, pneumatic or hydraulic support, and maintenance access are sometimes called secondary systems. In real production they are not secondary at all. They are the systems that keep the main components alive and stable.
This is one reason two machines with similar headline specifications can age very differently. If one has better support-system integration, it may hold accuracy and serviceability far longer. If the support layer is weak, every primary component pays the penalty. Contamination rises. Heat increases. Wear accelerates. Recovery time after faults gets worse.
For practical buyers, this means support systems should be read as part of the machine’s real cost model. The glamorous components make the quote. The support components determine how often the shop regrets the quote later.
Maintenance Access Changes Whether Good Components Stay Good
A machine can be built from solid components and still become troublesome if those components are difficult to inspect, clean, lubricate, adjust, or replace. Maintenance access deserves to be counted among the practical basics because it determines whether the rest of the stack will actually stay within a healthy range under factory conditions.
Serviceability belongs in machine comparison from the start. If the team cannot reach the real wear points easily, routine care gets deferred. When routine care gets deferred, component quality on paper matters less because the operating condition drifts anyway. The machine then appears less reliable than its original build would suggest.
Good buyers therefore ask not only what the components are, but how the shop will live with them. That question often reveals more about long-term value than another round of specification comparison.
A Machine Is Only as Strong as Its Weakest Layer
This is the most important buyer lesson. An NC machine is not a sum of independent features. It is a layered system where weakness in one layer limits the value of the others. A rigid base with weak motion components disappoints. Good drives on poor structure disappoint. Advanced control paired with unstable workholding disappoints. Strong headline specifications on a weak support layer disappoint more slowly, but they still disappoint.
Mature shops compare machines by interaction, not by checklist length. How do the structure, motion, process head, control, feedback, and support systems work together? Where does the design seem balanced? Where does it seem overbuilt in one area and compromised in another? Those are the questions that make comparison real.
The same rule also helps maintenance teams. When symptoms appear, the likely cause is often not the whole machine. It is one weak layer forcing the others to compensate until the result reaches the finished part.
Applying the Stack Logic to Machine Selection
This layered logic applies across machine families. A routing or nesting machine emphasizes structure, travel, spindle behavior, hold-down, and coordinated drilling or cutting. A stone machine emphasizes rigidity, process-head stability, support systems, and contamination control around abrasive material. Even when the machine family changes, the component stack remains recognizable: structure, motion, control, process head, holding strategy, feedback, and support environment.
That is why broad equipment comparison often works better when it starts from category-level machine families such as CNC nesting machines rather than from an isolated feature count. The stack changes in detail, but the buyer question stays the same: which layers matter most for the production bottleneck I am trying to solve?
For shops working through this evaluation, reviewing the available machine lineup with the stack logic in mind is more productive than comparing spec sheets side by side. The machine that wins on paper may not be the machine that wins in production.
Understand the Stack Before You Compare the Machine
The basic components of an NC machine are not just a controller, some axes, and a spindle. They are the full set of layers that turn numerical instruction into controlled, repeatable material work: structure, motion transmission, process head, control, feedback, holding, and support systems.
Once buyers understand the stack, they stop asking weaker questions like which machine has more features in isolation. Instead they ask whether the machine’s layers match the real workload, the expected precision, the maintenance discipline, and the operating environment. That shift usually leads to better buying decisions and better troubleshooting later, because the machine is understood as a system rather than as a brochure headline.