Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
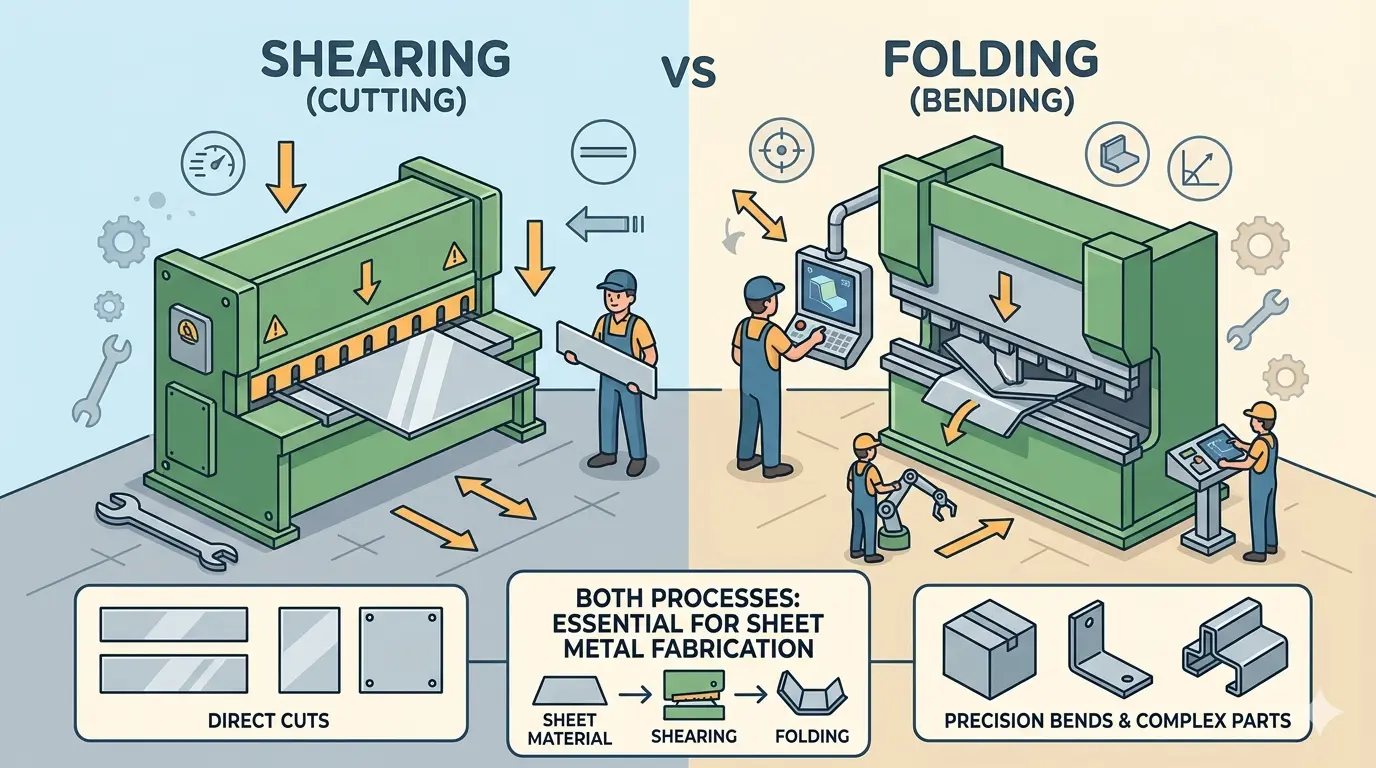
Before comparing machine specs, trace a single part from raw sheet to finished component and locate where the friction actually starts. Shearing and folding are sequential tools, not substitutes: one disciplines blank preparation upstream, the other controls formed geometry downstream. The real buying decision is not which machine is more advanced, but which missing capability is destabilizing your line—whether scrap begins with inconsistent blanks or with bends that force manual correction during fit-up. Follow the bottleneck through queue behavior, scrap classification, and touch time before committing capital.
Start With The Part, Not The Machine
The confusion between shearing and folding usually starts when the buying conversation skips the process map. A CNC shearing machine and a CNC folding machine solve different manufacturing steps. Shearing produces straight-edged blanks from sheet stock. Folding takes a prepared blank and creates a three-dimensional part with bends, flanges, hems, and formed geometry. One manages separation. The other manages shape.
So the real question is not which machine is better. It is which missing capability is costing more money in your current route. If downstream teams are waiting on clean, repeatable blanks, the pressure is upstream. If blanking is under control but welding, fitting, or assembly quality suffers because bends are inconsistent, the pressure is in forming. Follow one real part from raw sheet to finished component, and the comparison usually stops looking ambiguous.
Walk The Part Through The Route
Raw sheet arrives. It is separated into blanks. Those blanks may pass through punching, laser cutting, secondary trimming, deburring, or other preparation steps depending on the part family. After the flat pattern is correct, the part moves into forming, where bends and flanges create the final geometry. Later operations such as welding, hardware insertion, painting, or assembly depend on what happened earlier.
Shearing belongs near the beginning of that route. Folding belongs after the flat pattern already exists. That does not mean they always sit directly next to each other. In many routes, other operations live between them. But the hand-off point is the same: a shearing machine prepares flat material; a folding machine converts flat material into shape.
Once that hand-off point is clear, the buying discussion becomes less about machine comparison and more about bottleneck location. Where does the queue start? Where does scrap begin? Where does manual touch time expand? That is the layer that deserves the budget first.
What Shearing Actually Solves
Shearing creates straight cuts quickly and repeatedly. Its strongest fit is not artistic flexibility. It is disciplined blank preparation. When a factory needs strips, rectangles, repeat panel sizes, or straight-edge blanks that feed later operations, shearing is an efficient upstream tool. The value is not only the cut itself. The value is that downstream punching, forming, welding, and assembly receive material that is closer to the correct starting point every time.
That matters more than many buyers first assume. A weak blank-preparation stage does not only waste sheet. It destabilizes the rest of the line. Operators downstream compensate for wrong sizes, inconsistent edge conditions, or stop-start material flow. Scheduling becomes noisier because later stations are waiting on something that should have been routine. In that environment, a shearing upgrade is not just a speed decision. It is a line-discipline decision.
Shearing is especially effective when the part family is dominated by straight-edged work and when the commercial gain comes from repeatability and feed stability more than from complex geometry. If the business makes many simple blanks that later become bent or assembled products, better shearing can clean up the whole front end of the route.
Where Shearing Stops Helping
The limit of shearing is just as important as its value. Shearing is not a universal flat-pattern tool. If the part family depends on complex contours, internal holes, nested geometry, notches, tabs, or irregular outlines, a straight-cut blanking method may only cover part of the job or may not fit at all. In those cases, the upstream decision may need to shift toward laser, punch, plasma, router, waterjet, or another cutting path depending on the material and the geometry.
This is where buyers sometimes misread the economics. They see that blanks are delayed and assume any faster upstream machine will help. But if the part family is fundamentally contour-driven, faster straight blanking will not solve the actual route. It may simply create a second handling step before the real shaping process begins.
So the first discipline in a shearing decision is honesty about the part family. If most of the work can be reduced to clean straight blanks, shearing deserves attention. If the value of the part starts with geometry that a shear cannot create, the real upstream debate sits elsewhere.
What Folding Actually Solves
Folding operates on a different commercial problem. It assumes the blank already exists and asks how consistently the shop can convert that flat blank into final geometry. That is where repeat angle behavior, flange accuracy, hem quality, part alignment, surface condition, and labor consistency begin to matter more than raw blanking speed.
When a folding stage is weak, the business often feels it through secondary symptoms. Assemblies need correction. Hardware alignment drifts because bend position varies. Welding preparation takes longer because formed parts do not line up the same way from one batch to the next. Operators compensate manually because the machine stage before assembly is not giving them a repeatable formed part. Those are not blanking problems anymore. They are forming-control problems.
That is why a folding machine can create far more value than its headline cycle time suggests. It does not improve the line by cutting material faster. It improves the line by giving downstream work a more reliable geometry to build from.
Where Folding Usually Creates More Value Than Better Blanking
Folding deserves first priority when the factory already has a workable way to generate flat patterns, but the shaped parts leaving the bend stage are still unstable in labor, fit, or quality. Common warning signs include repeated rebending, angle adjustments during assembly, inconsistent flange length, too much dependence on skilled manual correction, or visible throughput loss in stations waiting on formed components rather than on blanks.
In that situation, buying more upstream blanking speed can actually make things worse. The factory does not need more flat parts faster. It needs a more controlled route for turning flat parts into finished shapes. If forming is the unstable stage, feeding it more aggressively only builds a larger queue in front of the wrong bottleneck.
This is why folding often carries the higher leverage in enclosure work, formed-panel work, and product lines where the commercial value sits in the accuracy of the finished shape rather than in the speed of initial blank separation.
They Are Sequential Tools, Not True Substitutes
In a healthy process map, shearing and folding do not really compete. They live in sequence. Shearing prepares material for the stages that follow. Folding creates geometry after the flat work is ready. The reason they get compared as if they were interchangeable is usually that management is still discussing the shop through a broad label such as “sheet metal automation” instead of tracing where value is actually created and where delay actually begins.
That is also why direct machine-to-machine comparison can be misleading. One machine improves front-end preparation. The other improves downstream forming control. If a buyer is genuinely torn between them, the most likely issue is not technical overlap. The most likely issue is that the current route has not yet made the bottleneck visible enough.
Recent job history is usually more revealing than any brochure in this situation. Look at where orders slow down, where parts are adjusted by hand, where scrap gets classified, and where internal complaints begin. Those signals usually tell you whether the missing discipline is blank preparation or shape creation.
Read The Bottleneck Through Scrap, Queue, And Touch Time
Cycle time by itself can mislead because a fast station can still be the wrong investment priority. What matters is where the expensive friction begins.
If scrap starts with wrong blank sizes, poor upstream feed, or repeated errors before the part ever reaches forming, the front end deserves attention first. If scrap begins after bending, during fit-up, or during downstream assembly checks, the forming stage may be the real leverage point. If labor time is being burned on measuring, re-bending, squaring, adjusting, and re-checking, that usually points toward a forming-control gap, not a blanking gap.
Queue behavior matters as much as scrap behavior. When operators at later stations are repeatedly idle because blanks are not ready, shearing or another upstream cutting solution may be the priority. When blanks are stacked and waiting but formed parts are still the constraint, better folding or other forming improvement should move ahead first.
Touch time is the third clue. A station that looks acceptable on paper can still be destroying margin if it depends on too much manual rescue. Buyers should pay attention to where human judgment is being used to correct a process that should already be repeatable. That is often the clearest sign of where capital will work hardest.
A Priority Map For Different Shop Profiles
Different factories feel this decision differently because the part mix changes where leverage sits.
- A blank-supply or service-center style operation often leans toward shearing first because the core value is delivering flat material into later routes quickly and predictably.
- An enclosure or panel-forming shop often leans toward folding first once blank supply is already reasonably stable, because final geometry and assembly fit drive more of the commercial outcome.
- An HVAC or light-fabrication operation may need to examine whether the real pain is feed speed into forming or repeatability of the formed profile itself. The answer can change by product family.
- A high-mix job shop should be especially careful. If it handles many shapes and low volumes, the upstream debate may not be shearing versus folding at all. It may be whether straight blanking is even the right first cut process for the work it actually sells.
These profiles are not rules. They are reminders that machine priority should follow the revenue pattern of the shop, not generic industry language.
Questions That Expose The Better First Investment
When the buying team is still split, these questions usually force a clearer answer:
- Are delayed jobs more often waiting on flat blanks or on formed parts?
- Does scrap usually begin before forming, during forming, or after forming during fit-up?
- Is the product family dominated by straight blanks, or by parts whose value depends on controlled bends and flanges?
- If one stage is made faster, will the next stage simply become a larger queue?
- How much labor is being spent correcting shape instead of creating it?
- Would upstream speed help if the downstream geometry is still inconsistent?
- Are current blanking limits caused by straight-cut preparation, or by a need for more complex flat-pattern cutting methods?
These are better buying questions than “Which machine is more advanced?” because they tie the decision back to the route that actually makes money.
When The Bigger Decision Is The Whole Cutting Route
Sometimes this comparison is only a surface symptom of a broader equipment-planning issue. If the shop keeps discovering that parts need irregular shapes, internal features, or contour-driven blanks before they ever reach forming, then the upstream question may be bigger than shearing. It may require a broader look at which cutting process fits which material and workflow rather than assuming every flat-pattern problem should be solved by a shear.
The same discipline applies when proposals are already on the table. Buyers should not compare shearing and folding packages only through headline capacity. They should compare what is actually included in the route, the support burden, and the assumptions hidden in each offer. That is why it is useful to borrow a stricter method for checking quotes without missing scope differences.
And if the project is broader than one isolated station, it can help to step back and review the Pandaxis machinery lineup as a reminder that equipment choices should support the whole production flow, not just the noisiest bottleneck of the week.
Choose shearing when flat blank preparation is the missing discipline. Choose folding when shape accuracy and formed-part repeatability are where the margin is leaking. If the route still cannot distinguish between those two needs, the process map needs work before the budget does.