Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
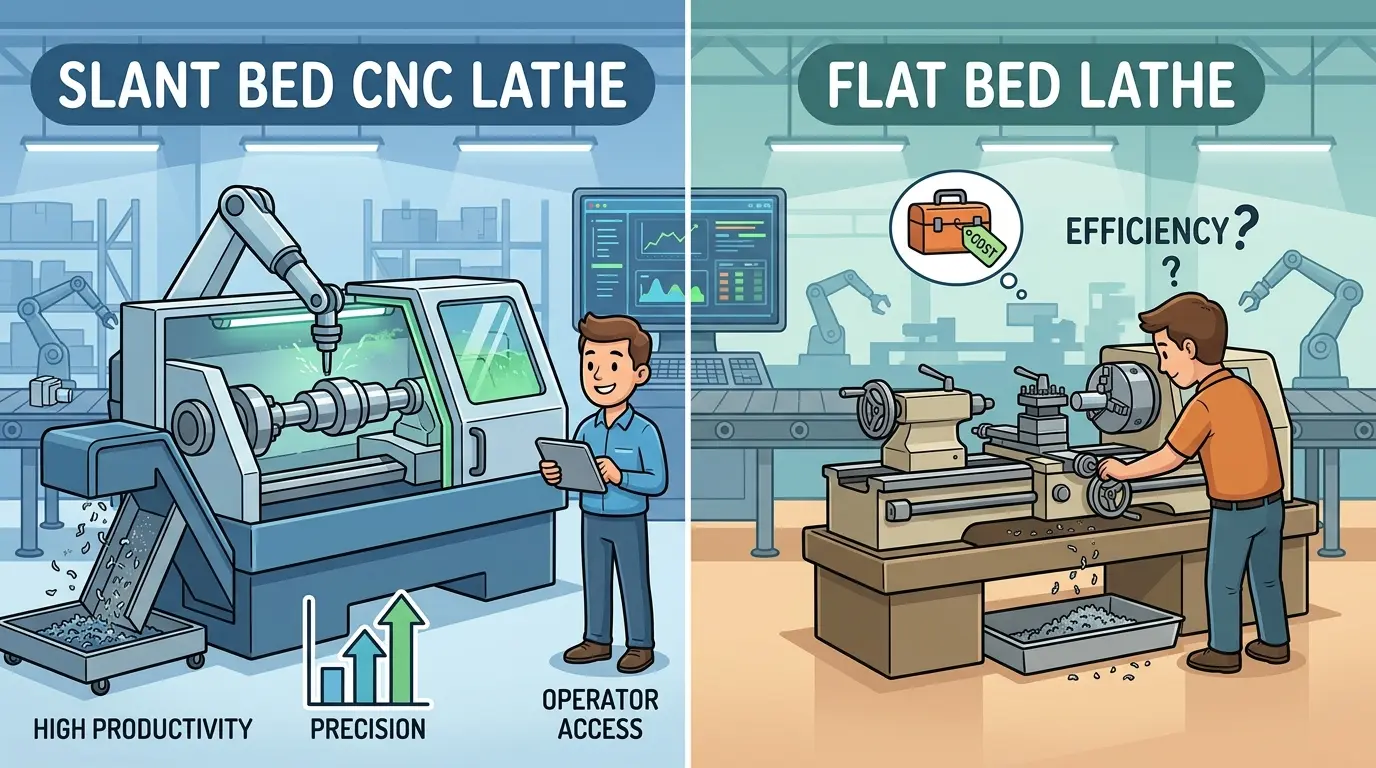
When your turning cell is being planned around repeated cycles, chip behavior, and operator rhythm, the bed angle is not a cosmetic detail—it is a production variable that shapes every shift. Slant-bed geometry clears swarf from the cut zone, tightens the machine footprint, and shortens the load-check-measure loop, while flat-bed layouts keep their edge for long shaft work, retrofit projects, and mixed job lots where manual handling dominates. The decision matters because it determines how often an operator intervenes, how cleanly automation integrates, and whether your part family runs with fewer interruptions. Match the layout to the workflow you actually run, not the one on the spec sheet.
Why the Bed Layout Question Comes Up in the First Place
When a shop starts comparing CNC lathes, the bed layout is usually one of the first visible differences. But the decision is not about how the machine looks on the showroom floor. The angle of the bed changes chip evacuation, operator access, machine footprint, automation compatibility, and the type of turning work the machine can support over years of service. That is why procurement teams need to treat this as a production-planning question rather than a design preference.
The slant-bed configuration dominates modern production turning because the angled structure lets chips fall clear of the cutting zone and creates a compact, ergonomic machine envelope. Flat-bed lathes remain relevant for longer workpieces, simpler turning operations, retrofit projects, and certain heavy-duty applications. Neither layout is inherently superior. Each one suits a different mix of production priorities, and the right answer depends on the parts you actually run.
What the Layout Actually Changes on the Shop Floor
In a slant-bed machine, the bed and guideways sit at an angle, typically between 30 and 60 degrees. This geometry does more than change the silhouette. It creates a natural path for chips and coolant to flow away from the cutting zone, keeps the turret closer to the operator for loading and gauging, and allows the machine builder to package the spindle, turret, and tailstock into a smaller footprint.
A flat-bed lathe keeps the bed horizontal. The cutting zone sits more open and accessible, which can be an advantage for certain setups. But chips tend to accumulate around the work area, and the operator often has to reach further across the machine to load parts or inspect tools. These differences look minor during a demonstration. After weeks of production, they become daily factors in cycle time, intervention frequency, and operator fatigue.
The practical question is not which layout looks more advanced. It is which layout reduces the number of small interruptions that accumulate over a shift.
Slant-Bed Lathes Favor Repeated Production Cycles
Slant-bed machines earn their keep in environments where turning is repetitive, chips are continuous, and uptime depends on clean evacuation. When swarf falls away from the cut instead of nesting around the tool, surface finish stays more consistent and tool life improves. The operator can also reach the turret and chuck more easily, which shortens the load-check-measure cycle that dominates most production shifts.
The architecture also supports automation more naturally. Bar feeders, gantry loaders, and robotic tending systems integrate more cleanly with a compact slant-bed envelope. The machine occupies less floor space per unit of turning capacity, which matters when you are laying out a cell with multiple machines and a single operator.
None of this means every slant-bed machine outperforms every flat-bed machine. It means the architecture aligns with shops that prioritize throughput, stable tool access, and a disciplined production rhythm. In many cases, the real benefit is not higher spindle speed or faster rapids. It is that fewer small problems interrupt the cycle.
Flat-Bed Lathes Still Earn Their Place in the Right Context
Flat-bed lathes remain the practical choice for long shaft work. When the part extends well beyond the spindle nose, the horizontal bed provides better support for steady rests and follow rests. The open layout also makes it easier to handle odd-shaped or awkward workpieces that do not fit neatly into a production-cell rhythm.
Shops with established legacy tooling, experienced operators, and mixed job lots often find flat-bed machines more familiar and easier to maintain. The simpler architecture can be more straightforward for a maintenance team to understand, and the open access makes inspection and adjustment less cramped. For retrofit projects, a flat-bed machine is often the more practical starting point because the structure is easier to modify and the control upgrade path is well understood.
The mistake is assuming that because slant beds dominate new production cells, flat beds are obsolete. They are not. They are simply suited to a different operating context, one where part length, setup variability, or manual handling matters more than compact packaging and chip-flow optimization.
Chip Control Is the Most Practical Difference Between Layouts
Turning performance depends heavily on how chips behave. Stringy chips, built-up nests, and poor evacuation force operators to stop the machine, clear the area, and restart. Each intervention costs minutes, and those minutes add up across a shift. Slant-bed geometry helps manage this problem because chips naturally fall away from the cutting zone rather than collecting in awkward places.
This benefit becomes especially visible in unattended or lightly attended production. When the machine runs longer between operator visits, the ability to clear chips without intervention directly affects how many parts you can produce per shift. Materials that produce difficult chip shapes, such as ductile steels or certain aluminum alloys, amplify the difference.
A flat-bed machine can still manage chips effectively with the right tooling, coolant pressure, and operator habits. But it starts from a less favorable geometry. If your material family already creates challenging chip behavior, the bed layout becomes a daily cost driver rather than a minor design detail.
Operator Access and Ergonomics Affect Output Over Long Shifts
Shop managers sometimes underweight ergonomics because it sounds less technical than spindle power or axis travel. But access to the chuck, turret, gauging positions, and part-loading area directly affects speed, consistency, and safety. Slant-bed machines typically package these interactions more efficiently. The operator stands closer to the work zone, reaches less, and maintains better visibility of the cut.
Flat-bed machines can offer their own access advantages for long or awkward setups, particularly when the operator needs to work along the length of the bed. But for routine turning cycles, the flat layout often asks more of the operator in terms of reaching, bending, and moving around the machine.
This matters most where one operator runs multiple machines. The easier each machine is to approach, clear, inspect, and reload, the more smoothly the cell runs. A turning cell that feels fine for ten minutes can feel very different after repeated load-check-measure cycles through an entire shift.
Part Family Should Drive the Decision More Than Marketing Language
Layout decisions become clearer when you stop thinking in general machine terms and start thinking in part families. Short, repeated parts with steady chip production and a production-cell rhythm point toward slant-bed logic. Longer, more varied parts with less dense cycle repetition keep flat-bed logic competitive.
This is also where the broader turning strategy comes into play. If your parts increasingly justify integrated operations, you may need to think beyond bed layout alone. A turning center with live tooling and sub-spindle capability changes the calculation differently than a standard lathe workflow. Bed layout does not answer the entire automation question, but it often indicates which direction the shop is already heading.
Comparison Table for Buyers
| Factor | Slant-Bed CNC Lathe | Flat-Bed Lathe |
|---|---|---|
| Chip evacuation | Usually more favorable in production turning | More dependent on tooling and operator intervention |
| Machine footprint | Often compact and production-oriented | Often simpler and more open in feel |
| Operator access | Typically efficient around turret and cutting zone | Can suit certain longer or simpler setups |
| Best fit | Repeated production turning and modern cell logic | Longer work, simpler tasks, retrofit or legacy environments |
| Common tradeoff | May cost more or feel more specialized | May require more chip and workflow management |
| Automation direction | Often aligns better with compact production flow | Often stronger where manual handling remains central |
The table is not absolute, but it frames the decision around workflow rather than tradition.
Automation and Handling Strategy Often Tip the Balance
The more your shop wants a compact, disciplined turning cell, the more the slant-bed layout tends to make sense. This does not require a fully automated lights-out operation. Even modest automation goals, cleaner operator circulation, or a tighter cell footprint can push the decision in that direction.
Flat-bed layouts still work well where loading style, part length, or setup variability keep the operation more manual by nature. The problem arises when buyers want slant-bed production behavior while keeping a flat-bed decision based on habit alone. The clearest indicator of fit is the handling rhythm the shop wants over the next few years. If you are moving toward bar feeders, robotic tending, or multi-machine supervision, the slant-bed layout supports that direction more naturally.
Maintenance, Training, and Shop Culture Influence the Best Choice
The right layout also depends on the people supporting the machine. Shops with strong modern turning culture, organized tooling, and repeatable setup practices often gain more from slant-bed architecture. The compact envelope and integrated chip management reward disciplined workflow. Shops built around experienced operators doing mixed, irregular work may remain comfortable and productive with flat-bed machines.
Procurement should consider not just the machine but the culture it will enter. The most efficient architecture on paper can still disappoint if the workflow and staffing around it are mismatched. This is why layout decisions are hard to outsource entirely. The best answer depends on how the shop actually behaves, not just on what spec sheets suggest.
Used-Machine Context Changes the Decision Again
In the used market, bed layout interacts with age and maintenance history differently. A slant-bed machine that has been run hard but maintained intelligently can still offer excellent production value. A flat-bed machine with simpler architecture may be attractive where the buyer values familiarity and inspectability. In both cases, condition matters more than layout reputation.
The used-buying question should stay grounded in actual machine health, part-family fit, and installed-cost reality. Some layouts age better than others, but the reasons usually sit in maintenance and workload history rather than geometry alone. Inspect guideways, check for wear patterns, and verify the control and drive systems before making a decision based on layout preference.
Common Procurement Mistakes to Avoid
One common mistake is choosing layout by habit. Buyers often default to what the current shop already has, even when the job mix has changed. Another mistake is choosing the slant-bed layout automatically because it appears more modern, without asking whether the actual parts, staffing, and capital plan will use those advantages.
A third mistake is focusing on layout too early and ignoring the bigger turning decision. If the shop has not clarified whether it needs a simpler lathe workflow, a more integrated turning platform, or a different part-handling strategy altogether, the bed discussion becomes a false precision exercise. A better approach is to compare part families, chip behavior, operator involvement, and expected duty cycle first. That makes the layout decision much easier and much less emotional.
Keep the Comparison Inside the Right Machine Family
Like many CNC buying questions, this one improves when the shop avoids mixing unrelated categories. A turning layout question should stay a turning workflow question. The same discipline applies across broader capital planning, whether the business is evaluating metal turning or entirely different production categories in the wider Pandaxis product catalog. Different machine classes exist for different problems. The bed-layout question is only meaningful once the turning family itself is already the right family.
Some buyers jump from flat-bed versus slant-bed to completely unrelated machine comparisons without first confirming what their turning process actually needs. That creates confusion and delays the procurement cycle without adding useful information.
Ask Which Layout Makes the Shift Easier to Run
The cleanest way to decide is to think about an ordinary shift rather than an ideal demonstration. How do chips behave after dozens of cycles? How often does the operator need to intervene? How awkward is gauging and reload? How well does the machine support the part family that keeps coming back? Which layout fits the staffing reality the shop actually has, not the staffing reality it imagines?
Those questions expose the answer quickly. Slant-bed CNC lathes usually fit production better when chip evacuation, compact packaging, ergonomic access, and repeated turning cycles matter most. Flat-bed lathes still make sense where longer workpieces, simpler turning tasks, retrofit traditions, or established operating habits dominate.
The best choice depends on the real part family, chip behavior, operator rhythm, and how modernized the turning workflow needs to be. Treat the layout as a production decision, not a cosmetic preference. The better layout is the one that makes the shift easier to run, not the one that looks more modern in isolation.