Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
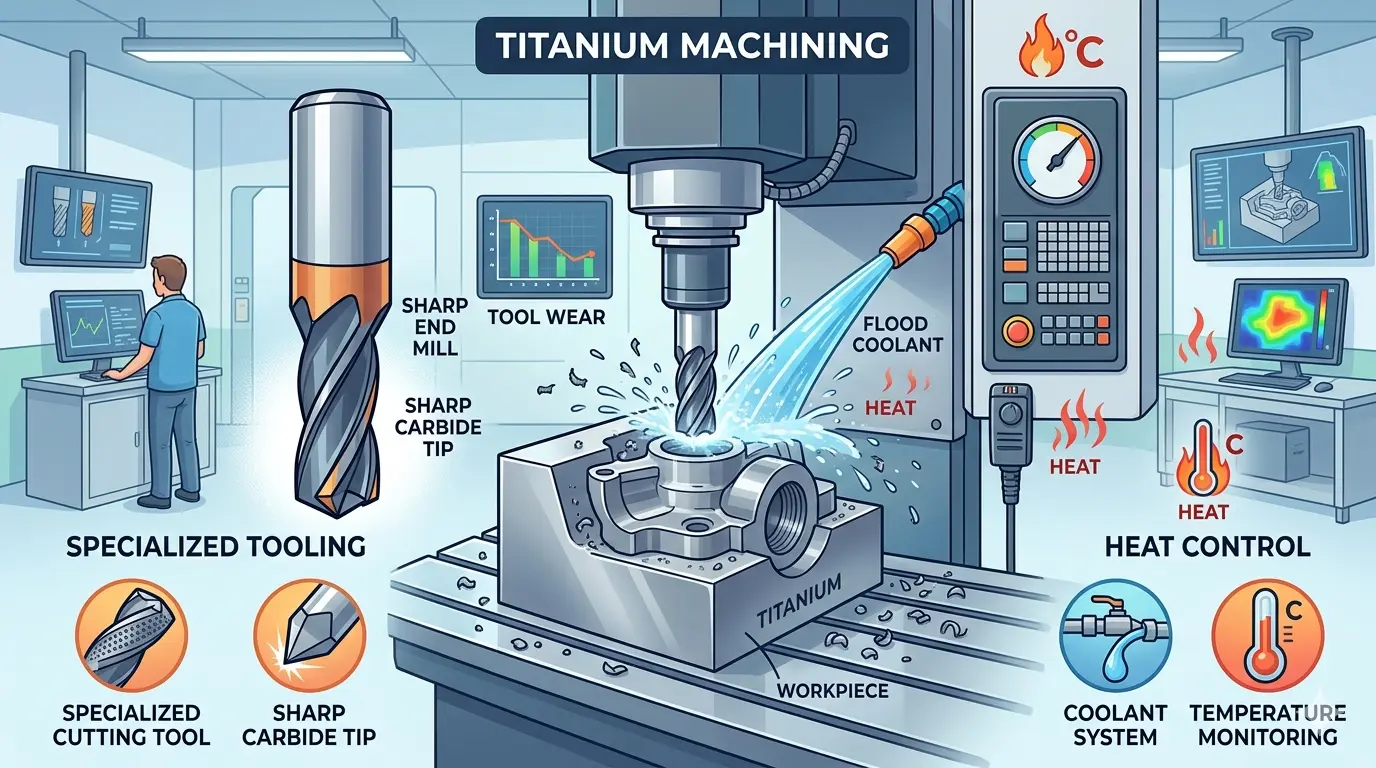
Titanium machining fails not from a lack of spindle power but from uncontrolled heat at the cutting zone, where the tool edge carries the thermal burden and degrades rapidly once engagement, chip flow, or rigidity slips. This article addresses the full production loop—tooling selection, holder rigidity, runout, evacuation, and fixturing—that determines whether a route survives real batch conditions or drifts into scrap. For buyers and engineers, the decision matters because quoting, cycle-time assumptions, and supplier selection all hinge on whether the process stays stable after edge wear begins, not just on the first good part.
Titanium Punishes Heat Buildup Faster Than Many Shops Expect
The central titanium machining problem is concentrated heat at the cutting zone. Titanium does not pull heat away from the edge as forgivingly as easier materials, which means the tool often carries more of the thermal burden. If the edge stays sharp, engagement is controlled, and chips leave the cut cleanly, the route can stay productive. Once one of those factors slips, heat remains where it hurts most.
That changes the whole behavior of the process. Instead of a clean shearing action, the tool begins to rub more, the edge wears faster, and the next pass begins from a weaker condition than the last one. Shops sometimes describe this as a route that “falls off a cliff,” but the cliff is usually built one unstable pass at a time.
This is why titanium planning should begin with a simple question: where is the heat supposed to go? If the answer depends on hope, aggressive feed claims, or a vague promise that “the machine has enough power,” the process is not really defined yet. Power helps only when the entire cutting package can keep the edge alive.
In practice, heat control is not one variable. It is the result of cutter selection, holder rigidity, runout control, engagement strategy, chip evacuation, coolant or air delivery, fixturing stiffness, and inspection discipline. Titanium rewards shops that treat those items as one connected loop instead of separate departments.
Tooling Quality Sets The Ceiling For The Entire Route
In easier materials, a shop can sometimes survive with tooling choices that are merely acceptable. Titanium is less tolerant. A cutter that looks economical on paper can become expensive quickly if it loses edge condition too early, cannot evacuate chips reliably in the real geometry, or demands replacement so frequently that cycle planning stops making sense.
That does not mean the most expensive tool is always the right tool. It means the tooling package has to match the route honestly. Roughing, semi-finishing, finishing, slotting, thin-wall work, and deep-feature access do not impose the same load on the edge. Shops with strong titanium results usually treat tooling as part of route architecture, not as a consumable line item added after the CAM work is done.
Good titanium tooling decisions usually answer practical questions such as these:
- What edge condition is needed to keep the part stable through the longest heat-producing features?
- How much stick-out is really required for the geometry, and where is it being added only for convenience?
- Which operations can tolerate gradual wear, and which ones fail quickly once the edge softens?
- Where does one tool save time but increase finish risk later in the route?
That is why tooling cost in titanium should not be treated as simple overhead. It is part of buying process stability. If a more capable tool holds size longer, reduces rework risk, and avoids mid-batch failure, its real value is broader than the insert or end mill price alone.
Holder Rigidity, Runout, And Stick-Out Decide Whether Good Tools Actually Work
A strong cutter mounted badly is still a weak process. Titanium makes that obvious. Small setup errors that might be tolerable in softer materials become much more visible when the edge is already carrying high thermal stress.
Runout matters because it distributes the load unevenly. One flute works harder than the others, heat rises faster, and tool life becomes less predictable. Excess stick-out matters because it reduces system stiffness right where the process needs control. Weak holder discipline matters because titanium does not forgive intermittent edge loading for long.
This is one reason titanium jobs are often misquoted. The estimator sees an operation that looks straightforward, but the real route requires more conservative extension, more rigid workholding, more careful holder inspection, or more frequent tool changes than the initial assumption allowed. The geometry may not look dramatic on the print, yet the machining conditions are far less forgiving than the drawing suggests.
For production teams, the lesson is simple: do not separate cutter choice from holder choice. Titanium routes should be reviewed as a complete cutting system. Shops that do this well are usually not the ones making the loudest claims. They are the ones that remove avoidable instability before the spindle starts.
Chip Evacuation Is A Survival Issue, Not A Cleanup Detail
Titanium does not tolerate recutting well. Once chips stay in the cut, the process begins to fight itself. The tool is no longer engaging clean material under controlled conditions. It starts interacting with trapped heat and broken chip flow, which raises wear and destabilizes finish quality.
This is why geometry matters so much. Open-profile work is not the same as a deep pocket. A short, accessible path is not the same as a long-reach cavity with limited exit paths for chips. A route that looks efficient in a simple simulation can still become fragile if the chip evacuation strategy is not realistic for the actual feature.
In titanium, poor evacuation does more than shorten tool life. It changes the economics of the whole job:
- The shop may need more conservative toolpaths than first planned.
- Cycle time may rise because passes must be made safer, not just faster.
- Surface finish may vary across the feature instead of failing uniformly.
- Operator intervention may increase, which hurts scheduling and labor efficiency.
That is why strong suppliers talk about evacuation early when reviewing titanium work. If they focus only on nominal cycle time and say little about how chips leave the cut, they may still be pricing a route that looks cleaner in software than it will on the machine.
Engagement Strategy Often Decides Whether The Edge Lives Or Rubs
Titanium machining is full of routes that look productive until the engagement pattern becomes unstable. Full-width cuts, abrupt direction changes, repeated shock loading, or inconsistent stepovers can all push heat into the wrong place. Once the edge stops cutting under repeatable load, rubbing begins to replace clean material removal, and the route starts to deteriorate.
That is why the best titanium strategies are usually not the most dramatic ones. They are the ones that keep the cutter engaged in a controlled way long enough to finish the job without thermal collapse. The smartest route is often the one that looks slightly less aggressive on paper but remains stable deeper into the batch.
Buyers and engineers should care about this because it affects more than machining theory. It determines whether the supplier can hold tolerance and finish quality predictably over time. A quote built around aggressive engagement assumptions may look competitive at first, but if it depends on perfect edge condition for too much of the route, it may not survive real production.
Good titanium planning therefore balances speed against survivability. The point is not to cut timidly. The point is to keep cutting conditions repeatable enough that the tool continues to shear instead of sliding toward heat-driven instability.
Coolant And Air Strategy Have To Support The Actual Geometry
There is no universal coolant rule that solves titanium automatically. What matters is whether the chosen delivery method actually reaches the cut, supports evacuation, and keeps the thermal situation under control for that specific operation. Some routes depend on well-directed coolant. Others rely heavily on air blast and clean chip movement. Many require a combination of disciplined delivery and geometry-aware planning.
The weak version of coolant planning sounds like this: “We run titanium with coolant.” The useful version sounds like this: “Here is how coolant or air reaches the tool on the deepest features, where evacuation gets difficult, and where we see the route becoming vulnerable.”
That distinction matters because titanium problems often begin in local conditions, not across the whole part. One pocket, one corner transition, one long-reach tool, or one unsupported wall can become the place where heat stops being managed well. A general process rule is not enough if the risky features demand something more specific.
When a supplier can explain how thermal control is maintained across different feature types, it is usually a good sign that the route has been thought through. When the answer stays broad and generic, the process may still be relying on past success with less sensitive materials.
Part Rigidity And Fixturing Usually Drive The Hidden Cost
Many titanium jobs become expensive not because the part is large, but because it is mechanically vulnerable during cutting. Thin walls, long unsupported features, narrow ribs, deep cavities, or awkward clamping access can all reduce stability. Once that happens, the toolpath has to become more conservative, finishing passes may multiply, and inspection burden may rise.
This is where buyers often underestimate the route. They assume titanium cost comes mainly from slower material removal, but real cost often comes from the extra care required to protect geometry while the part is still attached and partially unsupported.
Fixturing review is therefore not a side conversation. It is part of the machining strategy. A stable clamp plan can protect finish quality, reduce chatter risk, and make tool behavior more predictable. A weak clamp plan can turn an otherwise manageable route into a slow, interruption-heavy process.
For suppliers, honest titanium pricing usually reflects this. Shops that understand the work will often ask more questions about access, sequencing, support, and interim stability than buyers expect. That is not wasted effort. It is where a large share of the batch risk is found.
The First Good Part Does Not Prove The Batch Is Safe
Titanium routes often look healthy at the beginning. Fresh tooling hides weaknesses. Surface finish appears acceptable. Dimensional results are in range. Then the process starts drifting as the edge condition changes and heat management gets harder.
That is why first-article approval should never be mistaken for full-batch confidence. The better question is whether the route stays credible after meaningful edge wear begins. Shops with mature titanium discipline usually have clear rules for when tools are replaced, when offsets are reviewed, when in-process inspection frequency rises, and which features are most likely to reveal drift first.
Without that discipline, the process can fail quietly:
- Surface finish degrades before size fails.
- Tool marks become less uniform before the operator treats them as a warning.
- Thin sections move slightly more as the edge condition worsens.
- Cycle time stretches because the team starts compensating manually.
These are not minor details. They affect schedule reliability, scrap exposure, and customer confidence. In titanium work, process control over time matters more than a clean first impression.
The First Signs Of Titanium Instability Usually Show Up In A Small Number Of Ways
The early warnings are often familiar. What matters is whether the team treats them as symptoms of a thermal-control problem rather than isolated shop-floor annoyances.
| Early Signal | What It Often Suggests | What Usually Happens Next If Ignored |
|---|---|---|
| Finish turns dull or streaky mid-batch | Edge wear is rising or the tool is beginning to rub | Tolerance stability becomes harder to hold and cycle confidence drops |
| Chips stop clearing cleanly from deep features | Evacuation path is weak for the geometry | Heat rises, recutting starts, and tool life shortens quickly |
| Tool life varies sharply from run to run | Runout, stick-out, or local engagement is inconsistent | Quoting becomes unreliable and troubleshooting consumes production time |
| Thin walls start moving more than expected | Fixturing or sequence is not protecting rigidity well enough | Extra finishing passes, scrap risk, or manual corrections increase |
| Operators intervene more often than planned | The programmed route is less robust than the setup sheet suggests | Labor cost climbs and throughput assumptions stop matching reality |
This table is useful because it keeps the diagnosis operational. Titanium rarely needs a dramatic explanation. It usually needs a shop to connect visible symptoms to the specific combination of heat, edge condition, and stability that caused them.
What Buyers Should Ask Before Sending Titanium Work To A Supplier
When buyers compare titanium suppliers, the goal is not to hear polished language about precision. The goal is to learn whether the supplier understands where the route will become unstable and how that instability is controlled.
Useful questions include:
- Which feature or operation is likely to carry the highest thermal risk on this part?
- How is tool replacement managed before visible finish failure appears?
- What part geometry makes the route most sensitive to chip evacuation problems?
- Which operations are most dependent on rigid holding or low runout?
- How does the supplier monitor drift after first-article approval?
- Where do cycle-time assumptions become less certain if tool life is shorter than expected?
Good answers are usually concrete. They refer to a pocket, a wall, a reach problem, a tool-access issue, a finishing risk, or a wear threshold. Weak answers stay abstract. They repeat that the shop machines difficult materials regularly without identifying the feature that actually governs the route.
Large quote gaps should be treated carefully for the same reason. One supplier may be pricing real thermal risk, honest tool life, and inspection discipline. Another may be pricing an optimistic route that works only if everything stays favorable. The same verification mindset used when comparing machinery quotes line by line is useful here as well, even though titanium machining itself sits outside the verified Pandaxis product-category scope.
Why This Topic Still Matters When Buyers Compare Machines
Titanium machining is not a direct Pandaxis catalog topic, but the logic behind it still matters for industrial equipment buyers. Any factory comparing machine tools, fixturing strategy, cooling discipline, or long-run process stability is really asking the same broader question: will this setup stay predictable when the route gets demanding?
That is why the best buying conversations go beyond headline specs. A machine can look impressive in marketing language and still disappoint if rigidity, heat control, chip handling, or integration discipline are weak where the real work happens. Buyers screening broader industrial equipment options can use the same mindset while reviewing the Pandaxis machinery lineup: focus on workflow fit, stability under load, and how the system behaves once production pressure replaces showroom conditions.
Titanium simply makes that lesson harder to ignore. If a shop can keep the thermal loop under control, protect the edge, evacuate chips cleanly, and hold the part rigid through its vulnerable features, titanium becomes manageable. If not, the material will expose the gap quickly. In real production, that is the difference between a route that stays profitable and one that keeps looking more expensive every hour it runs.