Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
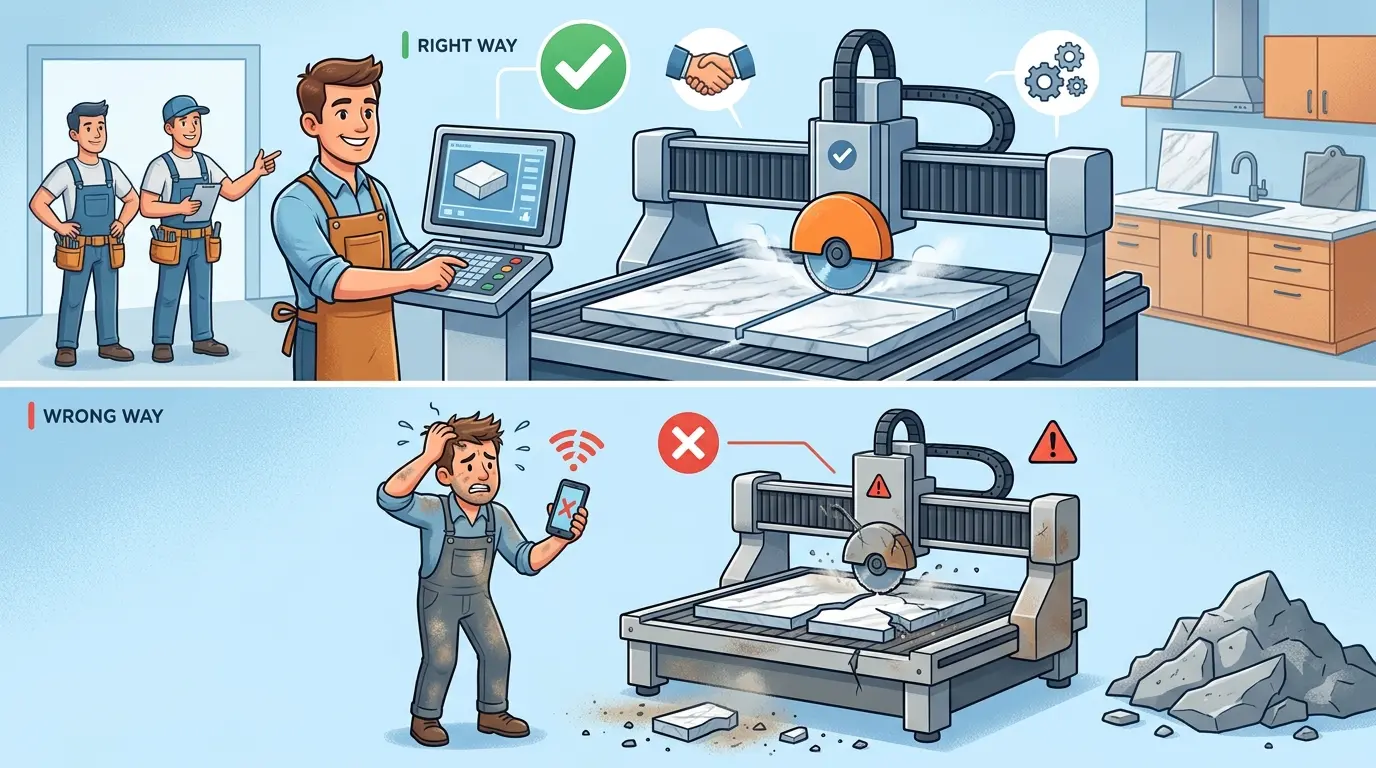
Stone shops routinely buy CNC equipment by comparing feature lists and demo cycle times, yet the real failure begins earlier: the production constraint is never defined. Edge profiles needing hand correction, inconsistent sink cutouts, or output tied to one experienced operator are the actual losses driving automation—but category labels and showcase samples often replace that analysis. Before any specification sheet matters, the buying team must map where time, labor, and material are lost daily, then match the machine to the dominant job mix, material behavior, and finishing flow. Otherwise, a technically capable center becomes an expensive detour that moves problems downstream faster instead of removing them.
Why Stone Shops Buy the Wrong CNC Machine
The buying conversation for stone CNC equipment usually starts with the wrong question. A shop owner sees a machine cutting a complex sink profile at a trade show, watches a polished demo part come off the table, and begins comparing feature lists and quoted cycle times. That approach feels productive, but it skips the step that determines whether the investment pays off: defining the actual production problem the machine is expected to solve.
Stone fabrication is not a single process. A shop running repeated quartz countertop production faces different constraints than one handling mixed natural-stone vanity work or architectural cladding components. The machine that solves one shop’s bottleneck can become another shop’s expensive storage platform. Before any specification sheet gets serious attention, the buying team needs to identify where time, labor, and material are actually being lost in the current workflow.
Mistake 1: Buying a Machine Category Instead of Solving a Production Constraint
Most stone shops do not wake up one morning and decide they need a CNC router. They wake up because edge profiles require too much hand correction, sink cutouts vary from part to part, or experienced operators are spending their shifts repositioning and rechecking work instead of producing. The decision to automate usually follows a pattern of repeated waste, but the buying conversation often drifts away from that pattern.
When buyers start with a category label instead of a measurable constraint, they tend to compare machines that may not address the real loss point. A shop whose primary problem is inconsistent edge profiles needs a different configuration focus than one whose problem is slow throughput on repeated countertop blanks. The machine category is the same, but the selection criteria are not.
The practical way to start is to list the specific failures that occur on a weekly basis:
- Edge profiles that still need significant hand correction after machining
- Sink or cooktop cutouts that vary enough to create fit problems at installation
- Operators spending excessive time repositioning parts or rechecking dimensions
- Parts reaching polishing with avoidable inconsistency in surface or edge condition
- Output that depends heavily on one or two experienced operators who cannot be absent without slowing production
If these problems appear daily, a CNC investment is likely justified. If they are occasional or poorly documented, the machine purchase becomes a solution in search of a problem. The discipline of defining the loss point first—rework, slow throughput, inconsistent profiles, unstable handoff to polishing, or installation-related variation—keeps the buying process grounded in production reality.
Mistake 2: Buying for Maximum Capability Instead of Daily Job Mix
Stone shops rarely run one type of work indefinitely. Some are built around repeated countertop production with predictable part sizes and profiles. Others handle a mixed stream of vanity tops, islands, cutouts, wall cladding pieces, and custom architectural details that change frequently. A machine that looks impressive in a broad demonstration may still be poorly matched to the work that actually fills the shop schedule.
The selection logic should follow the revenue pattern. A shop producing repeated quartz countertops for residential projects needs stable routing, consistent profile output, and dependable throughput that feeds the finishing line without surprises. A shop handling mixed custom work needs flexibility across changing part sizes, quick program changes, and the ability to handle irregular geometries without excessive setup time.
| Daily Work Pattern | What Buying Focus Usually Matters Most | Common Buying Risk |
|---|---|---|
| Repeated Countertop Production | Stable routing, profile consistency, and smooth movement into finishing | Paying for complexity while the real need is dependable daily throughput |
| Mixed Custom Kitchen and Vanity Work | Flexibility across changing part sizes and regular program changes | Buying around one showcase application instead of the full job mix |
| Granite-Heavy or More Demanding Stone Work | Stable output under tougher machining conditions and consistent finish preparation | Judging the purchase by ideal samples instead of everyday production conditions |
| Decorative or Architectural Components | Shape complexity, contour repeatability, and good downstream finishing coordination | Choosing a machine that fits straight work better than the complex parts that create margin |
This does not mean buyers should ignore growth plans. It means growth assumptions should be realistic. If the shop expects more custom work or a higher visual finish standard, the machine choice should support that direction. But buying for a hypothetical future production model that never materializes is just as risky as buying only for today’s constraints. The machine should fit the work that pays the bills now, with enough margin to handle realistic evolution.
Mistake 3: Ignoring Material Mix and Finish Standards
Stone fabrication decisions are never only about geometry. Material behavior matters in ways that affect workflow, finishing load, and tolerance for error. Quartz, granite, marble, and engineered materials do not place identical demands on the machining process or the downstream finishing team. Buyers who talk about “stone” as though it is one uniform processing category often miss the selection logic that matters most.
Quartz countertop production typically involves consistent slab dimensions, predictable material behavior, and a finish standard that customers inspect closely at the edge profile. Granite work often involves harder material, more variation in slab condition, and a different set of handling challenges. Marble and softer natural stones require careful attention to edge breakout and surface integrity. A machine configuration that handles one material family well may struggle with another.
When evaluating stone CNC machines, the conversation should stay tied to the materials processed most often and the finish quality customers actually expect. A shop producing polished quartz kitchen tops for repeat residential projects is making a different buying decision from one producing varied natural-stone vanity work or architectural pieces where visual detail and edge presentation carry more weight.
The practical questions are straightforward:
- Which stone types dominate the order book?
- Which parts require the tightest visual and dimensional consistency?
- How much hand polishing or edge correction happens after machining today?
- Are customers buying functional fit first, premium finish first, or both?
When buyers skip these questions, they often end up with a machine that is technically usable but commercially misaligned. The equipment may run, but the finishing team carries more correction work than expected, or the shop discovers that the machine’s strength is concentrated in a narrow slice of actual production.
Mistake 4: Treating the CNC Center as a Standalone Solution
One of the most common buying errors is assuming the machine itself will automatically solve a broader workflow problem. In practice, stone CNC performance depends heavily on everything around it: drawing preparation, slab staging, part identification, operator handoff, edge finishing, polishing flow, inspection, and packing or installation preparation.
A CNC machine removes material according to a program. It does not fix a shop where drawings are incomplete, slabs are staged inconsistently, or parts move into finishing without clear identification. If the surrounding process remains chaotic, the machine may simply push problems downstream faster. Shops sometimes invest in better machining but leave the same confusion in job preparation, batch tracking, or finishing coordination. The disappointing result comes not because the machine category is wrong, but because the workflow around it was never tightened.
The buying review should cover the full process, not only the machining stage. Buyers should check how the machine fits into questions such as:
- How drawings, templates, or part programs reach production
- How stone slabs or parts are staged before machining
- How operators keep repeated jobs organized during busy production periods
- How parts move from machining into edge finishing or polishing
- How quality is confirmed before parts leave for assembly or installation
If these surrounding steps remain inconsistent, the CNC center cannot deliver its full value. The machine’s output is only as useful as the process that feeds it and the process that receives it.
Mistake 5: Overlooking Slab Handling, Layout, and Shop Flow
Stone parts are not light, easy to reposition, or forgiving when traffic patterns are poor. A machine can be well chosen in principle and still underperform because the surrounding floor layout makes material movement awkward, slow, or risky. Slab handling is often the hidden constraint in stone fabrication, and it becomes more visible once a CNC machine is introduced.
Before buying, review the machine in relation to the physical flow of material through the shop:
- Infeed and outfeed space around the machine
- Slab staging discipline before machining
- How finished parts leave the CNC area
- Whether operators can keep parts separated by job without confusion
- How close the CNC process sits to finishing, inspection, and packing
Stone fabrication loses time in handling just as easily as it loses time in machining. If operators spend too much effort repositioning work, clearing pathways, or searching for the next part in sequence, the machine will not deliver the workflow gains buyers expect. Layout fit is especially important when the shop is trying to improve throughput without expanding floor space at the same rate. A machine that requires extensive material movement across the shop may create new bottlenecks even as it solves the original machining problem.
Mistake 6: Underestimating Tooling, Maintenance, and Daily Process Discipline
Some buyers evaluate a machine as though its best performance is permanent. In reality, stone processing quality depends on routine discipline as much as on the initial purchase. Tooling condition, setup habits, inspection routines, and maintenance consistency all affect whether the machine keeps delivering stable output over time.
Stone tooling wears. Diamond tooling in particular degrades in ways that affect edge quality and surface finish long before the tool becomes visibly damaged. A shop that does not track tooling hours or replacement intervals will see quality drift gradually, often blaming the machine for problems that are really tooling management issues.
The buying decision should never stop at “Can this machine produce a good sample part?” The real question is whether the shop can sustain good output every week without falling back into correction-heavy habits. Areas that deserve attention before buying include:
- How the shop manages tooling condition and replacement timing
- Whether operators follow consistent setup and checking routines
- How quality drift is detected before rework builds up
- Whether maintenance discipline is strong enough to protect daily repeatability
- How much output quality depends on one skilled operator not being absent
When buyers ignore these factors, they sometimes blame the machine for problems that are really process problems. A capable CNC system cannot protect production results if the shop has weak daily control over the conditions that affect consistency. The machine amplifies the discipline of the process around it; it does not replace that discipline.
Mistake 7: Comparing Cycle Time but Ignoring Total Cost of Poor Fit
Headline speed is easy to compare. Production fit is harder. That is why shops often overemphasize cycle-related claims while underestimating the hidden cost of manual finishing, scrap, job confusion, inconsistent fit, and installation-related correction.
A machine that cuts a sink profile 20 percent faster but produces edges that require more hand finishing may not actually save time. A machine that is cheaper to purchase but requires more operator attention, more rework, or more downstream correction can become more expensive in daily operation. The comparison that matters is not the machine in isolation; it is the machine’s contribution to the complete production flow.
| What Buyers Often Compare First | What They Should Compare Instead | Why It Matters |
|---|---|---|
| Headline machining speed | Total parts released to finishing without rework | Output only helps if downstream teams can use it cleanly |
| Purchase price alone | Combined cost of scrap, hand correction, and delays | A cheaper machine can become more expensive in daily operation |
| One good demo sample | Repeatable quality across regular production | Factories run shifts and batches, not isolated showcase parts |
| Machine capability in isolation | Full workflow time from staging to ready-to-finish part | Real productivity depends on the complete process, not one step |
Return on investment in stone fabrication usually comes from better workflow behavior: more stable profiles, smoother finishing preparation, less avoidable manual correction, more predictable handoff, and fewer downstream surprises. Buyers who judge the investment only by cycle time often miss the variables that affect profit more directly.
Questions to Answer Before You Buy
Before committing to stone CNC equipment, pressure-test the decision with a few operational questions. These questions should be answered by the people who run production daily, not only by ownership or sales staff:
- What exact production problem are we trying to remove?
- Which material types and part categories dominate our real workload?
- How much manual finishing or correction are we trying to reduce?
- Will the machine fit the way parts move through the shop today?
- Are we buying for repeat countertop flow, mixed custom work, architectural detail work, or a realistic combination?
- Can our team support the machine with stable programming, tooling, maintenance, and inspection discipline?
- Will this purchase reduce downstream friction, or will it only move the same problems to the next department faster?
These questions usually reveal whether the investment is grounded in workflow logic or in equipment excitement. The difference matters because stone CNC equipment is most valuable when it removes repeated production waste, not when it simply adds technical capability on paper.
Selection Focus: Common Mistakes When Buying Stone CNC Equipment
The biggest mistakes in buying stone CNC equipment usually come from weak problem definition, poor workflow analysis, and feature-led comparison. Shops get into trouble when they buy for the brochure instead of the bottleneck, ignore material and finish requirements, overlook slab handling and finishing flow, or assume the machine can fix weak process discipline on its own.
The better buying approach is practical: define the daily production loss, match the equipment to the real mix of stone work, evaluate how the machine fits the full fabrication sequence, and judge the investment by repeatable output rather than isolated claims. When that fit is real, stone CNC equipment helps protect profile consistency, reduce rework, and make fabrication more stable. When the fit is weak, even a capable machine can become an expensive detour that adds technical capability without adding production value.