Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
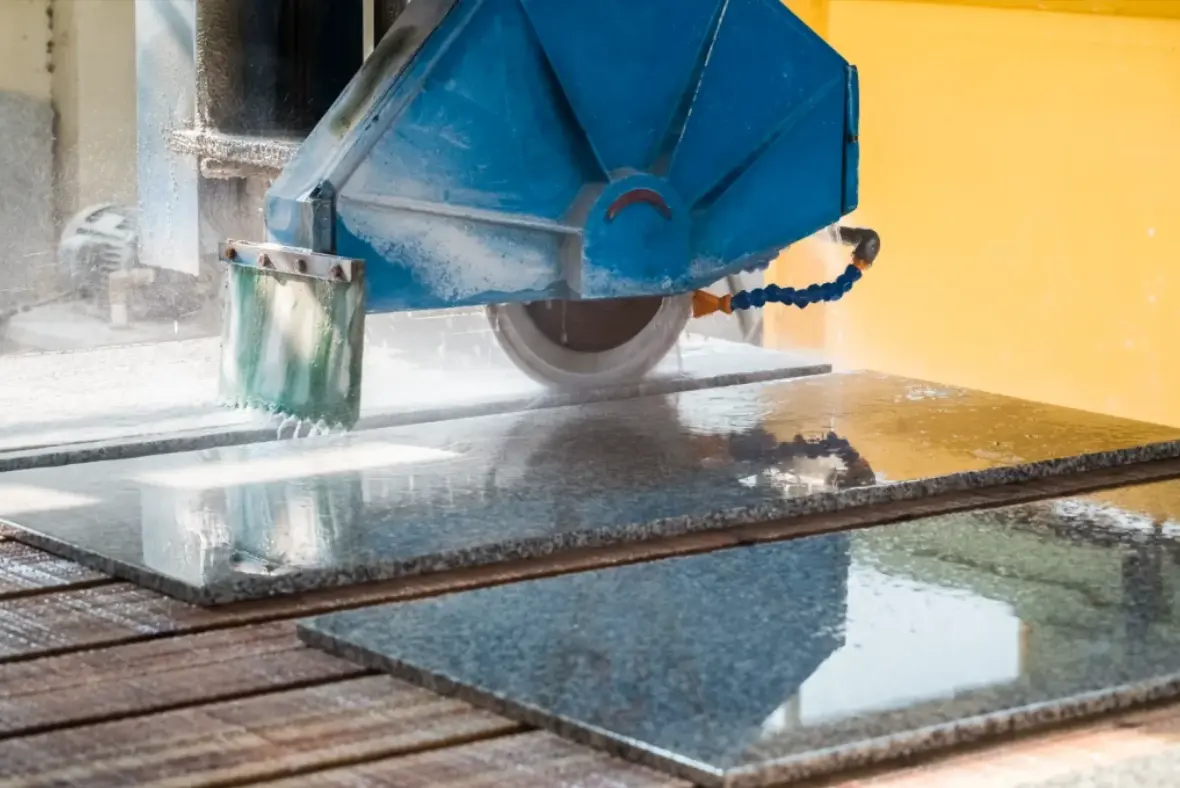
Before comparing spindle power or axis counts, custom stone shops must first identify the production bottleneck that a CNC purchase is meant to solve. Inconsistent sink cutouts, excessive hand correction on edges, slow changeovers between quartz, marble, and granite jobs, and rework that surfaces only during polishing or installation are the real constraints that justify the investment. A machine that fails to hold reference stability across varying part geometries or that cannot absorb daily job variation will simply shift the bottleneck downstream. Match the machine to the workflow you actually run, not to the capability you imagine needing.
Start With the Bottleneck, Not the Machine
Most shops begin a stone CNC purchase by comparing machine capability in the abstract—spindle power, axis count, travel dimensions, advertised feed rates. That usually starts the wrong conversation. The better starting point is the problem the machine must solve in daily production, because a CNC machine is a process-control investment, not a capability trophy.
In custom fabrication, the recurring problems are usually specific: inconsistent sink and hob cutout accuracy, excessive hand correction on edges and profiles, repeated layout and re-referencing between operations, slow changeovers between one custom job and the next, difficulty keeping quartz, marble, and granite work consistent across different operators, and rework that only appears during polishing, assembly, or installation.
If those are the real constraints, a stone CNC machine is justified because it improves process control. If the main issue is slab handling, templating quality, or final polishing discipline, then a machine upgrade alone will not solve the problem. Buying a CNC to fix a templating problem is an expensive way to learn that the bottleneck moved rather than disappeared.
Custom Fabrication Changes the Buying Criteria
Custom stone work is not repetitive straight-line production. A shop producing one countertop program after another with varying sink positions, edge details, and part geometries needs more than raw cutting capacity. It needs a machine workflow that absorbs variation without turning every job change into a setup problem.
That changes the buying criteria in practical ways. In a custom environment, the machine should deliver reliable referencing from one operation to the next, repeatable edge profiles across different jobs, cleaner changeovers between programs and part types, better control of openings, radii, and shaped features, and less dependence on manual marking and correction.
Consider a typical week in a custom shop. Monday brings a quartz island with a curved profile and an undermount sink. Tuesday runs three granite vanity tops with standard edges but different cutout positions. Wednesday introduces a marble backsplash with decorative edge work. Each job demands different toolpaths, different clamping strategies, and different quality expectations. The machine that handles this mix well is not necessarily the one with the highest spindle rating—it is the one that lets the operator move from job to job without re-establishing reference points, re-teaching tool offsets, or manually verifying every dimension.
This is why the best machine for custom fabrication is not automatically the most complex one. It is the one that matches the level of variation your shop actually handles while keeping the workflow stable. A five-axis machine with every optional spindle is wasted capability if your job mix is 80 percent standard countertops with sink cutouts. Conversely, a basic three-axis router will frustrate a shop that regularly produces shaped edges, carved details, or multi-plane profiles.
Match the Machine to the Work You Actually Run
Stone shops use the phrase “custom fabrication” to describe very different production realities. One business may mainly produce kitchen countertops with frequent sink cutouts. Another may focus on vanities, stairs, wall panels, or reception pieces with more edge and shape variation. A third may handle a mix of architectural and decorative work where detail quality matters more than sheer output.
Those differences matter because the machine should be judged by application fit, not by general capability claims.
| Fabrication Scenario | What Usually Matters Most | Why It Changes the Buying Decision |
|---|---|---|
| Countertops with frequent cutouts | Opening accuracy, edge repeatability, and less manual correction | Errors become expensive when parts move to finishing and installation |
| Vanities, islands, and bar tops | Flexible profile work and stable referencing on shaped parts | Visual quality and fit often matter as much as raw throughput |
| Stair treads, wall panels, and architectural components | Dimensional consistency across batches and repeatable edges | Installation quality depends on parts arriving predictable and aligned |
| Decorative or detailed custom work | Controlled shaping, carving, and finish preparation | Detail variation quickly increases manual labor if the process is unstable |
| Mostly straightforward parts with limited shape variation | Efficient routing and edging without unnecessary workflow complexity | A more advanced configuration is harder to justify if the work stays simple |
The honest question is not whether the machine can do more. It is whether your shop regularly needs more. Buying well means matching capability to the job mix you expect to run most often, not to the one impressive project you landed last quarter. A machine that can carve intricate 3D reliefs is impressive, but if that work appears twice a year, you are paying for capability that sits idle while the machine handles the same sink cutouts a simpler configuration could manage.
Workflow Fit Matters More Than Headline Specifications
For custom fabrication, the buying mistake that shows up most often is treating the machine as an isolated asset. In reality, the CNC step sits between templating, material preparation, edge finishing, polishing, quality control, and installation release. If those handoffs are weak, a machine that looks strong on paper may still underperform on the shop floor.
That is why workflow fit usually matters more than any single headline specification. Buyers should look closely at how the machine supports the production sequence around it.
What usually matters most includes how the part is referenced when machining starts, how easily that reference can be maintained through routing, profiling, and detail work, how much manual repositioning is still required between steps, how clearly jobs can be released, checked, and changed over, and how well the machine supports downstream edge finishing and polishing rather than creating more correction work.
The stronger the workflow fit, the more likely the machine will improve practical outcomes: cleaner openings and profiles, better repeatability between similar jobs, less hand rework before polishing, smoother part fit during installation, and more predictable daily throughput.
Let us trace a typical part through the workflow. A granite countertop arrives from the templating stage with a digital template or a physical pattern. The operator loads the slab, references the part position, and runs the cutout program. If the machine holds that reference reliably, the sink opening is accurate to the template, and the edge profile is consistent along the entire length. The part moves to polishing with minimal hand correction. If the reference drifts—because of table flex, spindle deflection, or poor vacuum hold-down—the operator catches the error during inspection, and the part goes back for correction or, worse, is scrapped.
The difference between these two outcomes is rarely visible in a specification sheet. It shows up in how the machine handles the physical realities of stone: slab weight, vibration, tool wear, and the need for stable workholding across varying part geometries.
Evaluate Material Mix and Finish Expectations Honestly
Quartz, marble, and granite do not behave the same during routing, edging, and finishing. A machine that fits one material mix well may be less ideal if your shop often shifts between harder materials, more delicate natural stone appearance standards, or jobs that demand more refined visual detail.
Granite is dense and abrasive. It wears tooling faster, generates more heat during cutting, and demands rigid machine construction to avoid chatter and deflection. Marble is softer but more prone to chipping and edge breakout, especially on thin profiles or intricate details. Quartz is engineered and relatively consistent, but it can be sensitive to feed rates and spindle speeds—too aggressive a cut can burn the resin binder or produce a rough edge that requires extensive hand finishing.
That does not mean the machine choice should be based on one material alone. It means buyers should evaluate the machine in the context of the full mix they process most often.
Questions worth clarifying include whether the shop is primarily focused on quartz countertops or frequently switches between quartz, marble, and granite; whether edge profiles are mostly standardized or change often from job to job; whether the business wins most of its work on fit-critical kitchen and vanity projects or on decorative and architectural pieces where detail variation is higher; how much hand finishing is still acceptable after CNC processing; and where visible quality matters most—edge shape, opening precision, surface transition, or final installation fit.
These questions help define whether the machine needs to support a broad custom workflow or a more concentrated production model. A shop that runs granite and marble in equal measure needs different spindle and tooling considerations than one that runs quartz almost exclusively. Granite-heavy shops should prioritize rigidity and dust extraction, because granite cutting produces fine, abrasive dust that can shorten the life of linear guides, bearings, and electrical components if the machine is not properly sealed and ventilated. Marble-heavy shops should focus on edge quality and chip control, because marble’s tendency to fracture at edges makes tool geometry and feed control critical.
When a Stone CNC Machine Adds More Value Than a Fragmented Process
In some shops, stone fabrication is still split across several loosely connected stages, with manual marking, repeated repositioning, and separate correction work between operations. That approach can still work for low-volume or simpler jobs, but it becomes harder to control as custom complexity rises.
Consider the manual workflow for a sink cutout. The operator lays out the opening with a template, marks the corners, drills starter holes, and cuts with a handheld router or bridge saw. The process depends on the operator’s skill, the accuracy of the template, and the stability of the handheld tool. Any variation in these factors produces an opening that is slightly off, requiring hand grinding or filler to correct. Multiply that by every sink, every edge profile, and every shaped detail in a custom job, and the cumulative labor cost becomes significant.
A CNC-centered workflow changes the equation. The cutout is programmed once, the toolpath is verified in software, and the machine executes it consistently. The operator’s role shifts from executing the cut to preparing the job and monitoring the process. That shift does not eliminate the need for skilled labor—it redirects it toward job preparation, tooling selection, and quality verification, where it has more leverage.
| Workflow Approach | Strong Fit | Main Advantage | Main Tradeoff |
|---|---|---|---|
| Stone CNC-centered workflow | Custom shops that need routing, profiling, and detail work to stay more repeatable | Better process consistency and fewer reference resets across custom parts | Requires stronger job preparation and process discipline |
| More fragmented manual workflow | Lower-volume work with simpler geometry or occasional shaped jobs | Flexible and often easier to adjust on the spot | More operator-dependent and usually harder to scale cleanly |
The point is not that one method is always better. A CNC-centered workflow becomes more attractive when the cost of inconsistency, hand correction, and repeated setup is already visible in the business. If you are tracking rework hours per job, you already know whether this threshold has been crossed. If you are not tracking rework, start now—the data will tell you more about your process than any machine specification will.
Buying Factors That Usually Matter Most
Before committing, it helps to compare options against the realities of your own production model. The table below organizes the factors that consistently separate good stone CNC purchases from poor ones.
| Buying Factor | Why It Matters in Custom Fabrication | What to Clarify Internally |
|---|---|---|
| Job variation | High variation changes the value of programmability and setup control | Are most jobs similar, or does geometry change every day? |
| Part complexity | Cutouts, shaped edges, and decorative details increase process sensitivity | How much of your work goes beyond simple straight geometry? |
| Reference stability | Multi-step custom work depends on parts staying aligned from operation to operation | Where do fit problems usually begin today? |
| Rework rate | Rework is often the clearest sign that the current process is under-controlled | How often are parts corrected before release or installation? |
| Labor dependency | Heavy reliance on individual operator judgment makes growth harder to manage | Is quality process-driven or person-driven? |
| Changeover burden | Frequent program changes can quietly limit real throughput | How much time is lost between custom jobs? |
| Finish standard | Higher visual requirements raise the cost of weak edge and profile consistency | What level of correction is still acceptable after machining? |
| Future business direction | The best choice should fit both current work and likely growth | Is the shop moving toward more volume, more customization, or both? |
Factories that answer these questions clearly usually make better decisions than factories that compare only machine complexity or generalized productivity claims. The table above is worth filling out with your own numbers before you talk to any supplier.
Failure Modes to Screen Before Buying a Stone CNC Machine for Custom Fabrication
Even experienced buyers can misread what custom fabrication really demands. The most common mistakes usually look like this: buying for maximum capability when most jobs are still operationally simple; comparing machines without mapping how parts actually move through the shop; ignoring where rework appears downstream in polishing or installation; underestimating the importance of job preparation and program control; and assuming the machine will fix process problems created by weak templating, poor handling, or inconsistent finishing.
The best buying process treats the CNC machine as one part of a controlled fabrication system, not as a standalone answer to every production problem. If your templating process produces inaccurate templates, the CNC will faithfully machine the wrong geometry. If your operators do not understand toolpath programming, the machine will sit idle while jobs wait for programs. If your polishing stage is understaffed, the CNC will simply feed more parts into a bottleneck.
Another common mistake is overlooking the physical installation requirements. Stone CNC machines are heavy, require stable foundations, and generate significant dust and noise. Shops that do not plan for compressed air capacity, dust collection, electrical supply, and floor reinforcement may find that the machine’s real cost extends well beyond the purchase price. A machine that cannot run at full capacity because the shop lacks adequate dust extraction is a machine that is not earning its keep.
Questions to Ask Before You Commit
Before making the investment, pressure-test the decision with a few direct questions. Are we buying to improve cutout accuracy, profile repeatability, labor efficiency, or overall workflow control? Which operation currently creates the most expensive rework? How often do custom jobs force manual repositioning or correction? Is our material mix stable enough to standardize more of the process? Can the shop support better job preparation and program management once the machine is installed? Will the machine remove a real bottleneck, or just shift it to another stage?
If the answers point to repeatable custom geometry, too much manual correction, and rising pressure on fit and finish quality, the case for a stone CNC machine becomes much clearer. If the answers are vague or the rework data is not tracked, spend a few weeks measuring before you buy. Track rework hours per job, time spent on manual correction, and the frequency of fit problems during installation. That data will either confirm the investment or reveal that the real problem lies elsewhere in the process.
Selection Focus: a Stone CNC Machine for Custom Fabrication
Choosing a stone CNC machine for custom fabrication is really about choosing how the shop wants to control variation. The strongest fit usually appears when the business needs more repeatable routing, edge shaping, cutout accuracy, and finish preparation across a changing mix of quartz, marble, and granite work.
If most jobs are still simple, low-volume, and easy to manage through a more manual process, a more advanced CNC workflow may be harder to justify. But when custom work is already exposing the cost of weak referencing, hand correction, and inconsistent quality, a stone CNC machine can help turn custom fabrication into a more stable and scalable process.
The decision ultimately comes down to matching the machine to the work you actually run, not the work you imagine running. Evaluate your job mix honestly, map your workflow from templating to installation, track your rework data, and compare machines against the specific constraints those realities create. Review the stone CNC machines available and compare them against the workflow criteria above before making a decision. A machine that fits your process will pay for itself in reduced rework, faster changeovers, and more consistent quality. A machine that does not fit will become another bottleneck.