Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
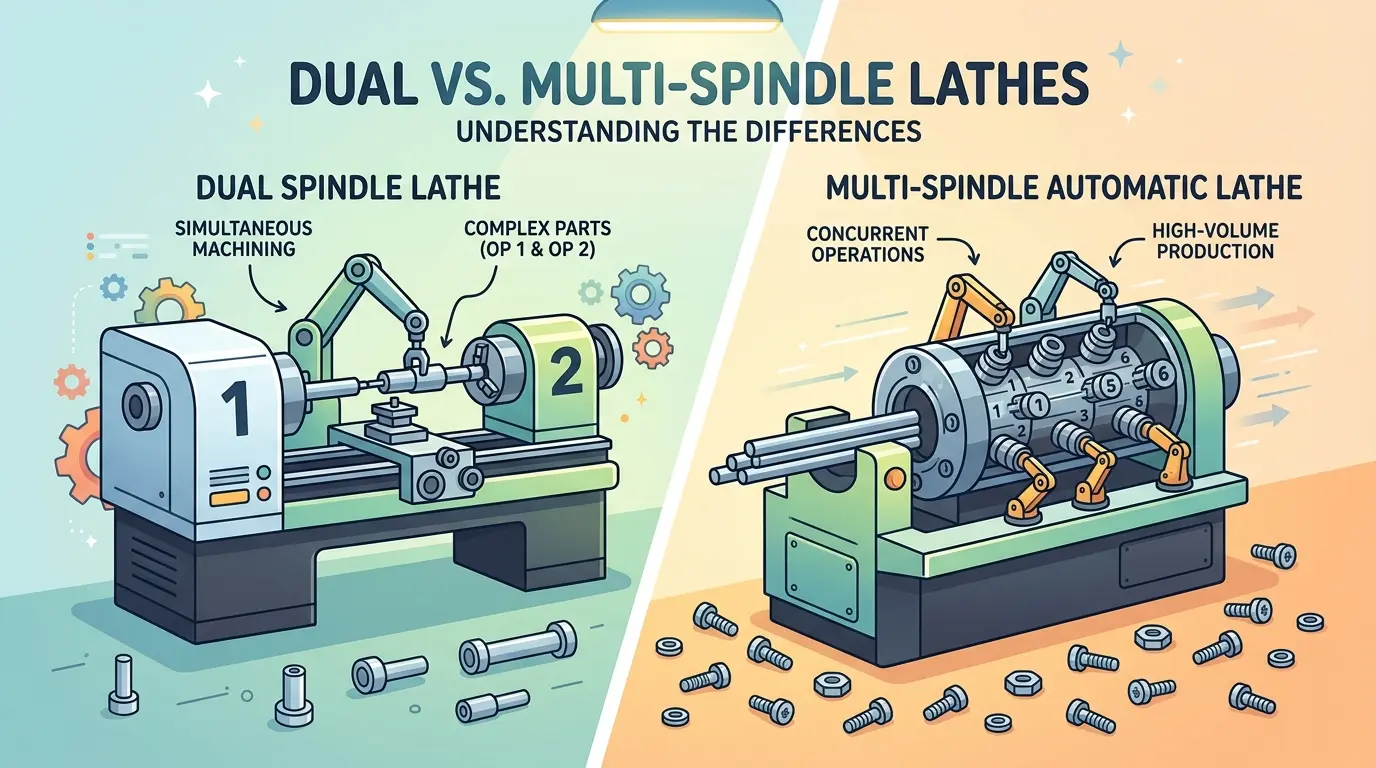
Comparing a dual-spindle lathe to a multi-spindle automatic by counting spindles will misdirect your capital decision. These machine classes solve opposite production problems: one integrates front-and-back operations to eliminate transfers and re-chucking, while the other compresses stable, high-volume part families into a dense sequential cycle. Before evaluating any equipment, you must locate your real bottleneck. If daily pain comes from handling, queue time, and inconsistent second-side work, dual-spindle logic wins. If output limitation on repeated parts is the constraint, multi-spindle automation justifies its setup commitment.
Match Spindle Configuration to the Production Pattern
When shops start comparing turning equipment, the number of spindles often becomes the headline spec. It is easy to see why. A dual-spindle lathe and a multi-spindle automatic both have more than one spindle, so the assumption follows that both are simply ways to get more parts out the door. That assumption is wrong, and it leads to expensive mistakes.
The two machine classes solve different production problems. A dual-spindle lathe is primarily a process integration tool. It keeps more of the part’s work inside one controlled environment, reducing transfers and re-chucking on parts that need front-and-back or staged operations. A multi-spindle automatic lathe is an output density tool. It compresses very high volumes of stable, repeating parts into a tightly sequenced cycle across multiple spindle stations.
The correct comparison is not about spindle count. It is about which kind of productivity your shop actually needs.
Route Integration Versus Output Density
Think of the decision in terms of two distinct production goals. The first goal is route integration: keeping the part inside one machine environment for as much of its turning work as possible. The second goal is output density: maximizing the number of identical parts produced per unit of time through specialized sequencing.
Dual-spindle lathes excel at the first. They allow a part to move from first-side machining to second-side machining without leaving the machine, without a manual transfer, and without the alignment risk that comes with re-chucking. That makes them valuable for shops running moderate volumes of parts that require more than one turning stage.
Multi-spindle automatic lathes excel at the second. They are built around a fixed sequence of operations distributed across multiple spindle positions. Each station performs a specific cut while the next part indexes forward. The result is a continuous, dense production flow that is extremely efficient when the part family is stable and volumes are high.
Neither approach is universally superior. A shop with frequent changeovers and a mixed order book will likely get more real value from dual-spindle equipment, even if a multi-spindle automatic looks more impressive in a brochure. A shop dedicated to long-running components will quickly find that a dual-spindle platform cannot match the output density of a properly set up multi-spindle automatic.
The question to ask is not “which machine is more advanced?” It is “where is the actual bottleneck in my turning operation?” If the bottleneck is too many transfers, too much re-chucking, and inconsistent second-side work, dual-spindle logic addresses it directly. If the bottleneck is sheer output on stable repeated parts, multi-spindle automatic logic is the more meaningful answer.
Dual-Spindle Lathes: Completing the Part Without Breaking the Route
The core value of a dual-spindle lathe is continuity. A part moves through more of its required operations inside one controlled machine environment instead of leaving the first spindle for manual transfer, a second chucking setup, or a separate turning stage. That continuity matters for several reasons.
First, it reduces labor. Every manual transfer is operator time that could be spent elsewhere. Every re-chucking is an opportunity for error. Second, it reduces queue time. Parts that would otherwise wait between first-side and second-side operations move through in one sequence. Work-in-process drops, and internal lead time shortens. Third, it improves consistency. When feature relationships are established in one setup, the risk of misalignment between operations drops significantly.
This is why dual-spindle logic appeals to shops producing repeated turned components that are not necessarily extreme high-volume parts but still benefit from a cleaner route. The machine supports more complete processing of each part before it leaves the turning environment.
The key distinction is that dual-spindle systems are about route completion, not raw multiplication of output. They become attractive when the part is complex enough to benefit from integration but not repetitive enough to justify the deeper specialization of multi-spindle automatic equipment.
Multi-Spindle Automatics: Built Around Stable Repetition
Multi-spindle automatic lathes belong in a different production conversation. Their value appears when the part family is stable, the quantity is high, and the economics reward a machine designed to cycle through operations at very high density. The machine is not doing more of the same turning in a flexible way. It is built around a specialized production structure.
That structure compresses time around a repeating part family. Multiple spindles hold multiple workpieces simultaneously, each at a different stage of the machining sequence. While one spindle is being loaded, another is being drilled, another is being turned, and another is being cut off. The result is a continuous flow of finished parts with minimal idle time.
But that structure demands commitment. Setup justification, tooling strategy, part stability, and process planning must all support the machine’s production logic. If part mix is highly variable or order volumes are too low, the automatic multi-spindle route becomes much harder to justify economically.
Buyers should treat multi-spindle automatic equipment as volume-first equipment. It is strongest when the business already knows that output density is the real commercial lever and that the part family is stable enough to reward specialization.
Order Book Analysis Drives the Decision
The best machine comparisons begin with the order book, not the brochure. Ask these questions before evaluating any equipment:
- What parts dominate the order book?
- How often do they repeat?
- How stable is annual demand?
- How much of the business depends on one or a few high-volume families?
- Is the current pain in handling and incomplete turning routes, or in sheer output limitation on stable repeated parts?
If the pain is mostly in handling, transfers, and front/back operations, dual-spindle logic makes sense. If the pain is mostly in output limitation on stable repeated parts, multi-spindle automatic logic becomes more compelling.
This is where many mistakes become visible. Buyers sometimes like the idea of multi-spindle output while their real order pattern still behaves like a flexible dual-spindle environment. Others stay on more flexible turning logic too long even though their stable volume has already crossed into a different economic case.
Setup Economics Are Not Equal Between the Two Classes
All turning equipment requires setup, but the economic weight of setup is not the same in these two classes. Dual-spindle machines usually make sense across a wider range of repeated moderate-volume work because the route retains more flexibility. Changeovers are less disruptive because the machine is not built around a highly specialized sequence.
Multi-spindle automatic lathes become truly attractive when their setup, tooling, and process commitment can be spread across enough production volume to justify that specialization. The theoretical output is high, but it is only realized when the machine stays in its rhythm long enough for the setup investment to pay back strongly.
That does not mean multi-spindle machines are impractical. It means they want the right business conditions. If the shop changes over too often or if volumes are not high enough, the machine’s theoretical output can be undermined by the cost and complexity of adapting too frequently.
Buyers should ask not only whether the machine can make the part, but whether their order pattern can economically support the way the machine wants to make it.
Front-End and Back-End Operations Are a Bigger Deal Than Many Buyers Admit
One reason dual-spindle machines often feel so valuable is that they solve a practical production frustration that does not always show up cleanly in brochures: what happens between first-side and second-side work. Manual transfer, queue time, re-chucking, and alignment risk all add labor, delay, and variability. A dual-spindle route addresses that by keeping more of the part journey inside one controlled turning environment.
This is different from the multi-spindle automatic value proposition. Multi-spindle machines are less about reducing awkward mid-route handling on moderate-volume jobs and more about keeping a highly repetitive production flow dense and fast. These are different operating pains, and buyers should not blur them together.
If second-side work and transfer discipline are your daily headache, dual-spindle logic deserves very serious attention.
Quality Logic Follows the Architecture
More spindles do not automatically mean better parts. Quality still depends on tooling, workholding, setup control, and how well the route protects critical relationships. A dual-spindle lathe may improve quality by reducing transfer variation and preserving feature relationships across stages. A multi-spindle automatic may improve consistency by stabilizing a very repetitive route. Both gains are real, but both come from process logic, not from spindle count by itself.
Buyers should not use spindle count as a proxy for quality. Instead, ask how the machine architecture reduces the specific sources of variation the current route suffers from. If transfer error is the issue, dual-spindle integration may help most. If cycle density and long-run repetition are the issue, multi-spindle automation may help most.
Inspection planning should follow the architecture. The machine choice changes where risk is removed and where the shop must still pay attention.
Tooling Strategy: Flexible Versus Committed
Tooling choices exist on both machine types, but the economic meaning is different. On dual-spindle lathes, tooling strategy supports an integrated but still comparatively flexible route. The shop can adapt to part changes without rethinking the entire machine setup.
On multi-spindle automatic lathes, tooling strategy is more deeply tied to the economics of output density. Once the route is established, the machine is most valuable when it stays in that rhythm long enough for the setup investment to pay back strongly.
That difference matters because some shops underestimate how much organizational discipline multi-spindle automatic systems require. The machine may be correct, but the company may not yet be commercially organized around the kind of stability that lets it win. That is not a technical problem. It is a business-model problem.
Buyers should examine not only whether the machine fits the part, but whether the company fits the machine.
The Same Part Drawing Can Lead to Different Rational Choices
Two shops can make the same turned part and still choose different machines rationally because their business models differ. One may be a mixed shop that wins work through responsiveness across several related part families. Another may run a narrow stable program where very high output is the dominant commercial advantage.
The part drawing alone does not always decide the answer. The order pattern does too.
If the shop sells responsiveness and integrated route control across many similar components, dual-spindle logic aligns with that commercial truth. If the shop sells output density on a narrower family of stable parts, multi-spindle automatic logic aligns better.
Many Shops Step to Dual-Spindle First
In practice, many businesses do not choose between these machines at the same maturity stage. Dual-spindle lathes are often a transitional improvement that helps the shop reduce handling, increase part completeness, and stabilize more of the route before its order book becomes narrow and dense enough to justify multi-spindle automatic capacity.
That sequence is not mandatory, but it is common for a reason. It mirrors how many businesses actually mature. First they need better integrated turning. Later they may need much denser output on a smaller family of repeated parts.
Understanding that progression helps buyers avoid buying too far ahead of their real order pattern.
Ask Whether Your Bottleneck Lives in Handling or in Density
This is the single most useful decision question. If your daily pain comes from front/back operations, part transfers, re-chucking, queue delays, and incomplete turning routes, dual-spindle logic is usually the stronger answer. If your daily pain comes from not being able to produce enough of the same parts quickly enough, and the volume is stable enough to justify a specialized route, multi-spindle automatic equipment becomes much more interesting.
This question works because it forces buyers to identify the real source of lost capacity instead of assuming the answer must be “more spindles.” Often, the real answer is “the right kind of spindle architecture for the kind of production problem we actually have.”
Secondary Operations Often Decide the Value
Many buyers compare these machines through turning cycle logic alone and overlook what happens outside the machine. If the current route creates queue time before second-side work, requires extra handling before deburring or inspection, or sends parts into secondary operations with unnecessary variation, dual-spindle integration can create value far beyond the spindle transfer itself. The part leaves the machine more complete, and that often simplifies the rest of the route.
This matters especially in shops where the commercial pain is not only machine time but flow disruption. A dual-spindle machine can reduce work-in-process buildup, shorten internal lead time, and make downstream scheduling easier because more of the part is finished in one controlled sequence. That is why some buyers choose it even when its theoretical output density is lower than a multi-spindle automatic. The real gain is not just spindle utilization. It is a cleaner route across the whole part lifecycle.
Buying Output Density Too Early Is a Real Risk
There is also a timing issue in this decision. Shops sometimes become fascinated by the output promise of multi-spindle automatic lathes before their order book is actually ready for that specialization. The result can be an impressive machine whose economics remain underused because the business is still too mixed, too changeable, or too dependent on moderate-volume families rather than a few dense, stable programs.
That is why the smarter comparison is partly developmental. What stage is the business in? Is it still rewarded mainly for flexibility and integrated route control, or has it truly crossed into a high-density production environment where specialization pays back strongly? A shop that answers that question honestly usually avoids buying far ahead of its real commercial position.
The Smarter Choice Follows the Production Pattern
A dual-spindle lathe and a multi-spindle automatic lathe do not solve the same turning problem. Dual-spindle machines are about completing more of the part in one controlled route and reducing transfers on moderate-volume repeated work. Multi-spindle automatic lathes are about extremely high output on stable part families where specialized sequential spindle logic pays back strongly.
The correct choice comes from understanding whether your real bottleneck is route integration or output density. If you need more complete turning without excessive handoffs, dual-spindle logic often makes more sense. If you need far greater production density on highly repeated parts, multi-spindle automatic equipment deserves the stronger look.
The right machine is the one that matches the production pattern your business actually lives with every day.