
 Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
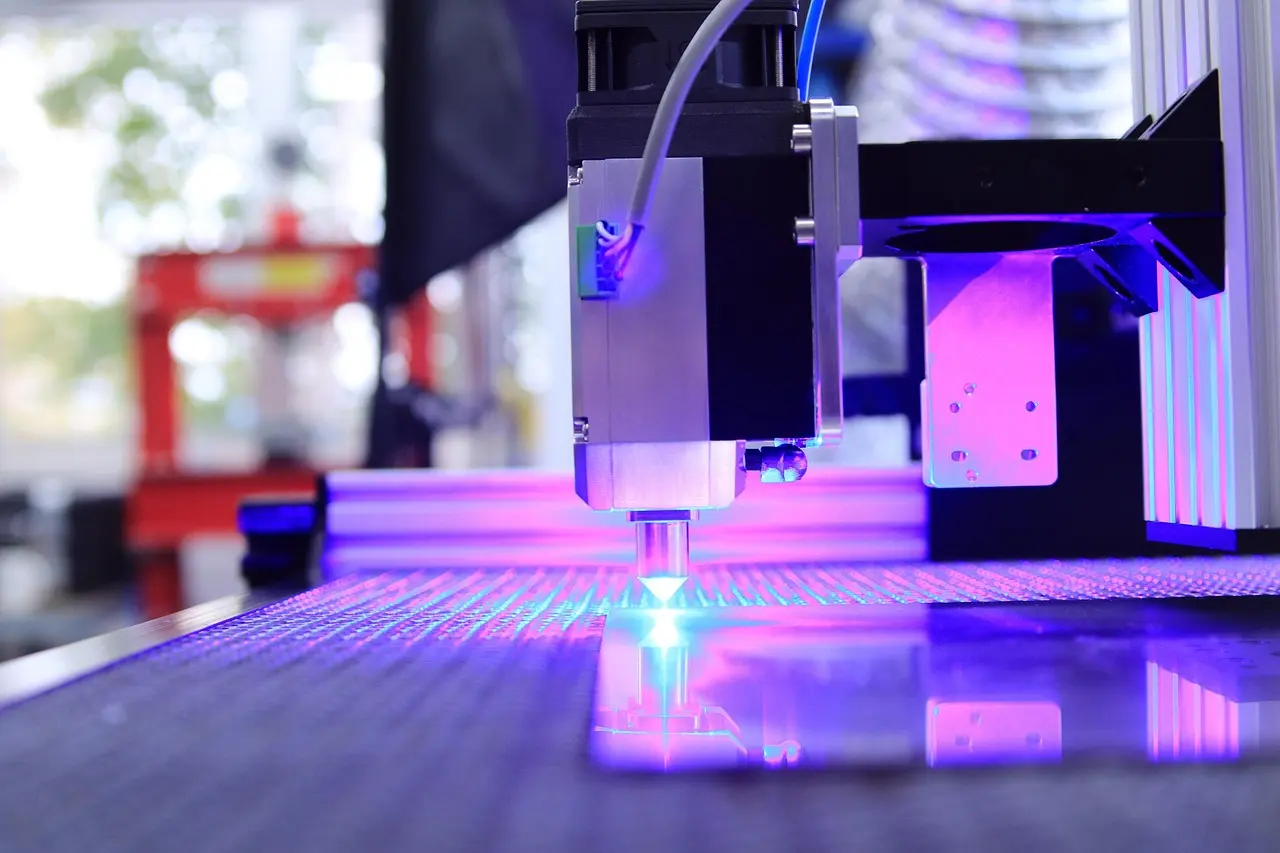
Precision failures in fiber laser engraving rarely trace back to the laser source itself; they originate in part presentation, surface condition, focus stability, and verification methods—variables entirely within the buyer’s control. A flawless demo on a polished stainless coupon tells you nothing about daily performance when machined brackets arrive with height variation, residual coolant, or mixed finishes. Before committing capital, you must distinguish traceability codes from cosmetic marks and fine detail from bold fixture IDs, because each stresses beam control and fixturing differently. Test actual parts, real variable-data changes, and your own inspection standard, or you risk buying a machine that generates rework instead of traceability.
Precision Problems Usually Start Outside the Laser Source
Many production teams assume that accuracy in fiber laser engraving is primarily a question of source power. The logic seems straightforward: more watts should mean cleaner marks, finer detail, and better consistency. In practice, precision failures in metal marking rarely originate at the laser source itself. They begin with part presentation, surface condition, focus stability, data handling, and verification methods—all of which sit outside the laser head and most of which are entirely within the buyer’s control.
A machine can produce a flawless sample on a polished stainless coupon during a vendor demonstration and still struggle in daily production when parts arrive with slight height variation, inconsistent surface finish, inadequate fixturing, or dense variable data that changes every cycle. The gap between demo performance and production performance is where most precision problems actually live. Understanding that gap before you commit capital is the difference between a marking cell that delivers traceability and one that generates rework.
This is especially true in metal work because parts are often smaller, harder, more reflective, or more varied than buyers expect during early evaluation. A machined bracket with a milled surface behaves differently under the beam than a laser-cut blank with a scaled edge. A polished nameplate reflects energy differently than a blasted housing. A part that arrives with residual coolant or oil changes absorption characteristics. A good trial should therefore test the full process: actual parts, actual code sizes, realistic loading conditions, and the same inspection standard the factory will use later. Anything less is a marketing exercise, not an engineering evaluation.
What Buyers Usually Mean by Precision Metal Work
The term “precision metal work” covers several distinct jobs, and each one stresses the process in a different way. Treating them as a single application category leads to poor machine selection and disappointed operators.
| Precision Work Type | Typical Parts | What Precision Usually Means | Common Failure Mode |
|---|---|---|---|
| Traceability Marking | Machined parts, brackets, housings, fabricated components | Readable codes, stable placement, reliable scanner performance | A mark looks acceptable visually but fails verification or drifts off location |
| Tool And Fixture Identification | Jigs, holders, gauges, dies, maintenance-critical items | Durable text in limited space, repeatable positioning | Marks are readable on large tools but inconsistent on smaller items |
| Cosmetic Product Identification | Metal panels, visible housings, nameplates, branded components | Clean line quality, crisp edges, consistent appearance | Heat tint, uneven fill, or line softness reduces finish quality |
| Fine Detail On Small Parts | Connectors, compact assemblies, precision hardware, miniature components | Small text clarity, narrow line control, minimal distortion | Spot size or fixturing inconsistency destroys small-feature readability |
This distinction matters because the best setup for a bold fixture ID on a large die block is not automatically the best setup for tiny machine-readable codes on a connector housing. The beam parameters, scan strategy, and fixturing requirements differ substantially. A buyer who evaluates only one application type and assumes the machine will handle the others equally well is setting up for a costly surprise.
Consider the practical differences. Traceability marking on a machined bracket typically requires a Data Matrix code that a scanner can read reliably under shop-floor lighting. The code must be placed within a defined location tolerance so that downstream vision systems can find it. The mark must survive subsequent handling, possibly washing or coating. Cosmetic marking on a visible housing, by contrast, demands uniform fill, sharp edges, and no heat tint—appearance criteria that may conflict with the higher energy density needed for deep, durable codes. Fine detail on small parts pushes the process toward smaller spot sizes and tighter focus control, which in turn makes focus stability and part height variation more critical.
The Variables That Actually Drive Accuracy
The strongest buying decisions come from testing the variables that control the result, not just the mark visibility. A machine that produces a beautiful mark on a perfectly flat, clean, stationary sample may fail entirely when parts arrive with burrs, residual oil, or dimensional variation from the previous machining step.
| Variable | Why It Matters in Real Production | What To Check During Evaluation |
|---|---|---|
| Beam Control And Spot Quality | Fine text and dense codes depend on controlled line width, not just raw output | Test the smallest real feature size your workflow requires |
| Focus Stability | Minor height changes can reduce mark sharpness faster than buyers expect | Run trials across actual part tolerances, not ideal flat samples |
| Fixturing And Part Presentation | If parts land differently every cycle, the mark position will drift even when the laser is stable | Evaluate workholding, repeat loading, and operator variation |
| Surface Condition | Polished, coated, blasted, anodized, and raw surfaces can behave very differently | Separate trials by surface type instead of grouping all metals together |
| Scan Strategy And Software Flow | Precision depends on path logic, fill pattern, and variable-data handling as much as on the source itself | Test real serial-number changes, code generation, and layout updates |
| Verification Method | A visually sharp mark is not always a production-ready mark | Use the same scanner, gauge, or inspection standard the line will use later |
One of the most common mistakes is to approve the machine based on a good-looking stationary sample and postpone workflow testing until after purchase. That usually reverses the real order of risk. The laser source is the most standardized component in the system. The variables that differentiate production success from failure are the ones that interact with your specific parts, your specific operators, and your specific inspection criteria.
Take focus stability as an example. A fiber laser with a short focal length produces a small spot size, which is excellent for fine detail. But the depth of field is correspondingly shallow. If your parts arrive with a height variation of even a fraction of a millimeter—from machining tolerances, deburring variation, or fixture wear—the mark sharpness will degrade across the batch. A machine with a longer focal length may produce a slightly larger spot but hold acceptable quality across a wider height range. The right choice depends on your part variation, not on the brochure specification.
Surface condition presents a similar challenge. Polished stainless steel reflects a significant portion of the beam energy, requiring different parameters than a blasted or coated surface. Anodized aluminum absorbs differently than raw aluminum. If your plant runs mixed materials and finishes through the same station, the machine must handle parameter switching cleanly and repeatably. A machine that excels on one surface type but requires extensive manual tuning for others will create bottlenecks and inconsistency.
Why Workflow Fit Matters as Much as Mark Quality
In precision metal work, a laser station does not operate in isolation. It sits inside a sequence that may include machining, deburring, washing, coating, assembly, inspection, and packing. If the marking step cannot keep pace with that flow, the accuracy advantage on paper may not translate into better output. A marking cell that produces perfect codes but requires 30 seconds of manual positioning per part will throttle an entire production line.
This is why buyers should ask a broader set of questions before committing to a machine. Will the operator load parts manually or through a fixture? Does the code content change every cycle, requiring variable-data input from a database or PLC? Is the mark verified immediately after marking, or only later in the line? Do different alloys or finishes run through the same station in the same shift? A machine that performs well on a single repetitive part may require a different setup discipline when the plant runs mixed batches with frequent changeovers.
Consider a typical scenario in a job shop that produces machined components for multiple customers. Each customer may require a different marking format: one wants a Data Matrix code with a serial number, another wants a logo and part number, a third wants a date code in a specific location. The laser station must handle these variations without excessive setup time or operator error. The software interface becomes as important as the beam quality. If changing from one job to the next requires manual parameter entry across multiple screens, the risk of error increases and the effective throughput drops.
For many factories, the real return from a fiber laser engraving investment comes from reducing remarking, preventing mix-ups, and making inspection faster. That means the best machine is often the one that keeps mark quality stable under normal production variation, not the one that only produces the most impressive demo sample. A mark that fails verification downstream creates a cascade of costs: the part must be quarantined, re-marked or scrapped, the process must be investigated, and the production schedule is disrupted. These costs far exceed the price difference between a marginal machine and a well-matched one.
When Fiber Laser Engraving Is Commonly a Strong Fit
Fiber laser systems are commonly chosen for precision metal work when the application calls for:
- Permanent identification on metal parts that must survive handling, washing, or mild abrasion
- Fine text or compact machine-readable codes that must remain legible at small sizes
- Durable tool, fixture, or component marking where labels or ink would not survive
- Variable data marking in high-mix production where code content changes every cycle
- Clean, controlled marks on small or accuracy-sensitive components where heat input must be minimized
That fit becomes stronger when the factory values repeatability, low-contact processing, and clear traceability without relying on labels or secondary marking steps. Fiber lasers offer several practical advantages in these applications. They produce a small, consistent spot size that supports fine detail. They operate at wavelengths that metals absorb well, reducing the energy required for a given mark depth. They have no consumables like ink or engraving bits, which simplifies maintenance and reduces operating cost. And they can be integrated into automated cells with relative ease, since the marking head can be mounted on a gantry, robot arm, or fixed frame.
The permanence of the mark is another factor that drives fiber laser adoption. A laser-engraved Data Matrix code on a stainless steel housing will survive years of service, temperature cycling, and exposure to industrial fluids. Labels peel, ink fades, and dot-peen marks can be shallow or inconsistent. For industries with strict traceability requirements—aerospace, medical devices, automotive, defense—the permanence and repeatability of laser marking often justify the investment on its own.
Many manufacturers reviewing this kind of investment also compare it against broader equipment priorities across the plant. In that context, the Pandaxis product catalog can serve as a general reference point for wider machinery planning, even when the laser decision itself still needs application-specific validation. The key is to evaluate the laser marking cell as part of a production system, not as an isolated purchase.
Where the Tradeoffs Still Remain
Fiber laser engraving is not a universal answer for every metal-marking problem. Buyers should define the limits early and understand where the technology requires compromise.
| Requirement or Constraint | Practical Tradeoff |
|---|---|
| Very Deep Engraving | Deeper results usually increase cycle time and process sensitivity |
| Highly Reflective or Mixed Surface Conditions | Process windows can narrow, making stable day-to-day setup more important |
| Thin Or Heat-Sensitive Parts | Excess energy or poor tuning can affect appearance faster than expected |
| Large Filled Graphics | Throughput pressure may shift from detail control toward total mark time |
| Irregular Or Hard-To-Locate Parts | Fixturing and presentation may matter more than the laser head itself |
Deep engraving is a common point of confusion. If the application requires a mark that can be felt with a fingernail—for example, a tool identification mark that must survive aggressive handling—the laser must remove more material. This increases cycle time, generates more heat, and narrows the process window. A mark that is perfectly readable but only 0.01 mm deep may be entirely adequate for traceability but unacceptable for a toolroom that expects a visible, tactile identification.
Highly reflective surfaces present another challenge. Copper, brass, and polished aluminum reflect a significant portion of the beam energy at fiber laser wavelengths. This does not make marking impossible, but it narrows the parameter window and increases sensitivity to focus and surface condition. A machine that marks stainless steel effortlessly may require careful tuning and consistent part presentation to achieve the same result on brass. If your production mix includes reflective materials, the evaluation must include those materials specifically.
Thin or heat-sensitive parts require careful energy management. A thin-walled aluminum housing can distort or discolor if the laser parameters are too aggressive. The operator must balance mark visibility against heat input, which often means multiple passes at lower power rather than a single high-energy pass. This increases cycle time and requires more process discipline. A machine with good parameter presets and repeatable behavior makes this balancing act easier, but it does not eliminate the fundamental tradeoff.
Large filled graphics—logos, warning labels, or decorative markings—shift the bottleneck from detail control to total mark time. A 50 mm square filled logo at high density may take several seconds to complete, which can throttle a high-volume line. Buyers should calculate the total mark time for their largest required graphic and compare it against the cycle time budget for the production cell. If the mark time is excessive, the options are to reduce the fill density, increase the spot size, or accept a longer cycle.
Questions To Resolve Before You Buy
The following questions will help separate a precision problem from a throughput problem or a workflow-discipline problem. The correct machine choice depends on which one is dominant.
- What is the real mark objective: readability, appearance, permanence, or depth? These criteria can conflict, and the priority determines the machine configuration.
- Which metal surfaces will run daily, and how much do they vary? A machine that handles one surface type well may struggle with mixed finishes.
- What is the smallest text, code, or graphic the factory must hold consistently? This defines the required spot size and focus stability.
- Is the real bottleneck mark time, part loading, fixturing, or verification? A fast laser with slow fixturing is still a slow cell.
- Will the station run repetitive batches or frequent variable-data changes? High-mix production demands software flexibility and parameter presets.
- Can the trial be run on actual production parts under normal setup conditions? A demo on polished coupons proves nothing about your process.
These questions usually reveal whether the buyer is solving a precision problem, a throughput problem, or a workflow-discipline problem. The better choice follows from the task that consumes the most machine time, not from the broader label. A precision problem demands attention to beam control, focus stability, and fixturing. A throughput problem demands attention to scan speed, part handling, and software automation. A workflow-discipline problem demands attention to operator training, parameter management, and verification procedures. Buying a more powerful laser will not solve any of these if the root cause lies elsewhere.
Production Takeaway: Fiber Laser Engraving Machine for Precision Metal Work
A fiber laser engraving machine can be a strong fit for precision metal work when the factory needs small-feature clarity, stable positioning, durable part identification, and repeatable results across real production variation. The technology is mature, the operating cost is low, and the integration path is well understood. But the most important point is that accuracy does not come from the laser source alone. It comes from the combined performance of beam control, focus consistency, fixturing, surface management, data handling, and verification.
The safest buying logic is straightforward: define what precision means for the actual part, test that requirement under production conditions, and choose the system that protects mark quality without creating a new bottleneck elsewhere in the workflow. Run trials on your parts, with your operators, using your inspection standard. Measure the mark quality across a batch, not just on a single sample. Calculate the total cycle time including loading and verification. And be honest about whether the application is truly precision marking or whether it is a different machine-class question entirely.
If the real production goal is metal cutting rather than high-clarity identification or shallow engraving, that is a different machine-class question and should be evaluated on a different basis. Fiber laser engraving and fiber laser cutting share a wavelength but diverge in power, optics, and process requirements. Confusing the two leads to undersized cutting systems or oversized marking systems, both of which waste capital.
For manufacturers who are still mapping their equipment strategy, the Pandaxis product catalog provides a useful reference for comparing machinery categories and understanding how a marking cell fits into a broader production plan. The laser decision itself, however, must be driven by application-specific validation on your actual parts. A machine that looks impressive in a demo hall may not survive contact with your production floor. A machine that performs reliably across your real part variation, your real operators, and your real inspection criteria is the one that will deliver the return you are projecting.