Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
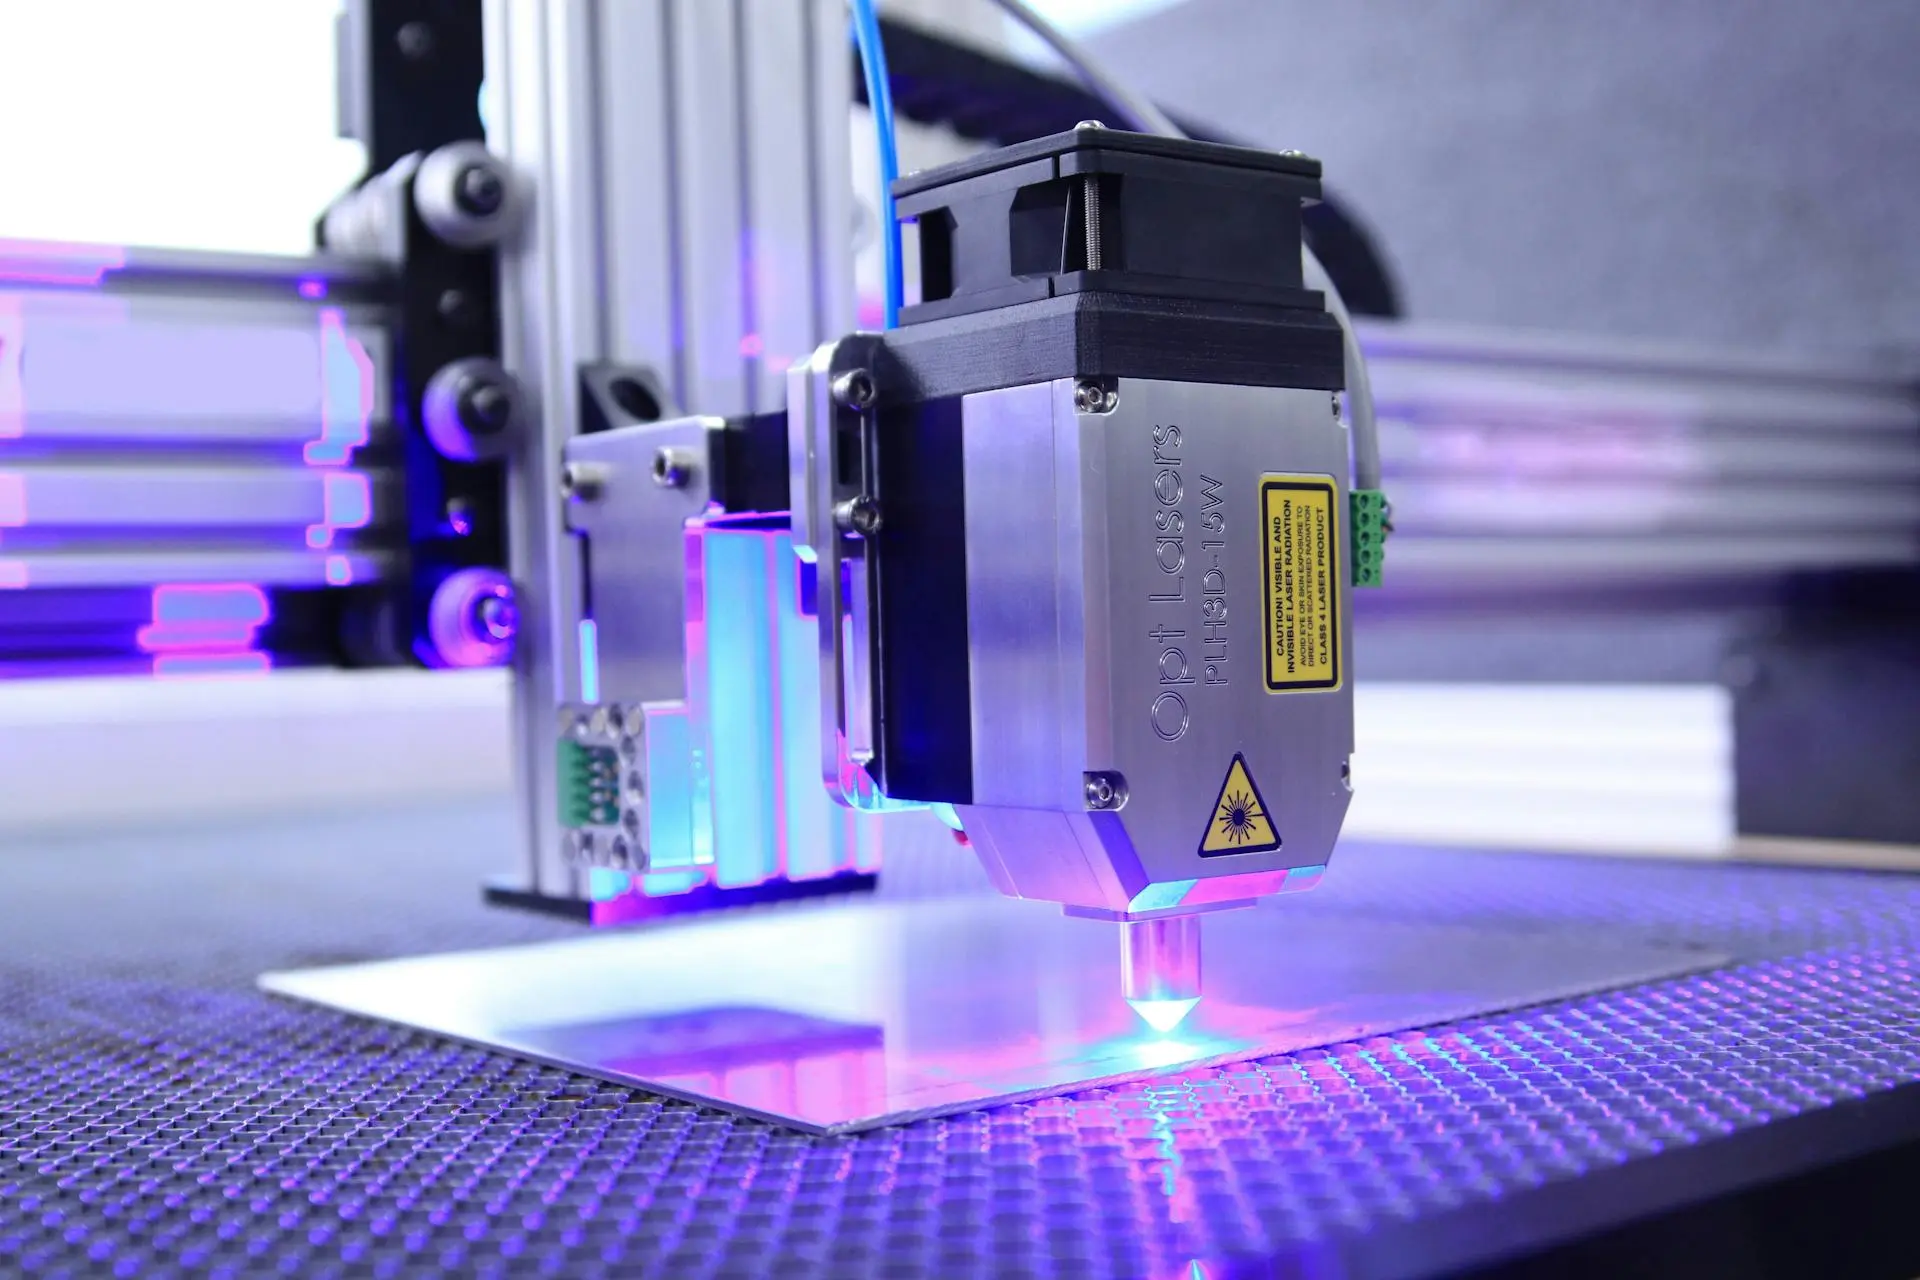
Adding glass engraving to a shop floor usually fails not at the laser source but at the material interface: glass looks forgiving yet punishes assumptions about support, recipe stability, and finish variation. This article addresses the real production problem of treating glass like wood or acrylic, which generates scrap, rework, and quoting errors before the first run completes. For buyers evaluating laser cutters for non-metal workflows, the decision hinges on accepting that glass engraving is a controlled surface-frosting process, not a deep-removal operation. Understanding that distinction early determines whether you invest in fixturing, recipe documentation, and inspection disciplineâor absorb the cost of broken parts and cosmetic rejects.
Why Glass Engraving Demands a Different Production Mindset
When a shop adds glass engraving to its workflow, the first surprise is usually not the machine. It is the material. Glass looks forgiving from across the room, but it punishes assumptions. A laser can mark a clean frosted logo on a flat panel in one pass, then chip or crack the next piece because the support surface had a slight wobble or the recipe was tuned for a different coating. That gap between what the machine can do and what the process actually delivers is where most production problems start.
For buyers evaluating laser cutters and engravers for glass and other non-metal workflows, the distinction matters early. Glass engraving is usually a controlled surface-marking process, not a deep-removal process. The workflow has to be built around that reality. Shops that treat glass like acrylic or wood will generate scrap, rework, and customer complaints that have nothing to do with the machine’s capability.
What a Glass Engraving Machine Actually Does in Production
In most laser-based workflows, glass engraving means creating a frosted or matte surface effect that makes text, logos, patterns, or graphics visible. The laser interacts with the glass surface to create micro-fractures and surface disruption that scatter light, producing the characteristic white or frosted appearance. That is useful because the process is non-contact and can produce fine detail, but it also means buyers should not judge success by depth alone.
The practical reality is that glass engraving is strongest when the production goal is:
- Decorative surface contrast that reads clearly under normal lighting
- Clean branding or logo placement on customer-visible surfaces
- Readable text or batch identification for traceability
- Repeatable graphic detail on finished pieces across multiple runs
- Short-run artwork changes without mechanical tool changes or mask preparation
That is very different from a workflow that needs heavy texture, deep carving, or edge shaping. Those are separate process decisions and should not be treated as automatic outcomes of the same machine. A shop that needs deep tactile engraving on thick glass panels is asking for a different process envelope than one that needs consistent frosted logos on drinkware.
Best Use Cases for Glass Engraving
The best glass engraving applications are usually the ones where surface appearance matters more than aggressive material removal. When the customer judges the part by how it looks under showroom lighting, laser engraving has a clear advantage over mechanical methods that risk chipping or stress fractures.
| Use Case | Why Laser Engraving Fits | What Buyers Should Watch Closely |
|---|---|---|
| Branded Drinkware and Giftware | Supports logos, names, and decorative marks without direct tool contact, preserving the structural integrity of thin-walled glassware | Curved surfaces require careful fixturing; cosmetic consistency across batches depends on recipe stability and part positioning |
| Awards and Presentation Pieces | Produces a clean frosted effect for text and graphics on customer-visible surfaces with fine detail that reads as premium | Reject cost is higher because minor defects are easy to see on polished surfaces; sampling is essential before committing to a run |
| Decorative Glass Panels and Inserts | Helps create repeatable patterns, branding, or accent graphics on flat parts without the setup time of masking and sandblasting | Large filled areas can expose uneven visual density if the recipe is unstable; power and speed settings need to be validated for each glass type |
| Identification on Finished Glass Components | Useful for readable part marks, batch information, or simple traceability fields on components that will be assembled into larger products | Mark strength must match the actual readability requirement rather than a deeper-is-better assumption; over-engraving can weaken thin sections |
| Mixed Non-Metal Production With Occasional Glass Jobs | Makes sense when the same shop already runs wood, acrylic, or similar decorative work and wants to expand service offerings | Process discipline has to tighten when switching from forgiving materials to brittle glass; operators need clear changeover procedures |
In all of these use cases, the value comes from appearance, repeatability, and flexibility. If the job is judged mainly by deep texture or structural shaping, another process may fit better. The buyer who understands this distinction before purchasing will avoid the disappointment that comes from expecting a surface-marking tool to behave like a carving tool.
Where the Limits Show Up Fast
Glass engraving becomes expensive when buyers expect the process to behave like deep carving or like a broadly tolerant marking method across every glass type and shape. The limits are not hidden; they show up in the first production run if the setup is wrong.
The most common limits are straightforward:
- Most laser glass engraving is surface frosting, not deep engraving; the mark typically has minimal measurable depth
- Thin, stressed, or edge-damaged parts can carry higher breakage risk because the laser introduces localized thermal stress
- Curved surfaces make support and consistent mark appearance harder; the focal distance changes across the part
- Different glass finishes and treatments can respond differently; coated, tempered, and annealed glass are not interchangeable
- Large solid fills may be less forgiving than small text or line art because heat accumulation varies across the engraved area
These are not minor details. They change quoting, fixturing, recipe approval, and scrap risk. A shop that quotes a job based on a sample made from one glass type and then receives a different finish from the customer will discover that the recipe needs adjustment, and that adjustment takes time and test pieces.
| Limitation | What It Means in Production | Why It Matters |
|---|---|---|
| Limited Depth Expectation | The result is commonly a visible frosted mark rather than a deep cavity; the effect is optical, not physical | Prevents the wrong process promise during quoting; customers need to see a sample before approving a design |
| Glass Fragility | Small support or handling mistakes can turn acceptable samples into batch rejects; thermal stress from the laser adds to existing stress in the material | Raises the cost of poor fixturing and rushed setup; a broken part mid-run interrupts production and wastes material |
| Variation by Part Type | Flat stock, coated pieces, and curved products may not react the same way; even clear glass from different suppliers can behave differently | Forces recipe separation instead of one generic setup; operators need documented settings for each part family |
| Visible Cosmetic Standards | Even slight inconsistency can be obvious on premium glass products; the human eye is very good at spotting uneven frosting | Makes quality control more visual and less forgiving; inspection criteria need to be defined before production, not after rejects appear |
| Edge Sensitivity | Existing chips or stress near the edge can raise reject risk; the laser can turn a small defect into a visible crack | Means part condition matters before engraving even begins; incoming inspection is part of the process, not an optional step |
This is why strong shops treat glass engraving as a controlled finishing process rather than as a generic “mark-anything” operation. They document recipes, inspect incoming parts, and validate samples before committing to a run. That discipline is what separates shops that make money on glass engraving from shops that lose money on it.
Material Tips That Reduce Rejects
Most glass engraving problems do not begin at the file stage. They begin with part condition, support, and unrealistic finish expectations. Operators who focus on the artwork first and the material second will generate more scrap than those who reverse the priority.
The most useful material-handling habits are usually simple:
- Separate recipes by glass type, finish, and part geometry; do not assume one setting works for all clear glass
- Clean the surface before running customer-visible work; fingerprints, dust, and residue can create uneven marking
- Support the part evenly so it does not rock or twist during the job; a stable platform is the foundation of consistent focus
- Keep critical artwork away from pre-chipped or visibly weak edges; the laser can propagate existing damage
- Test one approved sample when a new batch or finish is introduced; supplier variation is real and predictable
- Define the required look early: light frosting, stronger contrast, or decorative fill; the customer’s expectation drives the recipe
- Protect the finished surface during post-process handling and packing; a perfect engraving is worthless if the part gets scratched in transit
Those steps matter because glass defects are often blamed on the machine when the real cause sits upstream in setup, batch variation, or handling. A shop that blames the laser for a crack that started at a pre-existing chip will never fix the actual problem.
One more point matters for material planning: glass is not automatically interchangeable just because the parts look similar on a shelf. Clear stock, treated surfaces, and decorative finishes can respond differently enough that recipe discipline should be tied to the actual part type, not to the general word “glass.” A shop that engraves drinkware, flat panels, and awards needs three recipe families at minimum, and likely more once supplier variation is factored in.
Process Control and Recipe Development for Glass
Recipe development for glass engraving is not a one-time activity. It is an ongoing process that follows the material as suppliers change formulations, coatings, and finishes. Shops that treat recipes as permanent documents will eventually be surprised by a batch that behaves differently.
The practical approach is to build a recipe library organized by part family. Each entry should record:
- Glass type, thickness, and finish or coating
- Laser power, speed, and frequency settings
- Focal distance and lens configuration
- Expected visual result: light frost, medium contrast, or heavy fill
- Date of validation and the sample part used for approval
This documentation serves two purposes. First, it gives operators a reliable starting point when a repeat order arrives. Second, it creates a baseline for troubleshooting when a batch behaves differently. If the same recipe produces a different result, the variable is likely in the material, not the machine.
For shops that run mixed non-metal production, the changeover between materials is where discipline matters most. An operator who has been cutting acrylic all morning cannot assume the same focus and power settings will work on glass. The changeover procedure should include a test piece, a visual inspection, and a sign-off before production begins. That adds a few minutes to the setup but prevents a batch of rejects that would take hours to recover from.
When Laser Makes Sense and When Another Process May Fit Better
Laser engraving is not the only way to decorate or mark glass. Buyers usually get better results when they compare the workflow need rather than forcing one technology into every job. The wrong buying decision often starts with the wrong expectation, so it is worth laying out the options side by side.
| Process | Strongest Fit | Main Advantage | Main Limitation |
|---|---|---|---|
| Laser Engraving | Fine detail, short-run graphics, variable artwork, and non-contact surface marking on flat or gently curved parts | Fast artwork changes and clean digital workflow control; no masking or abrasive media to manage | Usually produces a frosted surface effect rather than deep texture; depth is limited and inconsistent across glass types |
| Sandblasting | Broader matte fields or stronger textured effects on flat panels and larger surfaces | More aggressive surface effect on the right jobs; can produce a deeper, more tactile result | Masking, cleanup, and process labor are usually heavier; fine detail is harder to control than with laser |
| Printing or Coating-Based Decoration | Color graphics and repeated visual layouts where full-color output is required | Supports visual variety and repeated image output without surface disruption | Does not create an engraved surface and follows different durability expectations; the mark sits on top of the glass rather than in it |
That comparison is useful because the wrong buying decision often starts with the wrong expectation. If the goal is premium frosted branding, readable detail, and fast artwork changes, laser engraving can be a practical fit. If the goal is deeper texture or a different visual finish altogether, a separate decoration method may deserve the lead role.
What Buyers Should Evaluate Before Choosing a Machine
Before comparing demonstrations or quotes, it helps to answer a few operational questions clearly. These questions matter more than generic feature language because glass engraving performance depends heavily on process control, part handling, and finish expectations.
- Are most jobs flat panels, curved pieces, or a mix? The answer determines whether a flat-bed machine with a fixed focus is sufficient or whether rotary attachment and adjustable focus are required
- Is the main goal decorative branding, fine text, or basic identification? Each goal has different tolerance for contrast variation and mark consistency
- How expensive is one broken or cosmetically rejected part? High-value parts justify more investment in fixturing and process validation
- Will glass be a dedicated workflow or an occasional part of a mixed-material queue? Mixed production requires changeover discipline and recipe management
- Does the shop need frequent artwork changes without long setup delays? Laser engraving excels here, but only if the workflow is set up to support it
- Is the customer expectation a light frosted finish or a more visually aggressive effect? The answer determines whether laser is the right process at all
A machine that fits the real part mix and supports repeatable setup will usually outperform a broader machine claim that ignores reject risk. Buyers who answer these questions before shopping will make better decisions on machine size, lens configuration, rotary options, and extraction requirements.
Shop-Floor Integration and Workflow Planning
Glass engraving does not exist in isolation. It sits between incoming material inspection, part preparation, and post-process handling. Shops that plan the full workflow before installing the machine will have a smoother start than those that plug in the laser and start experimenting.
The workflow should include:
- Incoming inspection: check for chips, cracks, and surface defects before parts enter the engraving queue
- Cleaning: remove dust, fingerprints, and residue that can affect mark consistency
- Fixturing: select the appropriate support for the part geometry; flat parts need a level bed, curved parts need a rotary or custom cradle
- Recipe selection: pull the documented settings for the specific glass type and finish
- Test piece: run a small sample when the batch or finish is new; inspect it under the same lighting the customer will use
- Production run: monitor the first few parts for consistency before letting the run proceed unattended
- Post-process handling: protect the engraved surface during packing and shipping; the mark is part of the product, not an afterthought
This sequence looks obvious on paper, but it is surprising how many shops skip steps in practice. The most common failure is skipping the test piece when a new batch arrives. The second most common is using the same recipe for different glass finishes because the parts look similar. Both failures generate scrap that could have been avoided with a few minutes of discipline.
Cost Drivers and Quoting Considerations
Quoting glass engraving jobs requires a different cost model than quoting wood or acrylic work. The material is more expensive per part, the reject rate is higher, and the inspection standard is more visual. Shops that quote glass like wood will underprice the risk and lose money on the jobs they win.
The main cost drivers are:
- Material cost per part, including the cost of test pieces for recipe validation
- Reject rate, which is influenced by part condition, glass type, and operator experience
- Setup time for fixturing and recipe selection, especially for curved or irregular parts
- Inspection time, because glass defects are visible and customers will reject inconsistent work
- Handling and packing cost, because finished engraved glass needs more protection than raw stock
Shops that track these costs per job will develop accurate pricing over time. Shops that guess will either underprice and lose money or overprice and lose work. The data is worth collecting from the first job onward.
Where It Earns Its Place: Glass Engraving Machines
Glass engraving machines are most useful when the job depends on controlled surface contrast, readable detail, and flexible artwork changes rather than deep removal. The best use cases usually include branded drinkware, awards, decorative panels, and similar applications where a frosted mark adds value without direct tool contact.
The main limits are just as important as the use cases. Glass engraving is usually a surface-marking process, glass quality and part condition affect consistency, and brittle parts punish weak support or careless handling quickly. Buyers who treat those limits honestly make better decisions on quoting, sampling, fixturing, and workflow fit.
In practice, the strongest results come from matching the machine to the real product mix, then controlling the material setup as carefully as the artwork itself. That is what turns glass engraving from a risky sample-driven experiment into a repeatable production process. Shops that document recipes, inspect incoming parts, and validate samples before production will generate consistent results and satisfied customers. Shops that skip those steps will generate scrap and frustration, regardless of the machine they choose.