Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
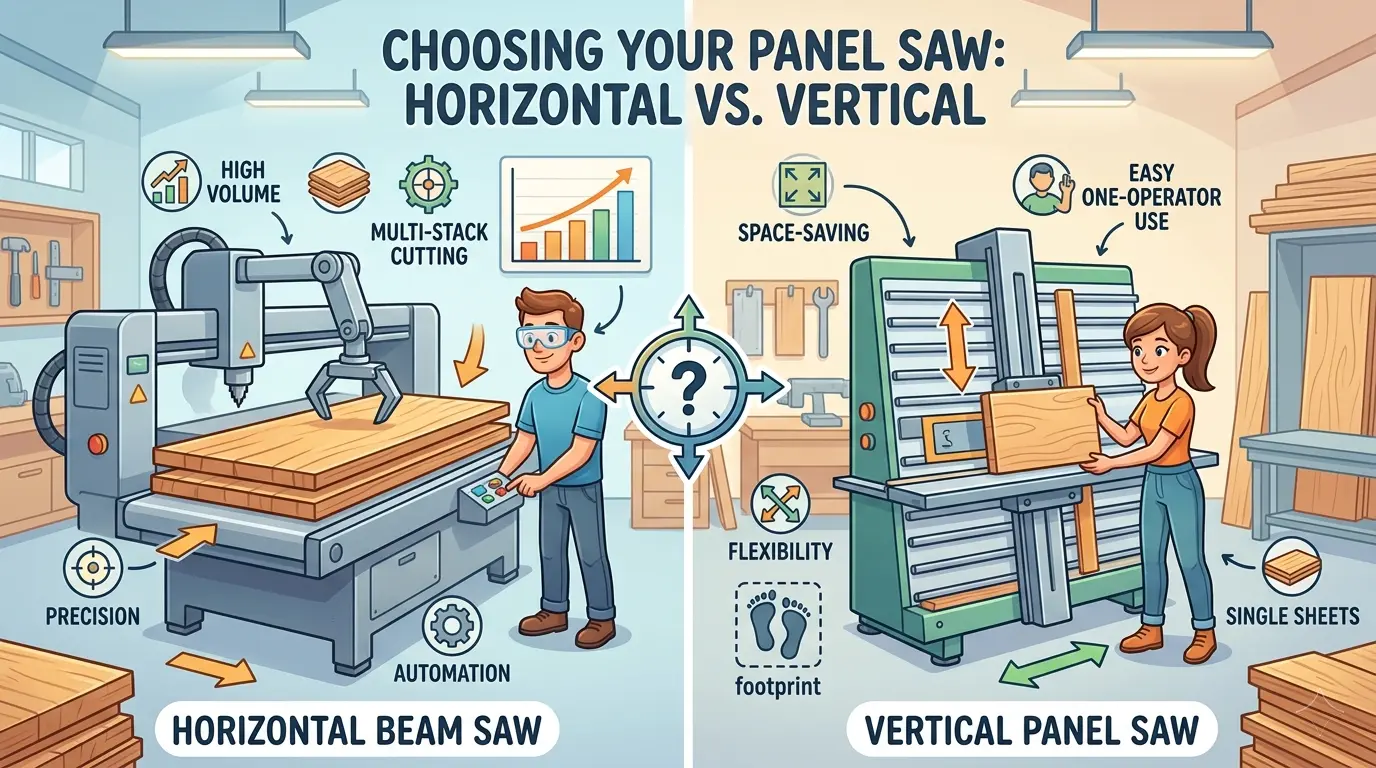
Before comparing feed speeds or blade specifications, identify the actual production constraint that is slowing your line. This article addresses the real decision between a horizontal beam saw and a vertical panel saw: not which cuts straighter, but which removes the dominant friction from your workflow. For cabinet and furniture manufacturers, the choice determines whether you stabilize repeated batch output for edge banding and assembly or preserve tight floor space while handling varied short-run jobs. The tradeoff is throughput consistency versus space efficiency, and selecting the wrong direction forces rework, operator-dependent variation, and costly layout reorganization downstream.
Start With the Bottleneck, Not the Brochure
Most shops begin comparing horizontal beam saws and vertical panel saws only after cutting has become the obvious constraint in the production flow. By that point, the conversation usually starts with accuracy, but that is rarely the real differentiator. Both machine types, when properly set up and maintained, produce clean, square cuts on MDF, plywood, particleboard, and melamine-faced board. The meaningful differences show up elsewhere: how much floor space the machine demands, how much operator involvement each cut requires, how quickly the machine adapts to job changes, and how consistently the output feeds edge banding, drilling, and assembly.
The choice is not about which saw cuts straighter. It is about which saw removes the biggest source of friction from your specific production model. A horizontal beam saw is typically selected to stabilize repeated batch cutting. A vertical panel saw is typically selected to keep full-sheet processing practical where space efficiency and day-to-day flexibility are the priority. Before comparing specifications, define the actual constraint in the shop.
Answer these questions honestly:
- Is cutting throughput slowing down edge banding, drilling, or assembly?
- Is floor space too tight to dedicate a large horizontal cutting cell?
- Does the team run structured cutting lists with stable volume, or frequent short-run job changes?
- Is downstream work suffering because front-end sizing is inconsistent between operators or shifts?
- Are you planning to add a nesting machine or a CNC router in the next 18 months, and if so, how will the saw fit alongside it?
Once the primary constraint is clear, the machine decision becomes more straightforward. If you are losing time because panel cutting cannot keep pace with repeated production, a horizontal beam saw usually fits better. If you are losing time because layout is tight, jobs vary more, or the cutting area needs to stay compact and flexible, a vertical panel saw may be the smarter direction.
What a Horizontal Beam Saw Is Built to Do
A horizontal beam saw is the standard choice for shops organized around repeated panel sizing. In cabinet, wardrobe, office furniture, and modular furniture production, this means a steady flow of rectangular parts that must move predictably into edge banding, drilling, and assembly. The machine is designed around a simple logic: load a full sheet onto the table, program the cutting list, and let the saw carriage execute the cuts with consistent positioning and feed.
The main advantage is not just raw output. It is production stability. The machine removes most of the cut-to-cut variation that depends on operator technique. Once the operator sets the program and loads the sheet, the saw executes the cutting list with consistent positioning and feed. This matters more than most buyers initially realize. In a manual cutting environment, the same operator can produce slightly different part sizes at 8 a.m. and 4 p.m. on the same day. Fatigue, rushing, and subtle differences in how the sheet is positioned all introduce variation. A beam saw eliminates most of that variation because the machine controls the positioning and the feed.
A horizontal beam saw is the stronger fit when management wants:
- More consistent part sizing across repeated jobs
- Lower dependence on operator skill for every individual cut
- Higher front-end throughput for batch production
- Smoother handoffs into downstream processes
- A cutting department that behaves like a system rather than a manual workstation
In practical terms, it suits factories that want the first stage of panel processing to become predictable and easier to scale. The saw becomes part of a repeatable manufacturing system, not just a tool. Consider a shop producing kitchen cabinets with a standard range of door and carcass sizes. The cutting list repeats weekly with minor variations. With a beam saw, the operator loads the program, places the sheet, and the machine works through the list. The operator’s role shifts from making every cut to managing the flow of sheets and stacked parts. That shift has a direct effect on labor allocation. One operator can manage a beam saw through a full shift, and the output feeds edge banding at a steady, predictable rate.
The tradeoff is space and investment. A horizontal beam saw needs a dedicated cutting area with enough room for the machine itself, the loading zone, and the offload side where cut parts are stacked and sorted. In a shop where floor space is already tight, that requirement can be a dealbreaker. The machine also represents a larger capital investment than a vertical panel saw, and it makes the most sense when the volume of repeated panel work justifies that investment.
What a Vertical Panel Saw Is Built to Do
A vertical panel saw solves a different problem. It allows a shop to process full sheets accurately without dedicating the same amount of floor space to a horizontal machine layout. The sheet stands upright against the machine frame, and the saw carriage moves across it. This makes it attractive for smaller cabinet shops, custom furniture workshops, interior fit-out operations, and other businesses where panel cutting must remain accurate but the cutting cell cannot dominate the workshop.
The vertical orientation changes the entire workflow. Instead of lifting a full sheet onto a horizontal table, the operator leans the sheet against the vertical frame. This reduces the physical strain of handling large panels and makes it practical for a single operator to manage full sheets without assistance. The saw carriage runs on rails across the face of the sheet, and the operator guides the cut. For rip cuts, the carriage moves horizontally. For crosscuts, the sheet is repositioned or the carriage is adjusted depending on the machine configuration.
A vertical panel saw is commonly valued for:
- A more compact machine footprint
- Practical full-sheet handling in tighter work areas
- One-sheet-at-a-time cutting with direct operator control
- Easier fit in smaller or mixed-use workshops
- Strong utility for short runs and varied daily work
This is not a low-accuracy option. It means the machine is solving a different problem. Instead of maximizing throughput in a structured production cell, it keeps panel cutting accurate and manageable within tighter layout and labor constraints. In a custom furniture shop, the daily work might include a few sheets of plywood for shelving, a couple of sheets of MDF for a built-in unit, and some melamine-faced board for a wardrobe. The cutting list changes every day. A vertical panel saw lets the operator handle each sheet individually, make the cuts needed for that specific job, and move on without the overhead of programming a full batch.
The tradeoff is throughput and consistency. Because the operator is directly involved in positioning the sheet and guiding the cut, there is more opportunity for variation between operators and between shifts. The machine does not remove the operator’s influence the way a beam saw does. For shops where the same operator runs the saw day after day, that is often acceptable. For shops with multiple shifts or rotating operators, it can introduce inconsistency that shows up downstream in edge banding and assembly.
Side-by-Side Workflow Comparison
The table below summarizes how the two machine types differ across key decision factors.
| Decision Factor | Horizontal Beam Saw | Vertical Panel Saw |
|---|---|---|
| Best Fit | Repeated batch sizing of rectangular panel parts | Space-constrained shops and varied short-run panel cutting |
| Floor Space | Needs a larger dedicated cutting area | Uses an upright layout more efficiently |
| Throughput Focus | Stronger for higher-volume, repeatable output | Better suited to moderate output with manual flexibility |
| Operator Role | More focused on setup, loading, and process flow | More directly involved in sheet positioning and cut execution |
| Job Change Pattern | Best when cutting lists repeat and production is structured | Better when jobs change often and cut mix is less standardized |
| Downstream Impact | Helps stabilize edge banding, drilling, and assembly flow | Works well when downstream flow is lighter or less standardized |
| Growth Logic | Stronger when scaling panel furniture batch production | Stronger when preserving flexibility and workshop space matters most |
| Labor Requirement | One operator can manage high output with minimal physical handling | Operator is involved in every cut; physical handling is lighter but attention demand is higher |
| Setup Time Between Jobs | Program changes are fast, but sheet loading and offload sorting take time | Minimal programming; the operator simply adjusts for the next sheet and cut pattern |
| Typical Part Size Range | Strong for long, repeated rectangular parts in standard sizes | Flexible across varied part sizes, including larger panels that stay in one piece |
The two machines should not be treated as simple substitutes. One is usually chosen to standardize output. The other is usually chosen to keep sheet processing practical in a more compact or varied production environment.
When a Horizontal Beam Saw Usually Makes More Sense
A horizontal beam saw is often the stronger choice if the shop is already organized around repeated panel work and needs the cutting department to support a more disciplined production rhythm. The machine becomes the front end of a system that includes edge banding, drilling, and assembly. When the cutting department runs consistently, the rest of the line can be planned with confidence.
It commonly makes more sense when:
- Most daily output comes from repeated rectangular cabinet or furniture components.
- Cutting capacity is slowing down edge banding, drilling, or assembly.
- Production relies on structured cutting lists and stable daily volume.
- Management wants less variation between operators and shifts.
- The factory is building toward a more standardized panel-processing line.
Consider a mid-sized cabinet shop producing 60 to 80 cabinet boxes per week. The cutting list is generated from a CAD package and includes a mix of carcass sides, shelves, rails, and stiles. Most parts are rectangular, and the sizes repeat across jobs. With a beam saw, the operator loads the program, feeds sheets, and the machine works through the list. The output is consistent, and the edge bander can be fed at a steady rate. The shop manager can plan labor around a predictable flow of parts. If the same shop relied on a vertical panel saw, the operator would need to position each sheet and execute each cut manually. That works for a few sheets, but when the volume reaches dozens of sheets per day, the manual involvement becomes the bottleneck.
The beam saw also changes how the shop handles scrap and offcuts. Because the machine optimizes the cutting pattern across the full sheet, it can reduce waste compared to manual cutting where the operator makes decisions on the fly. Over a year of production, that material savings can be significant, especially when working with higher-cost boards like melamine-faced panels or hardwood plywood.
When a Vertical Panel Saw Usually Makes More Sense
A vertical panel saw is often the better choice when the shop still needs accurate sheet cutting but cannot justify a larger horizontal cutting footprint or a more production-specialized setup. The machine keeps the cutting operation compact and flexible, which matters in shops where space is at a premium or where the work mix changes constantly.
It commonly makes more sense when:
- Floor space is limited and every meter needs to stay productive.
- The shop processes full sheets regularly but does not need a dedicated high-throughput cutting cell.
- Job mix changes often, including smaller batches and custom work.
- Direct operator control is still valuable in the cutting process.
- Investment needs to stay matched to moderate output rather than line-level scaling.
Think about a shop that does interior fit-out work. One week the team is building wardrobes for an apartment, the next week they are making shelving for a retail space, and the following week they are producing custom desks for an office. The panel sizes vary, the quantities are small, and the cutting list changes with every job. A vertical panel saw fits this workflow because the operator can handle each sheet as it comes, make the cuts required for the current job, and move on. There is no need to program a batch or manage a large offload area. The machine sits against a wall, takes up minimal floor space, and leaves the rest of the workshop open for assembly and other work.
The vertical panel saw also has an ergonomic advantage in certain situations. Because the sheet stands upright, the operator does not need to lift a full 18mm MDF sheet onto a horizontal table. That reduces fatigue and the risk of injury, especially for smaller shops where the same person handles cutting, assembly, and delivery. For a one- or two-person operation, that physical difference can be the deciding factor.
The Real Tradeoff Is Throughput vs. Space Efficiency
In most factories, this decision comes down to one core tradeoff. A horizontal beam saw helps standardize the line. A vertical panel saw helps preserve workshop space while keeping sheet cutting accurate and manageable.
The throughput argument for a beam saw is not just about cuts per hour. It is about the consistency of those cuts and the effect that consistency has on everything downstream. When every carcass side is exactly the same size, edge banding runs faster, drilling patterns line up, and assembly goes together without shimming or adjustment. That consistency has a compounding effect across the entire production process. A beam saw delivers that consistency because the machine controls the positioning and feed. The operator’s role is to manage the flow, not to make every cut.
The space argument for a vertical panel saw is equally practical. In many urban workshops, floor space is expensive and limited. A vertical saw can be placed against a wall, and the area in front of it can double as a staging area for sheets and finished parts. A horizontal beam saw needs dedicated space on all sides: loading zone, machine footprint, and offload area. In a shop where every square meter is already allocated, that requirement can force a reorganization of the entire layout.
There is also a middle ground worth considering. Some shops start with a vertical panel saw and add a beam saw later as volume grows. Others run both machines in parallel, using the beam saw for high-volume batch work and the vertical saw for custom jobs and one-off requests. That hybrid approach can work well, but it requires the floor space and the labor to support two cutting stations. If the budget and space allow, it gives the shop maximum flexibility.
How the Machines Affect Downstream Processes
The choice between a horizontal beam saw and a vertical panel saw has a direct effect on edge banding, drilling, and assembly. These downstream processes depend on receiving parts that are consistently sized and square. When parts vary, the downstream work slows down and rework increases.
With a horizontal beam saw, the output is predictable. The machine produces parts that are consistently sized, and the operator can stack them in an organized way that matches the downstream sequence. For example, if the cutting list is organized by cabinet, the operator can stack parts for each cabinet together, making it easy for the edge bander operator to work through the batch. This organization reduces the time spent searching for parts and sorting through stacks.
With a vertical panel saw, the output depends more on the operator’s discipline. Because the operator is directly involved in each cut, the consistency of the parts depends on how carefully the sheet is positioned and how consistently the cuts are executed. In a shop with one experienced operator, this is rarely a problem. In a shop with multiple operators or high turnover, it can lead to variation that shows up in edge banding and assembly.
The downstream effect also includes scrap and rework. A beam saw with an optimized cutting pattern can reduce waste by arranging parts efficiently across the sheet. A vertical panel saw relies more on the operator’s judgment, which means the cutting pattern may not be as efficient, especially for complex jobs with many different part sizes. Over time, that difference in material utilization can add up to a significant cost.
A Simple Buying Filter
The following filter is often more useful than comparing isolated features without tying them back to the actual workflow.
| If Your Main Issue Is… | The Better First Direction Is Usually… |
|---|---|
| Repeated batch cutting is limiting cabinet or furniture output | Horizontal beam saw |
| Floor space is tight but full-sheet sizing is still required | Vertical panel saw |
| The work changes frequently and batches stay relatively small | Vertical panel saw |
| The goal is more repeatable front-end flow into downstream operations | Horizontal beam saw |
| The shop needs shaped cutting plus routing or drilling integration | A different solution, such as CNC nesting, may deserve comparison first |
| Labor is scarce and the shop needs one operator to manage high output | Horizontal beam saw |
| The shop is a one- or two-person operation with varied daily work | Vertical panel saw |
Practical Considerations Before You Decide
Beyond the core tradeoff of throughput versus space, there are several practical considerations that often tip the decision one way or the other.
First, think about the physical flow of material in your shop. Where do sheets arrive? Where do cut parts go next? A beam saw needs a clear path for sheet delivery and a clear area for offload sorting. A vertical saw can be placed closer to the wall and can work with a simpler material flow. If your shop layout is already tight, the vertical saw may fit without major reorganization.
Second, consider the skill level of your operators. A beam saw reduces the skill required for each cut because the machine handles the positioning and feed. A vertical saw requires the operator to understand sheet layout, cutting sequence, and blade adjustment. If you have experienced operators who understand panel processing, a vertical saw can work well. If you are hiring new staff or rotating operators across shifts, a beam saw may be more forgiving.
Third, think about the range of materials you cut. Both machines handle MDF, plywood, particleboard, and melamine-faced board. But if you regularly cut thicker panels, laminated boards, or materials with brittle surfaces, the machine’s blade quality and scoring capability matter. A beam saw typically has a more robust blade and scoring system because it is designed for continuous production. A vertical saw can still produce clean cuts, but the operator needs to pay more attention to feed rate and blade condition.
Fourth, consider the future. If you plan to grow production volume, add a nesting machine, or expand into new product lines, the saw you choose today should fit that trajectory. A beam saw is a stronger foundation for scaling batch production. A vertical saw is a better fit if you plan to stay flexible and handle a wide variety of jobs without adding a dedicated cutting cell.
Production Fit: Horizontal Beam Saw vs. Vertical Panel Saw
Choose a horizontal beam saw when the shop needs higher-throughput, repeatable panel sizing that supports a more standardized production line. Choose a vertical panel saw when accurate full-sheet cutting is still important, but floor space, job variety, and a more compact machine layout matter more.
The right answer is not hidden in the machine name. It is in the production constraint. If the daily problem is unstable throughput in repeated panel work, a horizontal beam saw usually fits better. If the daily problem is limited space and more flexible sheet processing, a vertical panel saw is often the more practical fit.
Before you commit to either direction, map your current workflow from sheet delivery to assembly. Identify where the delays happen, where the variation enters, and where the space is tightest. That map will tell you which machine solves the real problem. If you are still weighing the options, review the panel saw category to see how different machine configurations align with your production model. The machine that fits your constraint is the one that will earn its place on the shop floor.