Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
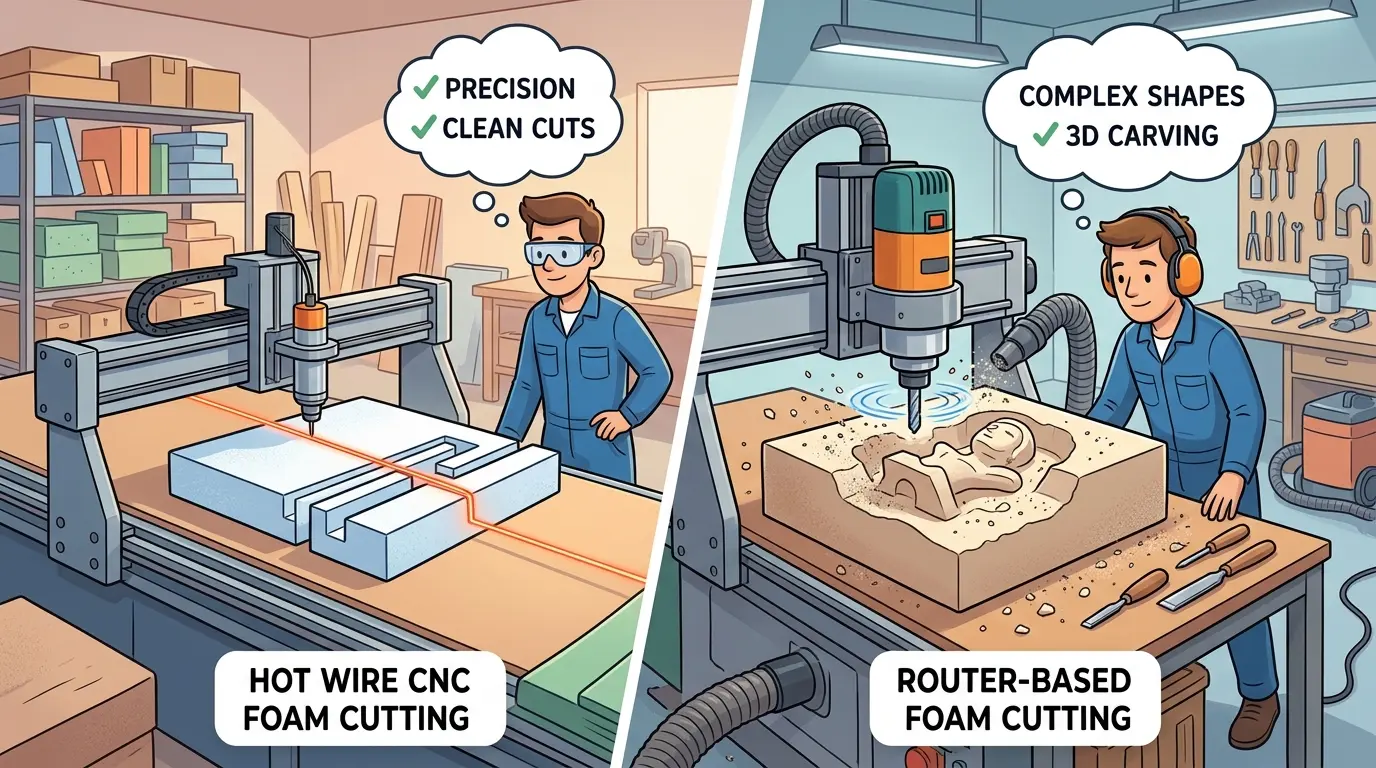
Before comparing machine specs, define the actual part geometry: hot-wire cutting melts a path through thermally suitable foam, while routing mechanically shears material to create pockets, steps, and assembly features. Buyers often pick a process based on a clean demo, then pay later in secondary operations, weak tolerances, or manual cleanup. The real production question is whether your work is mostly contour-driven or feature-driven. Long sweeping profiles favor hot wire; internal cavities, nested sheet layouts, and mixed-material flexibility favor routing. Match the process to the feature list, not the impression.
Start With the Part Geometry, Not the Machine
The quickest way to settle the hot-wire-versus-router debate is to stop comparing machines and start describing the parts you actually produce. Both processes remove foam, but they do it through completely different physical mechanisms. A hot-wire cutter uses a tensioned, heated wire to melt a path through the material. A router uses a spinning cutter to mechanically shear foam away. Those two mechanisms create different capabilities, different limitations, and different expectations for edge quality, internal features, dust generation, toolpath logic, and secondary finishing.
Buyers often make the wrong choice because they base the decision on which process looks cleaner or more impressive in a short demonstration. The correct choice depends on the foam type, the feature list, and what has to happen after cutting. Define those three things clearly, and the decision becomes a practical engineering question rather than a preference issue.
The first question is not whether you prefer thermal cutting or routing. The first question is what the part actually has to contain. Long sweeping contours, profile sections, wing-like forms, insulation shapes, and packaging blocks align well with hot-wire cutting. Deep pockets, steps, rebates, holes, drilled features, and nested flat-sheet components point toward routing.
That distinction matters because each process speaks a different geometric language. Hot-wire systems are naturally good at surfaces that can be described by wire movement between controlled points or along defined contour logic. Router systems are good at geometry controlled by cutter diameter, depth, stepover, entry path, and localized feature access. When buyers force the wrong process onto the wrong geometry, they usually pay later in secondary operations, weak tolerances, or slow manual cleanup.
The practical starting point is simple: write the feature list before you compare the machines. If the part depends mostly on external shape, hot wire deserves serious attention. If the part depends on cavities, shoulders, mating details, or controlled-depth features, routing usually becomes the more realistic answer.
Hot-Wire Cutting Excels When the Part Is Mostly a Contour Problem
Hot-wire systems are efficient when the foam is thermally suitable and the geometry is continuous rather than deeply detailed. EPS and similar materials used in packaging, insulation, scenic forms, and large lightweight shape generation often work well with this method. The cut can be clean, the process can be relatively fast, and the tool does not experience mechanical load in the same way a router bit does.
This creates a strong advantage on profile-driven work. If the job is essentially about getting from one outline to another cleanly and repeatedly, hot wire can be a very direct method. Long cuts that would create a large volume of routed particles may instead be handled with much less mechanical mess.
There is also a labor benefit when the job is repetitive. Once the process is stable, hot-wire cutting can move through large simple forms with less concern about cutter wear, bit breakage, or the cutting forces that affect lightweight materials during routing. For repeat contour families, that simplicity can be valuable.
Hot Wire Stops Being Elegant Once the Part Needs Localized Detail
The same process becomes restrictive when the part needs internal corners, pockets, shelves, local depth changes, or true three-dimensional machining logic. Wire behavior, entry strategy, kerf control, and feature access all become design constraints. That is not a weakness in the machine. It is simply what the process can and cannot do naturally.
Thermal behavior matters as well. Some foam types respond predictably. Others do not. Surface quality can degrade when speed, temperature, density, or wire condition drift out of balance. A part may look acceptable immediately after cutting and still reveal distortion, inconsistent edge behavior, or fit problems when it reaches assembly.
This is why buyers should be careful with simplified claims like “hot wire is cleaner” or “hot wire is more precise.” It can be cleaner for certain foam families and contour jobs. It can also become the wrong tool the moment the part starts asking for localized geometry instead of simple profile logic.
Router-Based Foam Cutting Wins When Feature Control Matters More Than Simple Shape
Routing earns its place when the part needs more than an outline. If the job requires pockets, rebates, steps, countersinks, holes, reliefs, assembly features, or controlled-depth machining, a router-based process usually offers much more control. The router is not just tracing a perimeter. It can create internal structure.
That makes routing especially useful when foam parts have to assemble with other components, receive inserts, support local loading, or fit into larger fabricated products. It also becomes more attractive when many different part types need to be nested and cut from common stock in one digital workflow.
This is often the real production difference. Hot wire is excellent when the part is mostly a shape. Routing is better when the part is a shape plus a set of functional features.
Routing Is Also Stronger in Mixed-Material or Mixed-Job Environments
Another reason shops choose routing is that the same machine logic can often support more than one foam type, and sometimes a broader set of lightweight materials, depending on tooling and process parameters. That wider applicability is important in mixed-production environments where one process backbone is more useful than a specialist lane dedicated to a narrow class of parts.
A router-based workflow also aligns more naturally with nested production thinking. If sheets need to be used efficiently and many part geometries must be laid out in a common job, routing often becomes easier to integrate with existing CAM habits, labeling routines, and handling logic.
In other words, even if hot wire would be faster for one narrow family of contour parts, routing may still win when the broader factory needs one more versatile process lane.
Foam Routing Fails When Buyers Underestimate Heat, Hold-Down, and Dust
Routing is not automatically better simply because it is more flexible. Foam reacts badly to careless routing. Wrong cutter choice, excessive spindle heat, poor chip evacuation, and aggressive engagement can create melted edges, ragged surfaces, dimension drift, or weak feature definition. Soft materials can also move, tear, or deform if hold-down is poor.
Dust and particle control are another major issue. Foam routing often creates large volumes of lightweight particles that spread quickly if extraction is under-designed. This is not just a housekeeping annoyance. It affects visibility, maintenance, air quality, machine cleanliness, and process consistency.
The labor burden can also rise if the shop assumes foam is easy and therefore underestimates fixturing, toolpath testing, and cleanup. Routing can absolutely be the right answer, but it still requires process discipline. Lightweight material is not the same thing as forgiving material.
Quality Should Be Judged by What Happens After Cutting
Part quality should be evaluated by downstream performance, not only by how attractive the cut looks in the machine. Hot wire may produce smooth contours with minimal dust and still fail the application if the part later needs local machining, mating features, or consistent structural seating. Routing may produce more cleanup burden and still be the correct process because it creates the functional geometry the assembly needs.
This is the point many buyers miss. The comparison is not just thermal finish versus mechanical finish. It is contour convenience versus feature control.
If the part will be glued, nested into another assembly, coated, skinned, or mechanically joined, those downstream steps matter more than which cutting method looks simpler in isolation.
Tolerance Expectations Need to Be Matched to the Process, Not Copied Across It
Tolerance language changes by process. Hot-wire cutting has to manage wire temperature, bow, thermal response, and path stability. Routing has to manage cutter diameter, runout, hold-down, chip removal, and local deflection. If buyers speak about both methods as though they share the same tolerance behavior, quotation accuracy usually suffers.
That is why a better question is not, “Which process is more accurate?” The more useful question is, “Which process achieves the features I need with less secondary work and fewer unstable variables?” That is the production question that matters.
For some profile parts, hot wire wins that test easily. For most pocketed or assembly-critical parts, routing usually does.
Cleanup Burden Is Part of the Process Economics
A short demo can make either process look ideal. The real question is what the floor looks like after a full week of work. How much operator intervention is needed? How much waste has to be cleaned? How often are settings adjusted? How many parts require touch-up before shipping or assembly?
Hot wire can be economical when the same contour family repeats and the material remains predictable. Routing can be economical when one machine supports many foam geometries and related materials in the same programming environment. Neither process wins every cost argument. The right answer depends on repeatability, part mix, and whether the shop values specialization or flexibility more highly.
This is one reason labor should be measured across the full shift, not just at the cutting head. A process that looks faster while cutting can still cost more if cleanup, rework, or staging gets worse.
Use a Geometry-and-Workflow Matrix Instead of General Claims
The table below helps keep the decision attached to real process needs.
| Requirement | Hot-Wire Cutting | Router-Based Cutting |
|---|---|---|
| Long contour profiles | Often excellent | Usually possible |
| Internal pockets and steps | Weak fit | Strong fit |
| 3D relief or local sculpted detail | Limited | Stronger |
| Low dust preference | Often better | Needs stronger extraction |
| Mixed foam types and broader versatility | More limited | Usually better |
| Nested sheet utilization | Weak | Strong |
| Toolpath simplicity on basic profiles | Strong | Moderate |
| Functional assembly features | Limited | Stronger |
| Shared workflow with broader sheet processing | Limited | Better integration |
This kind of matrix does not replace test cuts, but it exposes very quickly where a process is being forced into the wrong class of work.
Some Shops Need Both Processes, but for Different Reasons
There are environments where both processes are justified. A shop may use hot wire for large profile-driven foam forms and routing for localized features, assembly preparation, or mixed-material jobs. In that case, the important discipline is role separation. Do not ask both machines to compete for the same value. Assign each process the work it handles naturally.
This is especially relevant when foam cutting is not the main business. In some factories, foam supports packaging, templates, displays, or auxiliary components while the main production logic still revolves around routed panels, sheet processing, or other digital cutting work. When that happens, buyers should be careful not to optimize the whole investment strategy around a secondary foam task.
When Foam Cutting Sits Inside a Larger Production Plan
If the lasting production value sits in routed panels, nested sheet processing, or broader handling efficiency, the durable investment may be the routing backbone rather than a specialist foam machine. For that reason, CNC nesting machines are often the better long-term category to study in furniture, packaging-support, or sheet-processing environments where flexibility matters beyond foam alone.
And for buyers comparing when batch efficiency should dominate over programmable flexibility, the Pandaxis article on beam saw versus CNC nesting machine selection offers a useful workflow lens. Different material family, same buying logic: choose the process that fits the real bottleneck, not the most interesting machine demonstration.
The Right Process Usually Reveals Itself Once You Describe the Part Honestly
Choose hot-wire cutting when the job is dominated by long contours in thermally suitable foam and when internal machined features are rare. Choose router-based cutting when the parts need pockets, 3D form control, nested sheet layouts, or more flexible use across varying foam jobs.
The decision becomes clear once you name the geometry, the material behavior, the cleanup burden, and the downstream requirement. Do that first, and the process usually chooses itself.