Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
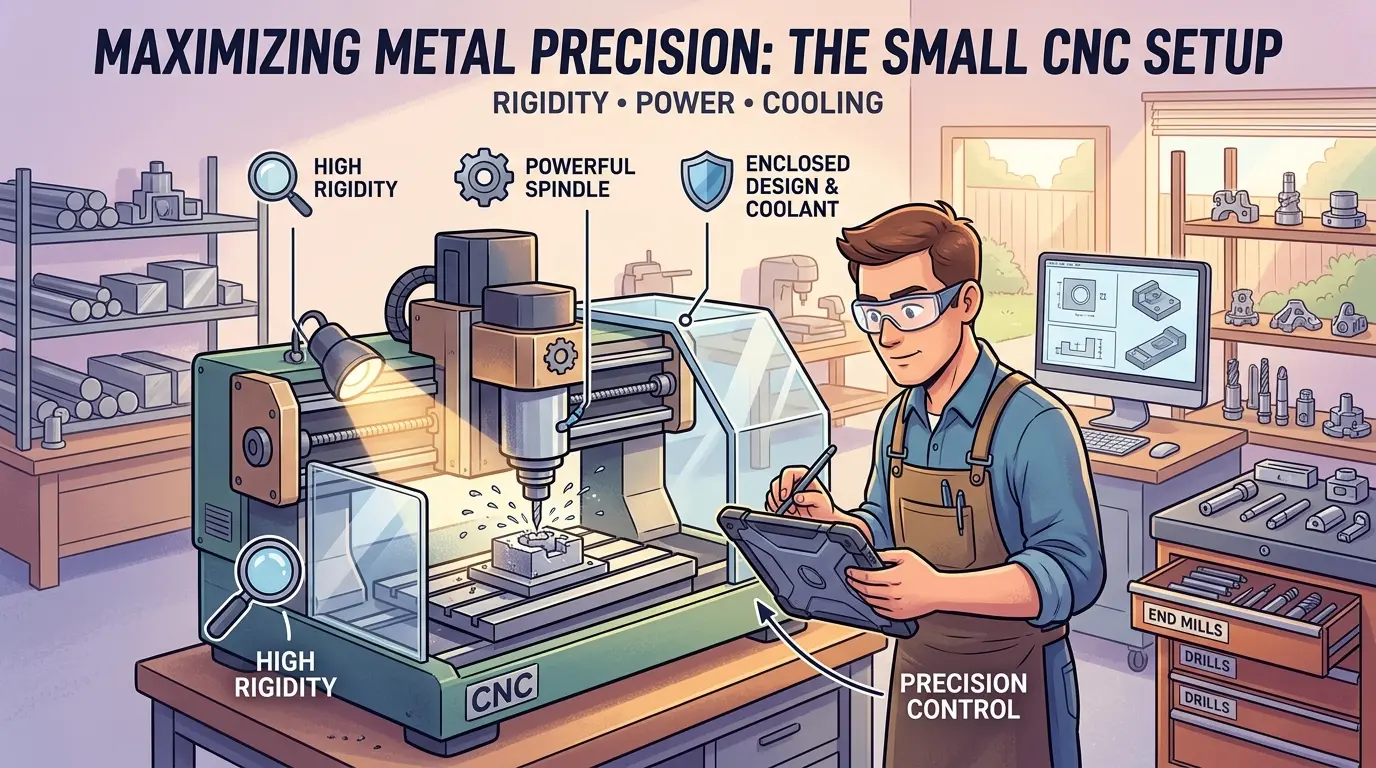
Compact metal CNCs attract buyers with low price and small footprint, but the real test is whether they hold up under daily production pressure. This article cuts through the brochure specs to expose the operational realities that determine success: usable envelope versus travel numbers, structural rigidity versus spindle power, and the hidden labor burden that often erases capital savings. For manufacturers evaluating small-format machines for aluminum, steel, or mixed material work, the decision hinges on process discipline, workholding fit, and honest material expectations—not just cutting capability.
Why Small Metal CNCs Fail to Meet Expectations in Real Shops
Small-format CNC machines attract buyers for understandable reasons. They cost less, fit into tight floor space, and seem less intimidating for operators who are new to metal cutting. The promise of machining aluminum or light steel without dedicating a full production bay to a machining center is genuinely appealing.
The problem emerges when those machines meet real metal. Metal cutting exposes weak assumptions far faster than wood, foam, or plastics do. A machine that produces clean demo parts can struggle badly on an ordinary Tuesday afternoon when the shop is warm, the tools are partially worn, and the operator is trying to finish an actual order rather than a polished sample.
The right question is not whether a small CNC can cut metal. It is which metal parts it can cut repeatedly, at what labor burden, and with what tolerance risk once the machine has been running for hours. Buyers who focus on travel numbers and spindle-speed headlines often miss the factors that actually determine whether a part is repeatable.
Travel Numbers Are Not the Real Work Envelope
Table travel is the first specification buyers check, but it is rarely the true capacity limit. In metal work, the usable envelope is always smaller than the brochure suggests. A vise, parallels, clamps, edge-finding space, tool approach clearance, and chip evacuation room all consume volume that the travel figures do not account for.
A part that looks easy on paper becomes awkward once the fixture sits high or the cutter needs safe movement around the workpiece. This matters because small machines are usually bought to save money, and the instinct to force too much into one setup is common. The result is cramped workholding, compromised toolpaths, poor chip evacuation, and longer proving time.
The buyer sees travel. The programmer sees approach paths. The operator sees chips piling against a vise jaw because there is no clean escape route. Those are not the same thing. A machine that technically fits the part may still be operationally too small for stable metal work.
Rigidity Determines Whether the Machine Is Useful or Merely Encouraging
The biggest gap between expectation and reality is usually rigidity. Metal cutting reveals every weakness in the frame, spindle mount, column, linear motion system, and workholding stack. A machine can survive light aluminum passes and still perform poorly once the job asks for deeper engagement, harder alloys, tighter finish expectations, or consistent dimensional behavior across a run.
Buyers often focus on spindle power without asking whether the structure can use that power effectively. A small machine with modest but honest stiffness can outperform a higher-speed machine that chatters the moment the cut becomes serious. Finish problems blamed on tooling are often structural problems in disguise.
This is where many “metal-capable” claims become misleading. Capability in principle is not the same as capability at a commercially useful pace. If the machine reaches the feature but only by slowing the cut so far that labor dominates everything, the part may be possible and still be a poor business fit.
The Process Window Collapses Before the Machine Breaks
Small machines do not normally fail in dramatic ways first. More often, the process window collapses quietly. The tool starts to chatter sooner than expected. Surface finish becomes inconsistent between parts. The operator backs off the feed to protect the cut. Tool life becomes unpredictable. Hole position drifts a little after warm-up.
None of those problems necessarily means the machine is broken. They mean the real operating window is narrower than the buyer assumed. Narrow process windows cost labor because the operator has to babysit more closely, prove more carefully, and accept less aggressive cycle planning. The machine can still contribute value, but only if the business expected this level of operator involvement from the start.
Thermal Drift Is More Visible on Compact Machines
Small metal machines are often installed in mixed-use rooms, light industrial units, garages, toolrooms, or prototype areas where temperature control is weaker and warm-up discipline is informal. Those conditions make thermal drift more visible. A machine that looks accurate immediately after start-up may move enough during steady running to affect hole location, pocket size, or finish consistency on longer jobs.
The fix is not automatically to buy a larger machine. The fix is to accept that even compact machines need process discipline. Warm-up routines, repeatable touch-off procedures, stable work offsets, and sensible inspection intervals are part of the ownership burden whether the seller mentions them or not.
This is also where buyers underestimate the value of probing and measurement routine. A machine advertised as simple can still become difficult to live with if its measurement workflow is improvised every morning.
Chip Control Is a Cutting Problem, Not a Cleaning Problem
Metal chips do not behave like woodworking dust. They trap heat, recut against the tool, scratch finished surfaces, and shorten tool life when they stay in pockets, slots, or corners. On a small machine, chip control is harder because the enclosure is tighter, coolant delivery may be limited, and operators are often tempted to run minimally wet or nearly dry to avoid mess.
That can work for a narrow range of parts. It becomes risky once the geometry traps chips or the material work-hardens. At that point the machine’s limitations become visible in the finish, in the tool wear, and in the operator time spent clearing chips manually.
This is why clean demo pieces prove so little. A polished sample cut is easy to show once. The real question is whether the chip-control method survives a real batch when the workpiece has deeper pockets, narrower channels, or a more demanding alloy.
Workholding Usually Becomes the Real Space Problem
Many buyers think the limitation on a small metal CNC is cutting power. In daily use, workholding is often the bigger issue. A compact machine can have enough spindle for the part and still become frustrating because the vise, clamps, fixture plate, or rotary accessory consumes too much of the usable volume.
This is especially true when the buyer expects the machine to grow from prototype work into short-run production. Prototype setups can tolerate awkward clamp positions and slow manual checking. Production-style repetition cannot. Once the job requires repeatability, quick loading, and stable clearance for tool changes or probing, the machine’s real capacity may shrink sharply.
Workholding should be evaluated before the machine is approved, not after delivery. In many cases, the fixture stack tells the truth about machine fit faster than the spindle brochure does.
Tooling Strategy Must Be More Conservative on Small Machines
Small machines reward conservative, well-matched tooling. Shorter stick-out, smaller radial engagement, realistic depth of cut, and sane toolpath choices are not signs of weakness. They are how a modest platform becomes reliable. The mistake is trying to imitate full-size machining-center strategies on a machine that does not have the same mass, damping, enclosure design, or spindle cartridge behavior.
Automatic tool changing is not the only measure of professionalism. A compact machine with manual changes can still do useful work if the part family is simple and the setup discipline is strong. On the other hand, a poor automatic tool system on an unstable platform does not create industrial capability by itself.
Tooling on small machines is really a question of process honesty. If the platform needs gentler engagement, simpler tool libraries, and more operator awareness, the business has to account for that rather than pretend it bought a miniature VMC.
Material Mix Should Drive the Decision More Than General Ambition
“Metal” is too broad to support a good buying decision. Aluminum, brass, bronze, mild steel, tool steel, stainless, and titanium do not create the same loads or the same tolerance risk. A small machine that handles aluminum brackets and fixture plates well may struggle badly with stainless pockets, harder steels, or interrupted cuts that demand torque and damping.
Buyers should define the actual revenue mix or internal workload mix instead of asking whether the machine can cut metal in principle. If the work is mostly aluminum prototypes, soft metals, jigs, light repair parts, or internal fixtures, a small machine may be justified. If the expected workload includes sustained production in demanding alloys, the machine may be a stepping stone rather than a true long-term answer.
That is not a failure if it is planned honestly. It becomes a costly mistake only when the buyer expects one compact machine to carry a material mix that really belongs on a heavier platform.
Labor Is Usually the Hidden Cost, Not the Machine Price
Compact metal CNCs often lose money through labor inefficiency before they fail mechanically. They require more proving, more careful setup, more cautious toolpaths, and more operator judgment to keep results consistent. If the business model depends on unattended output, dense multi-op parts, or rapid turnover between jobs, the labor burden can erase the capital savings quickly.
This is the overlooked part of many buying decisions. A small machine can be ideal for internal tooling, learning, prototypes, light service parts, and carefully controlled short runs. It becomes less attractive when the plant needs stable throughput and predictable quoting under pressure. At that point, the real comparison is not only small machine versus big machine. It is also small machine versus outsourcing, versus a heavier used platform, versus delaying the purchase until the job mix is clearer.
A Practical Screening Table Before You Buy
| Factor | Why It Matters On A Small Metal CNC | What To Check Before Approval |
|---|---|---|
| Frame stiffness | Governs chatter, finish, and realistic material removal | Column design, frame mass, vibration behavior under a real cut |
| Usable envelope | Determines whether fixtures and tools fit safely | Vise size, clamp space, probe clearance, tool approach room |
| Thermal stability | Affects repeatability through longer jobs | Warm-up drift, offset stability, environment consistency |
| Chip control | Protects tool life and finish quality | Coolant options, air blast strategy, pocket evacuation behavior |
| Tooling workflow | Shapes setup time and operator burden | Tool measurement method, change routine, practical stick-out limits |
| Material fit | Prevents unrealistic job assumptions | Actual alloy mix, hardness range, finish demands, batch size |
| Labor demand | Decides whether the machine is truly economical | Amount of operator babysitting required after proving |
This kind of table keeps the discussion tied to production rather than enthusiasm. It also helps prevent the classic mistake of assuming one successful demo cut proves broad machine fit.
Compare Small Machines Against Heavier Mills More Honestly
Many buyers do not really need an answer to “Can this compact machine cut metal?” They need an answer to “At what point does a heavier machine save money even if it costs more?”
That is why it helps to compare compact machines directly with larger-capacity platforms rather than only with hand tools or no machine at all. Once the part mix includes repeat steel work, denser setups, tighter tolerance control, or longer daily runtime, the cost of staying small can rise faster than expected. A more explicit look at how capacity changes the decision between small mills and industrial mills often clarifies that inflection point.
The correct answer is not always “buy bigger.” The correct answer is to stop treating smallness as neutral. It changes the economics of every downstream decision.
Buying Discipline Still Matters in the Entry Segment
Entry-level and compact machines are often sold with optimistic language around precision, versatility, and upgradeability. Buyers should still ask the same hard questions they would ask on larger equipment: what maintenance routines are required, what spare parts are common, how controller backups are handled, what metrology is assumed, and how the machine behaves after several hours of actual cutting.
It is also worth applying the same quote discipline used on bigger purchases. Freight, installation burden, workholding, tooling, metrology, coolant, chip management, and future upgrade cost all matter. The same habits used to compare CNC machinery quotes without missing critical details matter even more on compact machines because the budget leaves less room for surprise spending.
Look Beyond Capability to the Daily Operating Burden
Buyers do not usually overlook whether a small CNC machine can touch metal. They overlook how much process discipline the machine asks for once the work becomes real.
They overlook that the usable envelope is smaller than the travel numbers, that rigidity sets the process window, that thermal behavior changes the measuring routine, that chips become a cutting variable, and that operator time often becomes the hidden cost center. A small machine can be an excellent investment when the part family is honest, the material mix is realistic, and the business accepts the labor model that comes with it.
It becomes a poor investment when the shop expects compact size to behave like industrial mass. Small CNC machines for metal succeed when buyers define the part family clearly, respect the limits of structure and chip control, and build real discipline around workholding, warm-up, and measurement. They disappoint when travel numbers and spindle speed are used as substitutes for production reality.