Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
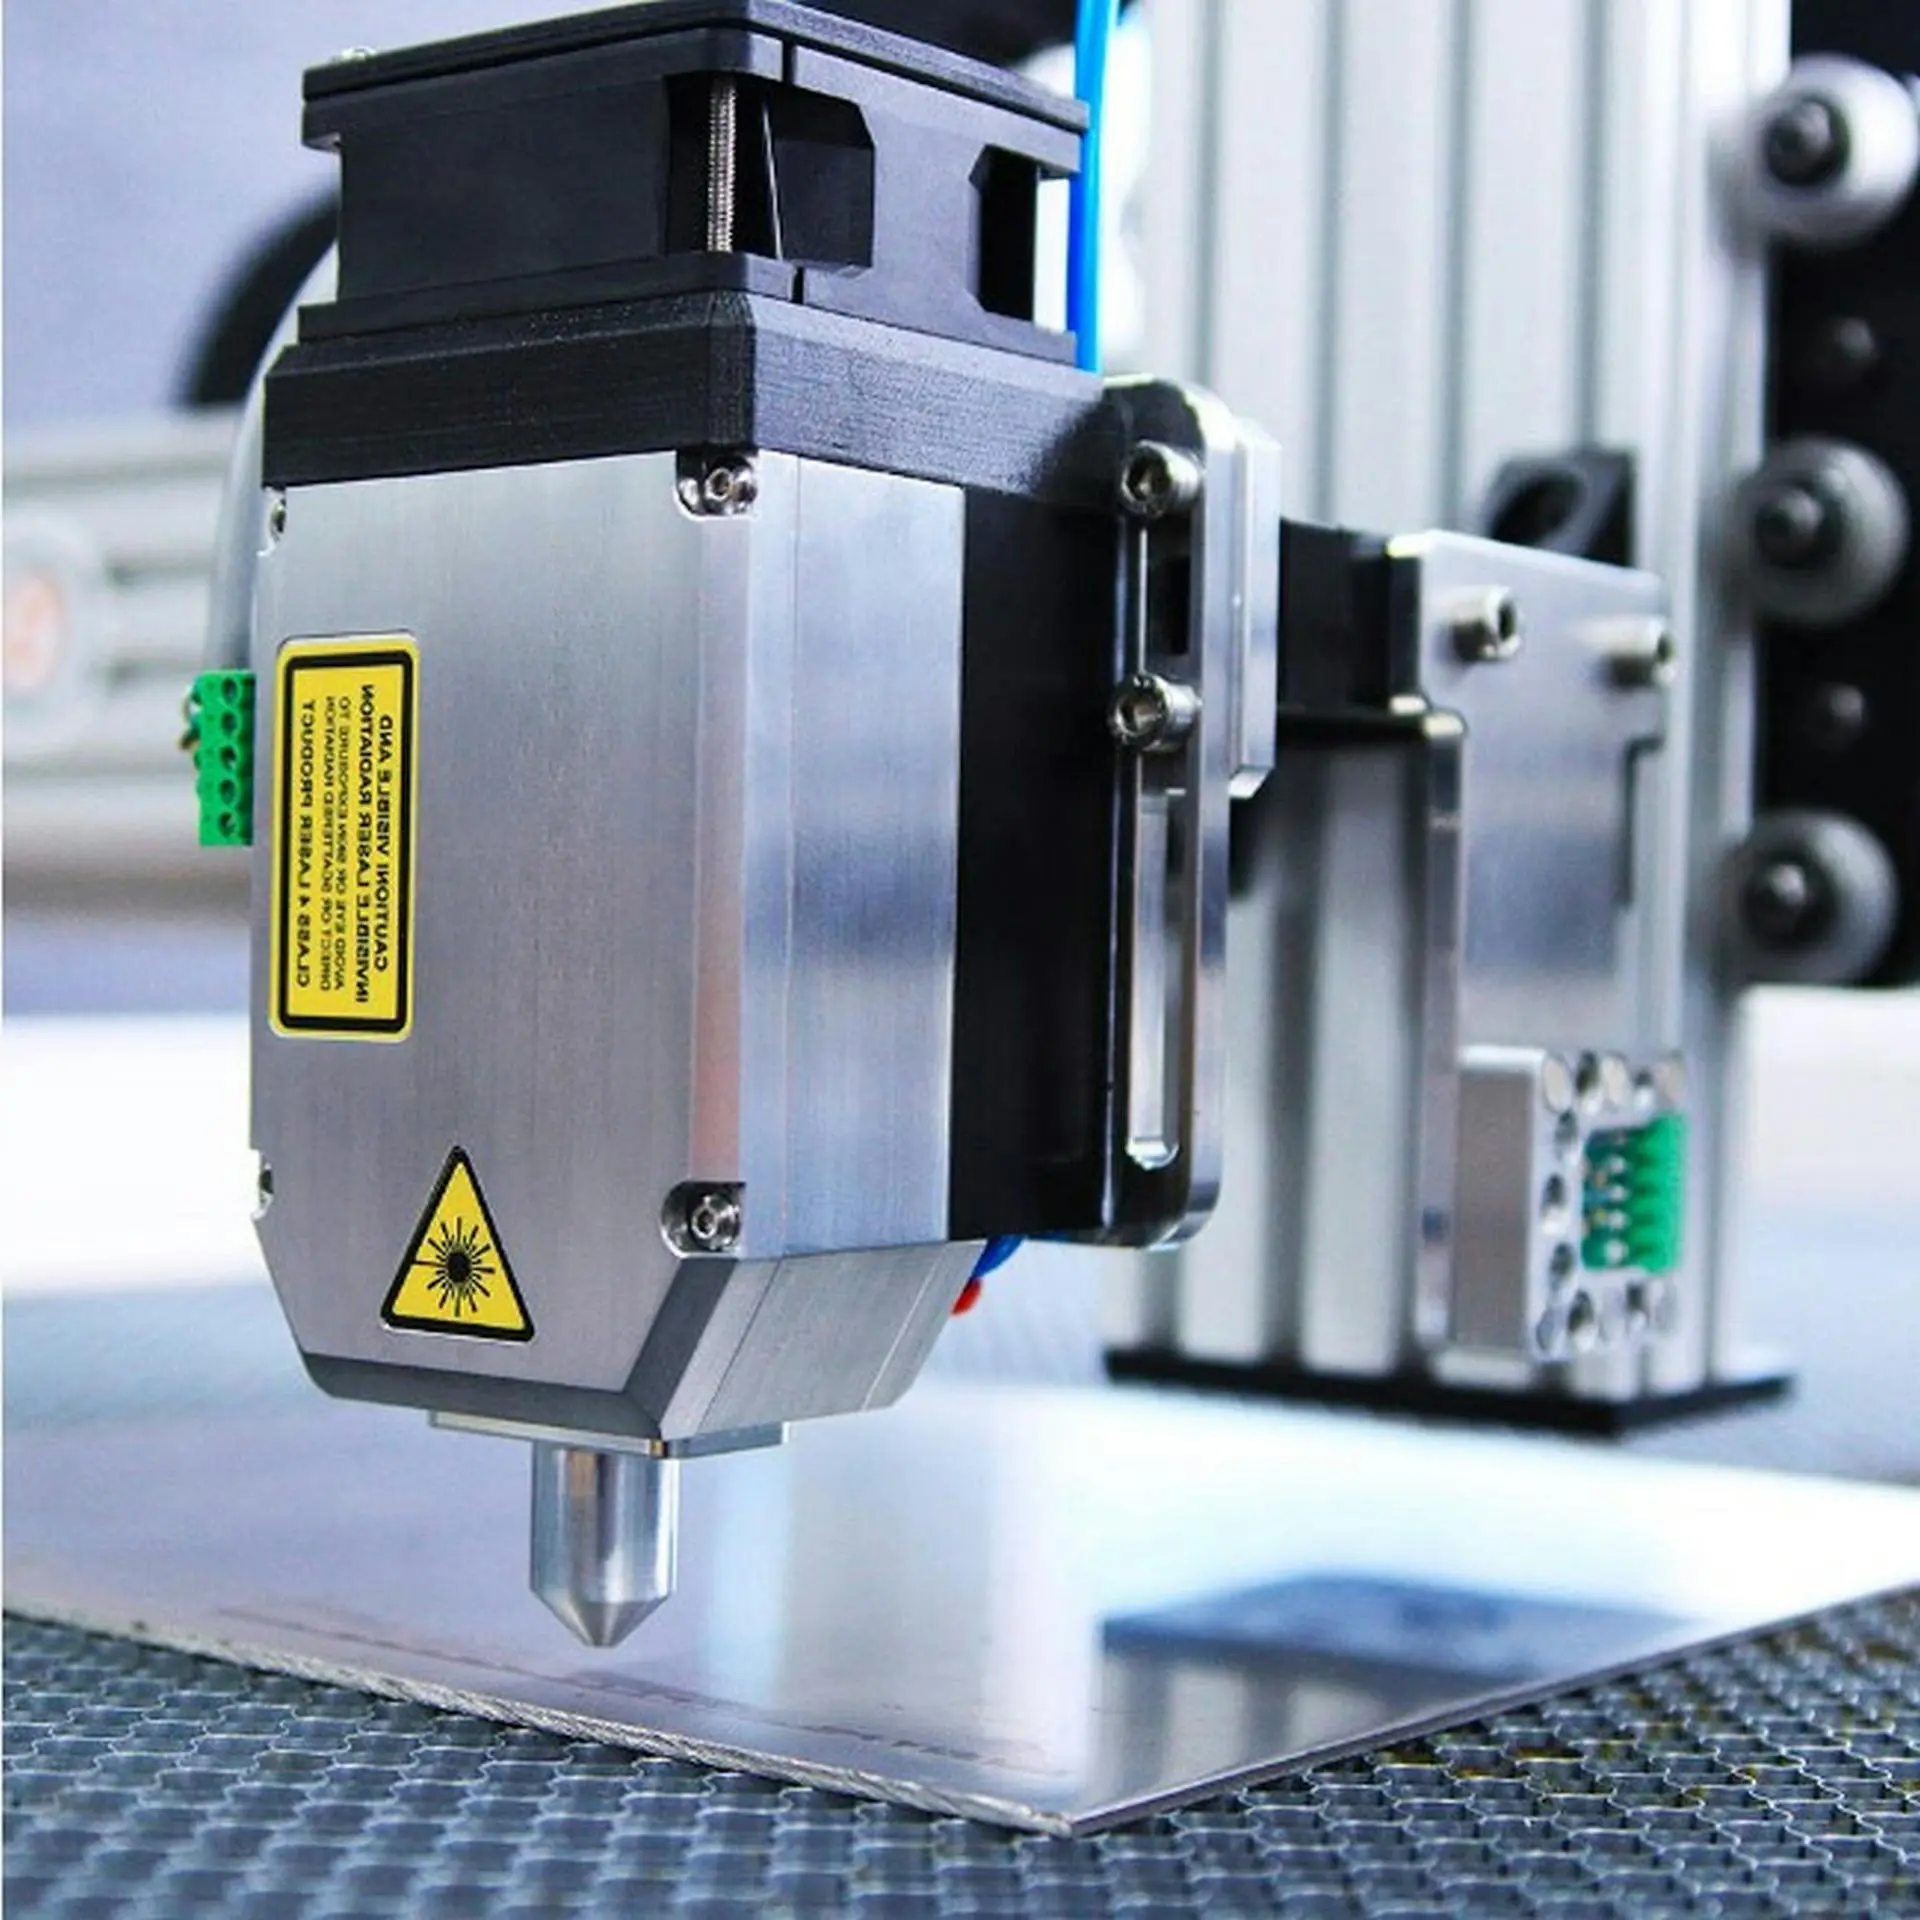
Part marking is often treated as an afterthought in fabrication and assembly shops—until a faded serial number or an unreadable data matrix code halts a production line and turns warranty analysis into guesswork. The real decision is not simply which machine to buy, but which marking method—fiber laser, dot peen, scribe, or mechanical engraving—matches your actual part material, surface condition, and permanence requirement. This article walks through how those processes differ in depth, speed, and durability, and why testing on real production parts matters more than any demo sample.
Why Part Marking Deserves More Than a Casual Equipment Decision
In fabrication and assembly shops, part marking often sits at the bottom of the priority list—until a faded serial number or an unreadable data matrix code stops a production line cold. A weak mark creates traceability gaps, confuses assembly teams, slows inspection, and turns warranty analysis into guesswork. When a part fails in the field and the only identifier is a smudged or shallow mark, the cost of that failure multiplies quickly.
Choosing a metal engraving machine for permanent part marking is less about the label on the machine and more about the result you need on the part. The right choice depends on how permanent the mark must be, what material and surface you are marking, how fast the line runs, and whether the mark must stay readable after coating, handling, abrasion, or heat exposure. These variables interact in ways that a spec sheet rarely captures.
What Permanent Part Marking Really Means in Production
In industrial use, permanent marking usually means more than leaving a visible mark on metal. It often needs to do several jobs at once:
- Stay legible after handling, cleaning, or abrasion
- Support traceability through serial numbers, lot codes, or data matrix codes
- Remain consistent across different part geometries and surface conditions
- Fit into inspection, assembly, and quality-control workflows without adding rework
For one factory, permanence may mean a high-contrast code that remains scanner-readable on finished stainless parts. For another, it may mean a deeper mark that can still be identified after paint, blasting, or long service wear. Those are not the same requirement, and they should not lead to the same equipment choice.
Consider a manufacturer of hydraulic fittings. The mark on a fitting body must survive high-pressure washing, thread lubricant, and repeated wrench contact. A shallow annealed mark might look perfect on a clean sample but disappear after the first wash cycle. Meanwhile, a medical device maker may need a mark that is readable under a microscope but must not create stress risers on a thin-walled implant component. Both buyers use the term “permanent marking,” but their equipment needs diverge completely.
Why the Term Metal Engraving Machine Can Be Misleading
Industrial buyers often use “metal engraving machine” as a broad search term, but permanent part marking can be produced in several different ways. Some systems discolor the surface, some displace material, and some cut into the part more aggressively. That distinction matters because the workflow outcome changes with the process:
- A shallow, high-contrast mark may be ideal for fast traceability on finished parts
- A deeper mark may be better when parts face abrasion, repainting, or harsh service conditions
- A low-stress line may be more important on some structural or cosmetic components than maximum depth
If a buyer treats all marking methods as interchangeable, the machine may look acceptable during a demo but underperform once it reaches real production. The demo part is usually clean, flat, and positioned perfectly. Production parts are often oily, textured, curved, or loaded in a hurry. The gap between those two conditions determines whether the machine earns its keep.
The Main Machine Types Used for Permanent Metal Marking
| Machine Type | How the Mark Is Created | Common Production Fit | Main Strengths | Main Tradeoffs |
|---|---|---|---|---|
| Fiber Laser Marking System | Uses a concentrated beam to create contrast, annealing, etching, or shallow engraving effects depending on setup and material | High-volume traceability, serial numbers, logos, barcodes, and data matrix codes on many metal parts | Fast, clean, highly repeatable, and well suited to automated code marking | The right result depends heavily on material, surface finish, and required permanence level |
| Dot Peen or Micro-Percussion Marker | Displaces material with repeated impacts | Rough castings, forgings, structural parts, and deeper industrial identification | Durable marks and good performance on uneven or less refined surfaces | Can be noisier and may produce a less refined visual finish |
| Scribe Marking System | Creates a continuous line by dragging a stylus across the surface | VIN-style characters, chassis marking, and applications needing lower noise or reduced stress compared with impact marking | Clean line quality and good permanence for many identification tasks | Not always the best fit for dense, high-speed code marking workflows |
| Rotary or Mechanical Engraving Machine | Physically cuts into the material with a rotating tool | Nameplates, deeper decorative marks, and applications where defined cut geometry matters | True cut depth and strong permanence when depth is the priority | Slower for many traceability tasks and more dependent on tooling, fixturing, and tool wear control |
For wood, acrylic, and similar non-metallic applications, laser cutters and engravers are commonly used. Permanent part marking on metal, however, usually pushes buyers toward different source types or different marking methods altogether. The physics of the interaction between the beam and the material changes completely when you move from a polymer to a ferrous alloy.
Fiber Laser Marking: Speed and Contrast for Traceability
Fiber laser marking systems have become the default choice for high-volume traceability applications on metal parts. The concentrated beam can produce several distinct effects depending on how the parameters are set. Annealing creates a contrasting oxide layer without removing material, which works well on stainless steel and some titanium alloys. Etching removes a thin layer of material to create a shallow cavity. Ablation removes coatings or surface layers to expose the base material beneath.
The speed advantage is real. A fiber laser can mark a serial number or a 2D data matrix code in a fraction of a second, which makes it attractive for lines running hundreds or thousands of parts per shift. The process is non-contact, so there is no tool wear and no mechanical stress on the part. That matters for thin-walled components, precision-machined surfaces, and parts that cannot tolerate deformation.
However, the result depends heavily on material composition and surface condition. A fiber laser that produces a crisp, dark mark on a clean stainless sample may produce a barely visible mark on a cast aluminum part with residual oxide or on a steel part with a heavy mill scale. The wavelength of a typical fiber laser is absorbed differently by different alloys, and surface reflectivity plays a major role. Polished surfaces can reflect a significant portion of the beam, reducing the effective energy delivered to the material.
Surface preparation becomes a practical consideration. Some shops add a cleaning step before marking, which adds labor and cycle time. Others accept a lower-contrast mark and rely on verification systems to catch unreadable codes. Neither approach is wrong, but both should be part of the decision process before the machine is purchased.
Dot Peen Marking: Durability on Rough and Uneven Surfaces
Dot peen markers, also called micro-percussion markers, create marks by driving a carbide or diamond-tipped pin into the surface repeatedly. Each impact displaces a small amount of material, and the pattern of dots forms characters, logos, or 2D codes. Because the pin physically displaces material, the mark has real depth that survives abrasion, coating, and rough handling.
This method performs well on surfaces that give laser systems trouble. Rough castings, forgings with scale, heat-treated parts with oxide layers, and machined surfaces with residual coolant all respond predictably to dot peen marking. The pin does not care about reflectivity or surface chemistry. It simply displaces material wherever it contacts.
The tradeoff is noise and speed. Dot peen marking is audible in a production environment, and the cycle time is longer than laser marking for the same code content. The mark also has a characteristic dotted appearance that some customers find less visually refined than a laser mark. For applications where durability matters more than aesthetics, that is an acceptable trade.
Fixturing becomes more important with dot peen marking. The pin must contact the surface at a consistent angle and depth. If the part moves or vibrates during marking, the dot pattern becomes irregular and the code may fail verification. Shops that already have robust workholding for machining operations often adapt those fixtures for marking, but shops that expect to hold parts by hand will struggle with consistency.
Scribe Marking: Clean Lines with Lower Stress
Scribe marking systems drag a stylus across the surface to create continuous line characters. The stylus displaces material rather than cutting it away, which creates a groove with raised edges. This method is common in automotive and heavy equipment applications where VIN-style characters or chassis numbers must be readable and durable.
The main advantage over dot peen is line quality. Continuous lines are easier for human readers to interpret, and the mark has a cleaner appearance. The process also generates less noise and less mechanical stress on the part compared with impact marking. For thin-walled sections or parts that cannot tolerate deformation, scribe marking offers a middle ground between the shallow contrast of laser marking and the aggressive displacement of dot peen.
The limitation is speed for dense code content. Scribing a long serial number or a complex 2D code takes longer than laser marking the same content. The stylus must physically traverse the entire path of each character, and the process cannot match the speed of a galvanometer-driven laser beam. For applications that need only a few characters per part, the speed difference may not matter. For high-volume lines with dense code content, it will.
Mechanical Engraving: True Depth for Nameplates and Heavy-Duty Identification
Rotary or mechanical engraving machines use a rotating cutting tool to physically remove material from the surface. This produces a true cut with defined geometry and significant depth. The mark is not a surface treatment or a displacement pattern; it is a machined feature.
This method is the right choice when depth is the primary requirement. Nameplates, identification tags, and parts that will face extreme abrasion or repeated coating cycles benefit from the physical depth of a machined engraving. The mark remains readable even after the surrounding surface has worn or been repainted multiple times.
The tradeoffs are speed, tooling, and fixturing. Mechanical engraving is slower than laser or dot peen marking for most applications. The cutting tool wears and must be replaced or resharpened, which adds consumable cost and maintenance time. The part must be held securely to prevent vibration, which can degrade cut quality. And the process generates chips or dust that must be managed in the work area.
For shops that already run CNC machining centers, the concept of tooling and fixturing is familiar. The engraving machine is essentially a small machining center dedicated to marking. The learning curve is shorter for shops with that background, and the maintenance discipline carries over naturally.
The Selection Criteria That Actually Change the Outcome
The most reliable buying process starts with the part and the workflow, not the machine brochure.
Material and surface condition come first. Mild steel, stainless steel, aluminum, coated parts, plated parts, and machined surfaces do not respond the same way. A mark that looks sharp on a flat, clean sample may behave very differently on oily, textured, oxidized, curved, or heat-treated parts. The alloy composition matters as much as the surface finish. A 300-series stainless behaves differently from a 400-series stainless under laser marking. A cast aluminum part with high silicon content marks differently from a wrought aluminum alloy.
The required mark style also matters. If the part only needs a readable serial number before final packing, a high-contrast surface mark may be enough. If the code must survive blasting, coating, repainting, or aggressive service wear, deeper displacement or engraving may make more sense. The distinction between “readable now” and “readable after service” is the single most important question in the selection process.
Throughput should be evaluated at the line level, not just per mark. The marking cycle, part loading method, fixture repeatability, operator handling, and verification step all affect actual output. A fast marking head does not solve a slow handling method. A shop that marks 500 parts per shift with a 10-second cycle may actually be limited by the 15 seconds it takes an operator to load and unload each part. Adding a faster marking head does nothing for that bottleneck.
Code quality requirements are equally important. Human-readable text, logos, UID-style codes, and scanner-dependent 2D codes do not place the same demands on the process. Some workflows care most about visual depth, while others care most about contrast, edge definition, and consistent readability under scanners. A data matrix code that must be read by a fixed-mount scanner on a conveyor has different requirements than a serial number that will be read by a human inspector with a magnifying glass.
Integration is another common dividing line. Some factories need a standalone workstation. Others need the marker to fit into a conveyorized line, robotic cell, or multi-station traceability process. In those cases, software handshake, fixture strategy, part orientation, and verification logic matter as much as the marking method itself. A machine that cannot communicate with the plant’s MES or ERP system will create data entry errors and manual workarounds.
When Depth Matters More Than Speed
Buyers sometimes focus too heavily on speed because it is easy to compare. In practice, the better question is whether the mark still does its job after the part leaves the marking station.
If the part will be painted, coated, blasted, or exposed to long-term abrasion, a deeper mark is often worth the slower cycle. A laser mark that is only a few microns deep may disappear under a single coat of powder coating. A dot peen mark or a mechanically engraved mark will remain visible through multiple coating cycles.
If the part is already finished and the real goal is rapid, repeatable traceability with scanner readability, a faster surface-oriented marking process may be the better fit. A medical device that is marked after final polishing does not need a deep mark. It needs a high-contrast code that a scanner can read reliably at the packaging station.
This is why sample testing should reflect the real workflow:
- Mark the actual production material, not a cleaner substitute sample
- Test before and after any coating, washing, or surface treatment
- Verify the mark with the same scanner or inspection standard used on the line
- Check the result on flat, curved, and tolerance-sensitive parts if those variations exist in production
The wrong test sample often leads to the wrong machine. A buyer who approves a laser system based on a clean, polished sample may discover that the actual production parts have a residual oil film that absorbs the beam differently. A buyer who approves a dot peen system based on a flat plate may struggle when the production part has a curved surface that changes the pin contact angle.
A Practical Shortlist by Production Priority
| If Your Priority Is… | The Process Often Considered First |
|---|---|
| Fast, repeatable serial numbers or 2D codes on metal parts | Fiber laser marking |
| More durable identification on rough or uneven industrial parts | Dot peen or micro-percussion |
| Cleaner line marking with lower noise in some identification workflows | Scribe marking |
| Deeper cut geometry or decorative engraved detail | Mechanical engraving |
This is not a rulebook. It is a shortlist. Final selection still depends on the exact metal, surface state, mark specification, and production environment. A shop that marks stainless steel surgical instruments will not make the same choice as a shop that marks cast iron pump housings, even though both use the term “permanent part marking.”
Buying Errors That Put a Metal Engraving Machine for Permanent Part Marking at Risk
One common mistake is buying by machine category instead of mark requirement. A buyer may decide they need engraving when what they really need is durable machine-readable marking. The opposite also happens: a buyer chooses a fast marking method when the application really needs greater physical depth. The machine category is a means to an end, not the end itself.
Another mistake is approving the process on ideal samples only. Permanent part marking should be evaluated on real parts with real finishes and real handling conditions. The sample that comes with the sales demo is almost always cleaner and flatter than the production part. The evaluation should include parts that have been through the actual manufacturing process, with the same oils, oxides, and surface variations that the production line produces.
A third mistake is ignoring downstream verification. If the code must be scanned later in packaging, assembly, warehousing, or field service, that requirement should shape the machine choice from the beginning. A mark that looks good to the human eye may fail a scanner read if the contrast is insufficient or the edge definition is poor. The verification standard should be defined before the machine is selected, not after.
Fixturing is also frequently underestimated. Even a capable marking system can produce inconsistent results if part position, focal consistency, or workholding stability varies too much. A laser system needs consistent focal distance. A dot peen system needs consistent pin contact angle. A mechanical engraver needs rigid workholding to prevent chatter. Shops that invest in good fixtures during the initial installation avoid a steady stream of rejected marks later.
Maintenance and consumables are another area where buyers underestimate the long-term cost. Laser systems have no mechanical tool wear, but they do have cooling systems, optics, and protective windows that need attention. Dot peen markers have pins that wear and must be replaced. Mechanical engravers have cutting tools that dull and break. The total cost of ownership includes these consumables and the labor to manage them.
What Industrial Buyers Should Clarify Before Requesting Quotes
Before comparing suppliers, buyers should document a few basics clearly:
- The exact part materials and surface conditions
- The required mark content, size, and readability standard
- Whether the mark must survive coating, wear, heat, or outdoor service
- The expected throughput and loading method
- Whether the system will be standalone, semi-automated, or fully integrated
Clearer inputs usually lead to better sample trials, more relevant quotations, and fewer surprises after installation. A supplier who receives a clear specification can recommend the right process and configure the machine appropriately. A supplier who receives a vague request will often default to the machine they sell best, which may not be the machine that solves the problem.
The mark content itself deserves careful definition. A serial number with a specific character height and font has different requirements than a data matrix code with a specific cell size and contrast ratio. The readability standard should specify the scanner model, the lighting conditions, and the acceptable read rate. These details turn a vague requirement into a measurable specification.
The integration requirement should also be documented. Does the machine need to communicate with a PLC, an MES system, or a barcode scanner? Does it need to receive part data from an upstream station or send verification results downstream? The software interface is often the most underestimated part of a marking system purchase.
Selection Focus: a Metal Engraving Machine for Permanent Part Marking
The best metal engraving machine for permanent part marking is not always the one that makes the deepest mark or the fastest mark. It is the one that creates a reliable result under your actual production conditions and supports the traceability, inspection, and durability requirements that matter to your operation.
For many industrial buyers, the real decision is not simply engraving versus not engraving. It is whether the job calls for laser marking, impact marking, scribe marking, or true mechanical engraving. Once that is clear, comparing machines becomes much more practical and much less risky.
The selection process should start with the part, the surface, the mark specification, and the production environment. It should include sample testing on real production parts, verification with the same scanners used on the line, and a clear understanding of how the machine will integrate with existing workflows. A machine that passes those tests will earn its place on the floor. A machine that only looks good in a demo will create rework, delays, and frustration.
Part marking is not a decorative step. It is the foundation of traceability, quality control, and warranty management. The machine that produces those marks deserves the same careful selection process as any other piece of production equipment.