Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
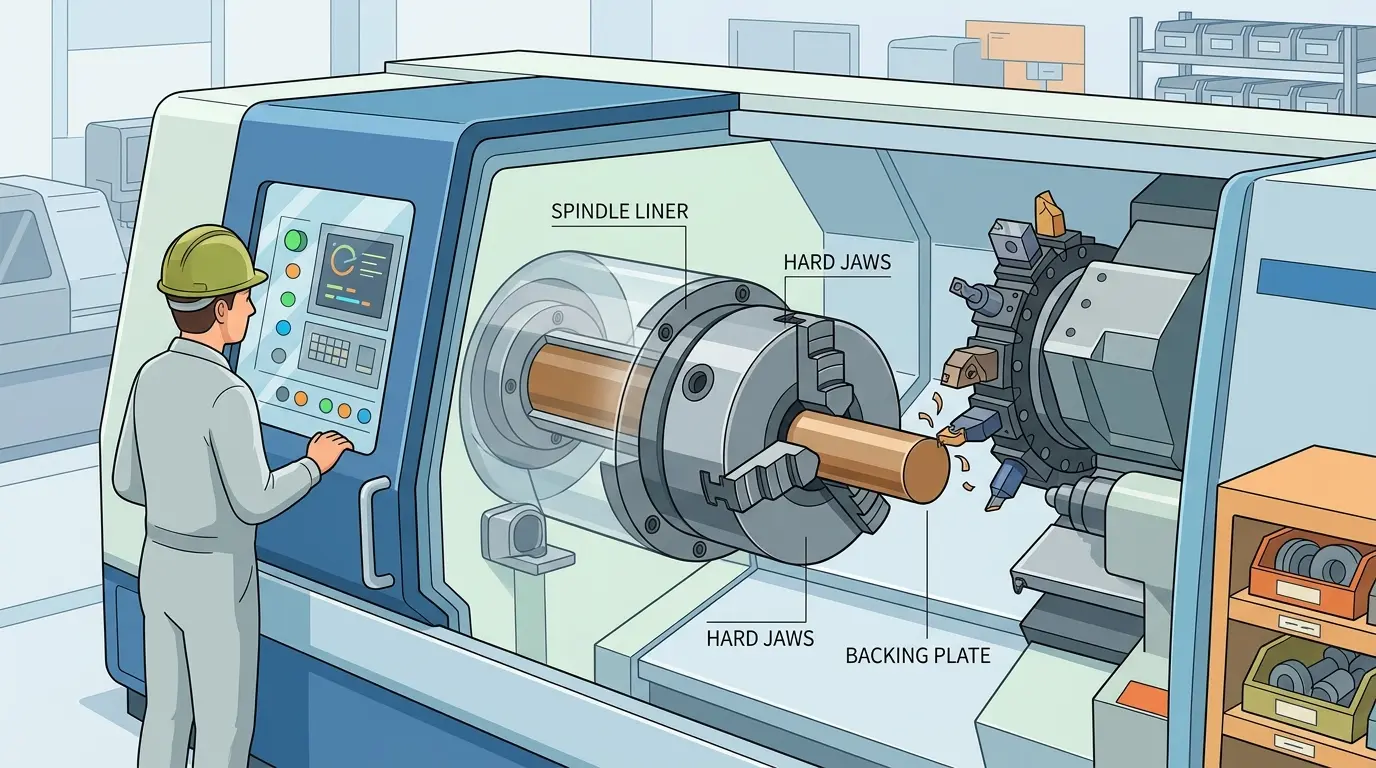
When a CNC lathe starts producing taper, chatter, or drifting diameters, most shops immediately blame the insert or the program—but the fault often sits in the workholding chain that transfers spindle truth to the stock. Spindle liners, hard jaws, and backing plates rarely get the scrutiny they deserve, yet a mismatched liner, a jaw chosen by habit, or a casually mounted backing plate can turn a capable machine into a source of unexplained vibration and poor finish. This article walks through how to diagnose symptoms through the support system, match setup hardware to part families, and treat these quiet components as controlled process tools rather than forgotten accessories.
Start With The Workholding Chain, Not The Cutting Tool
When a CNC lathe starts producing taper, chatter, or drifting diameters, the first instinct on most shop floors is to change the insert, adjust the program, or question the operator. Those are reasonable checks, but they often miss the real source of the problem. In many turning operations, the fault sits much closer to the spindle—in the setup hardware that holds, supports, and mounts the work.
Spindle liners, hard jaws, and backing plates rarely appear in machine brochures, and they do not generate much excitement during a capital equipment review. But they form the mechanical chain that transfers the spindle’s rotational truth to the stock. When that chain is weak, mismatched, or worn, the cutting tool receives a distorted version of what the machine is actually doing. The result is a lathe that behaves unpredictably even with fresh tooling, clean code, and an experienced operator at the controls.
The practical way to think about these components is not as individual accessories but as one integrated workholding system. The stock enters the spindle bore. The spindle liner supports and contains it. The chuck grips it. The backing plate mounts the chuck to the spindle face. If any link in that sequence is compromised, the symptoms show up downstream as vibration, poor finish, dimensional drift, or wasted setup time.
Why Spindle Liners Are A Safety And Stability Component
Spindle liners are commonly described as sleeves that adapt a larger spindle bore to a smaller bar diameter. That description is technically correct but commercially misleading. The liner’s real job is to support rotating stock consistently along its path through the spindle, reduce unsupported length, and keep the bar running true.
When a shop runs bar stock significantly smaller than the spindle bore without a liner, several problems appear quickly. Bar whip risk increases, especially at higher spindle speeds. Vibration becomes harder to diagnose because it originates inside the spindle rather than at the cut. Surface finish degrades. Chatter and taper can appear even when the cutting parameters look reasonable.
The safety dimension matters just as much as the quality dimension. An unsupported bar whipping inside a large spindle bore is a hazard waiting for a failure event. A properly selected liner contains the stock, reduces deflection, and keeps the bar path predictable.
Liner selection should follow actual bar strategy, not just nominal diameter. Ask these questions before choosing a liner:
- How much of the bar will remain unsupported between the chuck and the spindle exit?
- How straight and stable is the raw stock itself?
- How often does the shop run the same bar size?
- Is the work mostly short chucked parts, longer bar-fed jobs, or a mix that changes frequently?
Shops that standardize liner decisions by bar family and document those choices avoid the common trap of reusing a liner that “usually works” long after it stopped being the right fit. When vibration is blamed on cutting conditions but the support path has already degraded, the setup is the problem, not the tool.
Hard Jaws Reward Repeat Production, Not Variety
Hard jaws earn their place in a turning operation when the part family is stable enough that repeat gripping behavior matters more than geometric adaptability. In repeat production, hard jaws provide predictable holding with less need to remake gripping surfaces every time a job returns. That predictability translates directly into faster setups and more consistent part geometry across runs.
But hard jaws are not a universal solution. When part geometry changes frequently, when controlled deformation is a concern, or when the gripping surface needs to match a specific part family closely, soft jaws remain the better choice. The mistake is treating one jaw type as superior in all situations. Each jaw strategy belongs to a different production logic.
Buyers and supervisors should evaluate jaws by part family stability, not by habit. Repeat work rewards standardization. Mixed work rewards adaptability. A shop running the same shaft family every week will benefit from hard jaws that return to the same gripping position reliably. A job shop taking on varied geometries will find soft jaws more practical because they can be machined to fit each new part.
Grip Behavior Affects Quality, Not Just Holding
Many shops evaluate jaws only on whether the part slips during the cut. That is a narrow view. Grip behavior also influences part deformation, concentricity, repeatability between setups, and how confidently the operator can push the cycle once the machine is running.
A jaw setup that holds the part but distorts it is not a successful setup. This becomes especially important on thin-wall components, longer unsupported turning, and short repeat jobs where setup time must stay low without sacrificing trust in the workholding. In those cases, jaw strategy should be treated as part of the quality plan, not just as basic clamping.
Consider the gripping force distribution. Hard jaws apply force across their full contact surface, which is fine for rigid parts but can crush or distort thin-wall components. Soft jaws machined to the part contour spread the load more evenly and reduce deformation risk. The right choice depends on the part, not on what is already sitting in the tool crib.
Backing Plates Are Structural Interfaces, Not Background Hardware
Backing plates seem uninteresting until something vibrates, shifts, or becomes hard to explain. Their job is to connect the chuck body to the spindle in a way that preserves alignment, balance, and mechanical confidence. A poor match, worn mounting condition, or casually handled interface can turn the chuck assembly into a vibration source instead of a control point.
Backing plates should not be treated as interchangeable hardware unless compatibility is fully understood. Bolt pattern, fit, mounting condition, and assembly care all matter. When the interface is wrong, the spindle may still run, but the workholding truth reaching the part has already degraded.
A quality chuck does not protect the shop from a careless mounting interface. The full assembly depends on how the backing system locates and supports the chuck body. If the interface is worn, contaminated, poorly matched, or reassembled without discipline, the entire chuck system can start behaving unpredictably.
Backing plates deserve inspection standards and setup discipline of their own. They should be clean, controlled, and treated as precision mating parts. The more a shop values repeatability, the less acceptable it becomes to treat the chuck-to-spindle interface casually.
Match Setup Strategy To The Part Family
The right combination of liner, jaws, and backing hardware depends on the work. Long bar runs, repeat shafts, short chucked parts, thin-wall components, and mixed small-lot jobs all ask different things from the setup system. Standardization should not mean using the same hardware strategy everywhere. It should mean choosing deliberately and documenting what belongs where.
A useful rule is to identify which risk matters most on the current job:
- Bar instability?
- Grip inconsistency?
- Setup time?
- Vibration?
- Cosmetic finish?
- Part deformation?
The best setup hardware choice is the one that reduces the dominant risk for that work family. Shops that make these choices explicitly usually get faster setups and fewer unexplained quality problems because the setup itself has become part of the production method.
Read Symptoms Through The Support System
When turning problems appear, setup hardware should be part of the first diagnostic pass. Vibration at speed, inconsistent finish from one run to the next, unexplained taper, bar instability, and poor repeatability can all trace back to workholding choices that were treated too casually.
Shops sometimes burn hours swapping inserts or adjusting code when the real issue is a liner mismatch, a jaw choice that no longer fits the part family, or a mounting interface that is no longer trustworthy for the load and speed. Experienced teams learn to read symptoms through the support system, not only through the cutting tool. The faster the symptom is connected to the supporting hardware, the faster the machine returns to predictable output.
Workholding Hardware Needs Its Own Maintenance Logic
Setup components are often ignored in maintenance planning because they are not powered components. But they still wear, collect damage, and influence the process directly. Liners can stop matching the stock family being run. Jaw surfaces can stop reflecting the needs of the current parts. Mounting faces and backing interfaces can accumulate contamination or wear that appears later as vibration or drift.
Workholding hardware deserves cleaning, inspection, and replacement standards just as much as cutting tooling does. When it is treated casually, turning problems start appearing as “machine issues” even though the machine itself is not the first source. These parts sit quietly until they fail, and then they distort the whole conversation.
A Practical Matrix For Matching Setup Parts To Turning Needs
Use the table below to connect setup hardware to the real turning risks it controls.
| Turning Need | Component Emphasis | Why It Matters |
|---|---|---|
| Smaller bar in a larger spindle bore | Spindle liners | Improves support and reduces unsafe unsupported space |
| Repeat family with stable gripping geometry | Hard jaws | Supports consistent gripping behavior and faster return setups |
| Part families sensitive to deformation or shape-specific holding | Jaw strategy review, often beyond standard hard jaws | Protects geometry and grip accuracy |
| Chuck-to-spindle reliability | Backing plate quality and interface care | Protects alignment, balance, and assembly stability |
| Better finish and lower vibration | All three working together | Workholding stability shapes cut behavior before tooling can help |
| Multi-shift repeatability | Documented setup hardware standards | Reduces dependence on memory and operator variation |
Standardization Beats Experience Alone
These components are easiest to manage well when the shop documents which liner, jaw approach, and chuck-mounting arrangement belong to each repeat family of work. Without that, setup quality depends too much on who is present and what they remember from the last run. That is risky in any shop and especially costly in repeat production turning.
Standardization does not mean forcing every job into the same hardware recipe. It means making the correct recipe visible enough that it can be repeated confidently. That is often the difference between calm repeat setups and recurring mystery variation.
Documentation also shortens recovery time. If a setup has to be rebuilt after time away from the job, the shop should not have to rediscover which liner and gripping logic made the part behave correctly. Good setup records protect uptime as much as they protect quality.
Supervisors Should Ask Setup Questions First
If turned parts are drifting, a good supervisor should ask where the workholding assumptions live. Is the stock supported correctly? Are the jaws right for this family? Is the chuck mounting trusted for the current load and speed? Has the setup hardware been reviewed recently, or only reused because it seemed acceptable last time?
These questions often reveal more than another round of insert changes or offset edits. They also make it easier to separate process problems from operator problems. In many cases, the operator is dealing with a setup chain that was already unstable before the program began. The more repeat output matters, the more these setup questions become part of quality control rather than background hardware discussion.
Training Improves When These Parts Are Named Correctly
Another reason these components deserve more attention is training consistency. In many shops, newer operators or setup technicians learn tooling and offsets first, then absorb workholding details informally from whoever happens to be nearby. That usually creates uneven habits. One person learns to care about spindle support. Another thinks jaws are only about grip force. A third never gets taught that the chuck mounting interface can quietly create quality drift.
When the shop names liners, jaws, and backing plates as process controls instead of accessory hardware, training improves. New staff begin to understand that liners affect rotational support, jaws affect repeat gripping behavior, and backing plates affect chuck truth before a tool even touches the part. That shared language makes troubleshooting faster and setup reviews less dependent on memory.
This matters most in repeat turning environments where output must stay stable across shifts. The machine may be the same, but the quality of setup vocabulary often decides whether the process can actually be repeated with confidence.
Quiet Hardware Is Real Process Control
Spindle liners, hard jaws, and backing plates matter because they determine how reliably the spindle system transfers truth to the part. They affect safety, stability, finish, and repeatability long before the insert reaches the material.
Treat them as controlled setup tools, not as forgotten metal hanging near the lathe. Shops that do that usually spend less time chasing mystery vibration and more time making parts that behave the way the machine was supposed to behave in the first place. For shops evaluating turning equipment or upgrading existing cells, reviewing the workholding chain alongside the machine purchase is the practical way to protect the investment.