Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
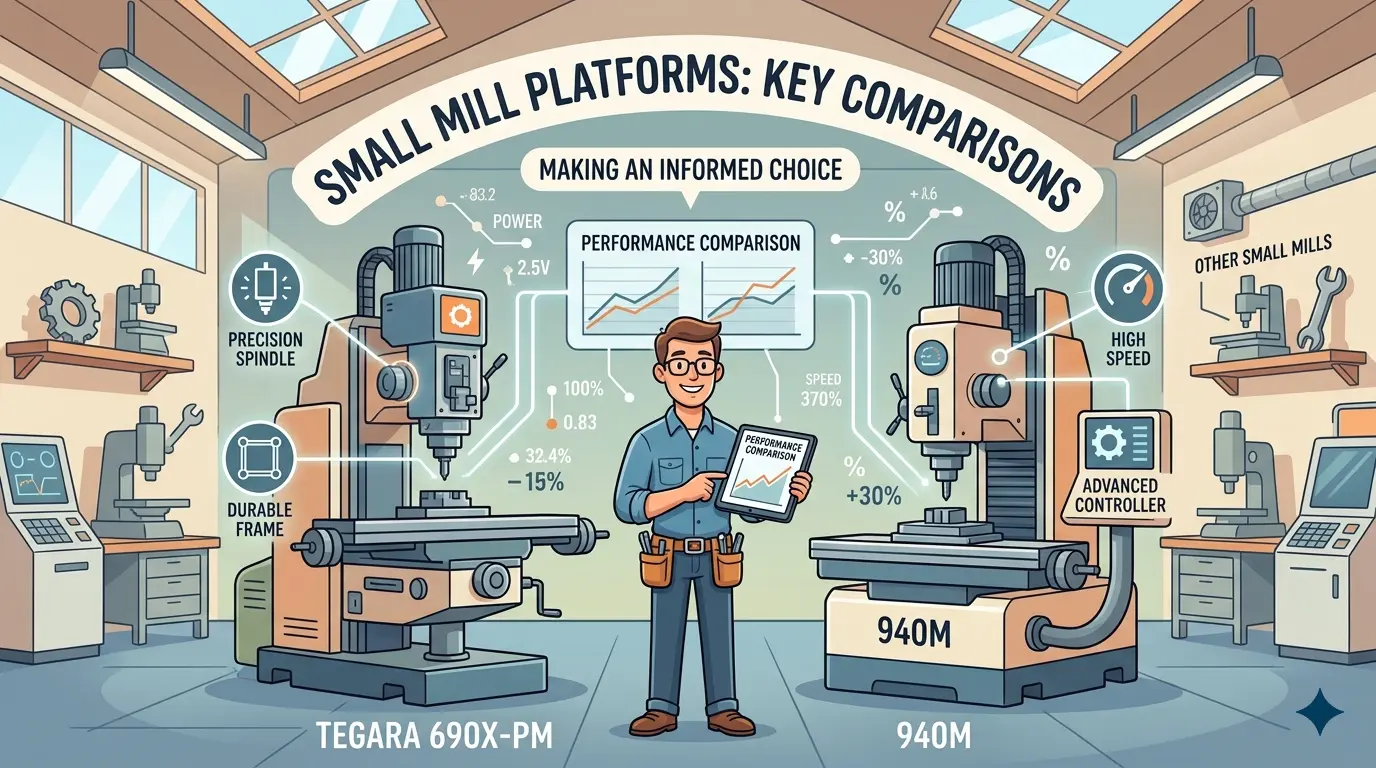
Small mill buyers routinely compare travel numbers and model names while ignoring the ownership path each platform demands. This article separates three distinct routes—heavier toolroom-style mills, purpose-built compact CNCs, and retrofit or open-build systems—and shows why that distinction matters more than table size. The real decision hinges on control philosophy, coolant and chip strategy, and operator burden, because a machine that fights the shop’s workflow will cost more in labor and troubleshooting than its price tag suggests. Match the platform to your actual operating reality before comparing specifications.
Small Mill Buyers Are Comparing Three Different Machine Philosophies
The search results look similar. Compact milling machines with familiar model names, comparable travel numbers, and forum threads full of owner opinions. But the machines behind those search listings often belong to three distinct ownership paths that behave very differently on the shop floor.
The first path is the heavier small mill or toolroom-style platform. These machines offer more mass and cutting confidence than desktop equipment while keeping a familiar, operator-involved workflow. The second path is the purpose-built compact CNC machine, designed from the start for structured operation with enclosure, coolant, and a more complete control environment. The third path is the retrofit or open-build route, where the buyer combines machine structure with a chosen control system and accepts a significant integration workload.
All three paths can produce good parts. They do not, however, ask the same things from the owner. One rewards mechanical familiarity and patient setup work. Another rewards process discipline and supporting infrastructure. A third shifts cost savings directly onto owner effort and troubleshooting time.
Buyers who skip this distinction end up comparing unlike systems. They wonder why one machine feels cheap but complicated while another feels expensive but calmer in daily use. The more productive approach is to decide which ownership path fits the shop before comparing individual model names inside that path.
Platform Architecture Matters More Than Table Travel
Travel numbers are easy to compare. They create the illusion of objective measurement. More travel seems like more machine, and buyers naturally gravitate toward the larger envelope.
In practice, travel only matters once the platform underneath it makes sense for the work. A slightly larger envelope on a machine the shop cannot support, maintain, or run confidently is not a real advantage. It is theoretical reach on paper.
What matters earlier is how the machine is built to be used. Does it assume enclosure and coolant discipline, or is it happier in a drier, more open environment? Does the control path favor straightforward repetitive workflow, or does it expect a mechanically engaged owner? Does the support structure around the machine feel like a complete operating system, or does the owner need to assemble that system personally?
These questions are more predictive than raw travel because they tell you whether the machine will settle into daily use or remain an ongoing integration project. A machine that fits the shop’s actual operating style will produce more usable output than one with slightly more travel that fights the workflow.
Control Philosophy Decides The Purchase Before The First Cut
In this market tier, buyers consistently underestimate how much the control approach shapes long-term satisfaction. Some platforms appeal because they promise straightforward small-shop ownership with familiar CNC expectations. Others appeal because they allow the owner more freedom to configure or adapt the system around personal preferences.
Neither path is automatically superior. They create very different workloads for the team.
This matters most when the shop does not have one dedicated machine person carrying all troubleshooting and process refinement. A platform that depends on active tinkering may look economical at purchase and then create friction once multiple users need the machine to behave consistently. A more structured control environment may cost more upfront but reduce the background effort required to keep the machine dependable.
Control philosophy belongs near the top of the comparison list for this reason. The machine that feels best in a single-owner technical environment may not be the one that makes sense in a small business with shared responsibility and delivery pressure.
Coolant And Chip Strategy Separate Serious Use From Hobby Thinking
Small mill shoppers often focus on the cutting event itself and ignore the rest of the workday. Chip control and coolant readiness strongly influence whether the machine remains pleasant to use over months of real ownership.
If the platform will handle repeat metal work, fixtures, or paid prototype jobs, chip containment and coolant behavior stop being secondary details. They become part of whether the machine can be integrated into a stable routine. A machine that looks fine in a short video can become exhausting if the owner spends too much time managing mess, improvising splash control, or working around an environment never prepared for repeated cutting.
This is one reason compact enclosed options and heavier open small mills are not direct substitutes. They may appear in the same search session, but they ask for very different shop behavior. An open mill without coolant containment can work well for occasional jobs with careful cleanup. The same machine becomes a constant source of friction when running daily production.
Operator Burden Is The Most Honest Long-Term Cost
Small mill platforms in this tier often differ less in whether they can make a part and more in how much operator burden they impose while doing it. Burden includes setup sensitivity, workholding awkwardness, cleanup, troubleshooting, and how much machine behavior depends on one skilled person remembering every quirk.
This is where some machines become excellent stepping stones and others become permanent side projects. If the platform gives the buyer more milling confidence but also consumes disproportionate attention, it may not really be cheaper than a more structured option. The cost has simply moved into labor and cognitive load.
Buyers should be explicit about this trade-off. Is the shop willing to own a platform that asks for active involvement and mechanical patience? Or does it need a machine that is calmer, more repeatable, and easier to hand off between operators? The answer changes the shortlist dramatically, and it has very little to do with model prestige.
Heavier Small Mills Work Well When The Work Stays In Their Lane
It is important not to overcorrect and assume the more structured or turnkey-looking platform is always the right answer. Heavier small mills and toolroom-adjacent platforms can be excellent when the workload is well understood.
For prototyping, toolroom support, fixture work, repair components, and low-to-moderate volume metal parts, these machines provide real confidence without requiring the scale or cost of a mainstream production VMC. The operator gets mechanical access, familiar controls, and a direct relationship with the cutting process.
The key is lane discipline. If the machine will mostly handle modest-size parts with predictable setups, and the owner values mechanical access and a hands-on relationship with the platform, that can be a very rational purchase. Problems start when the shop quietly expects the same platform to absorb growth into more continuous, more commercial, or more diverse workloads than the original buying logic supported.
In that situation, the platform is not failing. The shop is using the wrong tier as a growth substitute.
Purpose-Built Compact CNC Platforms Earn Their Cost Through Calmness
Purpose-built compact CNC machines in this broader small-mill conversation often justify themselves less through raw capacity than through calmness. They feel more settled as systems. Setup, control, enclosure, and daily operation require less improvisation. That matters a great deal to a small shop that wants to spend its time making parts rather than refining the machine ecosystem around the parts.
This does not make them automatically superior to all heavier manual-heritage platforms. It means buyers should understand what they are paying for. In many cases, they are paying for a more complete operating environment, not just for motion or spindle numbers. If that reduces friction enough to make the machine usable across more jobs or more operators, the price difference can be commercially justified.
Buyers drifting toward this lane should evaluate the broader ownership logic of compact enclosed mills rather than pretending all small mills solve the same problem. The purchase decision should reflect how the machine will actually be used, not how it looks in a specification table.
Retrofit And Open-Build Thinking Can Save Money Or Move Risk Onto The Owner
Some buyers in this category are not only comparing stock machines. They are also comparing the idea of a machine platform plus an owner-selected control or build path. That can be reasonable, especially for technically confident buyers who want flexibility and understand the integration burden.
It should be treated honestly. Cost savings here are often real only if the owner’s time is cheap or if the shop already has the right technical depth. In commercial environments, risk moves quickly when the platform depends on one person to interpret every behavior and solve every control issue.
That does not mean these routes are bad. They belong to a specific buyer type. If the team expects more standardized ownership, open-ended integration can become a liability. Buyers considering those paths should review the broader warning signs in open retrofit platforms for small mills, because that is often where cheap flexibility becomes a permanent machine project.
Service, Parts, And Documentation Matter More Than Brand Familiarity
Well-known names create comfort, but small-mill ownership rarely lives on comfort alone. The real test is how easy it is to keep the machine working when something drifts, fails, or needs replacement.
Documentation quality, part availability, communication speed, and whether the supplier actually understands the buyer’s use case all influence long-term satisfaction. This matters especially in the small-mill tier because these purchases are often made by shops that do not maintain large internal service departments.
If the support path is weak, even a mechanically attractive machine can feel risky. If the support path is clear, a less glamorous platform can become a safer commercial choice. Buyers should stop asking only whether a machine is good and start asking whether it is supportable in their region, by their team, under their real operating schedule.
Compare By Buyer Type, Not By Brand First
A useful way to keep the shortlist honest is to match platform type to buyer type.
If you are a technically confident individual owner who accepts hands-on adjustment and values flexibility, the heavier small-mill or open-ended platform path may suit you. You will get mechanical access and control freedom in exchange for your own time and troubleshooting effort.
If you are a small shop that needs a dependable prototype-and-fixture machine shared by more than one operator, a more structured compact CNC platform may be worth the extra spend. The higher purchase price buys consistency and reduced operator burden.
If you are an internal toolroom that wants more milling confidence than desktop equipment provides but still expects strong operator involvement, the answer may sit between those two paths. You need enough structure to keep work moving but enough access to handle varied jobs.
The point is not to force every buyer into the same conclusion. It is to stop comparing machines as though the same ownership logic applies to all of them.
The Best Small Mill Platform Matches Your Growth Pattern
The final comparison point is growth. Not abstract growth, but actual growth in workload. Will the machine remain in a prototype-and-toolroom lane? Will it become a paid short-run asset? Will more operators touch it next year than touch it today? Will the business expect enclosure, coolant routine, and faster turnaround from it as it becomes more central?
These questions determine whether the current platform choice is a stepping stone or a trap. A platform that is excellent for today’s single-operator prototype work may become awkward when the shop asks it to support more formal commercial activity. Conversely, a platform that looks expensive today may end up cheaper if it absorbs growth without forcing a second purchase too quickly.
Buyers should compare small mill platforms by ownership path, control burden, support, and growth pattern first, and by model name second. Once those issues are clear, the right shortlist usually narrows on its own. The machine that fits the shop’s actual operating reality will always outperform the one that merely looks good in a specification sheet.