Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
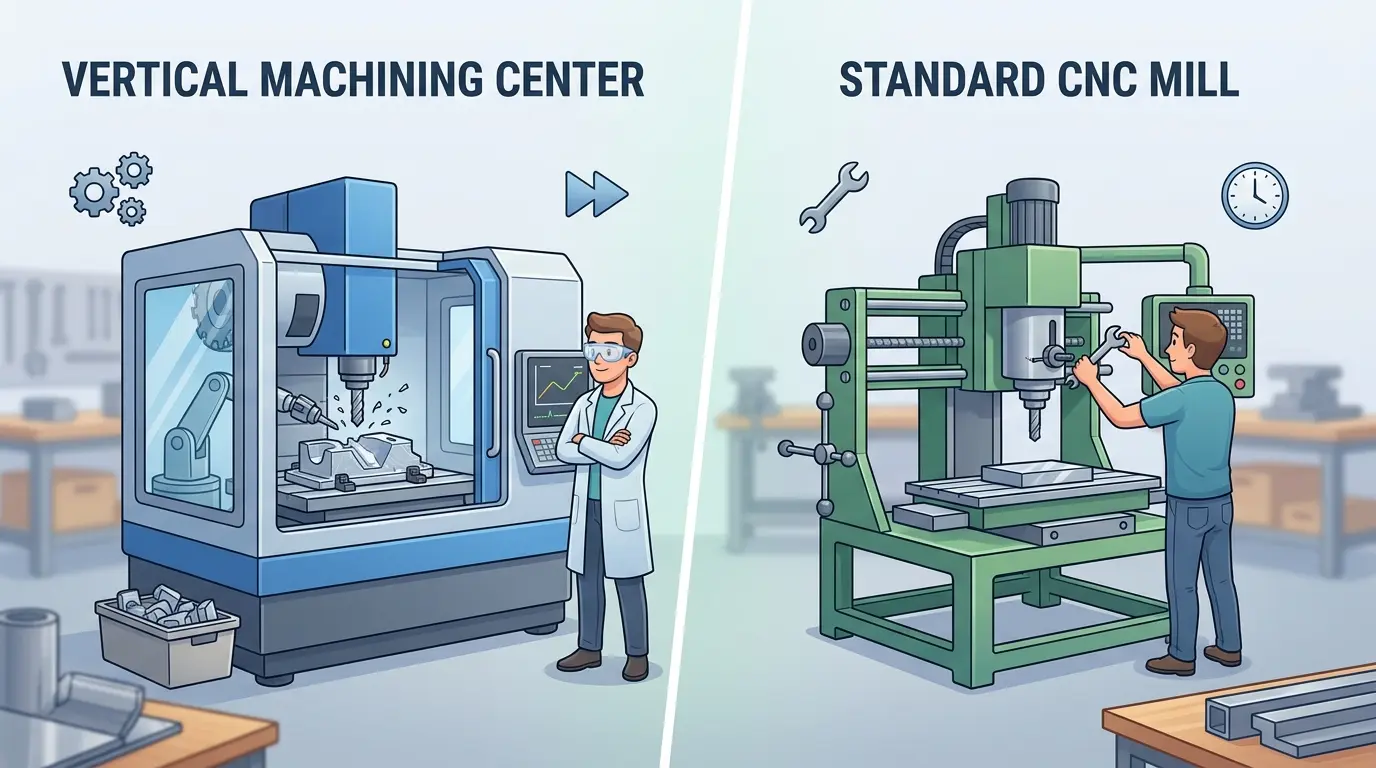
When a quote lists “CNC mill,” the real decision is not spindle speed or axis count—it is whether your shop needs an operator-led platform or a process-packaged production system. This article separates the practical tiers hiding under that label, from toolroom mills that reward quick intervention to VMCs that bundle automatic tool handling, coolant control, and chip evacuation into repeatable workflow. Before you compare spec charts, you must decide whether your part mix, labor structure, and setup culture will actually use that added infrastructure often enough to justify the capital.
Start With the Workload, Not the Label
Most buying conversations treat “CNC mill” as a complete answer. It is not. The term covers everything from a manual knee mill retrofitted with a control to a fully enclosed vertical machining center (VMC) with a 30-tool magazine and chip conveyor. When the budget gets serious, that distinction matters because you are no longer buying axis motion. You are buying a process package.
The confusion becomes expensive when sellers use the terms interchangeably. A VMC is not simply a CNC mill with a better paint job. It is a different production philosophy. The practical difference is not that one cuts metal and the other does not. Both produce accurate parts. The difference is how much production infrastructure comes with the machine and how much process repeatability the builder expects you to need.
The most useful way to frame the comparison is not “simple versus advanced.” It is “operator-led process versus process-packaged machine.” A standard CNC mill leaves more of the system in the operator’s hands. A VMC packages more of that system into the machine itself. The real question is how mature, repetitive, and structured you want your milling process to become.
What “Standard CNC Mill” Actually Covers
That phrase describes several distinct machine tiers. It may refer to a CNC-equipped knee mill, a bed mill, a toolroom platform, or a lightly enclosed vertical mill that still depends heavily on operator involvement. What these machines share is milling under numerical control. What they do not share is the same production expectation.
A standard CNC mill is usually bought for flexibility. Toolrooms, repair departments, prototype spaces, training environments, and mixed short-run job shops value accessibility, lower capital exposure, and fast operator intervention more than deep automation. In those settings, the operator stays close to the process. Tool changes may remain manual. Setup logic stays adaptive. The machine behaves more like a highly capable workbench than a tightly standardized production cell.
That does not make the machine lesser. It makes it appropriate for a different kind of work. If your jobs change constantly and your operators need to intervene quickly, a simpler platform may serve you better than a fully automated one.
What a VMC Adds Beyond Spindle Motion
A vertical machining center usually includes more than programmed axes and spindle speed. It packages the machine for repeated production use. Automatic tool changing, better coolant delivery, more consistent chip evacuation, full enclosure, formal work-offset logic, probing compatibility, and cleaner integration of repeat cycle execution are typically part of the value proposition.
That is why a VMC often feels less like a standalone mill and more like the foundation for a milling cell. The machine is designed so that tooling, setups, and programs can be repeated with less improvisation. The more frequently you run recurring parts or families of parts, the more valuable that stability becomes.
This is the difference buyers should actually watch. A VMC is usually not just more machine. It is more process system.
Tool Handling Is Where the Workflow Diverges First
Manual or lightly managed tool changing is not automatically a problem. In short-run, prototype, and toolroom work, it can be completely rational. The issue appears when your job mix starts relying on more tools, more repeated setups, and tighter cycle consistency.
A VMC’s automatic tool handling changes more than convenience. It changes how the whole shop thinks about setup:
- Tool libraries become structured and searchable.
- Repeat jobs are easier to re-enter without re-teaching offsets.
- Program logic assumes a stable machine state between cycles.
- Operator interruption drops, freeing labor for other tasks.
On a standard CNC mill, the same work may still be possible, but it often creates more interruption, more chances for tool-handling mistakes, and greater dependence on one operator’s habits. Measure your tool count honestly. If typical jobs use very few tools and change constantly, a simpler machine may be enough. If your part mix is already complex enough that tooling organization is becoming daily overhead, the VMC starts earning its price quickly.
Enclosure, Coolant, and Chip Control Are Production Features
One common mistake is to treat enclosure and coolant management as comfort extras. On real metal-cutting work, they are process controls. Better enclosure changes safety, chip containment, cleanliness, and operator confidence. Better coolant delivery changes tool life, heat control, and finish stability. Better chip evacuation changes whether the machine can stay productive through longer cuts without constant cleanup or recutting debris.
This is where VMCs often separate themselves clearly from simpler mills. The machine is not just more enclosed. It is more prepared to keep production conditions stable. If you are making heavier cuts, running repeated cycles, or trying to reduce operator hovering, those systems matter more than many buyers expect.
If your work is light, intermittent, and highly interactive, those VMC advantages may be less valuable. The more manual and irregular the work remains, the more likely it is that a portion of the VMC package will sit underused.
Workholding and Offsets Reflect Different Setup Cultures
A standard CNC mill often lives in a more adaptive setup culture. Operators may touch off frequently. Fixtures may change informally. Jobs may be treated as individual events rather than as repeatable process programs. There is nothing wrong with that if it matches your work. It is common and rational in toolrooms and prototype spaces.
A VMC tends to reward more formal process habits. Repeatable fixtures, consistent holders, probing routines, stored offsets, and documented setup logic all become easier to justify because the machine can reuse that structure profitably. The more stable your setup culture becomes, the more a VMC behaves like a production asset rather than just a sophisticated mill.
This is also why some factories underuse VMCs. They buy the machine but never change the process culture around it. The result is a production-oriented platform being used like a manually interrupted toolroom mill. The machine is capable, but the workflow has not matured enough to unlock it.
When a Standard CNC Mill Is the Smarter Purchase
There is a bad habit in machine buying that equates more automation with more intelligence. In reality, a standard CNC mill can be the smarter answer when you value quick intervention, lower capital exposure, easier access, and broad daily flexibility over deeper production packaging. Maintenance teams, prototype rooms, schools, and mixed low-volume job shops often benefit from that simplicity.
A simpler machine is not merely a compromise when your work does not reward a VMC’s extra process infrastructure. It can actively outperform a more complex purchase by being easier to justify, easier to keep utilized, and easier to adapt under changing work.
Do not ask only what the VMC adds. Ask whether your plant will use what it adds often enough to justify the added capital and process discipline.
When a VMC Earns Its Price
The best reason to buy a VMC is not that it sounds more industrial. It is that repeated work starts to feel easier on it. Tool changes interrupt less. Chip and coolant control are better contained. Setup logic is easier to document and repeat. Longer cycles feel less dependent on one person’s discipline. Multiple operators can inherit the same process more reliably.
That is the real return. Shops sometimes try to justify VMC value only through spindle performance or cycle time, but the broader gain is process calmness. If your plant is already feeling strain from repeated setups, manual tool management, or operator-dependent variation on a simpler mill, that calmness can pay for the machine faster than raw spec-sheet comparisons suggest.
Labor Structure and Scheduling Pressure Expose the Better Fit
A lower capital price can still be expensive if it creates repeated labor drag. A higher capital price can still be economical if it reduces intervention enough to keep production smoother. Staffing and scheduling are as important as spindle data.
Ask these questions before you compare specification charts:
- Who will run the machine, and how many operators are available per shift?
- How many shifts are planned per week?
- How often do jobs repeat, and in what batch sizes?
- How many tools do common jobs use?
- How much time is currently lost to manual interruption, tool changes, and chip cleanup?
Those answers often make the decision clearer than a specification chart. One strong toolroom operator may extract excellent value from a standard CNC mill. A department with several operators, repeated parts, and rising schedule pressure may find that a VMC reduces friction across the whole team. Neither answer is universal. Both are workflow answers, not terminology answers.
Ownership Package Matters More as the Machine Becomes More Integrated
The more integrated the machine, the more important commissioning, training, maintenance access, spare parts, and service clarity become. Compare the full ownership package, not just the machine body. That means service response, manuals, controller familiarity, tooling ecosystem, spare-parts path, and how the machine will scale if your workload grows.
This is where the discipline of comparing CNC machinery quotes line by line becomes useful. A VMC and a standard CNC mill should not be evaluated on base price alone because they do not carry the same ownership assumptions. A cheaper machine with weak support can become expensive very quickly if your plant depends on it heavily.
Expansion path matters too. If you expect to move from short-run work into more stable repeat production, buying too far down the capability ladder may force an earlier second purchase. If you will remain highly mixed and low-volume, buying too far up can trap money in features that do not earn their keep.
Signs Your Workflow Is Outgrowing a Standard CNC Mill
Shops often know the answer before they say it directly. If the machine waits too often for manual tool changes or repeated setup, the workflow may already need a VMC. The same applies when chip and coolant control are becoming a burden or when several operators need repeatable multi-tool cycles.
Another strong signal appears when the question shifts from “Can this machine make the part?” to “Can this machine make the part day after day without so much intervention?” That is usually the moment when the process has moved from toolroom logic toward production logic.
For buyers wanting a wider reference on that progression, it can also help to compare how small mills and industrial milling platforms diverge as capacity pressure rises. The point is not that every shop must scale up. The point is that scaling pressure changes what “enough machine” really means.
Match the Platform to the Process You Actually Want to Run
The difference between a vertical machining center and a standard CNC mill is fundamentally a difference in process maturity and production intent. Both can machine accurate parts. The VMC is usually built as a more complete production package, with tool handling, enclosure, coolant, and setup systems designed to make repeated work more stable. A standard CNC mill usually fits better where flexibility, lower capital exposure, and close operator involvement still create the most value.
The best buying decision is not based on the stronger-sounding label. It is based on whether your shop needs a capable milling platform or a more complete production system. When repeatability, tooling structure, longer cycles, and multi-operator consistency matter most, the VMC usually earns its place. When your work remains mixed, short-run, toolroom-oriented, or highly adaptive, the standard CNC mill may still be the more intelligent purchase.