Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
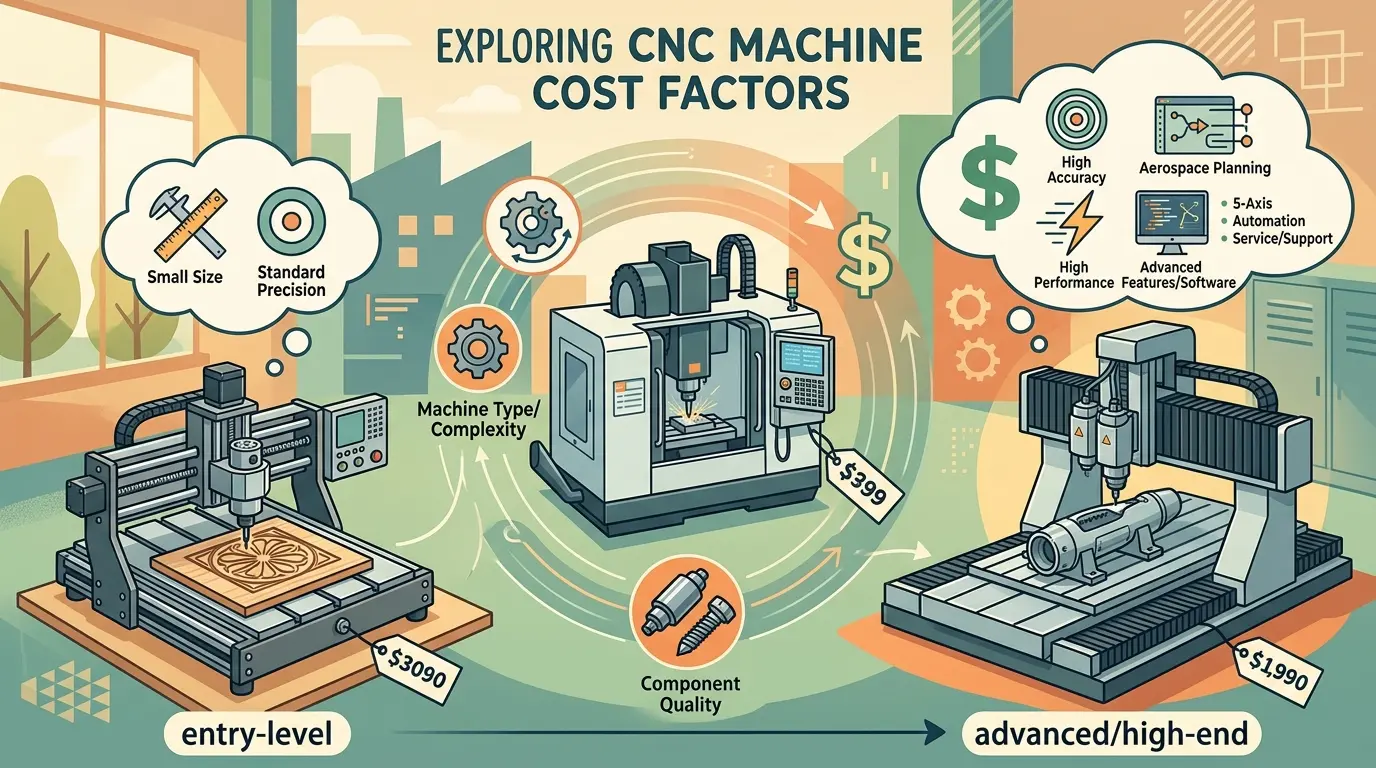
Before any cross-category CNC budget is approved, the quoted number must be read as a transfer of production risk, not a price tag on a frame. This guide breaks down why a router, machining center, turning system, stone processor, and laser cutter each raise their price floor for different reasons—structural duty, environmental burden, labor removal, or software continuity. For factory managers and procurement teams, the real decision is matching the machine’s cost logic to the workflow burden it must absorb, because a low invoice often simply shifts readiness, installation, and recovery risk back onto your floor.
Why a Single CNC Price Benchmark Misleads Buyers
Most CNC price guides fail because they try to answer one question—“what does a CNC machine cost?”—as if a router, a machining center, a lathe, a stone-processing system, and a laser cutter were all variations of the same product. They are not. A quoted price is never just a number attached to a machine. It is the price of a machine family, a duty expectation, a workflow role, an installation burden, a support model, and a level of operating risk transferred either to the supplier or back to the buyer.
Broad averages flatten those differences into a single misleading benchmark. A better approach is to ask what kind of production burden each machine type is being asked to carry. That question determines whether a price is reasonable, expensive, or suspiciously low.
Start With Plant Role, Not Category Label
Before interpreting any price, name the machine’s job inside the factory. Is it for light internal work, daily throughput, visible finish quality, replacing outsourced work, relieving a bottleneck, or reducing labor across several steps? The same budget can buy very different outcomes depending on that role.
Cross-category price discussions often go wrong when management asks for a broad comparison too late, after assuming the categories are interchangeable. A general router, a machining center, a turning system, a stone machine, and an integrated nesting line do not justify capital in the same way. They protect different parts of the workflow. A useful price guide should orient the buyer before shortlisting, not pretend to make the final purchase decision.
Price Rises Where the Machine Carries the Most Risk
The simplest way to read cost across machine types is to ask where each category raises its price floor first. Some machine families raise the floor through structure and sustained-load confidence. Others raise it through motion quality, finish behavior, environmental support, or the labor removed across several linked stages.
The machine category matters, but the real price logic sits underneath it. A more expensive machine is often not charging more for the acronym. It is charging more because it is carrying more responsibility for stability, repeatability, or workflow control. Two CNC systems that look superficially similar by size or travel can have very different cost logic.
Routers Carry Price Through Envelope, Rigidity, and Material Handling Fit
In router-style systems, cost climbs first through table size, gantry behavior, spindle package, hold-down method, and how well the machine matches the actual material route. A shop cutting occasional sheets does not need the same ownership model as one protecting daily output across panel goods, decorative parts, and secondary operations.
A low-price router can look acceptable on a basic list of travels and spindle power while simplifying the things that protect daily use: rigidity, vacuum performance, serviceability, and support around workholding and flow. The visible machine may be present, but the production burden may still sit with the buyer. Router price should be read through application pressure, not table dimensions alone.
Machining Centers Raise Cost Through Structural Confidence and Duty Expectation
Machining centers raise the floor through structural mass, axis behavior, control sophistication, tool-change depth, and confidence under sustained or demanding work. Buyers in this space are paying for the machine to remain stable while load, precision, and uptime expectations increase.
Broad comparisons with lighter-duty CNC categories become misleading quickly. The machine is not only doing motion. It is being trusted to maintain predictable behavior under a punishing workload. If a quote looks unexpectedly low, ask what has been reduced in structure, recovery logic, or operating confidence. The price difference is not decorative. It reflects the risk the machine is expected to absorb.
Turning Systems Price the Value of Keeping Work in One Stable Setup
Lathes and turning-focused equipment build cost through spindle arrangement, bed size, workholding logic, and the amount of turning work that can stay inside one stable setup. The more the machine is expected to simplify concentric work, reduce repositioning, and protect dimensional consistency across repeated cycles, the more its ownership model changes.
Turning is often compared too casually against general CNC expectations. A turning system is not merely another tool with a different axis layout. Its value is tied to process fit. Buyers are paying to reduce specific setup burdens and stabilize a certain family of parts. Cost in turning categories should always be read through workload fit, not headline machine similarity.
Stone Machines Carry Environmental and Structural Burden Together
Stone-processing equipment raises price through a combination of structure and environmental management. The machine is not only asked to move accurately. It is asked to survive a harsher processing environment while fitting into water, slurry, cleanup, and finishing realities that change the whole installed project.
This is one reason stone-capable systems can feel expensive even before site work is fully priced. The invoice is only part of the project. Water handling, slurry behavior, cleanup load, and the machine’s relationship to downstream finishing all shape whether the price is reasonable. Stone-machine cost should be judged as part of a process environment, not as a stand-alone equipment purchase.
Laser Systems Price Environmental Control and Motion Quality
Non-metallic laser systems are another category where buyers underestimate what drives price. Working area matters, but so do motion quality, cut-versus-engrave fit, exhaust behavior, enclosure logic, and environmental integration. A low invoice can still leave the buyer carrying a large share of the operational burden if smoke handling, maintenance realism, or production suitability are not well packaged.
A general CNC price guide cannot treat laser systems as if they were simply lighter cutting machines. The ownership burden is different. Environmental control and process fit often matter as much as the visible motion platform.
Integrated Line Equipment Prices Labor Removal Across Multiple Steps
When the machine becomes more of a line solution than a stand-alone processing asset, price behaves differently. Integrated nesting, transfer, drilling, loading, unloading, and linked flow systems look expensive because buyers are no longer paying only for motion. They are paying to remove labor touches and handoff failures across several stages at once.
These systems should not be compared too narrowly against stand-alone machine prices. A more integrated solution may carry a much larger invoice but a lower effective labor burden across the route. In workflow-heavy panel-processing environments, it makes more sense to think in terms of connected production-line planning than to keep asking why one machine category has a higher quote than another. The quote is often larger because the workflow responsibility is larger.
Structure, Envelope, and Duty Cycle Are Universal Price Raisers
Across categories, some cost drivers appear repeatedly. Larger work envelopes, heavier frames, better damping, and higher duty-cycle expectations all raise price because they reduce risk under real use. A machine built for occasional internal work and one expected to stabilize a daily bottleneck do not share the same price floor, even if they seem close in travel or nominal power.
Suspiciously low prices often hide in exactly these areas. The specification sheet may still look acceptable, but what has been simplified is usually not the visible travel. It is the confidence under sustained work. Buyers should ask not only what the machine can reach, but what kind of working life the price is assuming.
Software and Recovery Logic Belong Inside the Cost
Control systems, postprocessor stability, settings recovery, parameter backup, and digital handoff rarely dominate the quote line by line. But they often dominate how quickly the machine reaches stable output. A cheap machine with brittle digital continuity becomes expensive quickly if the factory loses time to programming confusion, hard-to-recover settings, or overdependence on one expert.
Software continuity is one of the easiest places to ignore until the machine is already on the floor. Stronger control and recovery environments do not always look dramatic in the quote, but they reduce absorption pain and make ownership calmer. Software should be treated as part of the purchase economics, not as a separate technical footnote.
Installed Cost Can Reorder the Ranking More Than the Machine Invoice
A shipped price is not the same as a project price. Electrical preparation, air, exhaust, vacuum, rigging, water handling, drainage, floor loading, clearance, startup time, and commissioning can all change whether one machine really remains cheaper than another. Different machine families make very different demands on the site.
This is where many cross-category comparisons become unreliable. A machine with the cleaner invoice can still create the more expensive project if it asks the building to change more around it. Environmental control is especially important. Dust, slurry, coolant, smoke, washdown, and noise are not side issues. In many categories, they are part of what the machine actually costs to own. Installed burden should be brought into the conversation earlier, not patched in later after internal expectations have already formed around the shipped quote.
Readiness Cost Distorts Many “Cheap” Approvals
Another recurring problem across machine types is first-year readiness cost. Tooling, workholding, jaws, fixtures, probes, spoilboards, gauges, and consumables often arrive after the machine is approved, when management is no longer comparing alternatives as rigorously. The exact mix changes by category, but the pattern stays the same: the machine price is not the same as the price of becoming ready to run the first serious job cleanly.
Broad price screening needs to leave room for readiness spend. A low machine quote does not guarantee a low time-to-production cost. In some categories, the supposedly cheaper choice pushes more readiness burden into fragmented spending that only becomes visible later.
Support Changes the Meaning of the Quote
Support depth rarely looks as large on paper as it feels during downtime. Two machines may appear numerically close, but if one offers a much clearer path to startup, diagnosis, spare-parts response, and ordinary recovery, the price difference may be economically modest in practice. A lower-cost machine can still become the most expensive asset in the room if recovery is slow and unstable.
Support belongs inside even a broad price guide. Buyers are not simply paying for metal and motion. They are also paying for how exposed they will be when normal problems arrive. For a more grounded explanation of why better-supported industrial equipment can cost more, it helps to read what industrial CNC investment is actually buying.
New Versus Used Does Not Change the Category Cost. It Changes the Risk Carrier
Used equipment often compresses the visible invoice but moves more condition risk, support burden, and recovery effort back toward the buyer. New equipment usually asks for more capital because the supplier is carrying more of the startup definition and commercial responsibility. The better question is not whether used or new is cheaper. It is which party is carrying the uncertainty.
Many broad category comparisons get distorted by mixing new and used expectations without saying so clearly. Teams think they are comparing technology classes when they are actually comparing risk positions. Used price should never be treated as the true price floor for a category without also pricing the responsibility it transfers.
Broad Price Guides Should Lead to Better Narrowing, Not Fake Precision
The purpose of a cross-category CNC price guide is not to give management a magical benchmark. Its purpose is to stop false equivalence early. It should help the team understand why different machine types cost what they cost, what burden each type is really carrying, and which cost drivers deserve closer attention before the shortlist becomes real.
Once the shortlist exists, broad guidance has done its job. At that point the buyer needs scope normalization, not category averages. That is where proper quote comparison becomes more useful than any high-level article. And if the business still needs to orient itself across machine families before narrowing, the Pandaxis machinery lineup is a more honest starting point than headline price alone.
The practical conclusion is straightforward: CNC price across different machine types makes sense only when the buyer understands what kind of workflow burden the machine is expected to remove. Structure, environmental integration, labor reduction, software continuity, readiness cost, and recovery logic all shape the real economics. The visible quote is only the surface.
Different CNC machine types cost different amounts because they absorb different kinds of production risk. A useful price guide does not flatten those differences. It makes them easier to see.