Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
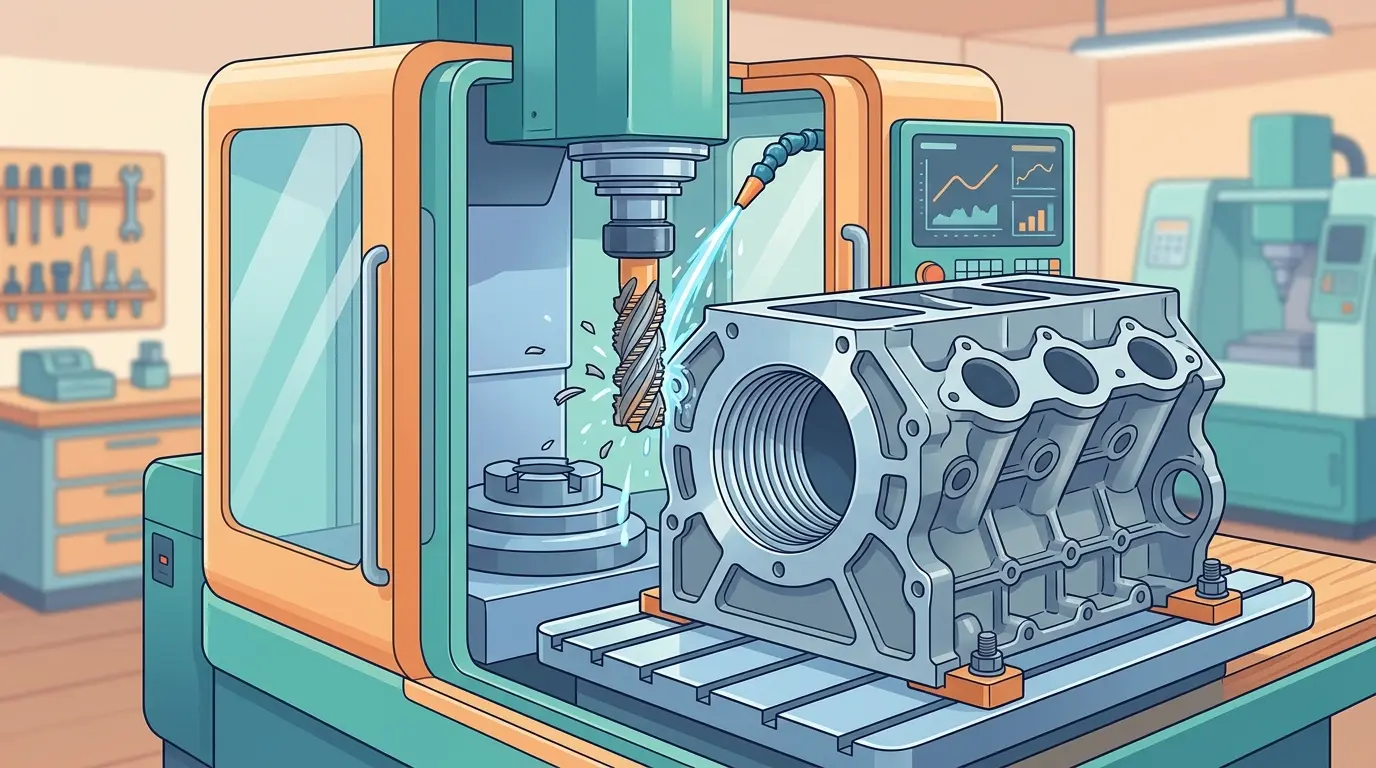
Thread milling gets pulled into conversations for the wrong reasons. A shop hears the term, assumes it is a more advanced version of tapping, and starts applying it to jobs where a standard tap would have been faster and cheaper. That is a costly misunderstanding. The real question is not which method sounds more sophisticated. It is which method fits the risk profile of the thread you are cutting.
A thread mill is a rotating cutter that generates threads by following a programmed helical interpolation path rather than driving a tap straight through the hole. That mechanical difference changes how the thread is formed, how much control the operator has, and what happens when something goes wrong. For routine threads in friendly material, a tap is often the better business answer. For larger threads, difficult materials, expensive parts, or awkward geometries, thread milling can be the difference between a recoverable process issue and a scrapped component.
The Decision Starts With Failure Cost, Not Tooling Status
Before comparing feed rates or cycle times, ask what happens if the thread goes wrong. On a simple low-risk part, a tap is fast, familiar, and effective. The consequences of a broken tap are manageable, and the economics favor speed. On a higher-value part, a deep blind hole, or a difficult material, the cost of a broken tap buried in the feature changes the calculation completely.
Thread milling removes material progressively along a helical path instead of forcing the full thread form in one direct axial pass. That gives the process more room to stay deliberate. When the thread sits inside a part you do not want to lose, that extra control matters more than raw speed.
How a Thread Mill Cuts Differently From a Tap
The technical distinction is straightforward. A tap advances directly along the hole axis, committing the tool and the feature to each other quickly. If the material, alignment, chip behavior, or tool condition is wrong, the process becomes unforgiving fast. There is no graceful way to back out of a tap that is binding halfway through a blind hole.
A thread mill approaches the same result differently. The cutter follows a programmed helical interpolation path and generates the thread gradually. That changes the process in several practical ways:
- The shop has more control over how the thread is cut, including the ability to adjust entry and exit strategies.
- A broken tool event is often less catastrophic than a broken tap buried in the feature.
- The method suits larger threads and awkward setups where tapping becomes physically uncomfortable.
- Depending on tool design, one cutter can sometimes cover related thread sizes within a pitch family.
This does not mean the tool is always better. It means it solves a different process problem.
Where Thread Milling Usually Earns Its Place First
Thread milling becomes attractive when one or more of these conditions appear:
- The thread diameter is large enough that tapping becomes awkward, slow, or tool-intensive.
- The material is difficult enough that tap breakage risk becomes a real planning issue.
- The part is valuable enough that damaged threads are expensive to scrap or repair.
- The feature geometry makes direct tapping uncomfortable, such as blind holes with limited clearance.
- The shop wants flexibility across a family of thread requirements without committing to a separate tap for every size.
In short, thread milling becomes rational when the thread is no longer a routine low-consequence event. The more expensive the mistake, the stronger the case for a method that offers more control.
A Practical Comparison: When Each Method Usually Wins
| Situation | Tapping Usually Wins | Thread Milling Usually Wins |
|---|---|---|
| Simple, repeatable threads in friendly material | Yes | Sometimes unnecessary |
| Higher-value parts where broken-tool recovery is painful | Less attractive | Often stronger case |
| Large threads or awkward feature situations | Sometimes awkward | Often more flexible |
| Shops prioritizing shortest possible cycle time | Stronger fit | Often slower |
| Jobs where one tool may need to cover related thread sizes | Limited advantage | Often stronger fit |
This table is a starting point, not a rulebook. The choice is about which method fits the risk profile of the thread, not which one sounds more advanced.
Broken Tap Consequences Change the Conversation
One of the strongest reasons shops move to thread milling is damage control. A broken tap inside a part creates a recovery problem that is often far more expensive than the threading cycle itself. If the part is costly, the material is awkward, or the feature is hard to salvage, the threading method should be judged by consequence rather than nominal speed.
Thread milling does not make failure impossible. It changes the kind of failure the shop has to manage. A broken thread mill is usually easier to extract than a broken tap, and the part has a better chance of being saved. That is why buyers should care about it most when the thread sits inside a part they do not want to lose. The tool is often a risk-management choice before it is a productivity choice.
Larger Threads and Difficult Materials Favor Control
Large threads place different demands on tooling and setup. The torque required for tapping grows with thread size, and the consequences of a tap seizing become more severe. Difficult materials raise breakage risk and make the shop less comfortable with a forceful one-step thread generation method.
In those cases, the programmed helical approach becomes attractive because it gives the process more room to stay deliberate. The shop may accept longer programming effort or a somewhat longer cycle because the threading event no longer feels like a low-risk commodity step. This is an important distinction for buyers reviewing supplier choices. If a shop selects thread milling in these conditions, the decision is likely sober and practical rather than excessive.
Thread Milling Is Not Free Control
The method earns its control by asking more from the process. Programming is usually more involved. CAM support matters more. Toolpath strategy matters more. The shop has to understand why it is choosing the method and how it will manage chip evacuation, entry, exit, and thread quality validation.
That means thread milling should not be approved casually. It is not the best answer for every threaded hole simply because the shop owns the tool. It is the best answer when the added process attention creates meaningful value.
The Tradeoff Is Simplicity Versus Flexibility
For many buyers, the simplest way to compare the methods is this:
- Tapping usually wins on straightforward simplicity.
- Thread milling usually wins on controlled flexibility.
If the shop already taps the feature reliably and cheaply, thread milling may add more effort than the job deserves. If the job keeps pushing the process toward breakage risk, difficult recovery, or higher-value thread control, thread milling may suddenly look much more rational. The best method is the one that matches the economic shape of the problem.
Chip Evacuation Still Has to Be Taken Seriously
Some buyers hear “more control” and assume the process becomes forgiving. It does not. Thread quality still depends on sound cutting discipline. Chips still need to move out of the feature cleanly. Toolpath choice still matters. A bad evacuation condition can still damage the result or compromise thread quality even when the shop is using a thread mill instead of a tap.
Mature shops do not talk about thread milling as magic. They talk about it as a better-suited method for certain conditions, provided the rest of the process is also planned properly.
One Tool Can Sometimes Cover More Than One Thread Situation
Another reason thread milling earns attention is flexibility. Depending on tool style and application, one cutter may cover related thread sizes or allow the shop to solve more than one threading requirement without treating every feature as a separate tap commitment. That can be useful in mixed work, prototype work, or supplier environments where thread variety is real and setup flexibility matters.
This does not erase the need for method discipline. It explains why some shops prefer thread milling even when the cycle is not the shortest. They are buying flexibility and recoverability, not just a thread form.
Blind Holes and Awkward Features Reveal the Difference Faster
The more awkward the feature becomes, the more clearly the difference between methods shows up. Blind holes, limited clearance, difficult exit conditions, and features where chip behavior is uncomfortable under a direct tapping approach can all push the shop toward a more controlled interpolation method.
This does not mean every blind-hole thread should automatically be milled. It means the feature geometry should be judged honestly. If a direct tapping event feels simple and safe, there may be no reason to complicate it. If the geometry reduces the shop’s comfort margin and makes failure or recovery uglier, the value of thread milling becomes easier to defend.
Prototype, Mixed Work, and Expensive Parts Change the Economics
Thread milling also becomes easier to justify in prototype environments, mixed part portfolios, and higher-value machining where flexibility matters more than raw speed. In those settings, the shop may care less about saving a few seconds per thread and more about keeping options open, reducing breakage risk, and avoiding part loss when the feature is not fully routine.
A job shop handling varied work may make a very rational decision to prefer a more controllable method on certain parts because the cost of being wrong is higher than the cost of being slightly slower. A dedicated high-volume line on a stable thread family may judge the exact same method differently. The same tool can look cautious and smart in one environment and unnecessary in another. The difference is not ideology. It is the economic shape of the work.
When Tapping Is Still the Smarter Business Choice
Thread milling does not replace tapping as the default winner in all situations. If the material is friendly, the thread is routine, the part is not unusually vulnerable, and the shop already taps the feature reliably, a tap may still be the more practical answer. That is not old-fashioned. It is efficient.
Buyers should be cautious when a process discussion implies that thread milling is automatically the more sophisticated choice and therefore automatically the better one. In many ordinary jobs, that logic simply does not hold. Better process decisions come from fit, not image.
What Buyers Should Ask Suppliers or Internal Teams
When thread milling shows up in a quote, routing sheet, or supplier explanation, these are the useful questions:
- Why was thread milling chosen instead of tapping?
- Is the material or part value part of that decision?
- What risk is the method controlling better than a tap would?
- Is the thread size or geometry part of the justification?
- How is chip evacuation and thread verification managed?
- Is the cycle-time penalty real, and if so, why is it worth it?
Questions like these keep the method tied to a visible process reason. That is where the real justification lives.
Where It Fits in a Broader Machining Workflow
Thread milling is not a product-category story for most equipment suppliers. It is machining-process literacy for buyers who need to understand why a supplier may choose one threading method over another. It matters most when the buyer is coordinating outsourced precision work, comparing quotes, or trying to judge whether a process step sounds mature or merely complicated.
For broader process context, it helps to review how CNC milling tools and applications fit real production decisions rather than isolated tool labels. When the bigger concern is whether the supplier really operates at a tighter machining standard than a more general shop, it also helps to compare where precision capability starts to matter in ways that show up in risk, recovery, and consistency. The useful habit is to read the method as part of process control, not as jargon for its own sake.
Good Shops Use Thread Milling Selectively, Not Emotionally
One useful sign of process maturity is that strong shops do not use thread milling everywhere just because they can. They use it where the case is specific and defendable: larger threads, awkward features, costly parts, difficult materials, broken-tool risk, or flexibility needs that make the method worthwhile.
That selectivity matters. It shows the shop is solving a threading problem instead of performing sophistication. Buyers who notice that distinction usually interpret process decisions more accurately.
The Best Approval Rule Is Simple
Approve thread milling when the shop can point to the exact value of extra control over the thread. That value may be lower breakage risk, easier recovery, better handling of a larger or more difficult thread, or more flexibility than a tap provides comfortably. If that value is vague, the process choice should be challenged.
That is the cleanest buyer rule because it keeps the method tied to consequence. Once the method has to defend itself in those terms, the right answer usually becomes clearer.
Use It When Control Pays for Itself
A thread milling bit is a cutter used to generate threads by interpolation rather than by direct tapping. Its strength is controlled thread generation where the job benefits from more flexibility, lower breakage consequence, or better risk management than a tap can offer comfortably.
Its weakness is that it usually asks for more programming and more deliberate process ownership. That makes it a strategic choice, not an automatic upgrade. When the thread failure cost is high enough, the method can be very smart. When the thread is routine and tapping already works, the simpler answer may still be the better business answer. That is the practical way to judge it honestly.