Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
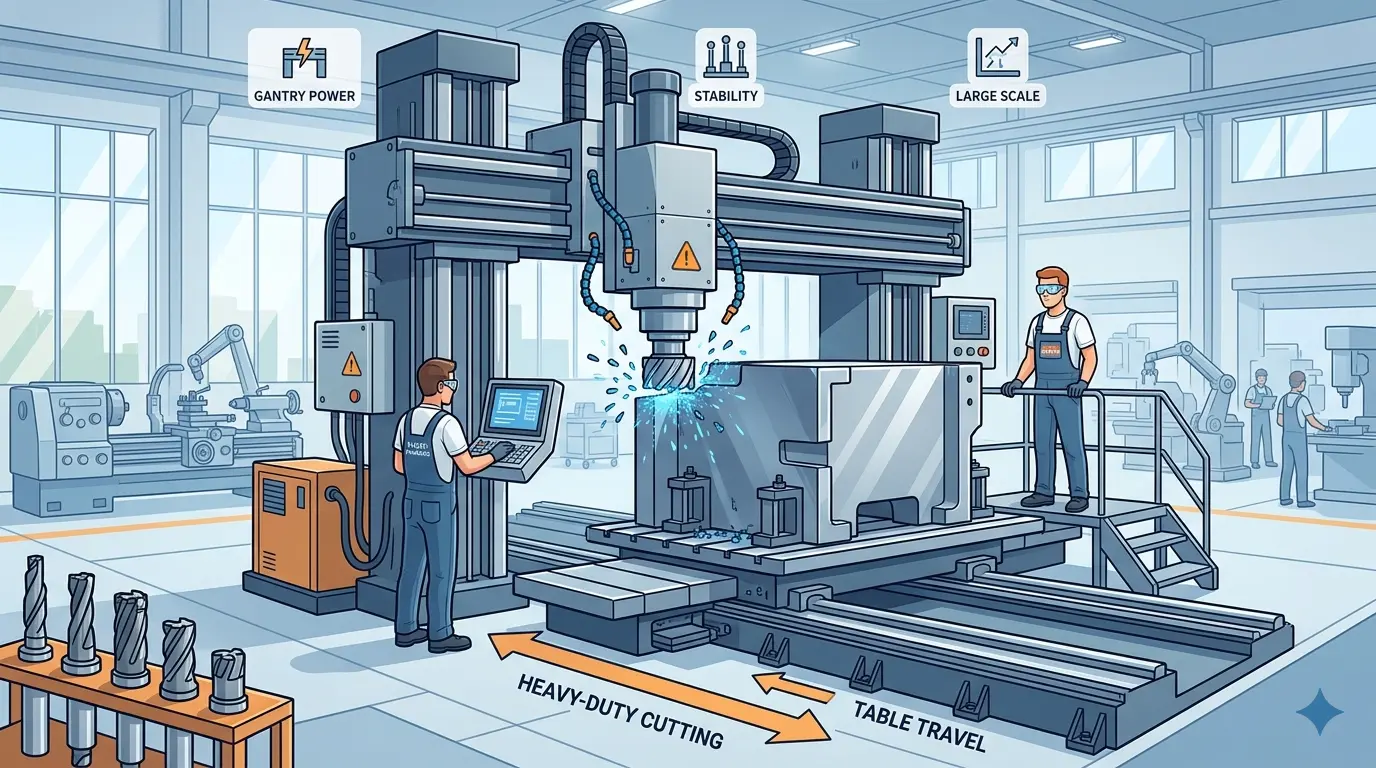
When a part family outgrows a standard vertical machining center, the first symptom is rarely a hard travel limit—it is a creeping loss of confidence across wide spans: finish drift, setup improvisation, and structural flex that smaller jobs never exposed. That is the point where double column milling stops being a catalog category and becomes a structural decision. This article explains why the layout exists to solve a rigidity problem, not a travel problem, and why comparing axis numbers alone will mislead your purchase. The real question is whether your recurring workload genuinely needs support across the full envelope, or whether you are buying scale without solving the actual bottleneck.
When a Standard Mill Stops Being Enough
Most shops arrive at the double column milling question the same way: not through a catalog, but through a problem. A part family starts growing. Plates get wider, mold bases get heavier, or structural components start demanding more envelope than the shop’s current vertical machining centers can handle with confidence. At first, the issue looks like travel. The part technically fits, but the process feels strained. Surface finish drifts across wide spans. Setup becomes an exercise in improvisation. The machine’s structure starts talking back, and not in a good way.
That is the moment to understand what double column milling actually is. It is not simply a larger mill with more axis travel. It is a different structural answer to a different class of workload, and confusing the two leads to expensive mistakes.
The Structural Logic Behind the Layout
At its core, double column milling refers to a machine architecture where the cutting head operates on or between two vertical columns connected by a bridge or crossbeam. The value of that layout is not aesthetic. It is support. When parts get larger and setups get heavier, keeping the cutting system stable across a broad work area becomes a far more serious concern than it is on compact machines.
Think about what happens on a conventional C-frame vertical mill as the table extends. The column carries the spindle, and the farther the head reaches from the column face, the more leverage the cutting forces have against the machine structure. On wide parts, that leverage translates into deflection, chatter, and inconsistency. A double column machine changes the load path. The head is supported from both sides, which distributes cutting forces more evenly and keeps the spindle stable across the full width of the work envelope.
That is why buyers should read the term as a structural concept first and a marketing category second. The layout exists to solve a rigidity problem that larger travel numbers alone cannot address.
Why Travel Figures Mislead Buyers
One of the most common mistakes in large-format machine selection is comparing only axis travel. Travel matters, but it does not describe how a machine behaves on larger workpieces. A layout can offer enough nominal reach while still leaving the cutter, setup, or table support less calm than the job actually requires.
Large parts magnify weaknesses that smaller jobs hide. A 400 mm plate might run fine on a standard VMC even with some structural flex, because the cutting forces are small relative to the machine’s mass. Scale that part up to 2,000 mm and the same flex becomes visible in the finish, the tolerances, and the tool life. The double column architecture addresses that specific failure mode by providing support across the entire machining envelope, not just access to a bigger area.
This distinction matters because it changes the buying question. The right question is not “which machine has more travel?” It is “which machine layout supports this part family more honestly?”
Where Double Column Layouts Earn Their Keep
Double column machines are typically evaluated when the part family includes large plates, mold structures, heavy bases, big prismatic components, or other work where machine support over a broader footprint directly affects stability and confidence. The layout also makes sense when fixtures themselves become substantial, even if the part geometry is not especially complex. A heavy tombstone or a large sub-plate can weigh more than many small workpieces, and that mass has to be carried and positioned without compromising the cut.
In those situations, the machine’s structural behavior can matter as much as spindle speed or catalog travel figures. A double column machine with a modest spindle can outperform a lighter machine with a higher RPM rating when the job is a wide, heavy plate that needs consistent depth of cut across its full surface.
A Bottleneck Table to Keep the Decision Honest
Before committing to a double column platform, it helps to map the current production pain against what the layout can actually solve. Not every large-part problem is a structural problem.
| Current Problem | Does Double Column Layout Directly Help? | What Still Needs Separate Work |
|---|---|---|
| Large part support across a wide area | Often yes | Fixturing and inspection logic still matter |
| Heavy setup weight and large fixtures | Often yes | Material handling and loading strategy |
| Poor finish on broad surfaces due to instability | Sometimes, if structure is the real cause | Tooling, cutter strategy, and spindle condition |
| Small-part throughput pressure | Usually not the main answer | Workflow balance and machine mix |
| Weak programming discipline | No | CAM, prove-out, and operator process control |
This table keeps the discussion focused on what the layout can truly solve and what it cannot. If the dominant problem is small-part throughput, a double column machine is the wrong tool. If the problem is structural instability on wide work, the layout deserves serious consideration.
Structural Mass Only Pays Back If the Workload Uses It
Double column milling can absolutely improve confidence on large jobs, but the gains are not free. The machine is typically larger, heavier, and more demanding in terms of installation, floor space, transport planning, and supporting infrastructure. If the shop only occasionally handles work that needs that structure, the machine can become an expensive answer to an irregular problem.
Part-family stability is the deciding factor. The machine should solve a recurring production need, not a memorable one-off job. A shop that runs large mold bases every week has a different purchase case than a shop that sees one big plate every few months. The first shop can justify the capital and the floor space. The second shop may be better served by outsourcing the occasional large job or by improving the process on existing equipment.
The Layout Changes Handling and Planning Around the Machine
As parts get larger, machining stops being only a spindle-and-toolpath discussion. Loading, part orientation, crane or forklift access, fixture installation, probing, inspection reach, and operator movement around the machine all become more important. A double column platform can improve the cutting side of large work, but it also pushes the shop to become more disciplined in logistics.
Buyers who ignore this often discover that the machine is ready for big parts before the rest of the factory is. The crane may not reach the table center. The inspection CMM may not have the travel to verify the finished part. The chip conveyor may not handle the volume of material being removed from larger workpieces. These are not minor details. They are the difference between a machine that produces and a machine that sits idle waiting for the rest of the process to catch up.
Programming and Tooling Still Decide a Lot of the Outcome
Large structure does not remove the need for good process planning. Cutter selection, overhang control, workholding strategy, sequence planning, and program stability still matter heavily. A shop can buy a structurally capable machine and still waste its potential if the tooling plan remains casual or the setup logic is not suited to large work.
Long-reach tools are a common failure point. On a large plate, the cutter may need to reach deep into a pocket or across a wide surface, and the tool overhang introduces its own deflection that no machine structure can fully compensate for. Shops that succeed with double column machines tend to be disciplined about tool selection, using the shortest possible tool for each operation and planning roughing and finishing passes with the machine’s rigidity in mind.
This is a recurring theme in industrial equipment decisions. A better machine can widen the safe process window, but it cannot replace process discipline.
Buyers Often Confuse Double Column with “Always Better”
That misunderstanding is expensive. A double column layout is not automatically a quality upgrade for every type of work. Small-part production, mixed short-run work, or jobs that do not really need the envelope may gain little while taking on more capital cost and more layout complexity. The structure is valuable when the workload is structurally demanding, not when the shop simply wants a machine that sounds more industrial.
Large-format purchases should be driven by recurring workflow evidence rather than ambition alone. If the part mix is stable and the structural bottleneck is real, the double column machine can be a transformative investment. If the purchase is driven by a desire to look more capable or to handle a single dramatic job, the machine may become a monument to a decision that was never fully justified.
Comparing Against a Standard VMC Requires the Right Question
The wrong comparison is “which machine is more powerful?” The right comparison is “which machine layout supports this part family more honestly?” a standard VMC is still the better fit for moderate parts.
Layout decisions should follow part behavior, not vocabulary. A shop that runs mostly 600 mm plates with light cutting loads does not need a double column machine, even if the parts are growing. A shop that runs 2,500 mm mold bases with heavy roughing passes has a structural need that a standard VMC cannot honestly meet.
The Machine Only Pays Back When It Reduces Real Pain
For a large-format platform to justify itself, it should relieve specific recurring pain. That may be poor process confidence on wide work, repeated handling compromises, unstable long-span cutting, or too much setup improvisation around heavy parts. If those pains are real and recurring, the structural layout can create meaningful value. If they are not, the shop may be buying scale without solving the actual bottleneck.
Management discipline matters here. The best purchases are tied to repeated factory reality, not to one dramatic demonstration. A machine that solves a weekly problem becomes a strategic asset. A machine that solves a quarterly problem becomes a cost center with a very large footprint.
Prove the Case with Representative Parts, Not a Generic Demo
The strongest test is to review real work the shop expects to run. How large are the parts? How heavy are the fixtures? Where does instability show up today? Does the setup strain the current machine? Does handling eat labor? What inspection burden follows from the current routing? Those questions reveal whether the purchase case is structural, logistical, or something else entirely.
If the argument for the machine cannot be demonstrated through representative parts, the purchase case is still too weak. A machine vendor can make any machine look good with a polished demo part. The only meaningful test is whether the machine can handle the shop’s actual workpieces, with the shop’s actual tooling, at the shop’s actual tolerances.
Large-Part Inspection and Recovery Planning Change Too
As the machine size grows, the inspection and recovery plan usually changes with it. Large parts are harder to move, harder to re-reference casually, and often more expensive to recover if something drifts late in the process. That means probing strategy, in-process checks, part access, and measurement planning become more important than they might be on smaller work. A shop that upgrades the machine but leaves inspection thinking at small-part levels may still underperform.
Recovery planning matters for the same reason. If a large workpiece must be removed, reloaded, or partially reworked, the cost of uncertainty rises. Double column milling can improve process confidence, but the surrounding process has to respect the size and value of the workpiece too. A probing cycle that takes two minutes on a small part may take twenty on a large one, and that time has to be built into the production plan.
Utilization Risk Is Real on Large-Format Machines
Another issue buyers should watch is utilization. Large-format equipment can be very productive when the workload is stable, but it can also tie up capital and floor space if the part mix shifts or the machine is approved mostly for occasional jobs. The right purchase case usually includes not just one difficult part, but a believable ongoing stream of work that benefits from the structural layout.
That does not mean the machine must run at full load every hour. It does mean the shop should understand whether the platform is supporting a repeat business pattern or a rare exception. That distinction often decides whether a large-format purchase feels strategic a year later or merely impressive.
Infrastructure and Occupancy Costs Should Be Counted Early
Large-format machining decisions are often distorted because buyers focus on technical capability and postpone practical site questions. Foundation requirements, access routes, loading clearances, power, chip handling, maintenance access, and floor-space occupation all influence the real cost of ownership. A shop that treats these as afterthoughts may approve the right machine on paper but the wrong machine for its building and production flow.
A double column machine is not a drop-in replacement for a standard VMC. It may require a reinforced foundation, a taller ceiling clearance, a different chip management system, and a crane with more reach. These costs should be quantified before the purchase decision, not discovered after the machine arrives.
Pandaxis Context Starts with Machine-Family Fit
For buyers comparing larger machining options more broadly, the Pandaxis machinery lineup is the right place to return once the structural concept is understood. The term double column milling is useful because it points to a class of machine behavior, but the commercial decision still depends on workload, size range, handling logic, and what kind of industrial value the machine is meant to protect.
Buy the Layout to Solve a Large-Work Problem
Double column milling is best understood as a structural machine solution for larger-format work that needs better support and stability across a wider envelope. Its strength is not simply size. Its strength is the way that size is supported.
That is the key buying rule. If the shop has a recurring large-work bottleneck tied to structure, support, and process confidence, double column layout may be exactly the right direction. If not, a smaller and simpler machine may still be the more intelligent answer. The machine should solve a production problem, not create a new one.