Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
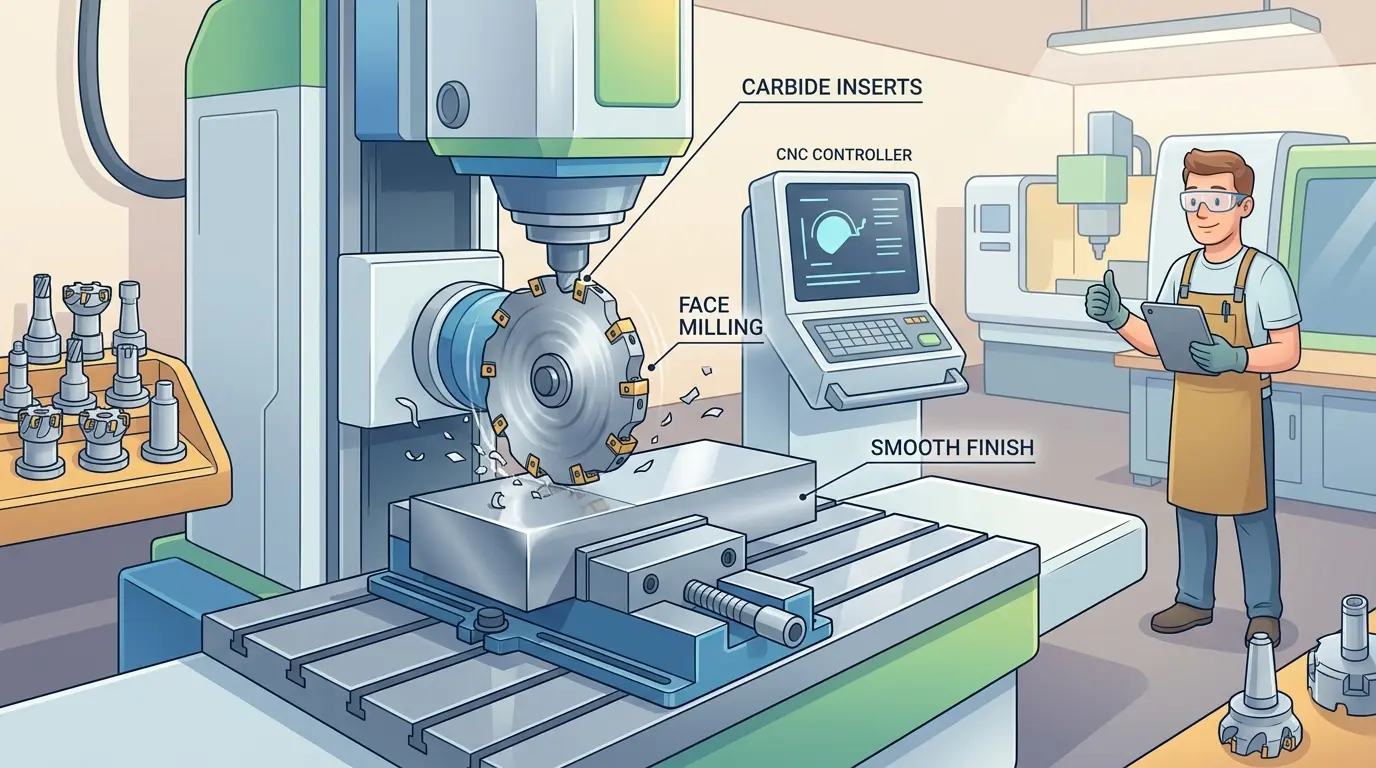
Face milling is often dismissed as a simple surfacing pass, but in production it is the operation that decides whether the rest of the route starts on honest ground. A saw-cut blank, flame-cut plate, or cast surface carries hidden variation that will quietly contaminate every bore, pocket, and mating surface referenced from it. Before you compare cutter diameters or machine classes, you need to know whether the pass is creating a datum, removing heavy stock, or refining a near-final face—because each purpose demands different tooling logic, support discipline, and inspection expectations. Misjudging that distinction turns a short cycle into a long correction story.
Face Milling Is a Foundation Operation, Not a Cosmetic One
Face milling looks straightforward. A cutter sweeps across a broad surface, removes material, and leaves a flatter face behind. But in production, that simple motion carries more responsibility than its cycle time suggests. The first clean face on a raw blank often becomes the reference for everything that follows. A stable face-milled surface reduces setup corrections, improves measurement confidence, and keeps later features from inheriting raw-stock inconsistency.
In many machining routes, face milling decides whether the rest of the process starts on honest ground or on a weak assumption. That distinction matters more than most buyers realize when they compare machines, tooling, or process strategies.
Why the First Flat Face Sets the Tone for the Whole Part
Face milling typically happens early in the workflow because the shop needs a more trustworthy reference than incoming stock provides. A saw-cut blank, flame-cut plate, cast surface, or otherwise irregular starting face may be good enough to hold in a fixture, but not good enough to build the rest of the part from confidently. Face milling creates order where the supplier left variation.
Once that first face is established, later operations can reference something stable. That reduces the chance that raw-stock inconsistency quietly contaminates the rest of the job. Bores, slots, pockets, hole patterns, and mating surfaces referenced from the face-milled plane all inherit the quality of that first surfacing pass.
Face Milling Is Not Automatically a Finishing Pass
One of the most common misunderstandings is assuming face milling means finishing. It does not. A face-milling operation can be roughing, semi-finishing, or finishing depending on stock condition, tool selection, insert choice, machine stability, and downstream needs. Some face-milled surfaces exist mainly to create a better base for the next setup. Others are nearly final and must satisfy stricter surface or flatness requirements.
The question should never stop at the cutter path. The real question is what the face is being asked to do next. That answer determines cutter choice, pass strategy, setup support, and inspection expectations.
Incoming Stock Usually Lies More Than the Print Suggests
Raw material and rough-cut blanks often look acceptable until the shop tries to reference them precisely. Saw-cut stock may carry subtle variation across its length. Flame-cut or rough-prepared material can hold enough unevenness to distort later assumptions. Cast or forged surfaces may look visually convincing while still being poor reference candidates.
Face milling is the moment when the shop stops trusting the stock and starts trusting its own process. It is not only producing flatness. It is replacing supplier or upstream variation with something the machining route can believe.
Match the Pass Strategy to the Operational Purpose
Because face milling serves different purposes, the process logic should follow the intent of the cut. The table below clarifies what changes when the goal shifts.
| Why the Face Is Being Milled | What the Shop Should Prioritize | Common Mistake |
|---|---|---|
| Create a datum for later operations | Stability, repeatability, and support | Treating the pass as cosmetic only |
| Remove heavy stock from a broad face | Calm cutting and predictable load | Choosing a cutter the setup cannot support |
| Improve a near-finished surface | Surface quality and controlled pass behavior | Using roughing logic on a finish-sensitive face |
| Bring inconsistent incoming stock into process range | Honest measurement after the pass | Assuming the raw blank was consistent enough already |
This table forces the team to tie the cut to an operational purpose instead of treating all flat-surface passes as equivalent.
Cutter Choice Changes the Outcome More Than Many Buyers Realize
Face milling may be visually simple, but tooling decisions carry weight. Cutter diameter, insert style, edge condition, number of teeth engaged, and the machine’s ability to stay calm under the chosen cut all affect whether the pass creates a useful surface or starts a vibration story. A broad cutter on a weak setup can quickly turn a simple surfacing job into chatter, uneven finish, or insert waste.
Experienced machinists rarely describe face milling as trivial. The geometry is simple. The system behavior is not always simple.
Broad Surfaces Expose Weak Support Immediately
Face milling is unforgiving when the workpiece is poorly supported. A part that looks firmly clamped may still flex, ring, or shift just enough to leave an inconsistent result across the face. Thin plates, awkwardly supported work, large overhangs, or improvised fixturing all show up quickly in a broad surfacing pass. The cutter is not only removing stock. It is testing the honesty of the setup.
A visible surface defect after face milling should not automatically be blamed on the tool or program. Work support and clamping deserve equal suspicion.
Squareness and Parallelism Problems Often Begin Here
Even when the drawing discussion later shifts to holes, pockets, or external dimensions, the first face-milled plane often influences whether the part can be held squarely and whether opposite surfaces can be brought into honest parallel relationship. Shops that rush the first surfacing step sometimes spend more time later correcting what looks like alignment trouble, when the real weakness began at the first reference face.
The operation deserves attention even in parts where the face itself is not visually important. It may still control how cleanly the rest of the geometry can be built.
The Surface Requirement Should Match the Next Operation
Shops also waste time when they machine a surface better than the process truly needs. If the next step only needs a stable reference plane, the face-milling strategy should be chosen around that requirement. If the surface is part of a visible assembly or a sealing interface, the strategy changes. Over-machining can quietly burn cycle time without improving the functional result.
The question “what does the next operation need?” keeps the surfacing pass tied to production logic instead of habit.
Face Milling Can Solve Problems That Look Like Measurement Problems
Shops sometimes blame inspection difficulty on measuring technique when the real issue is surface preparation. If the face being referenced is not truly stable or consistent, measurement drift is not surprising. Operators may think the problem lies in probing, indicator use, or final verification when it actually began earlier in the route.
This is one reason face milling has such leverage. A better surface can simplify downstream inspection even though inspection is not the operation itself.
Roughing Logic and Finishing Logic Need Different Discipline
When face milling is used mainly to knock down stock, the shop may prioritize calm removal and stable machine loading. When it is used to prepare a near-final surface, the priorities shift toward insert condition, toolpath behavior, pass consistency, and support quality. A shop that uses one logic for both situations often gets mixed results because the process is not aligned to the purpose.
This distinction also helps management read cycle time honestly. A quick rough face pass and a finish-sensitive face pass should not be judged by the same performance standard.
Tool Wear on a Broad Face Distorts Confidence Quickly
Because the operation covers so much visible area, small changes in insert condition or cutter behavior show up faster than managers expect. A face that looked stable earlier in the shift may begin to reveal faint inconsistency, finish change, or load variation before anyone feels alarmed by the tooling. Broad surfacing tends to make these changes easier to see, which is useful if the shop is paying attention and expensive if the shop ignores the warning.
Face milling often serves as an early indicator of wider process calm. The pass is large enough to reveal drift before more localized features make the problem harder to diagnose.
Downstream Payback Is Often Bigger Than the Face Pass Itself
Many of the best reasons to improve face-milling practice appear later. Better datums reduce setup correction. More stable references reduce measurement argument. Flatter surfaces improve assembly behavior. Later features align more predictably. The value of face milling is often distributed across later operations instead of being obvious inside the surfacing cycle alone.
This is why shops sometimes undervalue it. The pass looks short. The payoff is spread across the route.
Sometimes Two Deliberate Face Passes Are Cheaper Than One Compromised One
Shops under schedule pressure often try to make one pass carry too many responsibilities at once: heavy cleanup, final reference creation, and near-finish quality. Sometimes that works. Sometimes it produces a face that is technically machined but strategically weak. In tougher conditions, splitting the goal more honestly can be the better economic choice. One pass establishes order. A later pass refines the face under calmer conditions.
The important point is not that two passes are always better. It is that surfacing strategy should match the real burden being placed on that surface.
Representative Trials Should Measure More Than Finish Alone
If a shop is evaluating a new cutter strategy or a new approach to face milling, the trial should examine more than appearance. It should track whether the surface behaves correctly for the next setup, whether measurements stabilize, whether the work support remains calm, and whether the route after face milling becomes easier or harder. Finish matters, but finish alone does not capture the whole industrial purpose of the pass.
That broader view usually leads to better decisions than judging the operation by visual surface quality only.
Buyers Should Connect the Term Back to Machine Class
When face milling becomes a recurring point of concern, the discussion may actually be about machine capability rather than only programming or tooling. If the workload is full of broad surfaces, larger cutters, and heavy surfacing expectations, it helps to compare which mill layouts and machine classes actually support that work more honestly. The surfacing operation may be exposing a mismatch between the job and the platform carrying it.
That is a more useful reading than simply asking whether the face-milling strategy needs another tweak. For shops evaluating machine options for surfacing-heavy work, reviewing the machine classes available through Pandaxis can help clarify what platform matches the workload.
A Good Trial Should Track What Happens After the Face Is Cut
If management wants to judge whether a new face-milling approach is truly better, the test should extend beyond the surface itself. How easy is the next setup? Do probing and inspection become calmer? Do later features hold more predictably? Does the team spend less time compensating for variation that used to appear early? These are the outcomes that reveal whether the face pass created a genuinely better process foundation.
That kind of validation is more valuable than a simple before-and-after visual comparison. Face milling earns its keep when the whole route becomes easier to trust.
Judge Face Milling by the Stability It Creates
Face milling in CNC is best understood as a flat-surface operation that often creates the reference truth for the rest of the job. Its industrial value is not limited to stock removal. It lies in how well the pass stabilizes everything that comes after.
Do not judge face milling only by how the pass looks in isolation. Judge it by the stability, confidence, and downstream accuracy it creates for the rest of the route.