Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
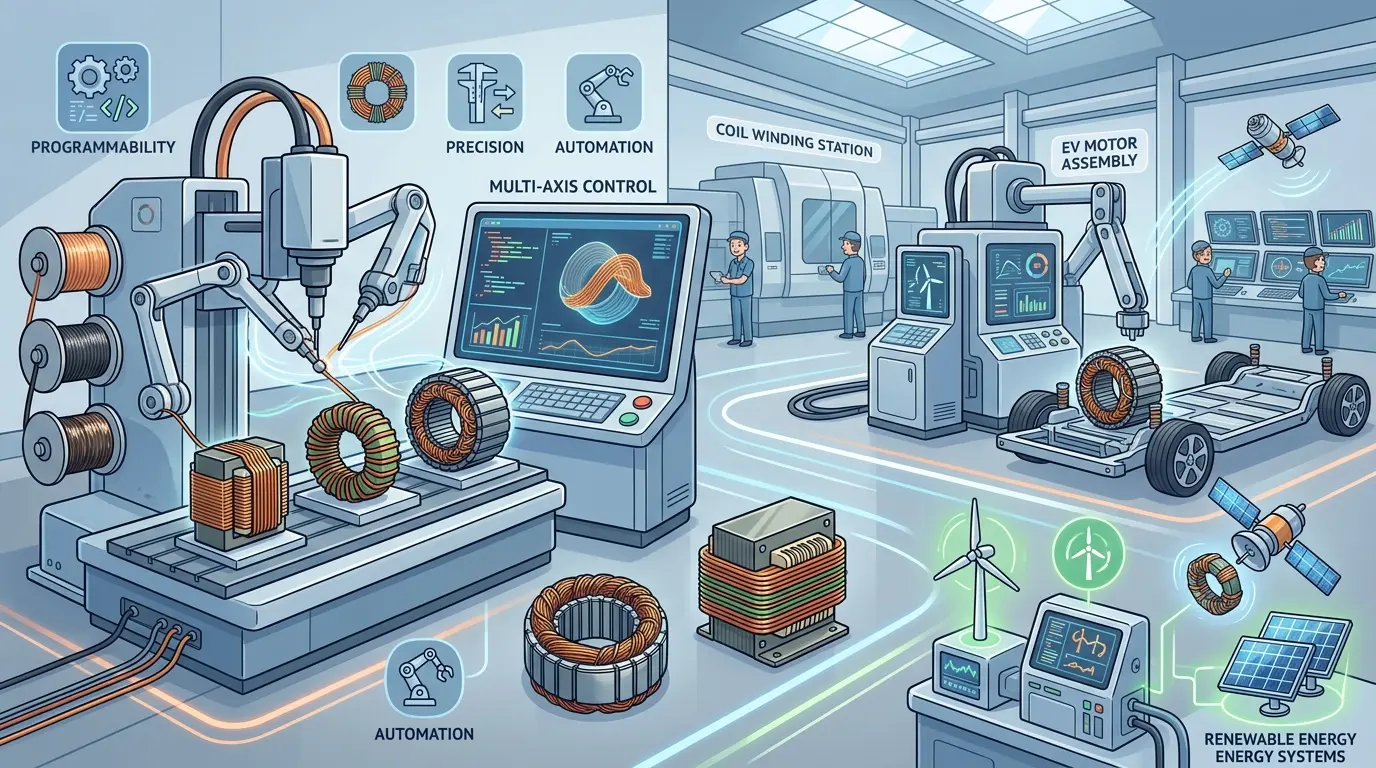
Standard CNC buying logic fails the moment the machine builds a structure instead of cutting one. A winding machine does not remove material; it controls tension, traverse, turn count, and layer sequence so the finished component survives electrical, mechanical, or thermal load. That shift changes every selection variable. Buyers auditing winding automation must stop comparing servo axes to machining centers and start asking whether the route, tension, and changeover discipline can be repeated reliably. If hidden defects are expensive and manual skill carries the process, the machine’s real job is stabilizing function, not accelerating motion.
Why Winding Machines Do Not Fit The Standard CNC Buying Checklist
When most production engineers hear “CNC,” they picture a spindle removing material: a router cutting panels, a mill profiling aluminum, or a lathe turning shafts. That mental model is useful for subtractive equipment, but it actively misleads buyers evaluating winding machines. A winding machine does not cut stock into geometry. It controls how wire, filament, or strip is fed, tensioned, counted, and laid down so the finished component behaves correctly under electrical, mechanical, or thermal load.
That distinction changes the entire purchasing framework. A machining center is judged by material removal rate, rigidity, chip evacuation, and repeatable cut paths. A winding machine is judged by whether it preserves turn count, layer sequence, tension behavior, and pattern logic well enough for the finished part to meet its functional requirements. The part may look orderly from the outside and still fail in service if the winding route drifted during production.
For buyers, the real question is not whether a winding machine qualifies as “another kind of CNC.” It is whether the product family depends enough on repeatable winding control that manual or semi-manual methods have become the hidden source of quality risk, slow changeovers, or throughput loss. Once the decision is framed that way, winding equipment stops looking exotic and starts looking like what it actually is: a process-control machine for function-sensitive products.
Winding Controls Placement, Not Material Removal
The cleanest way to separate winding from standard CNC work is to look at what physically happens on the shop floor. A router removes material. A mill removes material. A lathe removes material. A winding machine builds a controlled structure by placing a continuous medium according to a programmed pattern. The part emerges from accumulation and sequence rather than from subtractive shaping.
That changes which variables matter. In machining, tool wear, spindle load, and cut strategy dominate the conversation. In winding, the central issues are tension behavior, feed control, turn counting, traverse accuracy, indexing, insulation handling, and how reliably the machine can repeat a specific winding sequence over time. The machine succeeds when the wound structure performs correctly, not when the motion looks impressive on its own.
This is why buyers should avoid comparing winding equipment to standard CNC tools at the feature-label level. Servo axes and programmable motion may appear in both categories, but the performance question is fundamentally different. A winding machine is not “like a mill but for wire.” It is a production system for functional placement.
Where Winding Equipment Earns Its Keep
Winding machines are common in applications where the finished product’s behavior depends directly on how turns, layers, or coils are formed. Motors, transformers, inductive components, specialty coils, and related electromechanical parts often fall into this category. In each case, the machine is not simply making something neat. It is making something that must behave consistently under load, current, heat, or mechanical use.
That is why automation becomes attractive earlier in winding than some buyers expect. In many manufacturing processes, manual work can survive for a long time if appearance is acceptable and tolerance windows are forgiving. Winding is less forgiving because small process drift can create functional variation that is expensive to catch later. A component can look orderly and still fail electrically or thermally because the route was inconsistent.
The broader lesson is that winding equipment is usually justified by function sensitivity more than by visual complexity. If product behavior changes when winding behavior changes, a programmable route becomes easier to justify.
Tension Control Is The First Variable To Audit
When buyers first explore winding automation, many focus on speed, axis count, or software. Those matter, but tension control is often the real foundation. If tension changes during the process, the winding build changes with it. Layers can settle differently, spacing can drift, and the final part can behave differently even when the nominal turn count still looks correct. Stable tension is therefore not a secondary convenience. It is part of the part itself.
This is also why winding should never be treated as simple motion. The machine is not only moving from point to point. It is managing the behavior of a live material while it is being fed and placed. Spool drag, guide path condition, media quality, feed consistency, and the interaction between tensioning components and motion control all influence the final result.
A buyer evaluating winding equipment should therefore ask a hard practical question: how does this machine maintain stable tension during real production, not just in a clean demo sequence? A fast machine with inconsistent tension can create more hidden scrap cost than a slower machine with stronger control discipline.
Traverse And Index Logic Play The Role Toolpaths Play In Machining
In standard machining, toolpaths define how the tool moves through stock. In winding, traverse and indexing logic play a similar role. The machine has to know when to move laterally, when to shift layers, how to maintain pattern spacing, when to reverse or step, and how to preserve the same route across repeated parts. This is where CNC control becomes genuinely valuable.
The program is not only there to automate motion. It is there to preserve intent. If the route cannot be recalled reliably, or if operators keep reconstructing setups from memory, then the process remains more manual than buyers may realize even after automation has technically been introduced. That is why recipe management, program retention, and setup repeatability matter so much in serious winding operations.
Strong winding production usually treats the program as part of quality control. It is the formal memory of how the product is supposed to be built. Any machine that makes program recall fragile or changeovers informal should be reviewed very carefully.
Hidden Defects Make Turn Count Integrity A Quality Issue
One of the reasons winding equipment creates a different buying conversation from standard CNC tools is that defects are often hidden. A machined part with a bad profile can often be measured quickly. A wound component can look visually tidy and still carry a process defect that only appears in performance testing or later field use. Turn count integrity, layer order, pattern drift, and sequence mistakes may not be obvious from a simple visual pass.
This creates a different quality culture. Buyers should not ask only whether the machine winds neatly. They should ask whether the machine protects the variables that make hidden defects less likely. That includes counting logic, controlled route execution, tension consistency, and setup repeatability between lots.
The more expensive the downstream test, rework, or failure exposure becomes, the more valuable stable winding automation usually is. That is one reason companies often invest in winding control not because winding looks difficult, but because the consequences of small inconsistency are too costly to absorb casually.
What Winding Machines Optimize That Standard CNC Tools Do Not
Standard CNC tools are usually optimized around one central outcome: remove material efficiently while preserving the required quality. Winding machines optimize a different outcome: build a functional wound structure consistently enough that the part performs as intended. That means the important features are not identical.
In winding, buyers often care more about tension control, fixture suitability, wire handling path, indexing precision, recipe management, and changeover discipline than about the kinds of cutting metrics that dominate subtractive equipment purchases. If buyers evaluate winding machines through a machining lens, they may overweight the wrong details and underweight the variables that actually affect output quality.
The stronger approach is to start from the finished part and work backward. What makes this product good? Which process variable is most likely to drift? Which setup step causes the most variation today? How much of the current quality result depends on one skilled operator compensating in real time? Those questions reveal more about winding-machine value than generic automation language ever will.
Changeover Discipline Becomes Critical As Product Mix Expands
Some winding operations run the same configuration repeatedly. Others shift between multiple part types, turn counts, or winding patterns. In the second case, changeover discipline becomes a major part of the machine’s value. If operators can recall recipes reliably, move between jobs with less interpretation, and restore the correct route without rebuilding everything from habit, the process becomes much easier to scale.
This is where buyers often discover the difference between basic automation and production-ready automation. A machine that can technically wind several part types is not necessarily a machine that can switch between them smoothly. If product mix is rising, and setup memory currently lives in notebooks, operator habits, or tribal knowledge, winding automation can create value by turning that fragile memory into a stable digital process.
For many shops, this is the hidden tipping point. The decision is not that manual winding has become impossible. It is that manual variation in changeovers has become too expensive.
Throughput In Winding Means More Than Speed Per Part
Buyers also need to be careful with the word throughput. In winding, throughput is not only how quickly one part can be wound. It is how reliably the line can create acceptable parts without slowing down on correction, setup variation, retesting, or operator-dependent recovery. A machine that winds faster but produces unstable output may lower true throughput once rejects and interruptions are included.
This means winding productivity should be judged at the route level, not only at the machine level. How much time is lost to re-setup? How often does an operator intervene to correct a pattern? How much inspection load exists because the route is hard to trust? These questions matter as much as nominal machine speed because they reveal whether the machine is helping the process or merely accelerating unstable behavior.
In many operations, the winning machine is not the one with the boldest speed claim. It is the one that produces a calm, repeatable route with fewer surprises per shift.
Manual Winding Stops Scaling Before Demand Stops Growing
The investment case for a CNC winding machine becomes strongest when manual or semi-manual winding has clearly reached its limit. That limit may appear in several ways: rising labor dependence, inconsistency between operators, growing rework, slow changeovers, unstable output under higher volume, or the inability to document and repeat successful setups reliably.
At that point, automation is no longer about replacing hands for the sake of modernity. It is about protecting process stability. The machine’s real value comes from shifting the result away from live operator compensation and toward controlled, repeatable execution.
This matters especially in operations where quality failures are expensive to catch late. If the process depends on one experienced operator to keep everything stable by feel, the route may already be more fragile than management realizes. A winding machine can create value by making the process more formal, more repeatable, and easier to sustain as demand rises.
Fixtures, Guides, And Termination Handling Shape Real Results
Buyers sometimes focus so heavily on axes and software that they forget how much the mechanical handling path matters. In winding, the route between spool, guide, part form, and termination point is part of the process. If guides wear, if the path introduces drag, if fixtures do not present the work consistently, or if termination handling is awkward, then even a well-programmed machine can lose stability under real production conditions.
That is why winding trials should be evaluated with the full working setup in mind. It is not enough for the machine to demonstrate a clean pattern once. The buyer should consider whether the part can be loaded consistently, whether the guide path stays calm through repeated cycles, whether the transition between winding and downstream termination is clean, and whether the fixture arrangement supports stable repeat production rather than one good sample.
This is another way winding differs from generic CNC buying logic. The value of the machine lives in the total controlled route, not only in the motion system. If the guides, fixtures, or handoff steps are weak, the process can remain fragile even when the machine itself seems technically capable.
Buy A Winding Machine When The Product Depends On Repeatable Winding Behavior
CNC winding machines are used where controlled placement of wire, filament, or similar media directly affects the function of the finished product. They differ from standard CNC tools because they do not primarily remove material. They build a repeatable structure through controlled tension, traverse, indexing, turn counting, and sequence execution.
That is why the buying decision should begin with the process, not the acronym. If the product’s performance depends on stable winding behavior, if hidden defects are expensive, and if manual skill is carrying too much of the route, then a CNC winding machine is not a novelty. It is a practical way to formalize and stabilize production. The strongest reason to buy one is not that it is automated. It is that the winding itself has become too important to leave to drift.
For buyers navigating this decision alongside other equipment purchases, the same selection discipline applies across categories: judge the machine by the production variable it stabilizes, not by whether its control language resembles a standard machining center. That principle holds whether you are evaluating winding systems, panel processing equipment, or any other process-specific machinery in your production line.