Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
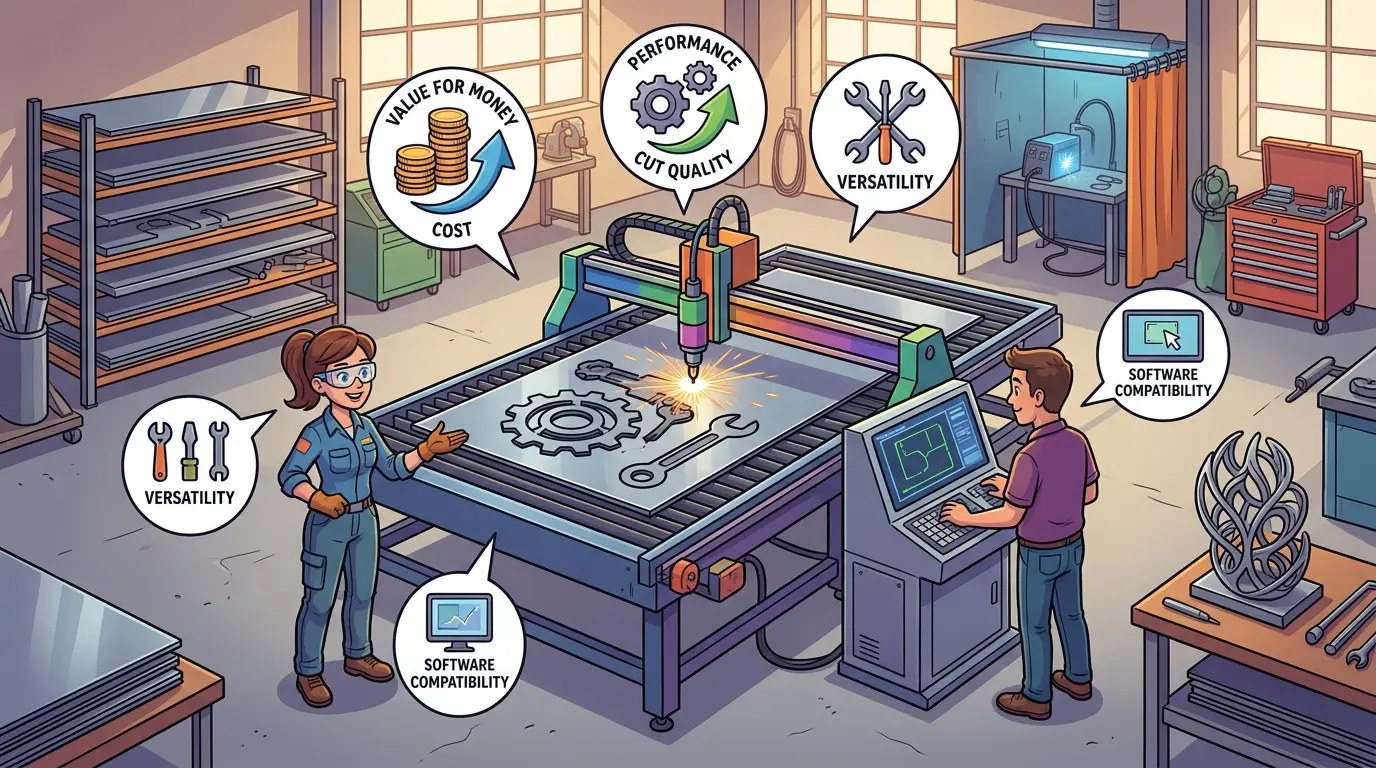
Start with the job, then compare power-source brands or arc-speed claims, a 4×8 plasma table purchase should start with a hard look at your daily material flow. The familiar sheet size is not the real decision; the real decision is whether the machine fits how your shop loads stock, nests parts, removes skeletons, and hands work to bending or welding. Buyers who focus on handling friction, downstream edge condition, slat maintenance, and software repeatability avoid turning a fast-cutting machine into a bottleneck with a labor cost that repeats on every sheet.
Start With the Sheet, Not the Machine
A 4×8 plasma table is an easy category to shop for because the sheet size is familiar and the footprint feels manageable. In daily fabrication, though, that familiar size is not the real decision. The real decision is whether the machine fits the way your shop moves material, cuts parts, and hands work to the next operation.
Before comparing brands or power sources, look at a representative month of orders. Ask what percentage of your work nests naturally on 4×8 stock. If recurring jobs are brackets, gussets, cover plates, tabs, and panels that fit the sheet without waste, the format makes sense. If you are routinely breaking nests, trimming larger sheets to fit, or sending oversized layouts to a secondary process, the 4×8 table is not solving a problem—it is hiding a daily workaround cost.
Run through four questions before you get deep into specifications:
- What share of your order mix fits 4×8 stock without modification?
- How often are nests broken only to fit the table?
- How many jobs currently require manual workarounds because of sheet size?
- Which jobs already feel efficient at this size, and which feel cramped?
If the answers are mixed, a 4×8 purchase can still be right. Just buy it as a deliberate tradeoff, not as an assumed default.
Compare the Cell in the Order Work Actually Moves
Plasma tables are often compared backwards. Buyers start with power-source branding, arc-speed claims, or motion headlines. A stronger comparison starts with the physical route of a sheet through the shop:
- Material is received and staged.
- The sheet is loaded onto the table.
- The nest is prepared and cut.
- Parts, remnants, and skeletons are removed.
- Finished pieces move to deburring, bending, welding, coating, or assembly.
If the proposed system creates friction at any stage in that sequence, operators will feel it every shift, whether or not the brochure mentions it. A table that cuts fast but loads slowly, or cuts clean but unloads awkwardly, is not a productive cell—it is a machine with a bottleneck attached.
Material Handling Usually Separates a Good Cell From a Tiring One
Arc time gets too much attention in plasma buying. Handling deserves more. Ask how easy it is to stage sheets near the table. Can one operator load and unload without awkward strain? Is there enough room to separate parts, park remnants, and clear scrap without turning the surrounding floor into a temporary storage zone?
These questions matter because a cell can look productive while the torch is moving and still waste time everywhere else. A good 4×8 cell feels organized in the minutes between cuts, not just during the cut itself. If the loading pattern requires two people, or if the skeleton removal routine is awkward, that labor cost repeats on every single sheet.
Downstream Work Should Matter as Much as Cutting Speed
The cutting cell should be judged by what kind of part it hands to the next department. If edge condition forces extra cleanup, if heat distortion creates fit-up trouble, or if small parts leave the table mixed together in a way that slows sorting, the cell is pushing hidden labor downstream.
If the next step is bending, welding, or assembly, ask whether parts arrive in a condition the next operation can absorb quickly. A faster cut that creates more grinding, more sorting, or more downstream delay is not automatically the better production result. The total cost of a part includes what happens after it leaves the table.
Fume Control and Slat Maintenance Are Part of Usable Capacity
Ventilation, water-table behavior, and slat maintenance are not support details to solve later. They are part of usable capacity. If fume behavior is poor, the work zone becomes less pleasant and less safe to run. If slat maintenance is awkward, the table stops feeling orderly and the cell slowly becomes harder to trust.
A cleaner, more manageable cell usually protects productivity better than a machine that only wins the headline-speed comparison. Factor the time and effort required to keep the table in cutting condition into your effective throughput calculation.
Software and Nesting Matter Because Material Cost Matters
Many 4×8 purchases are justified partly on labor and partly on material control. That means software, nest preparation, part labeling logic, and remnant strategy deserve more attention than they often get.
Buyers should ask:
- How easy is it to prepare repeat nests for normal work?
- How clearly can remnants be identified and reused?
- How much operator judgment is required every time a new layout is prepared?
- Does the software path help standardize normal jobs, or does it depend on one advanced user?
These questions matter most in mixed job-shop environments where daily variety exposes software weakness immediately. If nesting depends on one person who “knows the system,” you have a single point of failure, not a production tool.
Height Control and Motion Behavior Affect Labor More Than Buyers Expect
Not all cut problems come from headline power or top speed. In daily work, torch-height control and overall motion behavior often decide whether the table feels dependable. A system that reacts inconsistently to warped plate, heat movement, or changing sheet condition will create more operator intervention than the quote suggests.
That affects edge appearance, consumable usage, part confidence, and whether the operator can manage the cell instead of managing the cut continuously. A table that requires constant babysitting is not a labor-saving purchase. It is a new job.
It is also worth stepping back to compare whether laser and plasma fit different fabrication workflows before treating table size as the only decision. The two processes have different strengths in edge quality, speed, and operating cost, and the right choice depends on your part mix.
Service Access Matters More Than Buyers Admit
Plasma cutting is usually bought to improve responsiveness. That means downtime hurts more than buyers sometimes admit during the shopping phase. The stronger the business case depends on quick turnaround, the more important service access, consumable support, and troubleshooting clarity become.
Ask who answers the phone when the table stops. Ask how quickly consumables can be sourced. Ask whether the manufacturer provides clear diagnostic paths or leaves you to guess. The table is only valuable when it is producing.
Compare the Table Against Your Shop Type, Not Against a Generic Ideal
The right 4×8 plasma table for one metal shop can be the wrong one for another because the workloads are different. This matrix is more useful than a generic feature list:
| Shop Reality | What the Table Must Do Well | What Buyers Should Watch Closely |
|---|---|---|
| Mixed job shop with many part numbers | Fast setup, flexible nesting, easy sorting, fast reloads | Software ease, operator workflow, part recovery, remnant handling |
| Repeat fabrication of common parts | Consistency, predictable cycle flow, low interruption | Consumable stability, unloading routine, maintenance burden |
| Small shop with limited floor space | Compact cell behavior without creating clutter | Surrounding access space, loading pattern, skeleton handling |
| Growing shop planning more internal cutting | Room to scale workflow discipline, not just cut speed | Software repeatability, service support, downstream integration |
| Shop where cutting feeds bending and welding every day | Predictable part release and manageable edge condition | Sorting logic, edge-cleanup burden, downstream handoff |
Quote Comparison Should Focus on the Daily Method
By the time a shop is reviewing quotes, the discussion should already be broader than machine specification. The key question is not only what is included. It is what kind of daily method the quote actually assumes.
Does the quote assume a certain loading pattern? Does it make remnant handling easy or leave it to the shop? Does it assume a level of maintenance discipline that has not been discussed? Is the software and support path clear enough to protect uptime?
It still helps to compare machinery quotes line by line and, if factory-direct buying is part of the conversation, to review what to verify before committing. The cheapest quote is only cheap if the daily method it assumes matches your shop.
When 4×8 Is a Strong Fit and When It Is Quietly Too Small
A 4×8 plasma table is usually a disciplined purchase when the shop processes standard sheets regularly, needs a contained cell, and benefits from a cutting station that stays manageable for loading, unloading, and cleanup.
That is often true in small and mid-sized fabrication shops where:
- Standard sheet work dominates the order book.
- The team wants better nesting control than manual cutting offers.
- Floor space is at a premium.
- Oversized plate is not the main revenue driver.
- The shop values a cell one team can keep under control every day.
The same format becomes limiting when the shop repeatedly works around the table instead of through it. If that pattern is persistent, the issue may be format mismatch rather than weak operator discipline. In that case, it is useful to compare the 4×8 decision directly against the step up to a 5×10 plasma table when larger cutting area starts paying back.
The Best 4×8 Purchase Is the One That Makes the Cell Feel Predictable
This kind of purchase should be judged by daily production burden, not only by the number at the bottom of the quotation. Buyers should normalize startup help, training, install expectations, maintenance access, consumable planning, spare parts, and support response before calling one table cheaper than another.
The real business case should be tied to visible operating gains: cleaner sheet movement, calmer cutting, faster part release, less cleanup friction, and output that the next process can absorb without drama. The most useful comparison is not which machine claims the most. It is which one lets the shop run a calmer, cleaner, better-controlled cutting cell every day.
Cut Quality Expectations: What Plasma Can and Cannot Deliver
Before committing to a 4×8 plasma table, it is worth being precise about the edge quality you can expect. Plasma cutting produces a heat-affected zone, a slight taper on the cut edge, and a characteristic dross pattern that varies with material thickness, amperage, and travel speed. This is not a flaw in the machine; it is the physics of the process.
Shops that understand this tend to be more satisfied with their purchase. Shops that expect laser-like edge finish from a plasma table are usually disappointed, regardless of which brand they buy.
Ask yourself what your downstream operations actually require. If parts go to grinding or sanding before coating, minor dross and edge taper are absorbed quickly. If parts go directly to tight-fit welding or precision bending, you may need to budget for edge cleanup that the cutting process cannot eliminate.
Material thickness also changes the picture. A 4×8 plasma table that cuts 10-gauge sheet cleanly may produce noticeably more dross on 1/2-inch plate. The same machine that handles thin material at high speed may require slower travel and more operator attention on thicker stock. Compare the machine against the thickness range that actually dominates your order book, not the maximum rating in the brochure.
Consumable Life and Operating Cost Are Predictable—If You Track Them
Plasma consumables—nozzles, electrodes, swirl rings, and shields—wear with every start and every hour of cutting. The cost per part depends heavily on how the machine is operated and maintained. Shops that track consumable life across different material types and thicknesses can predict operating cost with reasonable accuracy. Shops that do not track consumables tend to discover the cost only when the cutting quality suddenly degrades mid-job.
Piercing technique matters as much as cutting technique. Every pierce stresses the nozzle and electrode. A nest with hundreds of small holes will consume consumables faster than a nest with a few large parts, even if the total arc time is similar. If your work involves many small parts with frequent pierces, factor that into your consumable budget.
Cutting with dry air versus nitrogen or other gas mixes also changes consumable life and edge quality. The gas choice affects both the cost per part and the consistency of the cut. Ask the manufacturer for realistic consumable-life expectations under your specific duty cycle, and build that into your per-part cost model.
Water Tables Versus Downdraft: A Decision That Affects Every Shift
One of the most consequential choices in a 4×8 plasma table purchase is how the machine handles fumes, dust, and heat. The two dominant approaches are water tables and downdraft systems, and each changes the daily workflow in different ways.
Water tables submerge the cutting zone, which suppresses fumes, captures dross, and reduces heat buildup in the workpiece. The tradeoff is water maintenance: sludge removal, water level checks, and occasional cleaning. In humid environments, water tables can also create rust concerns on parts that sit before finishing.
Downdraft systems pull fumes and fine dust through the cutting surface into a filtration unit. They keep the work area drier and make parts easier to handle immediately after cutting. The tradeoff is filter maintenance and the fact that some dross still accumulates on the table surface and slats.
Neither approach is universally better. The right choice depends on your shop’s ventilation situation, your tolerance for water maintenance, and whether parts need to move to downstream operations quickly. A shop in a shared building with limited exhaust capacity may need a water table to control fumes. A shop with good ventilation and a fast part-flow may prefer the drier workflow of a downdraft system.
Slat Management: The Quiet Driver of Cut Consistency
Slats—the metal bars that support the sheet during cutting—are easy to ignore during the buying process and impossible to ignore during production. As the torch cuts, it inevitably nicks the slats. Over time, the slats wear unevenly, and the sheet no longer sits flat. That uneven support translates directly into inconsistent cut height, more dross, and more operator intervention.
Ask how the slat system is designed. Can slats be rotated or replaced individually? How long does a slat change take? Is the slat spacing appropriate for the material thickness you cut most often? A table with a well-designed slat system can run for weeks with minimal attention. A table with poor slat access can turn a 15-minute maintenance task into a half-day project.
Some shops keep a spare set of slats and rotate them on a schedule. Others replace slats only when cut quality visibly degrades. Either approach works, but the machine design determines how painful the routine is. Factor slat maintenance into your effective uptime calculation, not just the cutting speed.
Pierce Height and Edge-Start Behavior Affect Part Consistency
The moment before the cut begins—the pierce—is where many quality problems originate. If the torch pierces at the wrong height, the initial cut can be rough, the consumables can wear prematurely, or the part edge can show a noticeable defect at the start point.
A good plasma table manages pierce height automatically, lifting the torch to a safe distance, piercing, then dropping to cutting height. The consistency of this sequence determines whether every part in a nest looks the same or whether the first part of each cut cycle shows a defect.
Shops cutting thin material should also pay attention to edge-start behavior. Starting the cut at the edge of the sheet, rather than piercing in the middle, reduces consumable stress and produces a cleaner edge. If your work involves many edge-start cuts, the machine’s ability to handle this pattern reliably matters more than its maximum speed.
Training and Operator Skill: The Hidden Variable in Every Purchase
A 4×8 plasma table concentrates a significant amount of production capability into one cell. That concentration works only if the operators running the cell can use the machine effectively. Training is not a one-time event at installation; it is an ongoing process as operators encounter new materials, new part geometries, and new nesting challenges.
Ask what training is included with the purchase. Is it limited to basic operation, or does it cover nesting strategy, consumable management, and troubleshooting? Can the manufacturer provide documentation that operators can actually use on the shop floor, or is the knowledge locked in a service manual that nobody reads?
Shops with high operator turnover should think carefully about how easy the machine is to learn. A table that requires deep expertise to run well will struggle in a shop where operators rotate frequently. A table with clear prompts, simple nesting software, and predictable workflows will maintain quality even when the person at the controls changes.
Electrical and Air Requirements: Verify Before the Concrete Is Poured
Plasma cutting places specific demands on electrical supply and compressed air. A 4×8 table with a 60-amp or 80-amp plasma power source draws significant current, and the supply must be sized correctly to avoid voltage drops that affect cut quality. Compressed air must be clean, dry, and delivered at adequate pressure and flow—moisture or oil in the air supply will degrade cut quality and shorten consumable life.
Before finalizing the purchase, verify that your shop’s electrical panel can handle the machine’s draw without tripping breakers during heavy use. Check the air compressor’s duty cycle against the plasma system’s consumption. If the compressor runs continuously during cutting, it may overheat or fail to maintain pressure.
These checks are easier before the machine arrives than after. A table that cuts beautifully in a demonstration but starves for air or power in your shop will not deliver the performance you paid for. Include electrical and air verification in your pre-purchase checklist, not as an afterthought.
Resale Value and Future-Proofing: A Practical Consideration
Most shops buy a 4×8 plasma table expecting to use it for years. Still, it is worth considering how the machine will hold its value and whether it can grow with your shop. A table from a manufacturer with an active user base and ongoing software updates will retain value better than a machine from a brand with limited support.
Ask about software upgrade paths. Can the nesting software be updated as new features are released? Is the control system based on a platform that will remain supported? A machine that becomes obsolete because its software cannot be updated is a poor investment, regardless of how well it cuts.
Also consider whether the table can be expanded or reconfigured. Some machines allow for additional tooling, upgraded power sources, or enhanced automation later. Others are fixed at the configuration you buy. If your shop is growing, a machine that can evolve with your workload is worth more than one that cannot.