Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
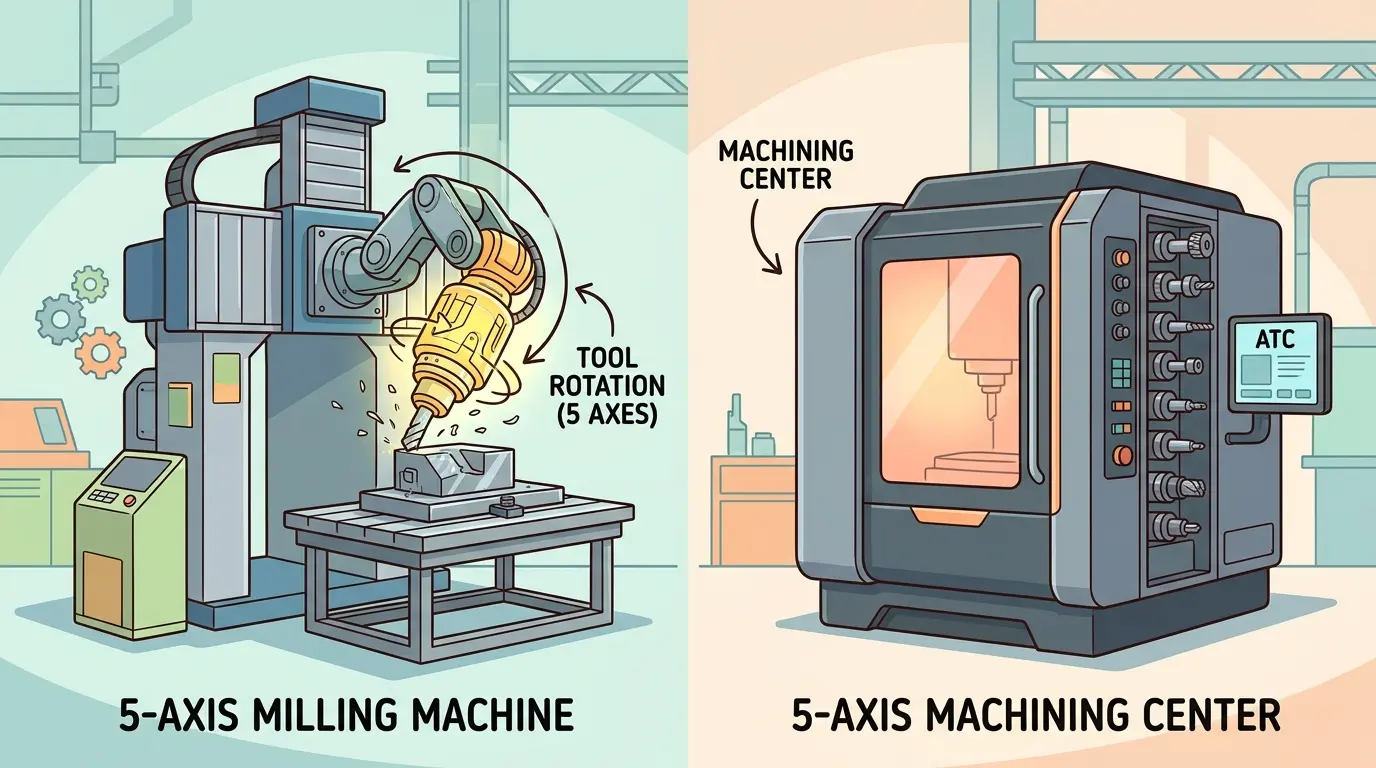
Procurement teams comparing five-axis quotes often find two suppliers offering identical kinematic capability under different names—one labeled a milling machine, the other a machining center—yet the terminology reveals little about daily shop-floor behavior. The real distinction lies in the production philosophy wrapped around the motion: whether the package delivers repeatable batch output through automatic tool changing, probing, and containment, or prioritizes open access for varied, custom-fixtured work. Before evaluating price, buyers must determine whether their dominant production stress is standardization or adaptability, because that decision determines which package features actually justify the investment.
Start With the Production Problem, Not the Product Name
Procurement teams and production engineers routinely hit the same wall when comparing five-axis equipment: two suppliers quote machines that both move on five axes, but one is called a 5 axis milling machine and the other a 5 axis machining center. The labels create confusion because they suggest a clear technical distinction that often does not exist in practice.
The more useful question is not what the machine is called, but what the quoted package is actually designed to do on your shop floor. A supplier may use either term for equipment with identical kinematic capability. The difference usually shows up in the production philosophy wrapped around the motion: one quote tends to describe a controlled, repeatable production cell, while the other tends to describe a more open, access-oriented platform for varied work.
Understanding that distinction matters more than the terminology, because it changes how you evaluate the quote, what you inspect during acceptance testing, and how the machine will behave in daily operation.
Translate the Labels Into Buyer Language
When you see machining-center language in a quotation, it usually signals a more integrated production package. That means automatic tool changing, probing or setup verification, software and postprocessor support, and containment for chips, dust, or coolant. When you see milling-machine language, it usually signals a more flexible setup with broader physical access to the workpiece and fewer assumptions about standardized routines.
That distinction translates into a practical buying decision:
| Buyer priority | The quote often leans toward |
|---|---|
| Repeatable batch output with standardized routines | 5 axis machining center |
| Flexible setups, changing fixtures, broader physical access | 5 axis milling machine |
This is a translation rule, not a universal law. Machine builders do not all follow the same naming discipline, so you still have to verify what is actually included in the package. But the rule gives you a starting point for asking the right questions.
Buy the Production Package, Not the Name
If your plant needs a five-axis machine to behave like a controlled production cell, the deciding issue is not whether the catalog page says machining center. The deciding issue is whether the package includes the elements that repeatability depends on:
- Automatic tool changing that supports longer machining sequences without operator intervention
- Probing or setup verification routines that catch errors before the cut starts
- A usable software and postprocessor path that matches the CAM environment your programmers actually use
- Containment and housekeeping control that keeps chips, dust, or coolant from becoming a production variable
- A clear route for operators to recover the next job consistently after interruptions or shift changes
If those pieces are present, the machine is commercially behaving like a machining center whether or not the supplier uses the exact term. If those pieces are missing, the label alone does not create production control. You are buying a five-axis machine that will require more manual decisions around it, regardless of what the quotation calls it.
Ask What the Shop Actually Needs to Standardize
Some factories need the next five-axis purchase to become a stable repeat-production asset immediately. The machine will run the same families of parts, hold the same datums, and follow the same tool paths week after week. Other factories need the machine to stay more open because the work changes constantly and fixture assumptions are still fluid.
That difference matters more than naming. If the real need is standardization, ask how the machine supports repeat datums, repeat tool flow, repeat probing, repeat cleanup, and repeat operator recovery after interruptions. If the real need is adaptability, ask how the machine handles unusual fixtures, changing part envelopes, irregular loading, and setup freedom without becoming awkward.
These are different engineering problems. A machine that excels at one may be mediocre at the other, and the label on the quotation will not tell you which one you are getting.
When Access Beats Automation Depth
Some buyers do not need maximum integration first. They need physical freedom around the part. This is common when workpieces are large, awkward, tall, custom-fixtured, or loaded in many different ways. In those cases, a more open five-axis milling platform may create more value because it reduces changeover friction and makes real setup work easier.
This situation often appears in:
- Contoured wood components that require access from multiple angles
- Large custom furniture parts that are difficult to maneuver into an enclosed envelope
- Irregular fixtures that do not fit a standardized workholding template
- One-off patterns or prototype forms where setup speed matters more than cycle-time optimization
- Certain stone pieces where support structure and approach space matter heavily
If your work fits this profile, an enclosed machining-center format may actually slow you down. The access you lose to the part can outweigh the automation you gain. The right choice depends on which constraint hurts your production more: the time lost to setup awkwardness or the time lost to manual intervention during the cut.
Structure Usually Tells the Truth Faster Than Vocabulary
The machine layout often reveals the real commercial intent faster than the product name does. An enclosed, more integrated structure typically fits cleaner process control. A more open bridge or gantry style typically fits access-driven work. Neither is automatically better. The right layout depends on whether your production problem is repeatability or adaptability.
When you evaluate a quote, verify these structural points directly:
- Where the rotary motions occur, and whether that arrangement suits the part geometries you actually cut
- What usable clearance remains with real fixtures in place, not just the theoretical maximum envelope
- How easy loading and unloading are with actual parts, including how operators reach the workholding
- How the structure behaves with the intended material and housekeeping load, especially for stone or heavy wood components
These points are often buried in the fine print of a quotation or left for the acceptance test to reveal. Do not let them wait that long. Ask for the structural details before you compare pricing.
Enclosure and Containment Change the Daily Operating Model
One practical difference often hiding behind the terminology is containment. A machining-center-style offer usually points toward better enclosure, cleaner chip or coolant control, and more stable operator routines around the machine. A milling-machine-style offer usually leaves more room for open access and more flexible interaction with the part.
This changes the daily operating model in ways that are easy to underestimate during the buying process. If your problem is environmental control and repeat shift behavior, containment carries more weight. Operators can follow a more predictable routine, housekeeping is more contained, and the surrounding workspace stays cleaner. If your problem is physically getting difficult work onto the machine and clamped correctly, access carries more weight. An enclosure that protects the process can become an obstacle when you are wrestling a large, awkward part into position.
For stone-related applications, judge this against the real stone CNC workflow context rather than by terminology preference alone. Slurry management, dust extraction, and the physical weight of the workpiece all change the containment calculation.
Workholding Strategy Separates the Two Paths
The quickest way to see which direction fits your operation is to study the fixture logic. If the plant can standardize datums, fixture families, and repeated part setups, a machining-center-style package usually becomes more attractive because it converts that stability into predictable throughput. The machine can run longer sequences with fewer manual interventions, and the investment in automation pays off through reduced labor per part.
If the work changes constantly and each job needs different pods, clamps, custom jigs, or support methods, a more flexible milling-platform approach may be better. It reduces setup awkwardness instead of forcing every job into a rigid production template. The cost of that flexibility is usually lower automation depth, which means more manual decisions during the cut. But if your workholding changes every job, that trade is often worth it.
Tool Flow and Recovery Matter More in Machining-Center-Style Packages
If the shop expects the machine to behave as a controlled production cell, tool flow becomes a core buying variable. Automatic tool changing, tool-life logic, setup verification, and predictable restart behavior all matter more when the machine is supposed to hold a steadier production rhythm.
This is often where machining-center-style packages justify their cost. The machine is not only moving in five axes. It is reducing the number of manual decisions required around it. An operator who would otherwise stop the machine to change tools, verify setup, or recover from an interruption can instead monitor multiple machines or handle downstream tasks. That labor saving is the real return on the higher purchase price.
If the quote does not clearly state what tool-flow automation is included, ask directly. A five-axis machine without automatic tool changing is not a production cell. It is a flexible milling platform that happens to move on five axes.
Software Support Can Make the Simpler-Looking Machine Harder to Own
Five-axis buying decisions are never only about iron. The digital workflow matters too much. A machine with excellent kinematics but poor software support will cost you far more in programming time and trial-and-error than the purchase price difference between quotes.
Useful supplier questions include:
- Is the required five-axis control scope already enabled, or is it a paid option that appears later in the quote?
- Is the postprocessor path proven for the CAM environment the plant uses, or will your programmers have to develop and validate it themselves?
- What collision-checking routine is expected, and is it included in the software package or an extra-cost add-on?
- What operator and programmer training is actually included, and does it cover five-axis-specific workflows or just basic machine operation?
Sometimes a machining-center-style quote looks more expensive because it includes more of the software and startup discipline needed for stable five-axis ownership. That higher price may be the cheaper option in the long run, because it reduces the risk of buying a machine that your team cannot program and run effectively.
Inspection and Setup Confidence Belong in the Comparison Too
Another useful distinction is how much setup confidence the package supports. A buyer looking for a machining-center-style route usually cares more about repeat setup verification, probing routines, and the ability to recover a job with less judgment-based variation. The machine should be able to confirm that the part is where it is supposed to be before the cut starts, and that the tool is the right one with the right geometry.
A buyer leaning toward a more open milling platform may accept more manual judgment if that trade buys enough access and flexibility. The operator checks the setup visually, makes adjustments, and relies on experience to catch problems. That approach works when the work is varied and the operator has the skill to handle it. It becomes a liability when the same part runs repeatedly and small setup variations create scrap.
The inspection habit around the machine should match the expected production style. If you plan to run repeat batches, invest in the probing and verification package. If you plan to run one-off work, that investment may be wasted.
Housekeeping Also Pushes the Decision
Five-axis machining changes the mess around the tool as well as the motion of the tool. Dust, chips, coolant, or slurry management can all affect what kind of machine package makes daily sense. A five-axis machine generates debris from multiple angles, and the machine structure has to handle that debris without compromising accuracy or creating safety hazards.
If containment and cleaner operator discipline are important, a machining-center format often helps. The enclosure keeps the mess inside, the extraction system handles the debris, and the surrounding workspace stays cleaner. If the work demands open access and the plant can support stronger surrounding housekeeping discipline, a milling-machine format may still be the better fit. But that choice puts more responsibility on the plant to manage dust, chips, or slurry outside the machine envelope.
The Better Choice Usually Matches the Dominant Stress in the Plant
Choose the direction that matches the plant’s dominant stress. If the stress is repeatability, tool flow, process control, and standardized recovery, the buyer usually wants the machining-center-style package. If the stress is access, loading freedom, part variety, and changing fixturing, the buyer usually wants the milling-platform-style package.
That is a much safer way to buy than trying to decide which label sounds more advanced. The label tells you little about how the machine will behave in your specific production environment. The stress analysis tells you what problem the machine has to solve, and that determines which package features matter most.
Questions Worth Settling Before Final Approval
Before signing, force the quote to answer the issues that change production behavior. These are the points that separate a machine that works on paper from a machine that works on the shop floor:
- What real machine structure is being proposed, including the layout of the rotary axes and the overall rigidity path?
- What is the usable envelope with actual fixturing in place, not just the theoretical maximum from the brochure?
- What automation and probing scope is included, not assumed, in the base price?
- What software, post, and training path comes with the machine, and who is responsible for validating it?
- How will housekeeping be managed in the intended application, and does the machine structure support that plan?
- What sample part or acceptance test proves the fit, and what criteria define a passing result?
These are exactly the points that should be normalized when teams compare machinery quotes line by line and verify how much startup risk is being left with the buyer under factory-direct purchasing terms. A quotation that leaves these questions unanswered is not ready for approval, regardless of what the machine is called.
The Better Name Is the One That Matches the Workflow
The practical difference between a 5 axis milling machine and a 5 axis machining center is usually not the fifth axis. It is the production philosophy wrapped around it. One quote is often selling a more controlled cell. The other is often selling more setup freedom.
Buyers should choose based on how the part will be loaded, held, programmed, cut, cleaned up, and handed to the next job. When that route is clear, the label becomes much less important and the right machine becomes much easier to recognize. The machine that matches your workflow will cost less to operate, produce less scrap, and require less troubleshooting than the machine that merely sounds more advanced on paper.