Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
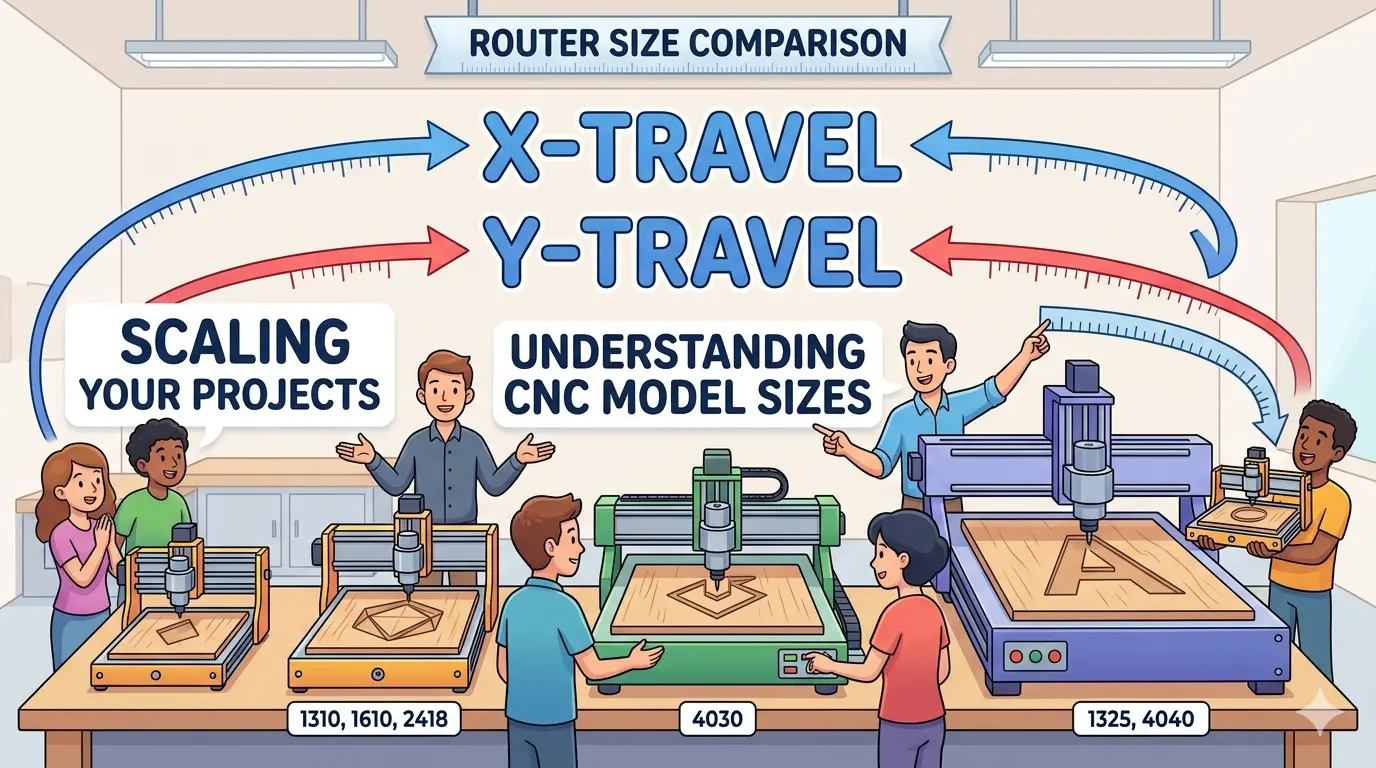
CNC router model numbers like 1310, 1325, and 4040 are routinely mistaken for performance ratings when they only hint at working envelope size. That misreading drives poor purchasing decisions: a compact machine gets assigned production work it cannot sustain, or a larger travel area creates false confidence in frame rigidity, spindle quality, and daily repeatability. This comparison breaks down what each code tier actually removes as a constraint—learning access, bench-scale routing room, or sheet-panel workflow—so you can match the machine to your recurring part burden and setup reality before committing capital.
Router Model Numbers: What 1310, 1325, 1610, 2418, 4030, and 4040 Actually Tell You
Walk through any CNC router listing and you will see the same pattern: a machine described as a “1310,” “2418,” or “1325,” followed by a spec sheet that treats those digits as if they define the machine. They do not. These model numbers are rough size cues, not performance ratings. Two routers sharing the same code can behave completely differently on the shop floor because the number only hints at the working envelope. Everything else—frame rigidity, spindle quality, control reliability, dust management, and daily repeatability—has to be investigated separately.
That gap between what the number suggests and what the machine delivers is where buyers get into trouble. The practical way to compare these codes is to stop reading them as identities and start reading them as workflow thresholds. Each tier points toward a different class of ownership questions, and those questions matter more than the digits themselves.
Read the Code as a Threshold, Not a Datasheet
The model number mainly tells you what kind of operational reality you are about to invite into your shop. At the small end, the risk is buying tiny access while quietly expecting broad capability. The machine is cheap and compact enough to feel like a harmless entry point, then it fails when you ask it to support recurring production work.
In the middle range, the risk shifts. The machine gets just large enough that you start assigning moderate real jobs to it, but the rest of the system may still be amateur: weak hold-down, poor dust strategy, basic controls, and no repeatable daily routine. The envelope invites ambition, but the machine may not be built to carry it.
At the larger end, the code starts pointing toward sheet and panel logic. That is where material handling, spoilboard maintenance, extraction, and downstream flow start mattering more than the number itself. The code is useful, but not because it tells you what the machine is. It is useful because it tells you what kind of ownership questions are about to become unavoidable.
1310 and 1610: Learning Access and Micro Work
Codes like 1310 and 1610 usually sit close to micro-desktop routing logic. Machines in this tier make the most sense for:
- Light engraving
- Tiny prototypes
- Very small decorative or label work
- Simple CAM learning
- Low-stakes experiments in zeroing, toolpaths, and basic workholding
That is not trivial value. These machines buy access. They let a user touch CNC without first solving larger space, extraction, or budget problems. For beginners, labs, and tinkerers, that can be exactly the right answer.
The danger is expecting general CNC freedom from a micro-envelope purchase. The smallest codes solve an entry problem, not a production problem. If the recurring work truly stays tiny, the machine remains useful. If you are already imagining regular custom parts, moderate fixtures, or customer-facing output, this tier is too small for the work you are really thinking about.
The smallest codes are strongest when the buyer says, “I need to learn, test, and make tiny parts.” They are weakest when the buyer says, “I need something small for now, but I want it to stretch into much broader work later.” That is wishful buying.
2418: Familiarity Can Mislead Buyers
The 2418 is widely recognized because it sits in a common entry-level CNC lane. That visibility helps buyers understand the market around it, but it also creates a false sense of safety. A well-known code is not automatically a mature machine class. It simply means more people have bought into that tier and talked about it. The actual fit still depends on what you need to do every week.
2418-class logic is often reasonable for:
- Early CNC skill building
- Hobby routing
- Small craft or prototype work
- Bench-scale experimentation with simple part families
- Users comfortable with a high level of operator involvement
The problem starts when the familiar code gets mistaken for stability. Buyers see a large online footprint and assume the class is already proven for whatever job they have in mind. It is proven for the jobs that fit it. That is a narrower statement.
A 2418-class machine still needs good setup discipline, good workholding, realistic material expectations, and a workflow that accepts operator attention as part of the process. Familiarity does not remove those burdens.
4030 and 4040: The Start of Bench-Scale Temptation
The important break in this list is not the difference between 1310 and 1610. The more important break is the point where the machine becomes large enough to invite broader ambitions. That is what happens around 4030 and 4040.
These size classes remove real frustrations. More working room means:
- Easier fixture placement
- Less clamp crowding
- More comfortable handling of signs and moderate-size routed parts
- A cleaner path for parts that never fit logically on micro desktop machines
Those are genuine gains. But this is also where expectation creep gets expensive. Buyers see the larger work area and begin assigning more serious tasks. They expect greater stability, more forgiving workholding, cleaner daily operation, and sometimes even customer-facing reliability. The trouble is that travel size is only one layer of machine quality. A 4030 or 4040 listing may invite broader jobs without proving the rest of the machine is ready for them.
That is why this tier produces sharply different outcomes. Some buyers love it because it removes a specific part-size constraint. Others regret it because the larger work area made them over-trust the whole machine.
1325: A Different Conversation, Not Just a Bigger Number
The 1325 is the most dangerous code in this list to read casually because it often points toward sheet-oriented woodworking and panel-processing thinking. Buyers hear the number and assume they have crossed into a serious routing category. Sometimes that is partly true. But the number alone still does not prove rigid structure, mature controls, strong service support, disciplined extraction, clean sheet handling, or stable production readiness.
What 1325 does prove is that the ownership questions have changed. At this point, you are no longer only asking whether the part fits. You are asking whether the shop can stage sheet goods, manage hold-down, maintain spoilboards, handle extraction honestly, and coordinate the downstream process well enough to use the larger machine profitably.
That is why 1325 should be treated less like a larger version of a bench router and more like a threshold into another operating model. The machine may sit in the same broad router family, but the daily requirements are starting to look very different.
What the Numbers Never Tell You
When comparing model codes, remember what the number does not tell you:
- Whether the frame stays calm under load
- Whether the spindle is suitable for repeated daily use
- Whether the control stack behaves predictably
- Whether support exists after delivery
- Whether hold-down will be practical for the real parts
- How much dust, cleanup, and spoilboard management the machine will create
- Whether the machine feels like a tool or like a project
Code-based shopping alone is weak. The code sorts the conversation quickly, but it cannot finish it.
Compare the Codes by the Constraint They Remove
A better way to compare these tiers is to ask what repeated limitation each size class is most likely to remove.
| Code Tier | Constraint It Usually Removes | What Buyers Often Misread |
|---|---|---|
| 1310 / 1610 | The barrier to learning CNC at all | They think tiny access means general capability |
| 2418 | The barrier to entry-level bench routing with a familiar ecosystem lane | They mistake popularity for maturity and stability |
| 4030 / 4040 | The part-size and fixture-space limitation of smaller bench machines | They assume larger travel also means broader machine quality |
| 1325 | The limit of smaller-format routing when work begins to look like panel or sheet processing | They assume the code alone proves production readiness |
This table is more useful than spec-sheet worship because it ties each code to a problem it can realistically solve. Good upgrades remove one repeated constraint cleanly. Bad upgrades add capability in theory while multiplying friction in practice.
The Hidden Cost of Moving Up Is Setup Complexity
When buyers move from one code tier to the next, they often focus on the visible gain and ignore the invisible burden. Larger work areas usually mean more than larger parts. They mean more fixture planning, more spoilboard attention, more material staging, more cleanup, and a higher price for weak hold-down decisions. The machine may no longer need job tiling, but it may now demand a more mature routine for clamps, vacuum, dust extraction, and part support.
This is why some owners feel delighted by a modest size jump while others feel burdened by it. The difference is not the number by itself. It is whether the surrounding workflow matured along with the machine size. If the hold-down plan, dust plan, and part-handling plan stay small while the machine envelope gets larger, the upgrade can feel disappointing very quickly.
The Real Comparison Is Between Ownership Models
At a certain point, model-number comparison stops being the best question. The issue is no longer whether 4030 beats 4040, or whether 2418 is a better starting point than 1610. The issue becomes what kind of machine ownership model your work now needs.
If the jobs are still small, irregular, and education-oriented, a smaller code may still be the most honest fit. If the jobs are moving toward signs, moderate fixtures, and more comfortable bench routing, a mid-size bench machine may be enough. If the jobs are turning into panel breakdown, integrated routing, and furniture-style sheet conversion, the real question may no longer be code size. It may be whether the work now belongs in CNC nesting machines rather than in another round of compact-router shopping.
That is also why it helps to review how to choose a CNC router for woodworking and, when relevant, what changes when a nesting machine replaces a general router. There is usually a point where one more code jump is no longer the right framework. If the decision is widening into a broader equipment plan, the Pandaxis product catalog offers a clearer category map than another round of raw model-number debate.
The Smart Comparison
These codes compare well only when you use them for what they are: rough size thresholds that point toward different ownership questions.
1310 and 1610 generally belong to micro-access and learning logic. 2418 often marks the familiar entry-desktop lane. 4030 and 4040 usually sit in the bench-scale range where useful routing room increases but so does the danger of overestimating the machine. 1325 often signals that the conversation has moved toward sheet or panel workflow, where hold-down, extraction, loading, and downstream handling matter as much as the cutting itself.
That is the practical comparison. The numbers help sort the market, but they do not prove machine maturity, daily stability, or production value. The better buying decision comes from matching the code to the recurring part burden, the setup reality, and the ownership model your shop can actually support without turning the machine into a bigger version of the same old frustration.