Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
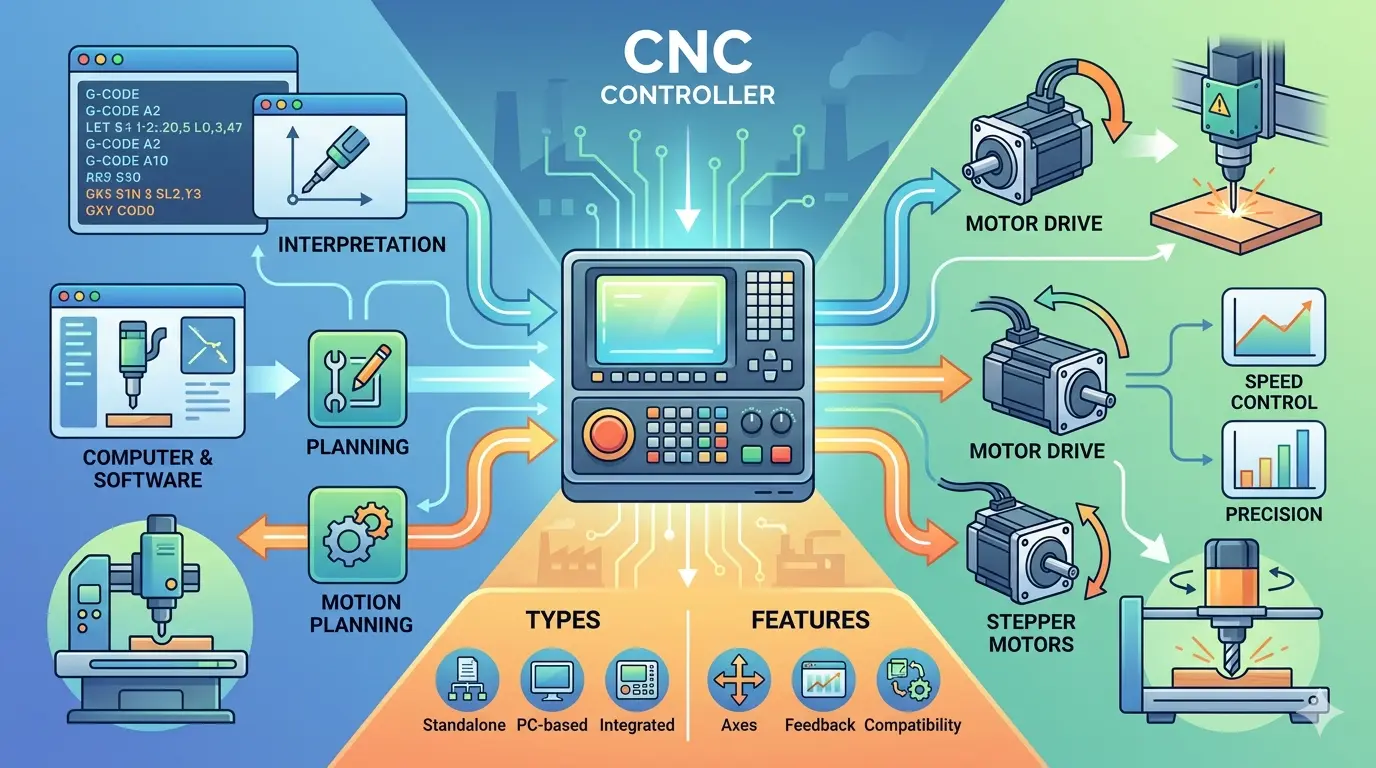
Every CNC machine purchase ultimately hinges on the control layer, yet it is often the least-examined line in a quote. This article cuts through interface hype to show why machine state clarity, motion blending, alarm recovery, and peripheral integration determine whether a router, cabinet line, or stone cell runs predictably across shifts. Buyers must weigh setup discipline, restart behavior, and serviceability against their actual ownership model—prototyping, repeat production, or retrofit—before committing. The controller is not a feature; it is the operating logic that makes trustworthy hardware either dependable or frustrating under real factory pressure.
What the Controller Actually Does Inside a CNC System
At the most basic level, the controller takes machining instructions and turns them into coordinated axis movement. That sounds simple until you remember how many things must stay synchronized at once. The machine needs position awareness, motion planning, speed control, start and stop logic, limit handling, reference management, peripheral control, and operator feedback. The controller sits at the center of all of that.
In practical terms, it governs several layers of machine behavior:
- How coordinate systems are established and maintained.
- How motion commands are blended into real axis movement.
- How feed and spindle instructions are interpreted.
- How homing, referencing, and machine zero are managed.
- How sensors, switches, and auxiliary devices feed into the cycle.
- How the operator sees alarms, status, overrides, and recovery options.
This matters because the controller is not just sending instructions forward. It is also interpreting conditions coming back from the machine. A motor can move only if the system understands where it is, what conditions are safe, what command comes next, and which exception path applies when something goes wrong. The controller is the place where those decisions become either usable or confusing.
That is why buyers should stop thinking of the controller as a feature line in a machine quote. It is part of the machine’s operating logic. If that logic is clean, the whole machine becomes easier to trust. If that logic is muddy, even respectable hardware starts to feel fragile.
Why Machine State Matters More Than Interface Style
Many controller comparisons start at the screen. That is understandable because the screen is what buyers see first. But interface style is not the core issue. The deeper question is whether the controller keeps machine state clear.
Machine state means the controller can answer, without ambiguity, where the machine thinks it is, which offset is active, whether reference has been established, what tool assumptions are in play, what limits apply, and what the machine will do if the operator presses cycle start after an interruption. That clarity is what separates a controller that looks modern from one that is genuinely dependable.
This shows up immediately during setup. An operator does not need a beautiful screen if the process for homing, touching off, selecting the correct coordinate system, and confirming the active origin is still easy to misread. Shops that care about reliable setup discipline usually end up caring a lot about controller quality, because the controller decides whether those daily steps feel structured or improvised.
If the machine state is obvious, setup gets faster and calmer. If the machine state is half visible and half assumed, the machine may still produce parts, but it will do so with unnecessary tension built into every changeover.
Motion Quality Depends on More Than Motors and Mechanics
When buyers talk about cut quality, they often start with spindle power, servo hardware, linear guides, or frame rigidity. Those factors matter. But the controller still shapes how motion becomes part quality.
The controller influences whether the machine moves through short segments smoothly, how it handles corners, how it balances acceleration with path fidelity, and how well it maintains predictable behavior when a program shifts from simple lines to more complex geometry. In routing, profiling, engraving, or contour-heavy work, that difference can affect edge quality, cycle stability, and the operator’s confidence in running the same job again tomorrow.
This is not a claim that the controller alone creates precision. Rather, the controller determines how effectively the machine’s mechanical potential gets turned into repeatable movement. A stiff machine with a weak control layer can still feel jerky, inconsistent, or overly dependent on cautious programming. A well-matched controller helps the machine behave in a more coherent way under real workloads.
Buyers should therefore ask not only whether the axes move, but how predictably the control handles transitions, interruptions, and variation in program complexity. A machine built for repetitive panel work may need one kind of control stability. A machine used for mixed jobs, complex contours, frequent one-offs, or retrofit duties may expose different strengths and weaknesses. Motion quality is not purely a hardware question. It is a system question.
Operators Judge Controllers Through Setup, Alarms, and Restarts
Sales demos make almost every controller look acceptable because the program is already prepared, the machine is already referenced, and the presenter already knows which buttons to avoid. Real production is less forgiving.
Operators judge a controller through small but costly moments:
- The first homing sequence of the day.
- The first work offset check after a fixture change.
- The first alarm during a rush job.
- The first broken tool in the middle of a part.
- The first paused program that must resume without guesswork.
- The first shift handoff when someone else must understand the machine state quickly.
If the controller keeps those moments clear, the machine earns trust. If it turns them into a puzzle, the shop starts building habits around caution, workarounds, and tribal knowledge. That hidden cost is what many buyers miss.
Alarm handling deserves special attention here. A good alarm system does more than flash a code. It helps the operator understand what condition changed, what the machine assumes now, and what must be verified before work continues. Without that clarity, every stop becomes a restart gamble. The risk is not only downtime. It is the temptation to restart with incomplete understanding because the schedule is already tight.
In multi-operator environments, this becomes even more important. A controller that only makes sense to one expert is not a stable production control. It is a dependency. If a machine will run across shifts, across departments, or under uneven staffing conditions, the controller has to support legibility, not heroics.
Integration Requirements Usually Expose the Real Controller Fit
The more a machine interacts with accessories and process devices, the more important controller fit becomes. A simple light-duty platform can tolerate a lighter control burden. Once the machine adds real production features, the controller has to coordinate more than axis motion.
Typical integration questions include:
- Will the machine use an automatic tool changer?
- Does it rely on probing, tool length measurement, or reference sensors?
- Will vacuum zones, clamps, lubrication, or coolant devices need reliable control logic?
- Are there safety interlocks, enclosures, or loading systems that affect cycle flow?
- Will the machine need custom I/O for fixtures, part presence checks, or downstream handoff?
None of this means every shop needs the most complex control platform available. It means the controller should match the event load of the machine. A system that is fine for learning, light routing, or intermittent use can become a poor fit once the machine is expected to coordinate more devices, more safety logic, and more repeatable recovery behavior.
This is where broader comparisons between lighter control ecosystems and industrial controller environments become useful. If a buyer is really trying to understand where the line sits between basic flexibility and production-grade structure, the cleaner next step is to study how lighter control platforms differ from industrial CNC controllers in real machine use. That comparison matters because controller choice becomes much easier once the intended ownership model is clear.
Serviceability and Support Matter Long After Commissioning
Controller selection is often treated like a commissioning problem, but ownership costs usually appear later. The controller influences how easily the shop can back up settings, restore parameters, retrain operators, adjust post-processing, diagnose faults, and maintain continuity when staff changes.
A strong controller match usually supports several practical maintenance goals:
- Backups can be created and understood without drama.
- Parameters are not mysterious to the point of being untouchable.
- Alarm history and status feedback help fault tracing instead of blocking it.
- Routine operator training does not require rebuilding the whole control philosophy from scratch.
- Changes to fixtures, tools, or workflow do not force an unstable chain of workarounds.
That is why buyers should ask who will own the controller after installation, not only who will install it. If the shop must live with the machine for years, then the controller has to be supportable under normal staffing conditions. A system that performs well only when the original integrator is nearby may still be the wrong choice for a factory that values autonomy, fast recovery, and internal process discipline.
This also connects to documentation quality. Clear controller documentation, stable parameter management, and understandable operating logic reduce dependence on memory. That matters more in growing shops than in small expert-led environments, because scale magnifies every weak handoff.
The Right Choice Depends on the Shop’s Ownership Model
Buyers often search for the best CNC controller as if one answer should fit every machine. In practice, the better question is which controller fits the way the shop will own the machine.
For example, a shop building prototypes, testing ideas, or running lower-duty one-off work may prioritize openness, familiarity, and flexibility. A production cell running repeat jobs under schedule pressure may care more about stable setup routines, stronger alarm handling, better I/O coordination, and cleaner restart behavior. A retrofit project may need a control layer that balances reuse of existing hardware with realistic expectations for future support. A growing factory may prioritize operator handoff, training efficiency, and the ability to maintain consistency across shifts.
Those are different ownership models, and they should not be judged by the same criteria. The controller that fits one well may frustrate another.
A practical way to think about it is this: the more the shop depends on repeatability, handoff clarity, and fast recovery under pressure, the more the controller should be judged on structure rather than novelty. The more the shop depends on experimentation, low capital risk, and operator-level customization, the more flexibility may matter. Neither path is automatically correct. The mistake is choosing without first naming the real workload.
Questions Buyers Should Ask Before Signing Off on a Controller
Once the discussion moves past marketing labels, controller evaluation becomes much more concrete. Buyers should press on a few specific areas before accepting a machine configuration.
Ask questions such as:
- How is machine state shown after homing, pausing, or alarm events?
- What is the normal recovery path after a stop in the middle of a part?
- How are offsets confirmed and protected during setup changes?
- Which peripherals, sensors, and machine functions are already integrated, and which require custom work?
- What backup and restore process exists for parameters and settings?
- How much of normal operation depends on one experienced technician knowing undocumented steps?
- How difficult is it to train a second operator to run the machine safely and confidently?
These questions are more valuable than a long list of generic controller features because they connect directly to production behavior. A feature matters only if the shop can use it reliably. A menu matters only if it supports a process. A controller brand matters only if it fits the machine, the team, and the recovery expectations around that machine.
How Controller Evaluation Fits a Bigger Machine Purchase
Most buyers do not purchase a controller in isolation. They purchase a machine, a workflow, and a support burden. That is why controller evaluation should sit inside a broader machine-comparison discipline rather than becoming a side argument between software names.
When you compare machine proposals, controller questions should appear next to questions about frame design, spindle configuration, workholding, automation level, safety features, installation scope, and service expectations. If those controller questions never appear in the quote review, the shop is likely underestimating how much the control layer will shape daily usability. A practical way to tighten that review is to compare machinery quotes line by line before committing, because controller assumptions often hide inside broader wording about options, upgrades, or compatibility.
For buyers still mapping the wider equipment picture, the Pandaxis machinery lineup is the right place to keep controller questions tied to real machine categories rather than abstract controller talk. A controller is never the whole purchase. It is part of how the machine will behave once the factory starts depending on it.
In the end, a CNC controller does three things that matter commercially: it shapes how clearly the machine can be set up, how predictably it runs during normal work, and how safely it can be recovered when normal work breaks. If buyers evaluate it at that level, they usually make better decisions than buyers who compare only names, menus, or theoretical code support. The right controller is not the most impressive one on paper. It is the one that makes the machine trustworthy for the actual workload the shop expects to carry.