Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
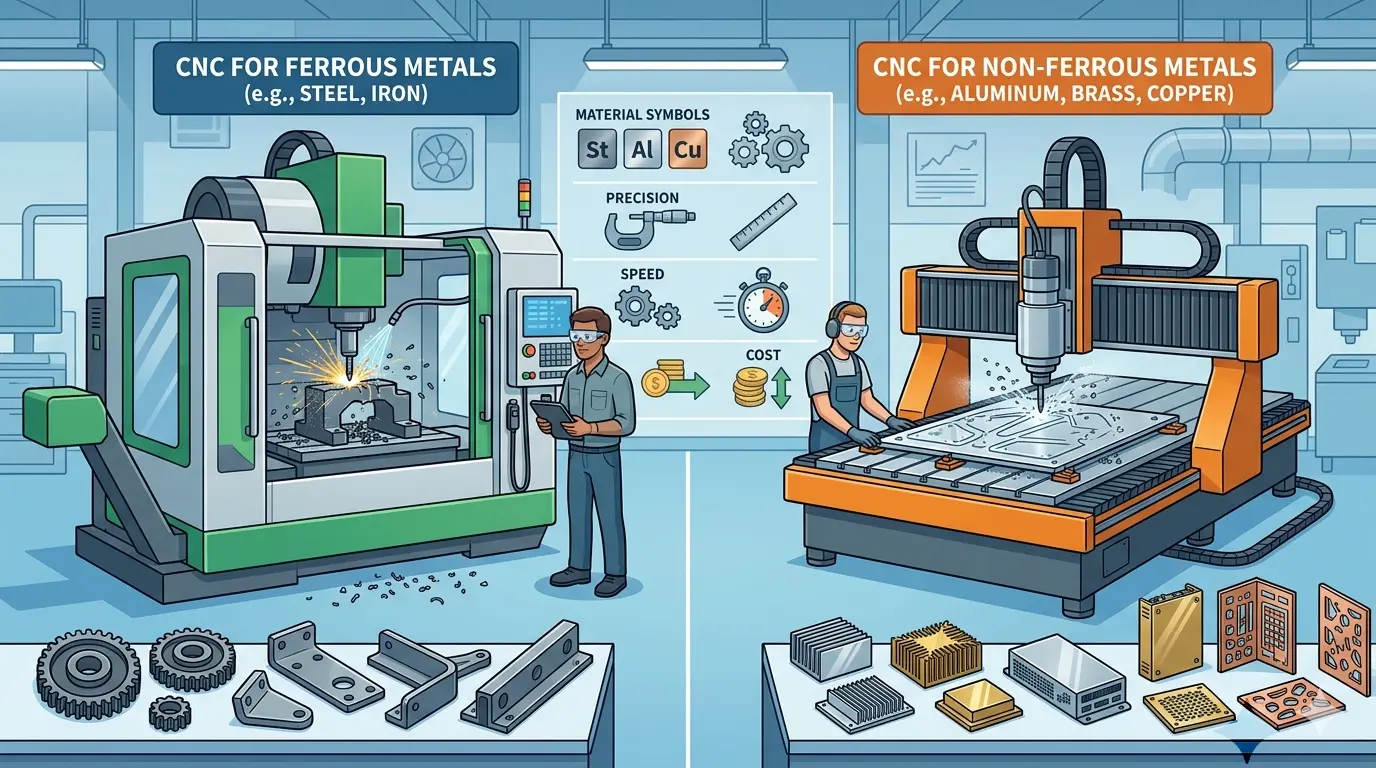
Most metal-cutting equipment purchases fail before a single quote is issued, because the team starts with the machine instead of the work. Flat blanks, turned shafts, and prismatic housings all get forced into one budget line, guaranteeing a compromise that serves none of them. The article forces the selection conversation back to the production route: stock form, geometry family, heat behavior, edge condition, and downstream cleanup burden. Before comparing laser power or spindle torque, you must decide which process removes the real bottleneck—otherwise the most versatile-sounding machine wins simply because it sounds safe.
Why Metal-Cutting Machine Selection Fails Before the Quote Stage
Most metal-cutting equipment decisions go wrong for a reason that has nothing to do with spindle speed, laser power, or axis count. The team starts with the machine instead of the work. Someone says the shop needs “a CNC for metal,” and suddenly flat blanks, turned shafts, machined housings, and welded fabrications are all competing for the same budget line. These part families do not belong in one machine conversation, and forcing them together guarantees a compromise that serves none of them well.
The useful starting point is not the machine. It is the route: what material enters the cut stage, what geometry must leave it, and what condition the next operation can tolerate. Ferrous versus non-ferrous matters, but only after you have defined stock form, edge requirements, heat sensitivity, downstream machining needs, and how much manual cleanup your labor budget can absorb. If those points stay vague, the most versatile-sounding machine usually wins—not because it lowers cost, but because it sounds safe.
Stock Form Decides the Process Family First
Before comparing laser, plasma, waterjet, turning, milling, or sawing, define what the part looks like before cutting begins. A shaft from bar stock, a bracket from plate, and a housing from billet are all metal parts, but they create three completely different process discussions.
Separate the workload into practical groups before any vendor conversation:
| Starting Stock | Typical Geometry | Process Family Usually Shortlisted First | What Usually Decides the Winner |
|---|---|---|---|
| Sheet or plate | Flat profiles, tabs, slots, contours | Thermal cutting, waterjet, saw, shear | Edge condition, thickness mix, downstream weld or finish work |
| Round bar or tube | Diameters, bores, shoulders, threads | Turning | Through-bore need, support on longer parts, finish and concentricity |
| Billet or block | Pockets, faces, datums, drilled patterns | Milling or machining center | Rigidity, workholding, datum control, tool access |
| Rough-cut plate or sawn stock | Features added after blanking | Combined cutting plus machining | How much roughing can be separated from finish-critical features |
This single step prevents the most common capital-planning mistake: comparing machines that are solving different problems, then acting surprised when the low-priced option creates extra work somewhere else in the route.
How Ferrous and Non-Ferrous Materials Change the Route
Material family matters, but not in the vague sense of “can this machine cut steel and aluminum?” The more useful question is how the material changes heat behavior, chip formation, edge cleanup, distortion risk, and tooling demand inside your actual production route.
Ferrous materials push the conversation toward scale, heat management, weld preparation, harder cutting loads, and how edge condition affects downstream fabrication. Non-ferrous materials shift the discussion toward burr control, gummy chip behavior in certain alloys, cosmetic finish, thermal movement, and how quickly light sections lose stability after cutting.
The comparison should focus on operational effects:
- Whether the cut stage can leave a weld-ready edge or a finish-ready edge.
- Whether the material is likely to distort enough to create trouble in assembly or follow-on machining.
- Whether tooling wear or heat concentration will make the process expensive even if the cut itself looks fast.
- Whether the part is sensitive enough that secondary deburring, straightening, or cleanup becomes the real cost center.
If the material discussion never gets this specific, the shortlist is still too abstract to defend.
Flat-Part Work: Choose by What the Next Department Receives
Flat-part cutting decisions are often made on cut speed and contour freedom alone. That is incomplete. The more important question is what the next department receives at the end of the shift. Does fabrication get a clean, stable blank? Does welding get an edge that needs extra prep? Does machining get a rough profile that still needs controlled stock left in the right places?
For sheet and plate work, compare processes through the downstream burden they create:
- How much burr removal is normally required.
- Whether heat affects flatness, coating prep, or weld fit-up.
- Whether the route values high contour freedom more than raw straight-line speed.
- Whether thick and thin materials must share one platform or can be routed differently.
- Whether blanking is the final geometry stage or only the first step before machining.
This is where apparently cheap cutting options become expensive. A fast separation process can still lose if it adds hours of edge prep, straightening, or refixturing later. If your downstream operations are sensitive to edge quality and flatness, a process that leaves a cleaner edge—even at lower raw speed—often wins on total route cost.
Rotational Parts Belong in a Turning Conversation Early
Once the real work is built around diameters, bores, shoulders, grooves, and threads, the selection logic should move out of generic metal-cutting language and into turning language. Shops lose time when they keep comparing flat-stock processes, mills, and lathes together after the part family is already clearly rotational.
The practical trigger is simple: if the feature strategy is organized around axisymmetric geometry, turning usually owns the route. At that point, the better questions are about spindle bore, work support, finish, repeatability on diameters, and whether secondary milling features are frequent enough to change the equipment strategy.
When buyers stay disciplined here, they stop asking for an all-purpose metal-cutting platform and start asking the more useful question: what kind of turning capacity fits the real queue? A lathe with a larger spindle bore or a steady rest for longer parts may cost more upfront but eliminates the need for secondary operations on parts that are already rotational.
Prismatic Parts: Evaluate Through Datum and Workholding Logic
Prismatic metal parts create a different decision structure entirely. If the part needs pockets, faces, drilled patterns, threaded locations, flatness across several surfaces, or positional relationships between features, the issue is no longer how the stock is separated. The issue becomes how reliably the shop can locate, hold, and machine the part through the required sequence.
Milling decisions are usually won or lost on:
- Datum strategy across multiple setups.
- Fixture stability and repeatability.
- Tool access into pockets, walls, and deep features.
- Chip evacuation and heat control during metal removal.
- How much stock condition varies before the part even reaches the machine.
Ferrous and non-ferrous materials still matter here, but they matter through tool life, finish stability, power demand, and deformation risk under clamping or cutting load. A machine that handles aluminum beautifully may struggle with steel if the spindle lacks low-end torque or the frame lacks rigidity. The machine must suit the behavior of the dominant material, not just the broad label “metal machining.”
Cost Heat, Distortion, and Cleanup Before Comparing Capacity
One of the easiest ways to overvalue a machine is to measure only the cut stage and ignore what the cut does to the part. Thermal processes can be the right answer, but they should be selected with a clear view of edge heat, residual stress, cosmetic effect, and how much manual correction the route will tolerate. Cold-cutting or chip-making routes can also be the right answer, but only if they do not create unnecessary handling, slow setup, or avoidable stock cost.
This is where buyers need an honest costing discussion. The useful comparison is not just dollars per hour or parts per hour. It is whether the route after cutting stays stable:
- Does the part go directly to weld, machine, coat, or assembly without heroic cleanup?
- Does the cut stage create variation the next process must fight every day?
- Does the operator need extra touch labor to make the part usable?
- Is the route robust enough that quoting remains accurate when volume rises?
Many disappointing machine purchases come from treating cleanup as a separate problem instead of pricing it into the first decision. A machine that produces parts requiring 15 minutes of deburring each may look productive on paper but loses to a slower machine that produces parts ready for the next operation.
The Best Process Simplifies the Whole Route, Not Just the Cut
Shops sometimes search for the “most capable” machine when the better target is the route with the fewest unstable handoffs. A process that produces a slightly slower first operation may still be the better business choice if it reduces deburring, straightening, weld prep, refixturing, or finish correction. Conversely, a process that looks highly productive at the cut stage may be the wrong answer if it creates constant friction downstream.
Good selection work maps the route from the first cut to the last accepted feature. Ask where the current pain actually sits:
- Are parts waiting to be separated from sheet and plate?
- Are blanks arriving quickly but creating delays in machining or welding?
- Are turned parts the real bottleneck, while flat-part capacity is already adequate?
- Are finish or cosmetic rejects coming from the cut stage rather than the final stage?
Once the bottleneck is visible, machine selection becomes narrower and far easier to defend. You are no longer choosing between machines; you are choosing the machine that removes the specific constraint your shop faces today.
Normalize Quote Comparisons Around Outcomes, Not Hardware
Buyers often compare quotations by machine category and invoice total, but that hides the most important difference: what each process actually delivers to the next step. A quotation for a profile-cutting system is not directly comparable with one for a machining center unless the buyer is explicit about which parts each machine is expected to absorb and what condition those parts should be in when they leave the machine.
Useful quote-normalization questions include:
- Which part families are supposed to move onto this machine and which are not?
- What edge quality, machining quality, or stock condition is being assumed?
- What manual work remains after the machine finishes its part of the job?
- What support burden, training need, and utility burden come with the route?
- How sensitive is the economics to a change in material mix?
If a capital team is comparing several options, it helps to compare CNC machinery quotes line by line before deciding that the lowest headline price is the lowest operating cost. The machine with the higher purchase price often wins when you factor in reduced labor, fewer rejects, and lower downstream correction costs.
Six Production Questions to Lock Before the Shortlist
Before the shortlist is locked, most buyers should be able to answer six practical questions without using any machine-brand language:
- What stock form dominates the workload: sheet, plate, bar, tube, or billet?
- Which geometry family consumes the most hours: flat, rotational, or prismatic?
- How much heat, burr, or distortion can the route tolerate before it becomes expensive?
- Which materials dominate real volume, not only occasional special jobs?
- Which downstream process is currently absorbing too much cleanup or correction?
- Are you buying first-cut capacity, finish-feature capacity, or both?
If the team cannot answer those questions clearly, it should not expect the machine comparison to become clear by itself. The machine will not resolve ambiguity in the production plan; it will amplify it.
Choosing the Route, Not the Label
CNC metal cutting is not one decision. It is a set of decisions about stock form, geometry, material behavior, edge quality, downstream operations, and where the real production bottleneck sits. Buyers get better results when they stop asking for a broad machine label and start asking what kind of part condition the route needs at the next handoff.
When selection work stays that concrete, ferrous versus non-ferrous becomes useful, quote comparison becomes cleaner, and machine choice becomes something operations can defend after installation rather than explain away six months later. The right machine is not the one with the most impressive specification sheet—it is the one that makes the rest of the shop run more predictably.