Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
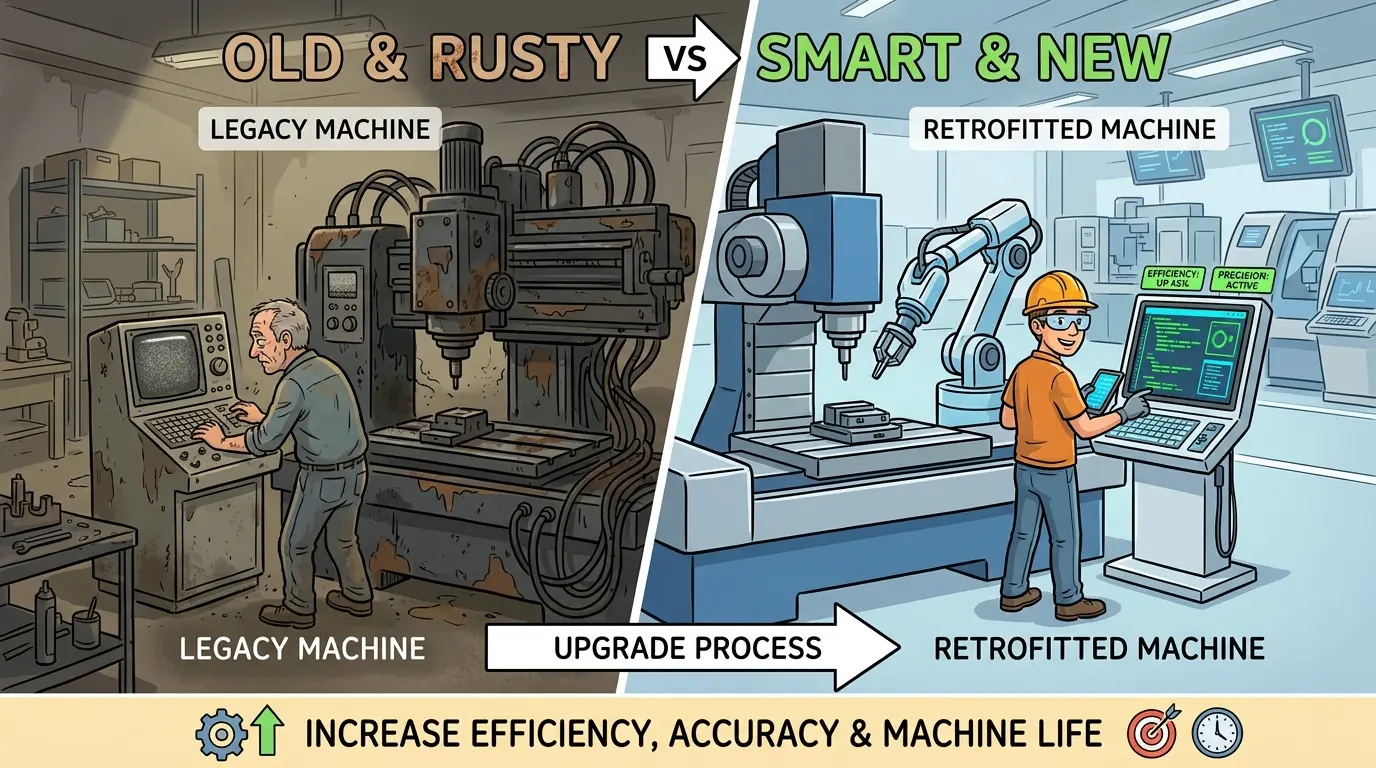
Retrofitting an aging CNC machine is a capital decision that fails when factories confuse electronic obsolescence with mechanical decline. Before any control upgrade, you must triage the iron: verify geometry across full travel, assess spindle and axis condition, and confirm the machine class still fits your part family. Hidden recovery work—undocumented wiring, worn feedback systems, lubrication neglect—routinely breaks budgets, and downtime during installation is part of the purchase price. Separate modernization scope from rebuild scope in every quote, run cutting trials first, and ask whether the plant would still want this machine if it worked perfectly tomorrow.
Start With Triage, Not Modernization
Retrofitting an older CNC machine is an attractive proposition on paper. It promises modern usability, better diagnostics, and easier programming without the capital outlay of a full replacement. Sometimes that logic is exactly right. Sometimes it becomes a slow rescue attempt that uncovers worn motion components, unsafe electrical work, weak documentation, spare-parts risk, and more downtime than the original budget ever admitted.
That is why retrofit should be treated as a triage decision before it is treated as a modernization project. The first question is not what new control to install. The first question is whether the machine still deserves a future at all.
Factories make better retrofit decisions when they separate three different problems that often get mixed together: an old machine that is structurally sound but electronically obsolete, an old machine that is mechanically worn and being disguised as a control problem, and an old machine that may be recoverable but no longer fits the production direction of the plant. Those are not the same capital decision, even though they can all arrive under the word retrofit.
The Iron Matters More Than The Interface
The first serious retrofit question is whether the mechanical platform still deserves trust. That means more than asking whether the casting is heavy or whether the machine once had a good reputation. It means checking whether the structure, axes, spindle system, lubrication path, and core motion behavior are still recoverable enough to support repeatable work.
Useful questions include:
- Does the machine still hold usable geometry across the full travel range?
- Are axis components worn but recoverable, or fundamentally unstable?
- Is spindle condition consistent with the type of work the shop still needs to run?
- Does backlash, vibration, heat growth, or drift already consume too much correction effort?
- Is the mechanical platform still stronger than the practical alternatives the plant could buy today?
If the answers are weak, new controls may simply make the machine easier to troubleshoot while leaving the production result fundamentally unchanged. That is not a real retrofit success.
Consider a typical scenario in a cabinet shop running a ten-year-old nested-based machining center. The control is obsolete, the touchscreen is failing, and the operator has to hand-code offsets that the original software used to manage automatically. The retrofit pitch sounds compelling. But if the linear guides on the gantry have measurable play, the vacuum pods no longer seal consistently, and the spindle bearings are noisy at operating speed, a new control will not restore the edge quality the shop needs. The machine will still produce parts that require secondary sanding or scrapping. The retrofit simply makes the failure more visible on a modern screen.
Separate Electronic Obsolescence From Mechanical Decline
Retrofit usually makes the strongest sense when obsolescence is genuinely the primary bottleneck. Common examples include unsupported controls, poor communication with current programming workflows, unreliable electronics, limited diagnostics, or spare-parts risk in the control layer. In those cases, the factory may already have a mechanically worthwhile platform that is being held back by an outdated electronic environment.
Retrofit is much weaker when the real pain comes from worn mechanics, unstable cutting behavior, poor repeatability, or a machine type that no longer fits the plant’s part family. In those cases, the control cabinet becomes a convenient villain because it is visible, even though the deeper problem lives in the machine itself.
That distinction is critical. Buyers should ask whether they are fixing a dead support ecosystem or trying to hide accumulated wear behind a modern screen. Those two projects are financially and operationally very different.
A practical way to test this is to run a controlled cutting trial before committing to any retrofit scope. Cut a representative part at the speeds and feeds the shop actually uses. Measure the result. Then ask an independent maintenance engineer or a retrofit vendor with mechanical inspection capability to evaluate the machine’s condition. If the cutting trial shows poor finish, dimensional drift, or chatter that cannot be explained by tooling alone, the mechanical system needs attention regardless of what happens to the control.
Hidden Recovery Work Is What Usually Breaks The Budget
A retrofit proposal often looks manageable when it is described as control replacement, drive refresh, and software modernization. The budget usually gets damaged when the project uncovers everything the machine has been quietly asking for over the last several years.
Undocumented wiring. Marginal motors. Aging feedback systems. Lubrication neglect. Guarding that no longer satisfies current expectations. Electrical cabinets that were modified without discipline. Mechanical wear that was tolerable only because the machine was being nursed along by experienced operators.
That is why retrofit budgets fail less because the planned scope was expensive and more because the real scope was never admitted early enough. Factories should expect the project to reveal the machine’s hidden debt. The question is whether that debt is small enough to absorb or large enough to force a different answer.
Take the electrical cabinet as an example. A machine that has been in service for fifteen years has likely accumulated modifications. Someone added a relay for a dust-collection interlock. Someone else replaced a drive and left the old wiring in place. A third person added a remote start station without updating the schematic. None of these changes were documented. When the retrofit vendor opens the cabinet, they find a wiring tangle that takes two days to map before any new hardware can be installed. That labor was not in the original quote. It is hidden recovery work, and it is the norm rather than the exception on older machines.
Downtime Is Part Of The Purchase Price
Retrofit is never just a hardware purchase. It is a live intervention inside a working factory. That means teardown, documentation review, installation, tuning, proof-out, operator adaptation, and the possibility that the machine will not return to productive work as quickly as the optimistic schedule assumed.
So the right question is not only whether the plant can afford the retrofit. It is whether the plant can survive the project without creating a more expensive production gap than the savings justify.
This is where many apparently sensible retrofits weaken. The shop may be able to pay for the work, but not to absorb the lost machine time, engineering attention, or maintenance focus required to finish the project properly. If internal bandwidth is already thin, retrofit becomes harder to govern, and the business case degrades fast.
A furniture manufacturer running two shifts on a panel saw and a nested-based machining center has limited flexibility. If the machining center is down for three weeks for retrofit, the shop must either outsource that work, run the panel saw and edgebander at reduced throughput, or delay customer orders. Each of those options carries a real cost. The retrofit quote might show a favorable payback period, but that payback calculation rarely includes the cost of the production gap. When it does, many retrofit projects stop making sense.
Supportability And Safety Usually Matter More After Retrofit Than Before
Some retrofits pay back well because they do more than update the operator interface. They reduce spare-parts anxiety, improve diagnostics, simplify program movement, and make the machine easier to support in the real production environment. That value is real and often underestimated.
But older machines also carry safety and compliance questions that a cosmetic modernization will not solve. Guarding, interlocks, electrical practice, emergency-stop logic, and operator expectations often need as much attention as the control itself. If a retrofit modernizes the screen but leaves the machine awkward to maintain or weak in safety performance, the project has not fully solved the problem.
That is why supportability and safety should be treated as part of the same decision. A machine that becomes easier to run but still risky to support is only partially recovered.
Consider the emergency-stop circuit on a twenty-year-old machine. The original design may have used a single-channel e-stop with a simple relay chain. Current safety standards expect dual-channel monitoring, positive-guided relays, and a documented risk assessment. A retrofit that replaces the control but leaves the original e-stop logic in place creates a machine that is easier to program but no safer to operate. In some jurisdictions, that also creates liability exposure if an incident occurs. The retrofit scope should include a safety review of the entire machine, not just the control cabinet.
Ask Whether The Plant Would Still Want This Machine If It Worked Perfectly Tomorrow
This is the strategic test that often cuts through emotion. Assume the retrofit succeeds. The machine becomes dependable, easier to program, easier to troubleshoot, and less exposed to parts scarcity. Would the factory still choose that machine class for the next several years of work?
If the honest answer is no, then retrofit may be solving the wrong problem. The plant may be preserving a machine architecture that no longer matches its part sizes, cycle expectations, labor model, or broader production direction. In that case, a successful retrofit can still be the wrong investment because it locks capital into yesterday’s production concept.
This question is useful because it separates technical recoverability from strategic fit. Both matter. A machine can be recoverable and still be the wrong future asset.
A stone fabrication shop might have an older bridge saw that is mechanically sound and electronically obsolete. The control can be replaced, and the saw will cut granite and quartzite accurately again. But if the shop is moving toward more complex edge profiles, waterjet integration, or automated nesting of countertop blanks, the bridge saw may no longer fit the production direction. The retrofit would preserve a machine that cannot support the shop’s next stage of growth. In that case, the capital is better directed toward a machine that matches the future workflow.
Good Retrofit Cases Usually Share The Same Pattern
Retrofit often makes sense when several conditions line up at once. The machine base is still mechanically credible. The main pain is electronic obsolescence rather than mechanical collapse. The machine class still fits the workload. Replacement would be expensive relative to the value still present in the platform. And the factory can manage the project without destabilizing the rest of production.
In those conditions, retrofit is not an act of nostalgia. It is a disciplined way of unlocking value that already exists in the iron.
These are often the strongest retrofit cases:
- The structure and motion system are still fundamentally sound.
- The current control is unsupported, unreliable, or operationally limiting.
- The machine still matches the plant’s part family and production role.
- The business can tolerate the project window.
- The retrofit partner can define scope clearly enough to keep hidden work visible.
When those conditions are present, retrofit can be commercially rational and operationally clean.
A woodworking shop running a ten-year-old CNC router for cabinet parts is a typical good candidate. The machine cuts consistently, holds tolerance within the shop’s requirements, and has a solid steel frame that has not shown signs of fatigue. The control, however, is no longer supported by the original manufacturer, and the shop cannot get replacement boards without paying premium prices on the secondary market. The retrofit replaces the control, updates the drives, and brings the machine into the shop’s current programming environment. The machine returns to service with better diagnostics and a clear support path. That is a defensible retrofit.
Weak Retrofit Cases Usually Start As Modernization And End As Partial Rebuilds
The weak cases have a different pattern. The project is introduced as a control refresh, then expands into motors, feedback devices, spindle work, geometry correction, cabinet cleanup, lubrication recovery, guarding changes, and a long list of miscellaneous mechanical discoveries. At that point the factory is no longer modernizing a sound platform. It is funding a partial rebuild inside a project that was not budgeted or governed as one.
This is why scope discipline is so important. Buyers should force the proposal to separate control modernization from recovery work. That means explicit visibility into:
- Control and HMI replacement.
- Drive and motor scope.
- Feedback and encoder replacement.
- Mechanical refurbishment.
- Electrical cabinet cleanup and rewiring.
- Safety and guarding upgrades.
- Commissioning, proof-out, and training.
If these layers are blurred together, decision quality drops immediately because the buyer no longer knows whether the project is saving a machine or quietly rebuilding one.
A typical weak case starts with a quote for a new control and HMI on a ten-year-old machining center. The vendor then discovers that two axis drives are marginal and recommends replacing them. Then the spindle encoder shows intermittent faults, so that gets added. Then the lubrication pump fails during commissioning, and the machine needs a new one. Then the operator reports that the machine still does not cut square, and a geometry check reveals that the gantry needs realignment. Each addition is individually reasonable. Collectively, the project has become a partial rebuild with a budget that is now close to half the cost of a new machine. The factory never made a deliberate decision to fund a rebuild. It drifted into one.
Compare Retrofit And Replacement As Future Production Systems
The most common retrofit mistake is comparing retrofit cost to replacement sticker price and stopping there. That comparison is too shallow. The factory should compare two future systems: an older platform that will be partially renewed and a new platform selected for the next stage of production.
That means evaluating more than capital outlay. It means asking which path gives the plant a more stable support future, lower technical uncertainty, cleaner startup path, better fit for coming work, and stronger long-term integration with the rest of the shop.
Retrofit may still win that comparison. But it should win by surviving the future-system test, not by looking cheaper in the first line of a spreadsheet.
Consider a panel processing line. The shop has an older edgebander that is mechanically sound but has a control that cannot communicate with the new production management software. The retrofit cost is a fraction of a new edgebander. But the new edgebander would bring features like automatic glue color change, faster changeover between edge materials, and integrated quality monitoring. If the shop’s order mix is shifting toward smaller batches with more edge changes, the new machine may pay for itself in reduced setup time alone. The retrofit would preserve a machine that cannot handle the future order mix efficiently.
Quote Review Should Expose Recovery Scope, Not Hide It
Retrofit quotations vary widely because each vendor chooses a different project boundary. One proposal may look expensive because it includes real inspection, clearer risk treatment, and a more responsible proof-out scope. Another may look cheap because it assumes away unknowns or quietly leaves more recovery responsibility with the buyer.
That is why retrofit offers should be reviewed with the same discipline as new-machine purchases. It helps to compare machinery quotes line by line so modernization scope, recovery scope, startup assumptions, and support boundaries become visible. If the retrofit partner is remote or factory-direct, the usual factory-direct verification steps matter here as well, because post-project support is often where the real risk sits.
When retrofit no longer survives that review, the better question becomes what replacement would buy in production terms rather than how much cash can be deferred. That is where what makes industrial CNC equipment worth the investment becomes the stronger framing. If the plant is widening the discussion beyond one rescue project, the Pandaxis shop can still serve as a general machinery reference point.
A practical quote-review checklist includes:
- Does the quote include a documented machine inspection before the retrofit scope is finalized?
- Are the control, drive, motor, feedback, and mechanical scopes listed as separate line items?
- Does the quote state what happens if the vendor discovers additional mechanical wear during commissioning?
- Is the proof-out procedure defined, including test parts, tolerances, and acceptance criteria?
- Is training included for operators and maintenance staff, or is it an extra?
- What is the support commitment after the retrofit is complete, and who provides it?
If the quote cannot answer these questions clearly, the buyer is taking on risk that should be priced and managed explicitly.
The Best Retrofit Decision Usually Sounds Less Exciting Than The Pitch
Good retrofit decisions are usually sober. They are based on surviving diagnosis, not on affection for a familiar machine. They assume hidden work will appear. They respect downtime as part of the cost. They separate electronic obsolescence from mechanical decline. And they ask, without sentiment, whether the machine still deserves a place in the factory’s future.
That is why the strongest retrofit choices are rarely romantic. If the iron is still good, the support problem is real, and the production role still matters, retrofit can be a smart extension of asset life. If not, replacement is often the cleaner and more honest investment.
The factories that make the best retrofit decisions share a few habits. They keep maintenance records that are detailed enough to show whether the machine has been cared for or neglected. They run cutting trials before committing to a retrofit scope. They force vendors to separate modernization from recovery work in the quote. They calculate the cost of downtime as part of the project budget. And they are willing to walk away from a retrofit when the numbers do not survive scrutiny.
Retrofit is not a shortcut. It is a judgment call that requires the same discipline as any other capital investment. When the machine is worth saving, retrofit delivers real value. When it is not, the most expensive mistake is pretending otherwise.