Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
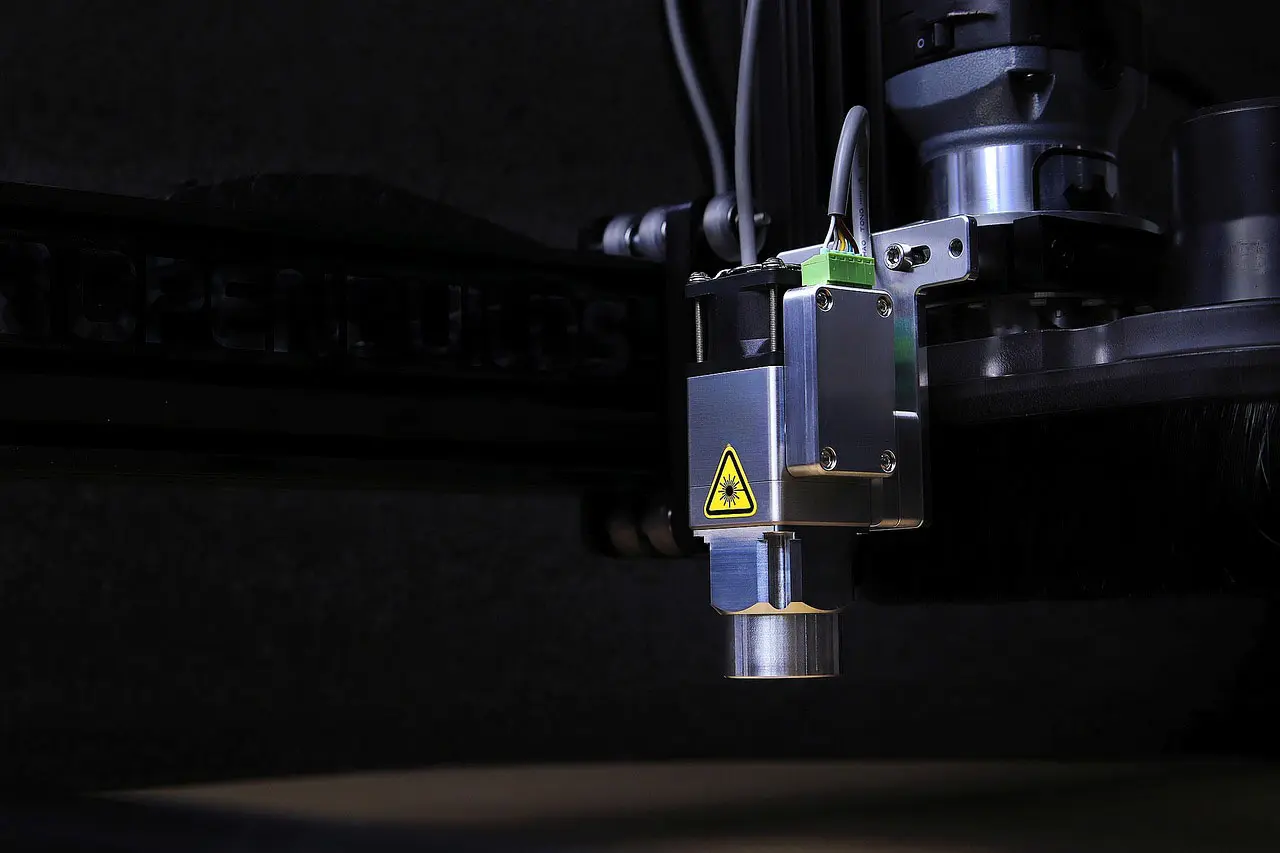
Laser cutting is often treated as a single process, but on the shop floor, it behaves like several different machines depending on what you feed it. A system that produces clean, flame-polished edges on acrylic signage can scorch wood veneers and struggle with the thermal demands of sheet metal. Conversely, a machine configured for high-throughput metal fabrication lacks the finesse required for detailed engraving on decorative panels.
For production managers and engineers, the practical question is not whether laser cutting works, but where it delivers a measurable return. The answer hinges on material-specific process fit: how the substrate reacts to heat, what edge quality the application demands, and whether the workflow requires cutting, engraving, or both. Getting this wrong leads to rework, scrapped parts, and bottlenecks. Getting it right means matching the machine direction to the material’s physical behavior.
Why Material Response Dictates Machine Choice
Laser cutting removes material through focused thermal energy, but the way different substrates absorb and dissipate that energy varies dramatically. This is not a minor variable; it determines the entire viability of the process for a given part.
Before evaluating specific machines, assess your application against these criteria:
- Material response to laser energy: Does the substrate vaporize cleanly, or does it char, melt, or reflect the beam?
- Required edge quality: Is the cut edge visible in the final product, or is it hidden in an assembly?
- Throughput targets: Are you cutting a few dozen parts per day or several thousand?
- Surface appearance requirements: Does the part need a pristine face, or is minor discoloration acceptable?
- Process scope: Do you need cutting only, engraving only, or a combination in a single pass?
- Risk tolerance: How much burning, melting, or surface damage can you afford before the part is rejected?
When these factors are defined upfront, the selection process becomes a matter of matching known machine capabilities to specific production outcomes rather than guessing.
Application Overview by Material
The table below summarizes the primary application logic for the four most common laser-processed material groups. Use it as a starting point for internal discussions, not as a definitive specification sheet.
| Material | Typical Application | Primary Buyer Objective | Main Process Risk |
|---|---|---|---|
| Wood | Decorative panels, furniture details, engraved branding, templates | Clean detail, repeatable contours, visual consistency | Burn marks, edge darkening, inconsistent finish across wood species |
| Acrylic | Sign letters, display panels, retail fixtures, point-of-sale components | Smooth, polished edges, precise shapes, fast changeover | Edge cracking, surface scratching, balance between speed and clarity |
| Metal | Fabricated brackets, enclosures, sheet components, structural parts | High-speed throughput, cut consistency, low cost per part | Material thickness limits, cut stability, overall process economics |
| Plastic | Shaped non-structural components, thin covers, labels, custom cutouts | Controlled shaping, dimensional accuracy, reduced manual trimming | Melting, edge deformation, fume generation, material-specific sensitivity |
Wood Processing: Detail and Repeatability Without Tool Contact
Wood remains one of the most practical materials for laser cutting and engraving, particularly when the application prioritizes intricate geometry and visual quality over raw cutting speed. Because the laser beam does not physically contact the workpiece, there is no tool wear to account for and no mechanical force to distort thin sections.
Common wood applications include:
- Decorative panels for cabinetry and furniture
- Engraved branding or surface graphics on finished goods
- Templates and pattern parts for jigs and fixtures
- Small-batch custom shapes that would require expensive dies or CNC tooling setups
- Furniture detail components where edge finish is visible
The operational advantage of laser processing on wood is the ability to switch between cutting and engraving in the same work cell without changing tools. This is particularly valuable in shops that handle frequent design revisions or produce a high mix of low-volume parts.
Where Laser Cutting Improves Wood Workflows
In a typical woodworking environment, laser cutting reduces reliance on manual trimming and secondary finishing operations. The process delivers consistent detail across batches, which is difficult to achieve with hand-guided routing or sawing on intricate patterns. Job changes are fast because the only setup required is loading the digital file and adjusting focus.
However, wood is not a uniform material. The same laser settings that produce a clean cut on Baltic birch plywood can cause excessive charring on a dense hardwood or leave burn marks on veneered MDF. Glue content in engineered panels also affects cut quality, as adhesives can vaporize unpredictably and leave residue on the cut edge.
Buyers evaluating laser systems for wood should pay close attention to:
- Edge darkening: Visible on light woods and often unacceptable for exposed edges
- Surface burn marks: Caused by reflected beam energy or incorrect focus
- Variation by wood type: Density and resin content change the required power and speed
- Finish expectations: A cut that is acceptable for a hidden joint may fail on a visible surface
The goal is not simply whether the machine can cut wood, but whether it can do so at the finish quality your product requires without excessive rework.
For shops focused on wood, acrylic, and other non-metal substrates, the most direct equipment fit is a dedicated laser cutter and engraver configured for these materials.
Acrylic Processing: Edge Quality Drives the Application
Acrylic is arguably the most commercially important laser-cut material outside of metal fabrication. Its use in signage, displays, and retail fixtures is widespread because the laser produces a flame-polished edge that requires no secondary finishing. This is a significant advantage over CNC routing, which leaves a frosted edge that must be manually polished or flame-treated.
Typical acrylic applications include:
- Sign letters and logos
- Display panels and shelf talkers
- Branded fixtures for retail environments
- Decorative inserts for architectural features
- Point-of-sale components
- Transparent or colored shape parts
The production value of laser cutting on acrylic lies in the ability to move from design file to finished part without hard tooling. In mixed-design production environments, where many part styles are cut from the same sheet stock, this flexibility translates directly into shorter lead times and lower setup costs.
Where Laser Cutting Helps in Acrylic Workflows
Laser processing on acrylic improves shape accuracy and edge appearance simultaneously. The process is repeatable across small and medium batches, which makes it suitable for shops that produce a wide variety of display components rather than long runs of identical parts.
The main concerns in acrylic cutting are:
- Edge finish quality: The flame-polished effect is desirable, but achieving it consistently requires precise power and speed settings
- Surface protection: The protective film on acrylic sheets can melt and adhere to the edge if settings are too aggressive
- Cracking risk: Poor process control, particularly excessive power, can cause micro-cracks along the cut line
- Speed versus visual outcome: Pushing the machine too fast reduces edge clarity and increases the risk of surface damage
For sign and display producers, appearance is often as important as cutting speed. A part that cuts 20 percent faster but requires manual edge finishing is not actually faster in total production time.
Metal Processing: A Separate Selection Path
Metal laser cutting is a major industrial process, but it operates under fundamentally different physics than non-metal processing. Reflective materials, thermal conductivity, and material thickness all require significantly higher power levels and different beam delivery systems.
Common metal applications include:
- Fabricated parts for machinery and equipment
- Brackets, enclosures, and mounting plates
- Sheet-based components for structural assemblies
- Repetitive industrial shapes produced in volume
In metal-focused environments, laser cutting is valued for high-speed, digitally controlled part production with strong repeatability. The buying logic centers on throughput, cut consistency, and how the machine integrates with downstream bending, welding, and assembly operations.
Where Laser Cutting Helps in Metal Workflows
The industrial logic for metal laser cutting includes:
- Supporting flexible part geometry without dedicated tooling
- Reducing dependency on hard tooling for short-run production
- Improving repeatability on programmed parts across multiple shifts
- Simplifying changeovers between product variants
However, metal applications are more sensitive to process fit than wood or acrylic. Buyers must evaluate material type, thickness range, edge quality expectations, and total operating economics. A machine that cuts 1 mm mild steel efficiently may be entirely unsuitable for 10 mm plate or highly reflective aluminum.
It is important to note that the current verified product language for Pandaxis laser equipment is centered on non-metal applications. Metal processing should be treated as broader industrial selection context rather than a direct category claim.
Plastic Processing: Selective and Material-Sensitive
Plastic is a useful but more selective laser category because different plastics respond very differently to heat. Some materials vaporize cleanly, while others melt, deform, or release hazardous fumes.
Common plastic-related applications include:
- Shaped non-structural components
- Thin panels or covers
- Labels and decorative parts
- Light-duty precision cutouts
- Custom small-run production
Laser processing is attractive for plastics when buyers need digital flexibility, repeatable geometry, and reduced manual trimming. However, the process requires more caution than wood or acrylic because the margin for error is narrower.
Where Laser Cutting Helps in Plastic Workflows
In the right applications, laser cutters support better geometric consistency, faster part changeovers, and cleaner small-part processing than manual methods. The process is efficient for short-run custom work where the cost of injection molding tooling cannot be justified.
Plastic applications should be evaluated carefully for:
- Heat sensitivity: Some plastics soften and deform well below their vaporization point
- Melt behavior: Materials like polypropylene tend to melt and recast rather than vaporize cleanly
- Edge deformation: Warping or beading along the cut line is common with certain polymers
- Fume management: Many plastics release toxic or unpleasant fumes that require adequate extraction
- Surface appearance standards: Visible discoloration or roughness may be unacceptable for consumer-facing parts
Not every plastic is equally suitable for laser processing. Buyers should approach plastic work with material-specific caution and test samples before committing to a machine configuration.
Matching Applications to Production Goals
It is often more useful to classify laser cutter applications by production objective rather than by material alone. This approach clarifies which machine direction is appropriate for your specific workflow.
If the Goal Is Decorative Precision
Laser cutting is strongest on wood, acrylic, and selected plastics when the priority is detailed contours and visually controlled part shapes. These applications benefit from the process’s ability to produce intricate geometry without mechanical tool contact.
If the Goal Is High-Volume Fabrication
Laser cutting is evaluated in terms of throughput, repeatability, and material-specific process economics. This is where metal applications are typically assessed, and where the machine must integrate with a broader fabrication workflow.
If the Goal Is Flexible Mixed-Job Production
Laser cutters are especially useful where designs change frequently, tooling changes need to be minimized, and small batches must be produced efficiently. This is why laser systems often fit sign shops, custom product makers, display fabricators, and decorative panel producers.
The table below connects production needs to the appropriate application direction:
| Production Need | Best-Fit Material/Application Direction | Why It Fits |
|---|---|---|
| Decorative wood panels or engraved components | Wood cutting and engraving | Strong fit for detail work and repeatable visual output |
| Signage, letters, and display fabrication | Acrylic processing | Strong fit for contour flexibility and display-part production |
| Industrial sheet-based part production | Metal-focused laser selection | Better aligned with fabrication throughput and repeatability |
| Light-duty custom shaped components | Selected plastic processing | Useful when material behavior is compatible and part geometry changes often |
Making the Buying Decision
The most practical way to evaluate laser applications is to connect the material to the production outcome. Start by identifying the primary material you process, the required finish quality, the job volume, and whether the workflow needs cutting only or cutting plus engraving.
For wood and acrylic, laser cutters are often the right choice for clean detail, decorative flexibility, and efficient custom production. For metal, laser applications should be evaluated through broader fabrication logic, with attention to power requirements and material thickness. For plastic, success depends entirely on the exact material and its heat response.
Buyers who compare laser applications this way are far more likely to choose the right machine direction for real production. If you are still evaluating how laser machinery fits into a larger production plan, the Pandaxis product catalog provides a useful view of how these systems sit alongside other equipment options.
FAQ
What Materials Are Most Commonly Processed With Laser Cutters?
Wood, acrylic, metal, and selected plastics are all common laser-cut materials, but each one requires a different application and machine-selection logic. Wood and acrylic are the most accessible for non-metal laser systems, while metal requires a separate, higher-power machine direction.
Is Laser Cutting Better for Wood or Acrylic?
Both can be strong applications. The better fit depends on whether the priority is decorative detail, edge quality, signage production, furniture components, or mixed cutting-and-engraving work. Acrylic offers the advantage of flame-polished edges, while wood offers greater variety in visual texture and finish.
Can One Laser Cutter Handle Wood, Acrylic, Metal, and Plastic Equally Well?
Not usually. Different materials are better matched to different laser machine directions and process conditions. A machine optimized for non-metal cutting typically lacks the power and beam delivery required for efficient metal processing.
Why Is Plastic More Caution-Sensitive in Laser Processing?
Because plastic materials vary widely in melt behavior, edge quality, and fume characteristics. Material-specific evaluation is important before choosing laser processing, and some plastics should be avoided entirely due to hazardous emissions or poor cut quality.
How Should Buyers Compare Material Applications Before Buying?
Start by identifying the main material, required finish quality, job volume, and whether the workflow needs cutting only or cutting plus engraving. Then compare machine direction based on those needs, and request sample cuts on your actual materials before making a purchase decision.