Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
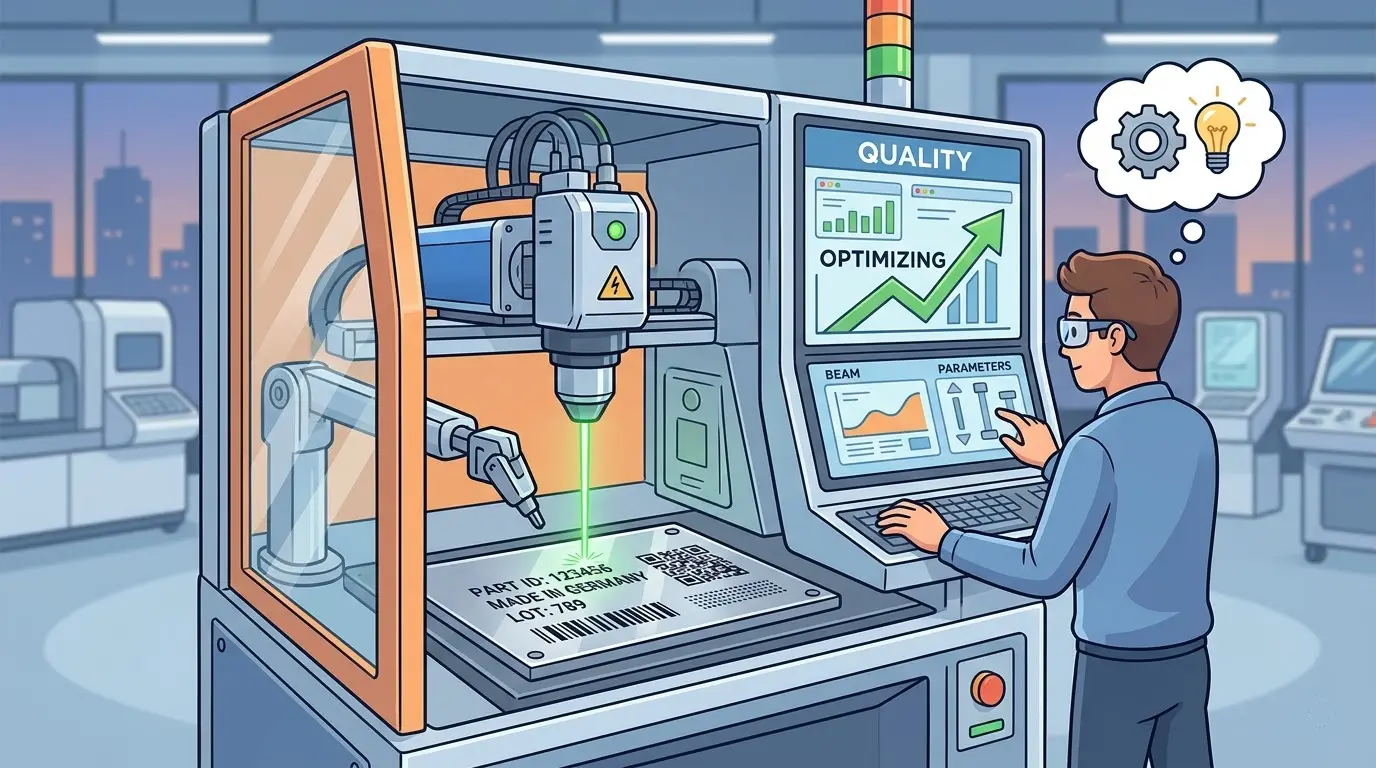
Metal marking failures rarely appear during the sample phase; they surface when oil residue, mixed finishes, and rising line speeds erode contrast and edge definition on real parts. Treating mark quality as cosmetic invites scanner rejections, batch holds, and costly rework that ripple beyond the marked component. This article walks production teams through the actual drivers of stable marks—surface condition, focus stability, energy density, fixturing, and heat accumulation—and explains why separating recipes by material and end-use requirement matters more than chasing a darker sample. Process discipline, not machine shopping, delivers repeatable results.
Why Metal Marks Fail in Production
Metal marking problems usually start the same way: the sample looks perfect, but the production run does not. A logo that appears crisp on a flat test coupon loses contrast on real parts covered with oil residue or mixed finishes. A data matrix code that reads cleanly at the bench starts failing once the line speeds up and parts warm up.
Treating mark quality as a cosmetic detail is a mistake. On an active line, it directly affects traceability, scanner reliability, part identification, inspection speed, and the amount of manual rework your team absorbs. The goal is not simply to make the mark darker. The goal is to make it stable, readable, and repeatable under actual production conditions.
When a mark fails mid-run, the cost is rarely limited to the marked part itself. The part may need to be scrapped, reworked, or routed through a secondary operation. If the mark is a serial number or a data matrix code tied to a quality record, a failed mark can hold up an entire batch pending reinspection. In high-mix shops, the problem compounds because each new material or finish introduces a new set of variables. Understanding why marks fail is the first step toward building a process that does not depend on luck.
Defining Mark Quality Beyond Visual Preference
Many shops describe a good mark as one that looks dark and clean. That definition is too narrow. In production, mark quality combines several requirements simultaneously, and each one can fail independently.
| Quality Factor | What It Means on the Line | What Usually Hurts It |
|---|---|---|
| Contrast | Operators and scanners can identify the mark quickly | Reflective surfaces, weak energy density, unstable focus, inconsistent finish |
| Edge Definition | Text, logos, and codes stay crisp instead of fuzzy | Excess heat, poor overlap settings, vibration, dirty optics |
| Repeatability | The mark looks consistent from part to part and lot to lot | Surface variation, unstable fixturing, drifting setup, poor recipe separation |
| Surface Control | The mark is functional without creating unwanted cosmetic damage | Too much heat input, wrong pulse behavior, slow scan speed, excessive dwell |
| Durability | The mark stays useful after cleaning, handling, or later processing | Marking too lightly, placing the mark too early in the workflow, testing only on ideal samples |
The best-looking sample is not always the best production result. A darker mark can come with rougher edges. A deeper mark can reduce speed or create unwanted surface change. A lighter mark can look elegant on stainless steel but become harder to read after cleaning or handling. The right answer depends on how the part is used and what the mark must survive.
Consider a stainless steel component that will be handled with bare hands throughout assembly. A light etch may look acceptable immediately after marking, but skin oils and minor abrasion can reduce contrast within hours. The same mark on a part that is coated or painted immediately after marking may be completely hidden. Defining the full lifecycle of the part before tuning the process prevents wasted effort and repeated requalification cycles.
Clarify the Mark Style Your Workflow Actually Needs
Buyers often use the word etching as a catch-all term, but shops are not always asking for the same physical result. In some workflows, the requirement is a shallow visible mark for branding or part ID. In others, the requirement is a darker annealed look on stainless steel. In others, the mark needs to survive abrasion, coating, or repeated handling.
| Mark Style | Where It Commonly Fits Best | Main Benefit | Main Tradeoff |
|---|---|---|---|
| Light Surface Etch | Serial numbers, logos, general identification | Good balance of readability and speed | May not hold up if downstream processing is aggressive |
| Dark Surface Mark | Stainless parts where visual contrast matters | Strong cosmetic readability on suitable finishes | Process window can narrow quickly on mixed surface conditions |
| Deeper Engraved Mark | Tooling IDs, harsh-service parts, marks facing wear | Better durability when surface abuse is expected | Slower cycle time and more visible surface disruption |
If the workflow is not clear, process tuning turns into guesswork. The machine team may chase more contrast when the real issue is durability. Or they may increase depth when the actual requirement is clean cosmetic readability with limited heat effect.
Take a common example from job-shop production. A fabricator runs the same stainless bracket for two customers. One customer uses the mark for internal traceability only; the part is painted within a day and the mark never needs to be read again. The other customer ships the bracket bare, and the mark must remain legible after months of storage and handling. Running both jobs with the same recipe forces a compromise. The traceability-only job may be over-marked, slowing cycle time and adding unnecessary heat. The bare-shipped job may be under-marked, risking field failures. Separating recipes by end-use requirement is not administrative overhead; it is the difference between a process that works and one that only works sometimes.
The Real Drivers of Mark Quality
For metal applications, mark quality is shaped more by a handful of process variables than by headline machine claims. Across the broader industrial market, metal etching and marking are often associated with fiber-based systems because of their compatibility with many metal surfaces. But even within that general machine class, process stability matters more than broad labels.
The variables that usually change results the most are:
- Surface Condition: Oil, oxidation, blasting texture, plating variation, brushed grain, and coating residue all change how the metal responds to the beam.
- Focus Stability: If part height shifts slightly from one nest position to another, edge sharpness and contrast often move with it.
- Energy Density: The real result comes from the balance between power, speed, pulse behavior, line spacing, and overlap, not from one setting alone.
- Heat Accumulation: When parts run continuously, the later pieces in the batch may mark differently if heat builds in the workpiece or fixture.
- Workholding and Presentation: Weak fixturing creates inconsistent focal distance, variable angle, and small motion errors that show up in fine text and codes.
- Optics Condition: Dirty lenses or protective windows can gradually reduce clarity long before the operator notices a major fault.
- Mark Geometry: Tiny characters, dense data matrix codes, and thin-line logos often fail because the design is too ambitious for the available process window.
That last point is often overlooked. A weak code is not always the machine’s fault. Sometimes the cell size is too small, the line weight is too thin, or the mark area sits on a surface finish that works against readability from the start.
Energy density deserves special attention because it is the variable most often misunderstood. Operators frequently assume that more power equals a better mark. In practice, the interaction between power and scan speed determines how much energy is deposited per unit area. Crank the power up without adjusting speed, and you may create a mark that is darker but also rougher, wider, and slower to produce. Reduce speed to compensate, and you add heat that can distort thin material or change the surface color in unwanted ways. The process window for a good mark is often narrower than operators expect, and finding it requires systematic testing rather than intuition.
Surface Preparation and Fixturing Deliver the Fastest Gains
When factories try to improve mark quality, they often go straight to parameter tuning. That makes sense, but it is not always the highest-return first step. In many lines, the fastest improvement comes from stabilizing the part before the beam touches it.
The most practical corrections often include:
- Standardize how parts arrive at the marking station.
- Remove excess oil, coolant, or surface contamination before qualification testing.
- Tighten fixture control so part height and orientation stay consistent.
- Separate recipes by material family and surface finish instead of using one universal program.
- Recheck optics cleanliness as part of routine line control.
These steps sound basic because they are basic. But they directly improve contrast, edge definition, and consistency. A better recipe cannot fully compensate for unstable part presentation.
Consider a line that marks machined aluminum housings. The parts arrive from a CNC cell with residual coolant and fine chips. If the marking station sits directly after machining, the surface condition varies from part to part depending on how long the part drained and whether the operator wiped it down. One operator may blow the part off with air; another may not. The result is a mark that looks acceptable on some parts and washed out on others. Adding a simple standardized wipe-down step before marking, or repositioning the station after a degreasing operation, often eliminates more variation than any parameter change could.
Fixturing is equally important. A part that sits on a flat nest with consistent locating pins will mark differently from a part that is hand-placed on a worn fixture with several degrees of freedom. Even a small height difference of a fraction of a millimeter can shift the focal point enough to soften fine features. Shops that invest in dedicated nests for high-volume parts typically see immediate improvements in repeatability, because the beam-to-surface distance stops changing from part to part.
Common Mark Defects and Their Root Causes
Line symptoms are often more useful than generic advice because they connect the visual problem to a likely root cause.
| Production Symptom | What It Often Indicates | Practical Response |
|---|---|---|
| The mark looks too light on polished parts | Reflectivity is narrowing the process window, or the surface finish differs from the approved sample | Qualify on real production finishes and separate polished parts into their own recipe group |
| The mark has blurry edges or a slight halo | Focus is drifting, heat input is too broad, or the optics need attention | Recheck focal stability, clean optics, and review speed-overlap balance |
| Some parts mark well but others in the same batch do not | Material or finish variation is wider than expected, or fixturing is inconsistent | Group parts by real surface condition and verify nest-to-nest stability |
| Scanner rejection is high even though the mark looks fine by eye | Code geometry is too dense, edge definition is weak, or lighting assumptions do not match the real line | Increase code size where possible and validate with the actual production scanner |
| The mark is durable but looks too harsh | The process is tuned too heavily toward depth rather than surface appearance | Rebalance the recipe around the cosmetic target or separate visible-part jobs from heavy-duty ID jobs |
| Contrast drops during longer runs | Heat buildup, dirty optics, or drifting setup is changing the process window over time | Add mid-run checks for temperature, optics condition, and first-part versus later-part comparison |
When teams read these symptoms correctly, they stop treating every problem as a machine-shopping problem. In many cases, the existing machine can deliver acceptable results once the part flow, fixture control, and recipe logic become more disciplined.
Scanner rejection deserves particular attention because it is the failure mode that costs the most money. A mark that looks acceptable to the human eye may still fail a vision system if the contrast ratio is marginal, the edge definition is soft, or the code geometry is distorted. The gap between visual acceptance and scanner acceptance is a common source of frustration. The fix is not always to make the mark darker; it is often to make the mark cleaner, with sharper transitions between marked and unmarked areas. This requires attention to focus, overlap, and pulse behavior rather than raw power.
When the Machine Configuration Is the Limitation
Not every mark-quality issue can be solved by better housekeeping. Sometimes the process window is too narrow because the machine configuration does not match the application.
That is more likely when:
- The workflow requires several different mark styles on different metals.
- Cosmetic stainless marks matter as much as utility traceability codes.
- Very fine graphics or dense codes need strong edge control at production speed.
- Mixed reflective and non-reflective surfaces run through the same cell.
- Heat-sensitive parts need good readability without excess surface effect.
In those situations, buyers should look beyond the generic phrase “metal etching machine” and evaluate whether the source type, pulse-control range, motion stability, and part-handling setup actually fit the process. A line that only runs simple utility marking may not need the same flexibility as a line that handles cosmetic branding, scanner-critical codes, and varying metal finishes in the same week.
For example, a shop that marks hardened steel tooling needs a process that can produce a durable, readable mark without annealing the surface or altering the hardness in the marked zone. A shop that marks decorative stainless panels needs a process that produces consistent color and contrast across large areas without visible banding or heat discoloration. These are different applications with different process requirements, and a single machine configuration may not serve both well.
Pulse control is one of the most important differentiators. A machine with a wide pulse-width range can be tuned for both fine surface etching and deeper engraving. A machine with limited pulse control may be forced into a narrow operating band that works for one application but not another. Buyers should ask how the machine behaves at the extremes of its range, not just at the settings that produced the best demo sample.
Build a Qualification Routine That Mirrors Real Production
The strongest improvement plans usually come from a more disciplined qualification routine rather than a single dramatic settings change. Before locking in a recipe or replacing equipment, validate the full process in a way that reflects the real job.
Use a routine like this:
- Test on actual production parts, not ideal sample coupons.
- Separate trials by material, finish, and any coating condition that affects response.
- Compare first-part results and mid-run results to catch heat or drift effects.
- Check marks after cleaning, handling, or any downstream step that could reduce readability.
- Verify with real line lighting and the actual scanner, not visual judgment alone.
- Record fixture position, optics condition, and recipe version so the result can be repeated.
This is where many avoidable marking problems become visible early. A mark that only works on a polished sample under bench light is not qualified. A mark that survives the process but slows output too much is not qualified either. Good mark quality is always tied to both readability and throughput.
The qualification routine should also include a time element. Run a batch long enough to expose drift. If the first fifty parts mark cleanly but the next fifty show fading contrast, the process is not stable. The cause may be heat accumulation in the fixture, gradual contamination of the protective window, or a change in the material as the batch progresses. Whatever the cause, it will not appear in a five-part trial. Plan for a qualification run that matches the expected production batch size, or at least long enough to reveal thermal and optical drift.
Another often-missed step is verifying the mark after downstream processing. A mark that is applied before a washing step may lose contrast if the wash solution attacks the marked surface. A mark applied before powder coating may be completely covered. A mark applied before heat treatment may change appearance as the material transforms. The qualification routine must include the full process chain, not just the marking step in isolation.
If the marking project sits inside a wider plant-upgrade decision, the Pandaxis product catalog can help buyers review adjacent factory-equipment categories in the same planning cycle.
Production Takeaway: Laser Etching Machine for Metal
Improving mark quality on metal is usually less about chasing one stronger setting and more about tightening the full process window. The best results come from defining the right mark style, controlling surface condition, stabilizing part presentation, separating recipes by real material behavior, and validating marks after the downstream process has had a chance to expose weaknesses.
Factories that follow that logic usually see the same outcome: clearer codes, more consistent contrast, better edge definition, fewer scanner failures, and less time wasted on requalification and remarking. Better mark quality comes from process discipline first and machine selection second, even though both still matter.
The practical sequence for most shops is straightforward. Start by auditing the current failure modes and identifying which quality factors are actually failing. Then stabilize the part flow and fixturing before touching any parameters. Next, build a recipe matrix that separates jobs by material, finish, and end-use requirement. Finally, qualify each recipe against the full production environment, including downstream steps and scanner verification. Only after these steps have been exhausted should the conversation turn to machine replacement.
When machine replacement is justified, the buying decision should be driven by the process requirements identified during the audit. A shop that needs cosmetic stainless marking and scanner-critical codes will need different capabilities than a shop that only runs utility serial numbers. The machine that wins the demo may not be the machine that wins the production run. Evaluate pulse control, focus stability, motion accuracy, and the ability to maintain consistent results over long batches. These factors matter more than the marketing language on the spec sheet.
In the end, mark quality is a process problem, not a machine problem. The machine is a tool within that process, and its value depends entirely on how well the surrounding workflow supports it. Shops that treat marking as a disciplined process with defined inputs, controlled conditions, and verified outputs will consistently produce better marks than shops that rely on operator intuition and hope.